
 Scan on WeChat
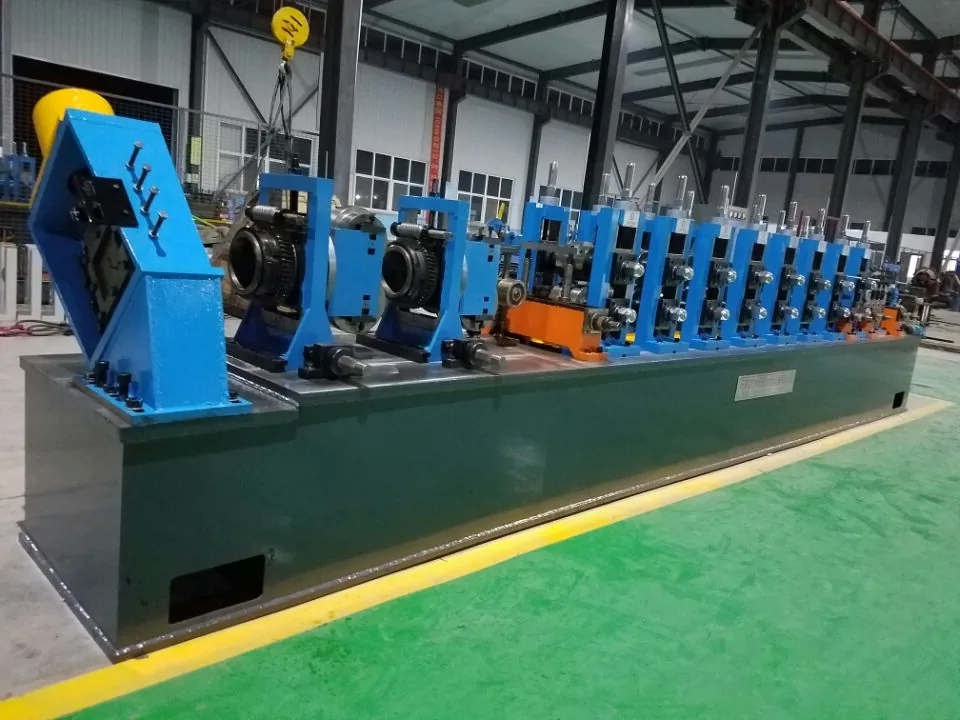
Roll forming is continuous bending: driven rolls press coil strip through one pass after another until it holds a fixed profile. Tengtian builds two kinds of line on that principle — one that closes the profile into a welded tube, one that leaves it open.
What Is the Roll Forming Process
On the purlin line the forming rolls are bearing steel, hardened after machining, and the dies and cutters are hardened Cr12. In the roll forming process the forming rolls turn continuously and press the strip, so the flat band is bent a little further at every pass until it reaches the intended shape. Nothing is heated to change the metal; the shape comes from the passes alone.
On a purlin line the same principle is used at room temperature to make an open section: the strip is stepped through eighteen passes into a C, Z or Ω profile. There is no phase change — the metal is worked purely plastically.
Here the variables are the pass count, the roll profile and the yield strength of the material, and they decide the geometric accuracy of the section and how much springback has to be controlled out.
Two consequences of that follow on the equipment side. The first is that roll passes are not only used before the weld: on a tube line the strip is cooled after welding and then run through sizing rolls and a straightener, so the final outside diameter and the straightness of the tube are also set by rolls. The second is what the roll set has to be changed for.
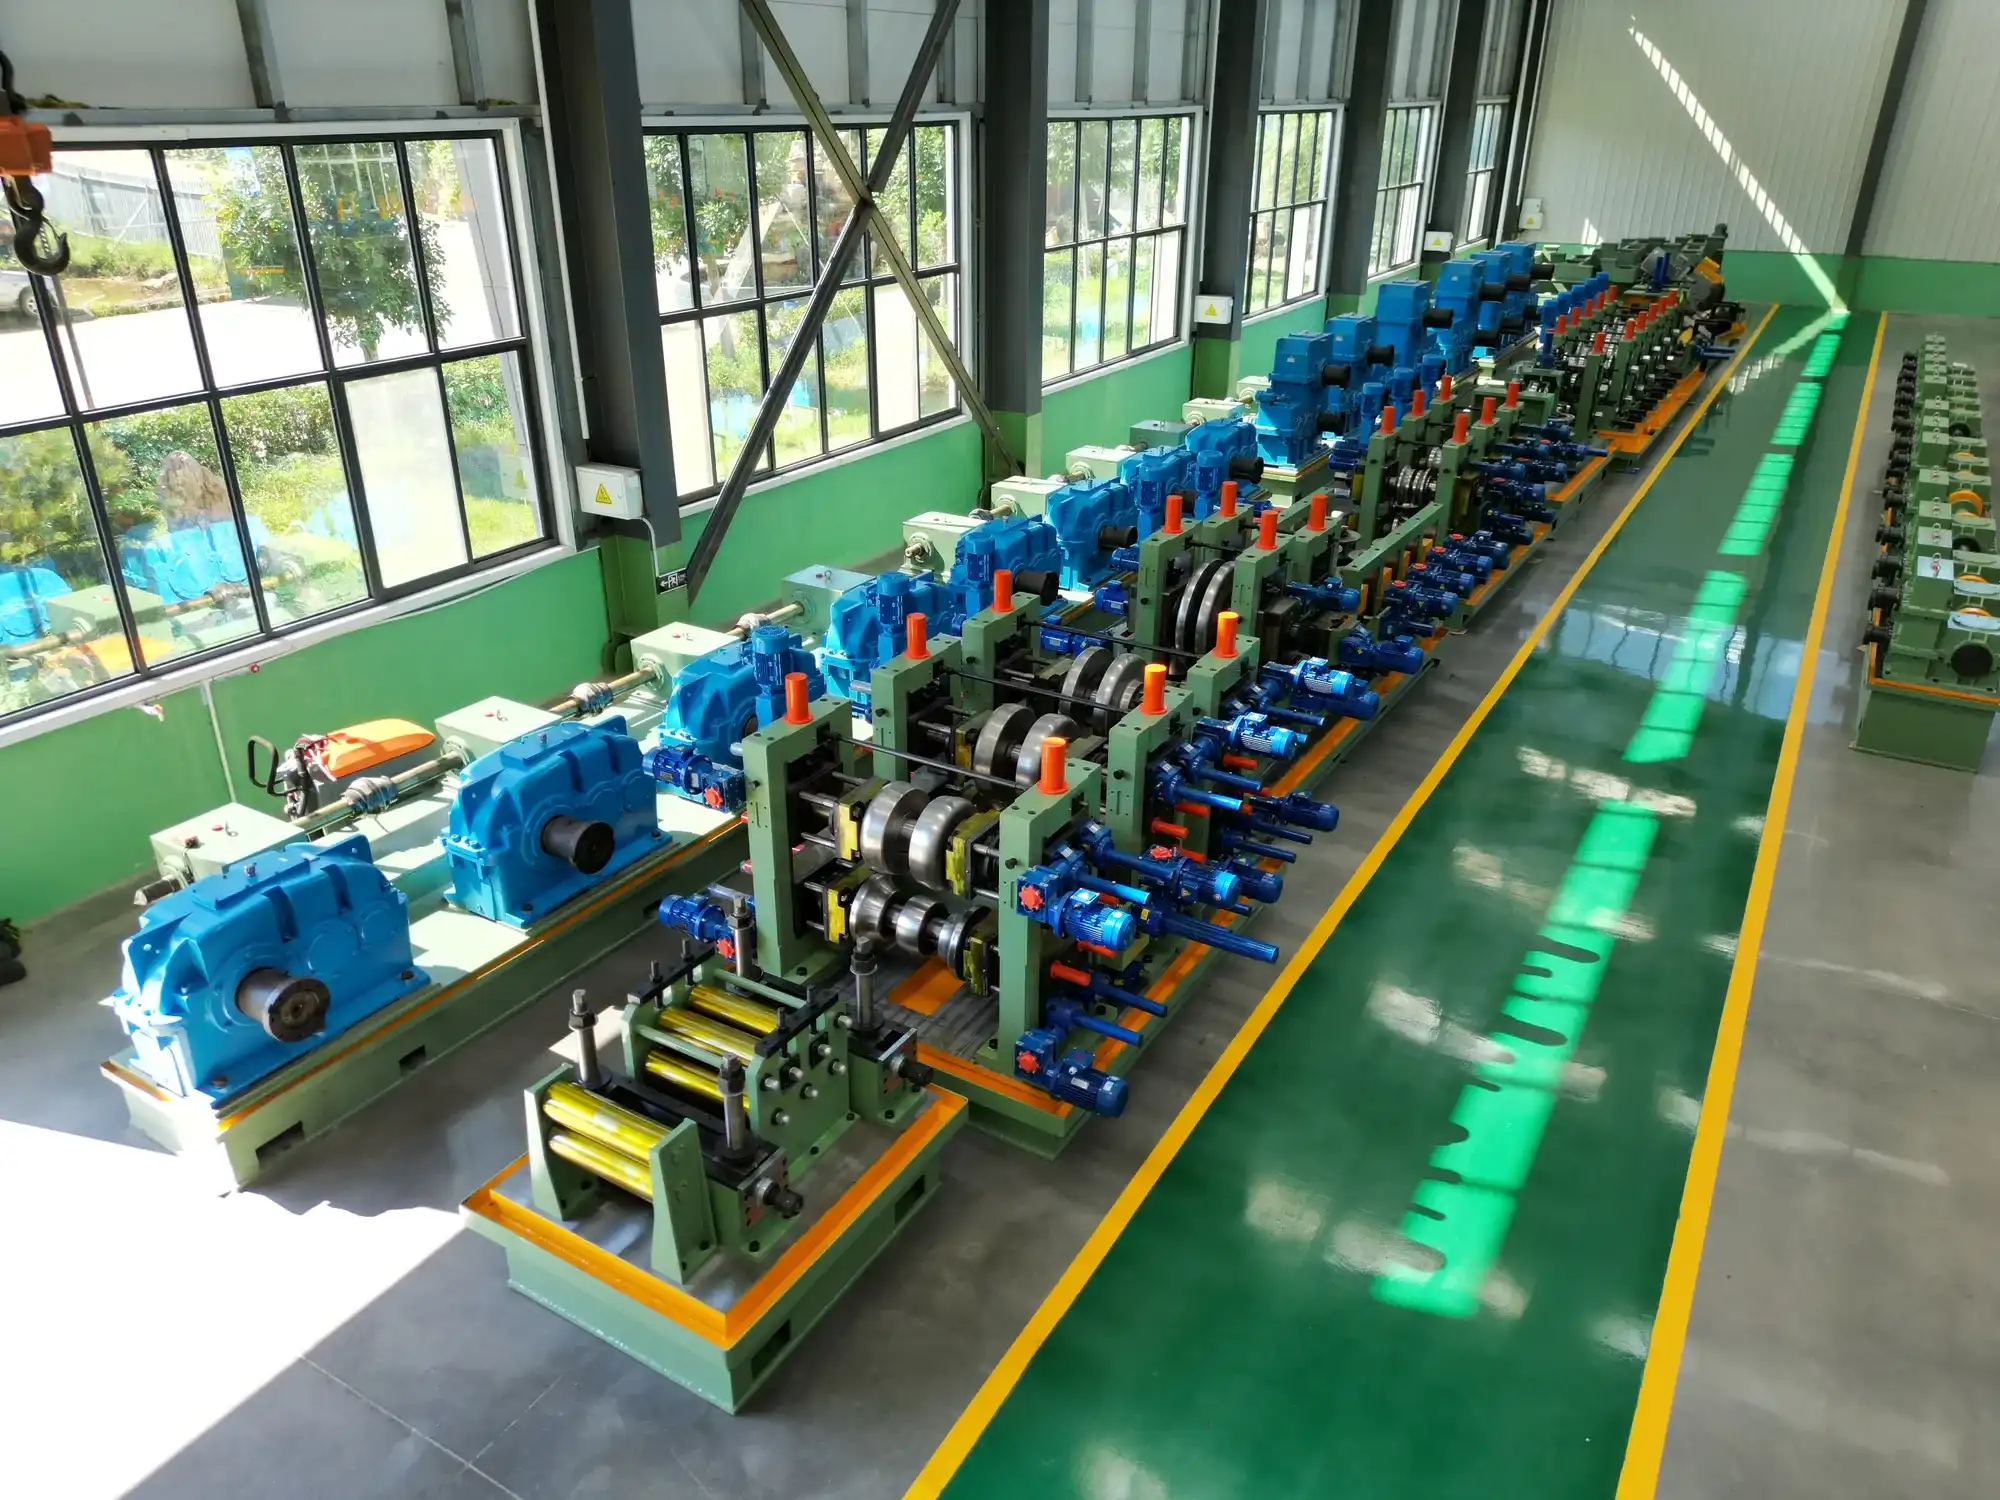
The purlin line is a semi-automatic C / Z interchangeable line: one set of tooling covers several sizes by stepless adjustment, and changing size needs no roll change at all. It runs strip 2 to 4 mm thick at forming speeds up to 20 m/min, and it punches, forms and cuts from the length, hole pitch and quantity that the operator enters.
There is no welding anywhere on it — that is what separates a cold roll forming line from a tube mill.
| Roll forming into a welded tube | Cold roll forming into an open section | |
|---|---|---|
| What comes off the line | round or square open tube blank, then closed and welded | C / Z / Ω open profile, not welded |
| Variables the line is set on | pass count · roll gap · roll profile | pass count · roll profile · material yield |
| What those variables decide | tube shape accuracy and weld-seam alignment | section geometry and springback control |
| Changing size | conventional line changes the rolls; the direct-square line adjusts by servo without a roll change | stepless adjustment, no roll change |
In roll forming process which rollers are used
Rolls, dies and cutters are carried as wear parts, one set supplied with the line, and the dies are reground or replaced on punch count.
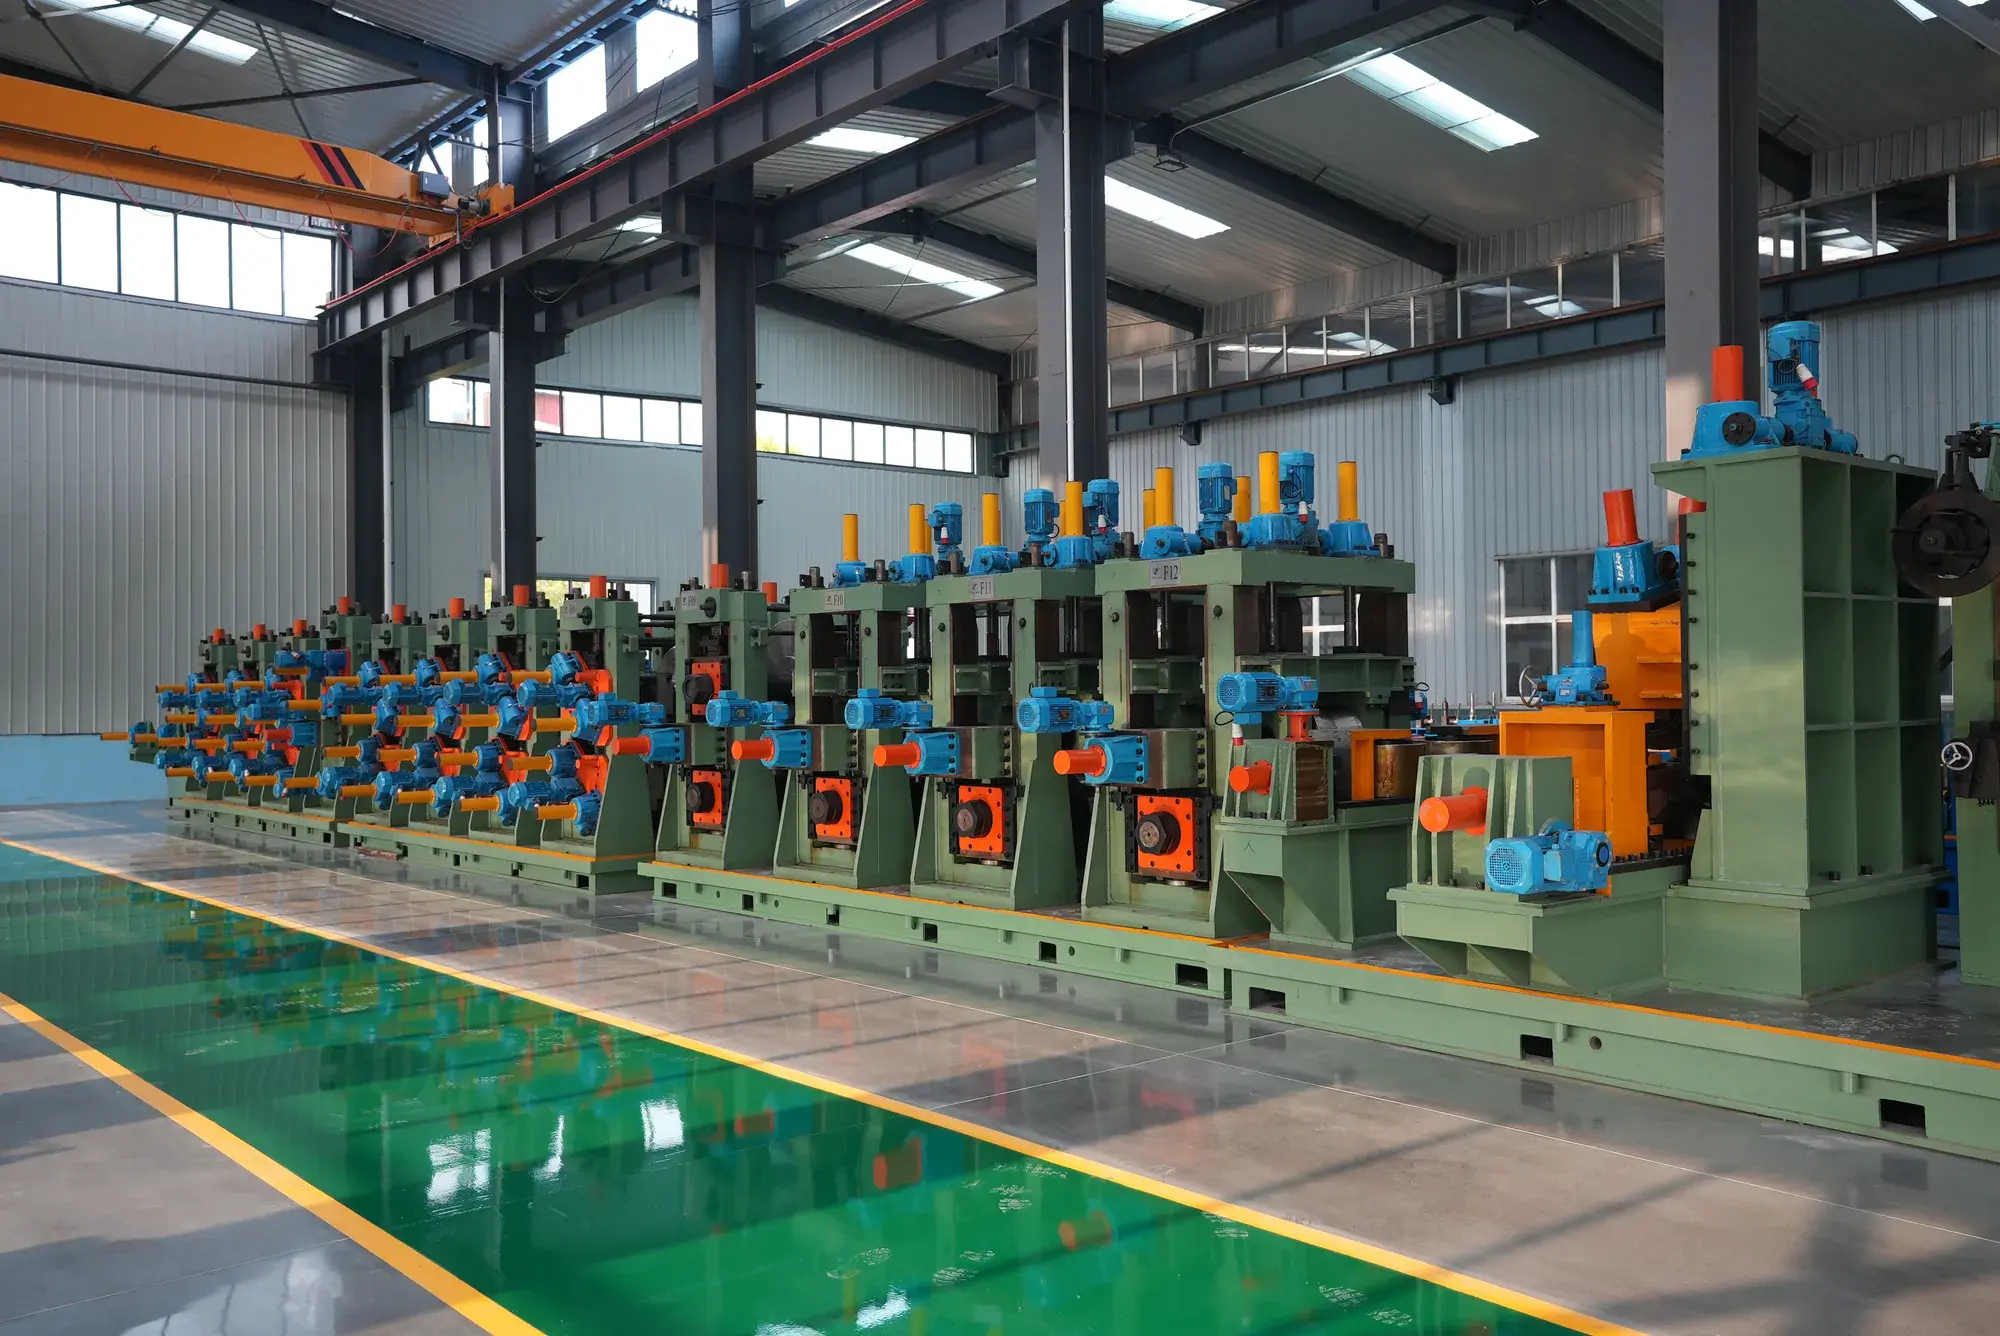
On a welded tube line the passes bend flat strip progressively into a round or square open tube blank, which is then closed and welded. The variables the line is set on are the number of passes, the roll gap and the roll profile, and between them they decide how true the tube runs and whether the two strip edges meet the weld point in line.
Frequently Asked Questions
Does anything on a roll forming line get heated?
Nothing is heated to change the metal — the shape comes from the passes alone, and there is no phase change. On a purlin line the same principle is used at room temperature to make an open section.
How many passes does a purlin profile take?
The strip is stepped through eighteen passes into a C, Z or Ω profile. Pass count, roll profile and the yield strength of the material decide the geometric accuracy of the section and how much springback has to be controlled out.
Does changing size mean changing the rolls?
Not on the purlin line: one set of tooling covers several sizes by stepless adjustment, and changing size needs no roll change at all. A conventional tube line does change the rolls; the direct-square line adjusts by servo without a roll change.
What is carried as a wear part?
Rolls, dies and cutters are carried as wear parts, one set supplied with the line, and the dies are reground or replaced on punch count.
From the Workshop
Send Your Enquiry
Tell us the pipe outside-diameter range, the wall thickness and the output you need. An engineer reads every enquiry — it does not land in a general sales inbox.