
 Scan on WeChat
Φ10 to Φ1620 mm. Two Welding Technologies. One Works.
HFW longitudinal mills in 12 diameter steps from HG32 to HG630, plus SSAW spiral lines for large-diameter pipe. You specify the pipe; we specify the line.
Scope of Supply and Acceptance Criteria — Set Out in Writing Before You Order.
Unit-by-unit scope, commissioning responsibility and the acceptance criteria your line will be signed off against. Set out up front, not negotiated after the deposit.
Built for Distributors and System Integrators.
Tiered configurations with resale margin built in, territory support, and parts supply from our own CNC shop. 22 partner programmes, published in full.
Production Lines We Build
Thirteen line types built in this works. Click any card for specifications, model steps and line video.
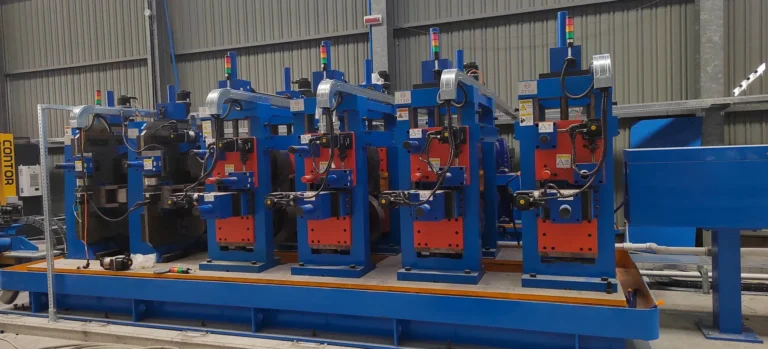 Tube Mill (HFW)Φ10–630 mm high-frequency welded pipe linesView Details →
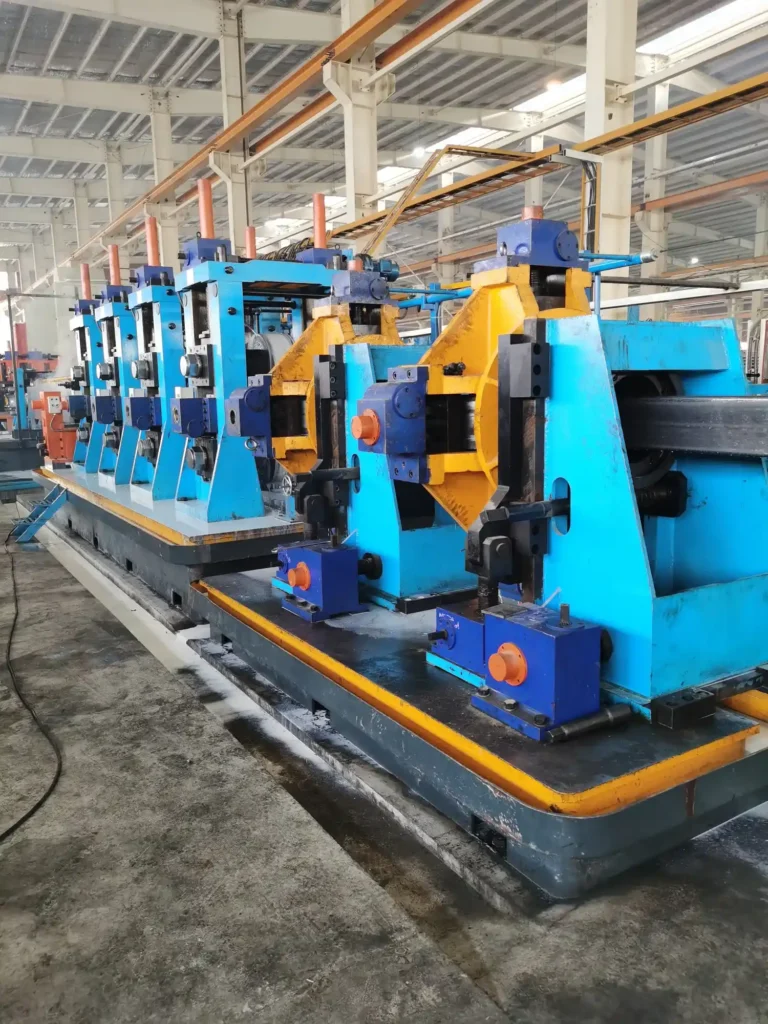 High Frequency Welded Pipe MillSolid-state HF welder, 150–600 kWView Details →
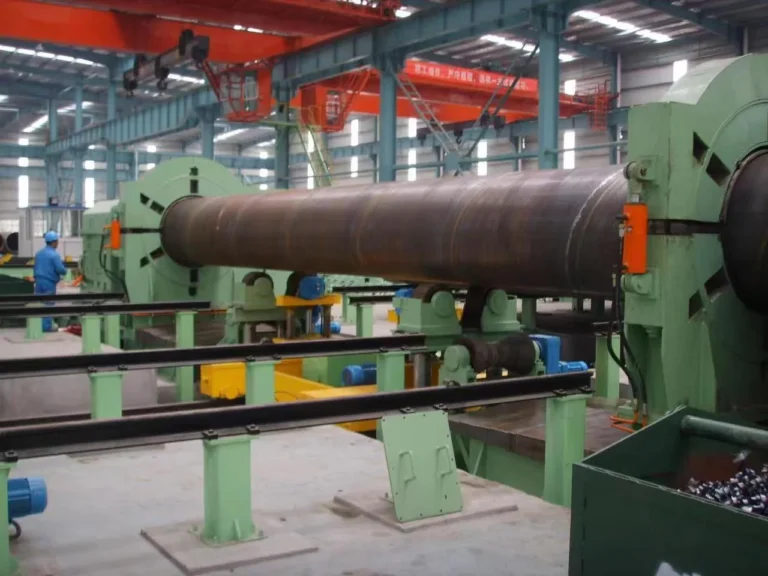 SSAW Spiral Welded Pipe MillΦ219–1620 mm, double-sided SAWView Details →
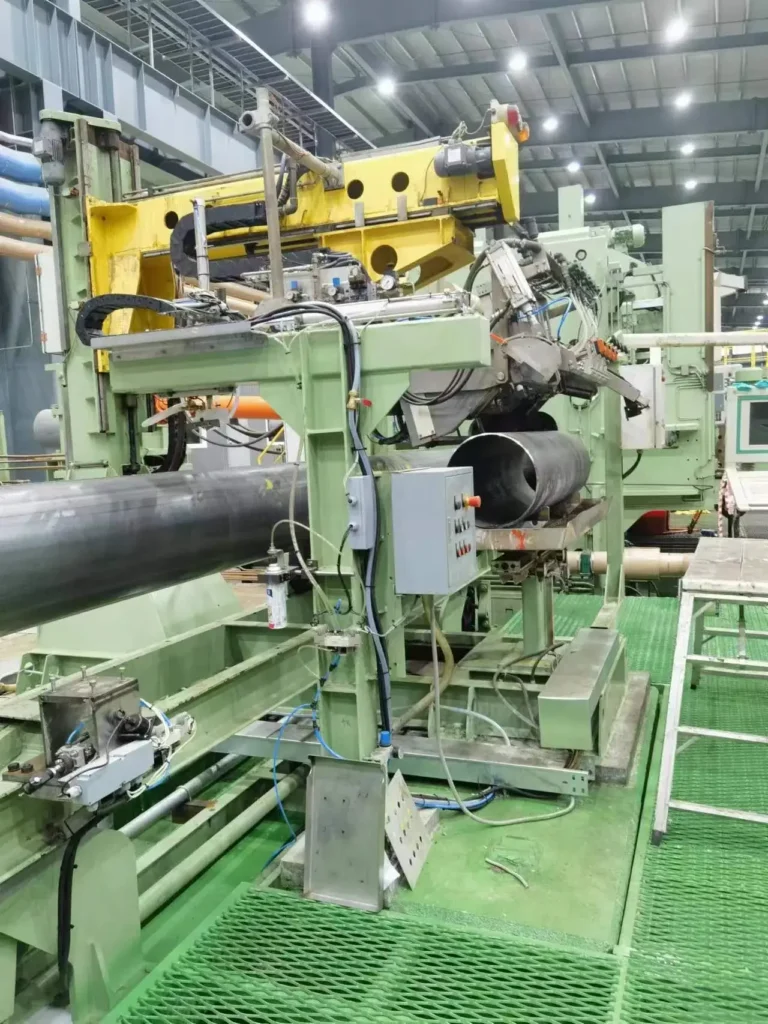 API Line Pipe MillAPI SPEC 5L inspection chainView Details →
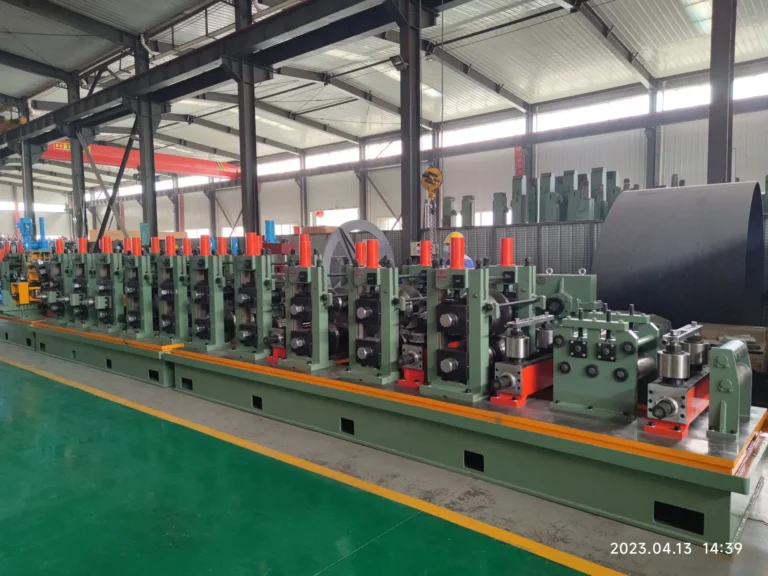 Direct Forming Square Tube Mill120×120 to 400×400 mm, no roll changeView Details →
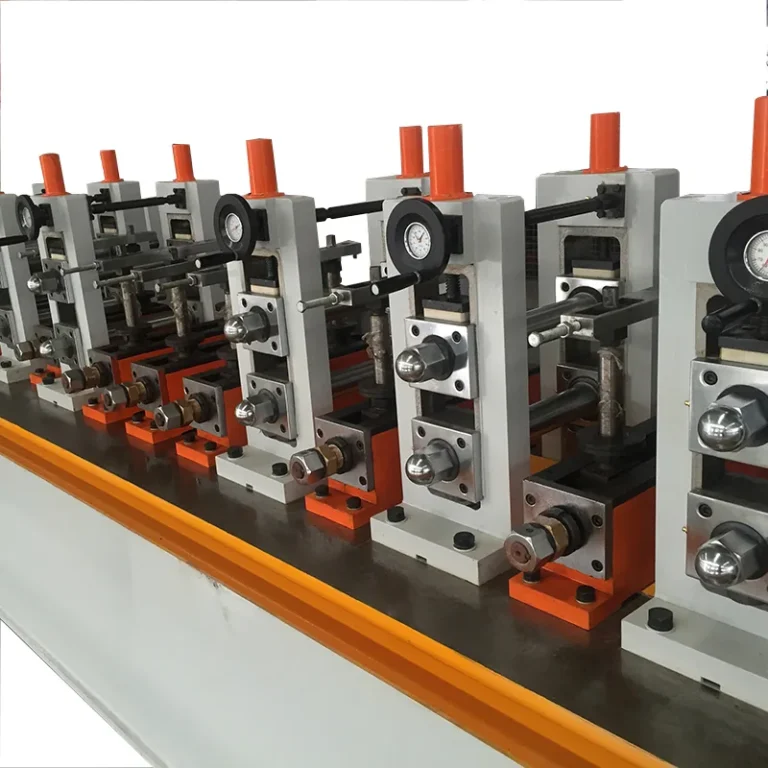 Small Diameter Tube MillHG32 · HG50 · HG76 · HG89 · HG114View Details →
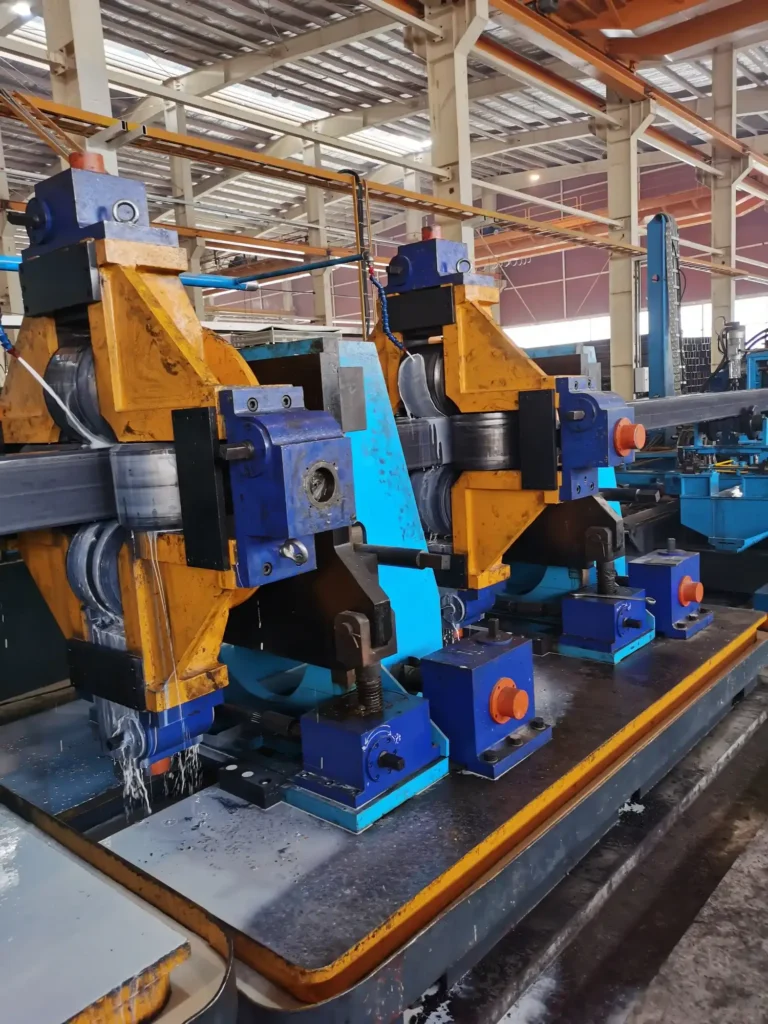 Large Diameter Tube MillHG165 · HG219 · HG273 · HG325 · HG426 · HG508 · HG630View Details →
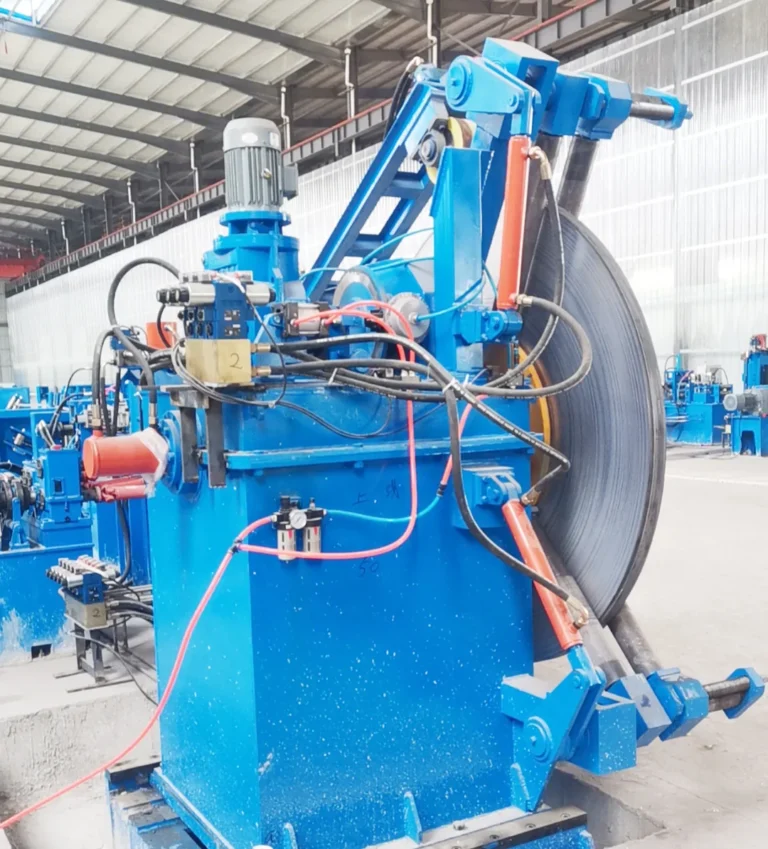
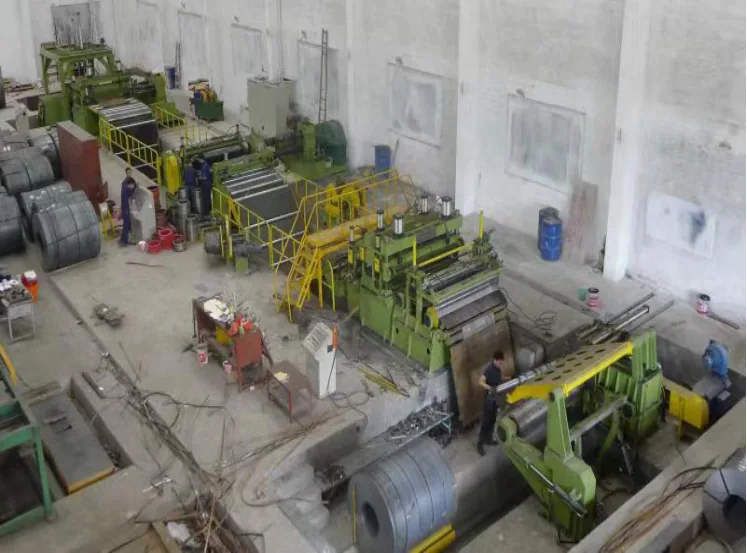 Coil Slitting Line±0.2 mm width, camber ≤0.5 mm/1000 mm (coil width ≥200 mm)View Details →Cut-to-Length LineCoil to sheet, up to 32 t coilView Details →
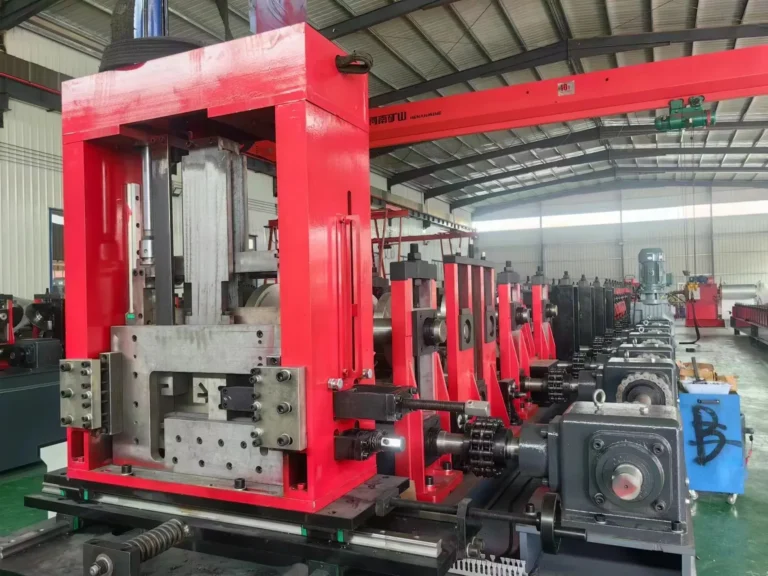 Cold Roll Forming MachineTooling and die design in-houseView Details →
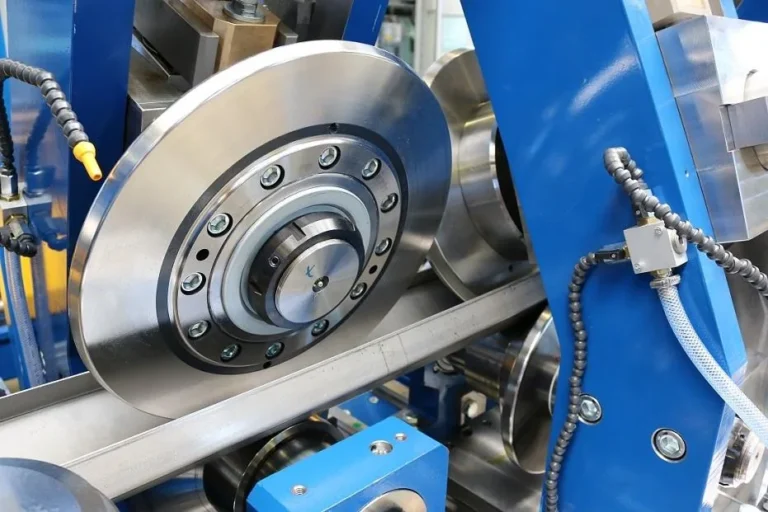 Purlin Roll Forming MachineC / Z / Ω profiles, 18-pass, 20 m/minView Details →
 H-Beam Production LineHFW H-beam to GOST R 58966-2020View Details →
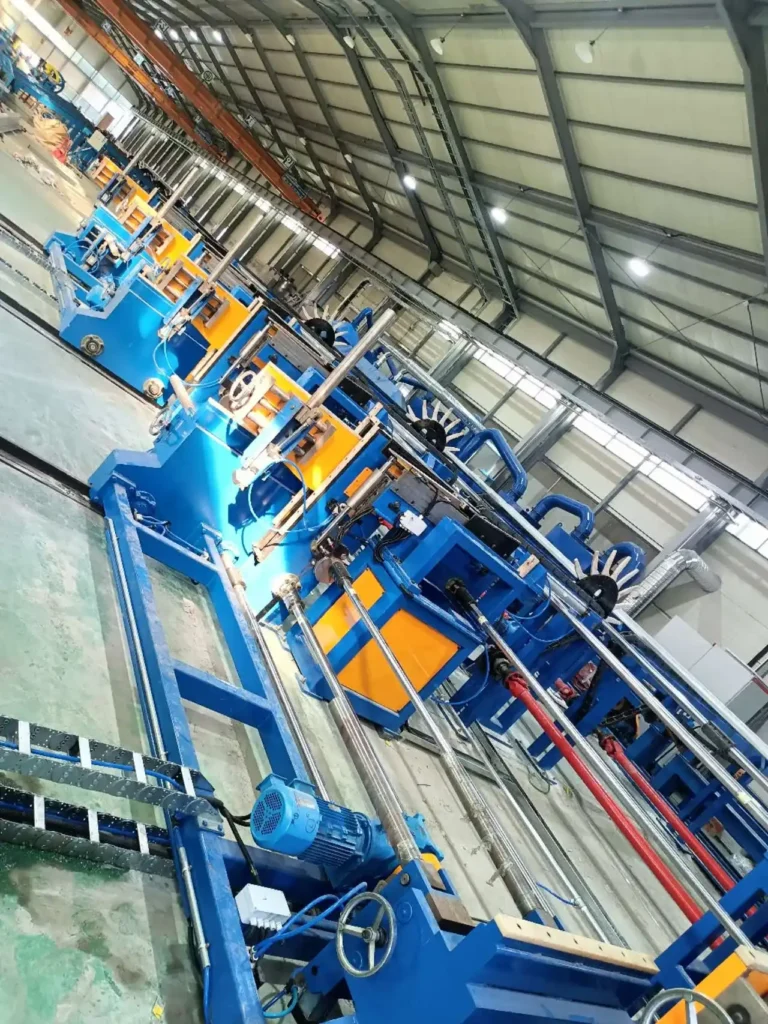 Auto Spray Paint LineIn-line tube coating, up to 60 m/minView Details →
How We Build Them
Everything below is built in our own plant in Zanhuang, Hebei — including the forming rolls and key wear parts, machined on our own CNC equipment, so spare-part supply does not depend on a third-party shop.
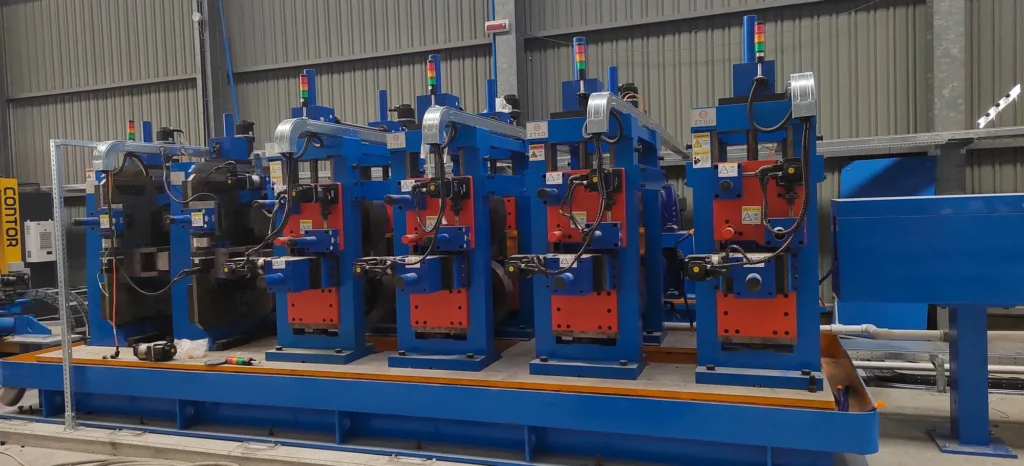 Rolls and Stands Cut in Our Own CNC ShopΦ10–630 mm round, square and rectangular pipe. Twelve model steps, HG32 through HG630.See How →
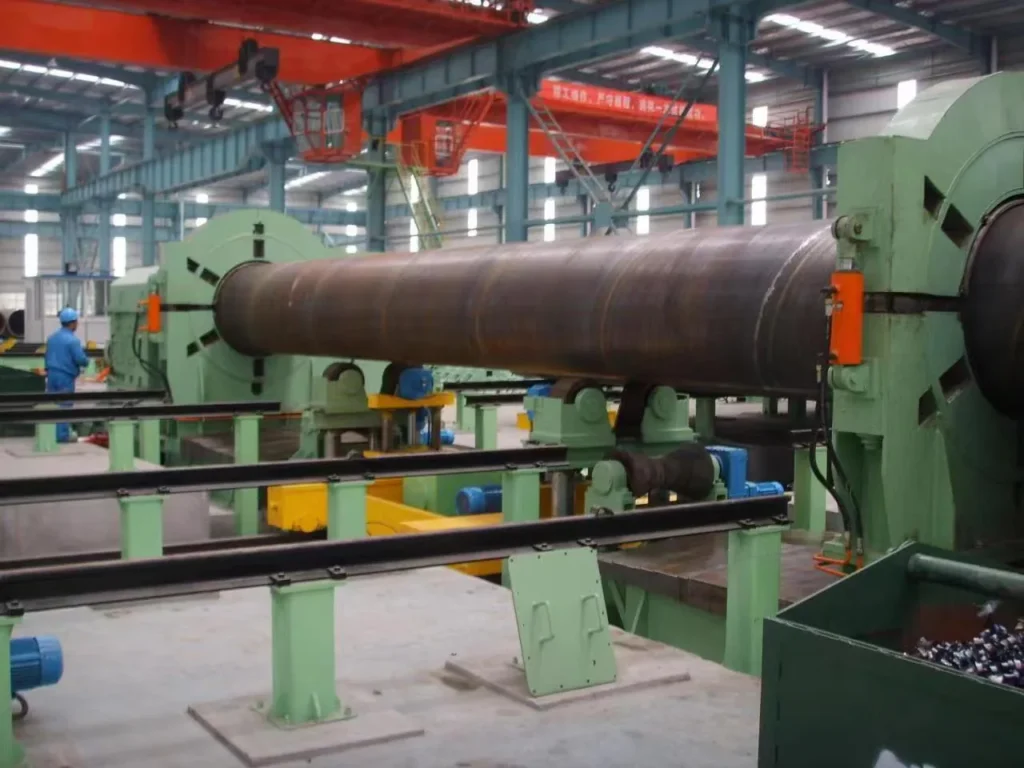 Three Rolls Set the Forming AngleΦ219–1620 mm × 5–16 mm. Bore changed by forming angle, not by changing rolls.See How →
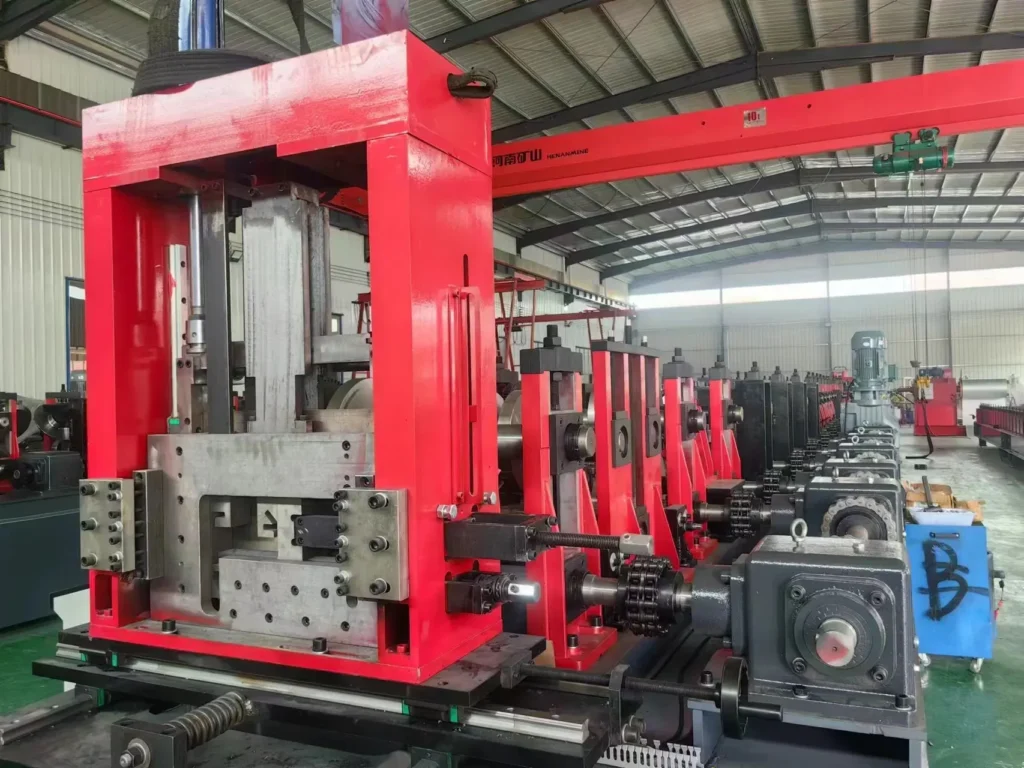 Formed Cold, Step by StepC, Z and Ω purlin and open sections, with tooling and die design done in-house.See How →
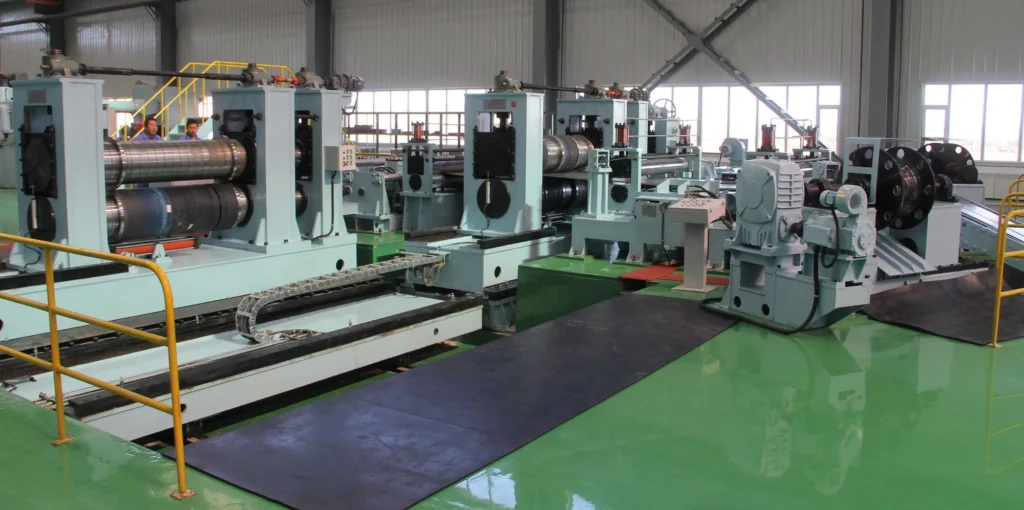 Knives and Spacers Set to Strip ThicknessCoil preparation upstream of any mill — ±0.2 mm width, coils up to 32 t.See How →
See the Lines Running
Filmed in our own workshop during production and factory acceptance — not rendered, not stock footage.


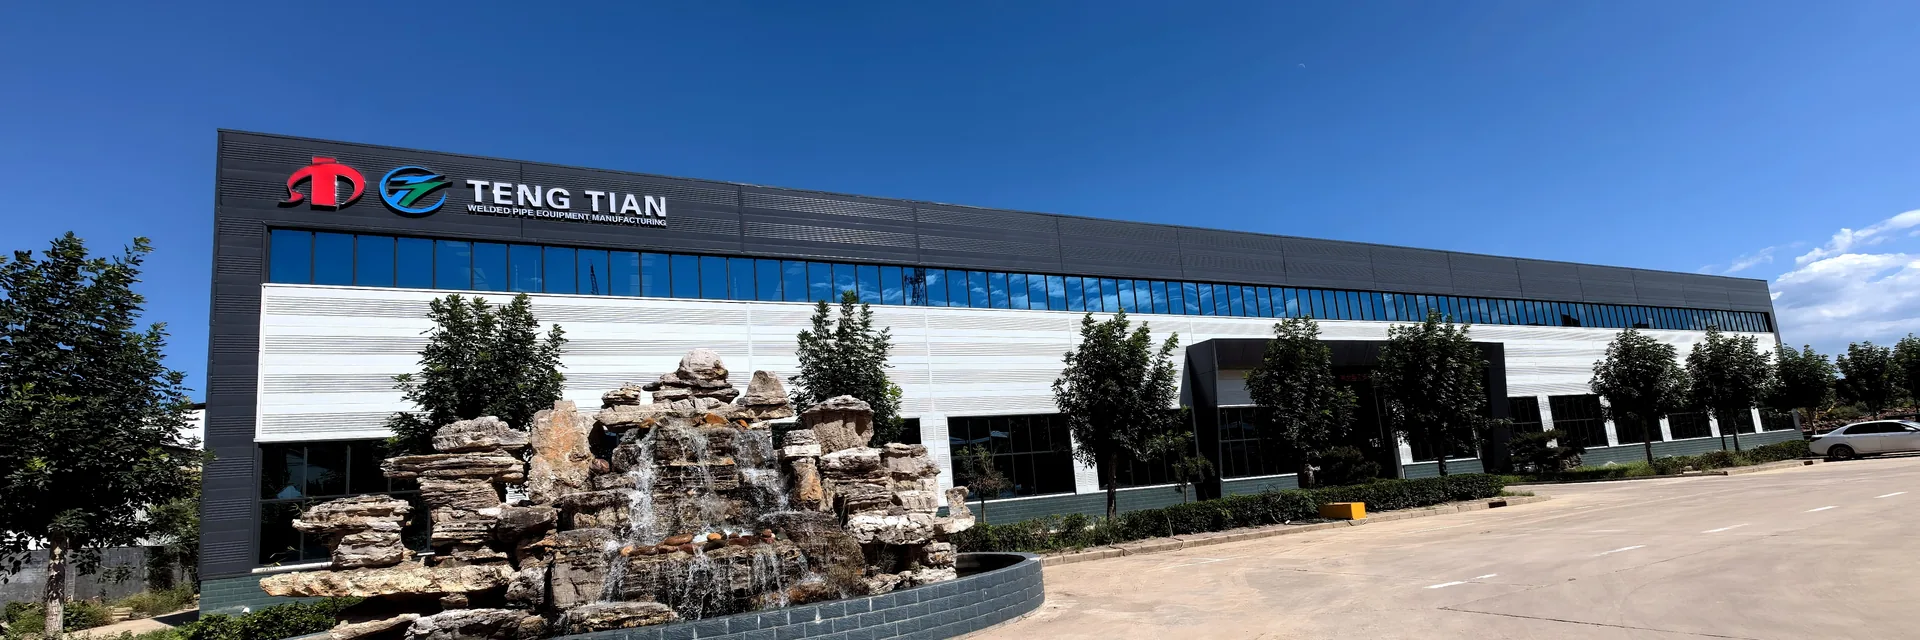
A Manufacturer, Not a Trading Company
Tengtian has built welded pipe and tube mills at its own works in Zanhuang, Hebei since 2014. Roll design, CNC machining of rolls and stands, mechanical assembly and electrical integration all happen on our own floor, in our own machining centre — you are buying from the people who cut the metal.
That floor covers the whole diameter range. High-frequency welded lines from Φ10 mm to Φ630 mm, spiral (SSAW) lines from Φ219 mm to Φ1620 mm, round, square and rectangular sections from the same mills. W, FFX and FF forming are all available, and every roll pass is designed in COPRA, the German roll-forming software.
An in-house innovation centre, opened in 2017, is where new pass designs are worked out by our own core R&D engineers — the same people who answer your technical questions and who see the line through manufacture, shipment, installation and commissioning at your plant.
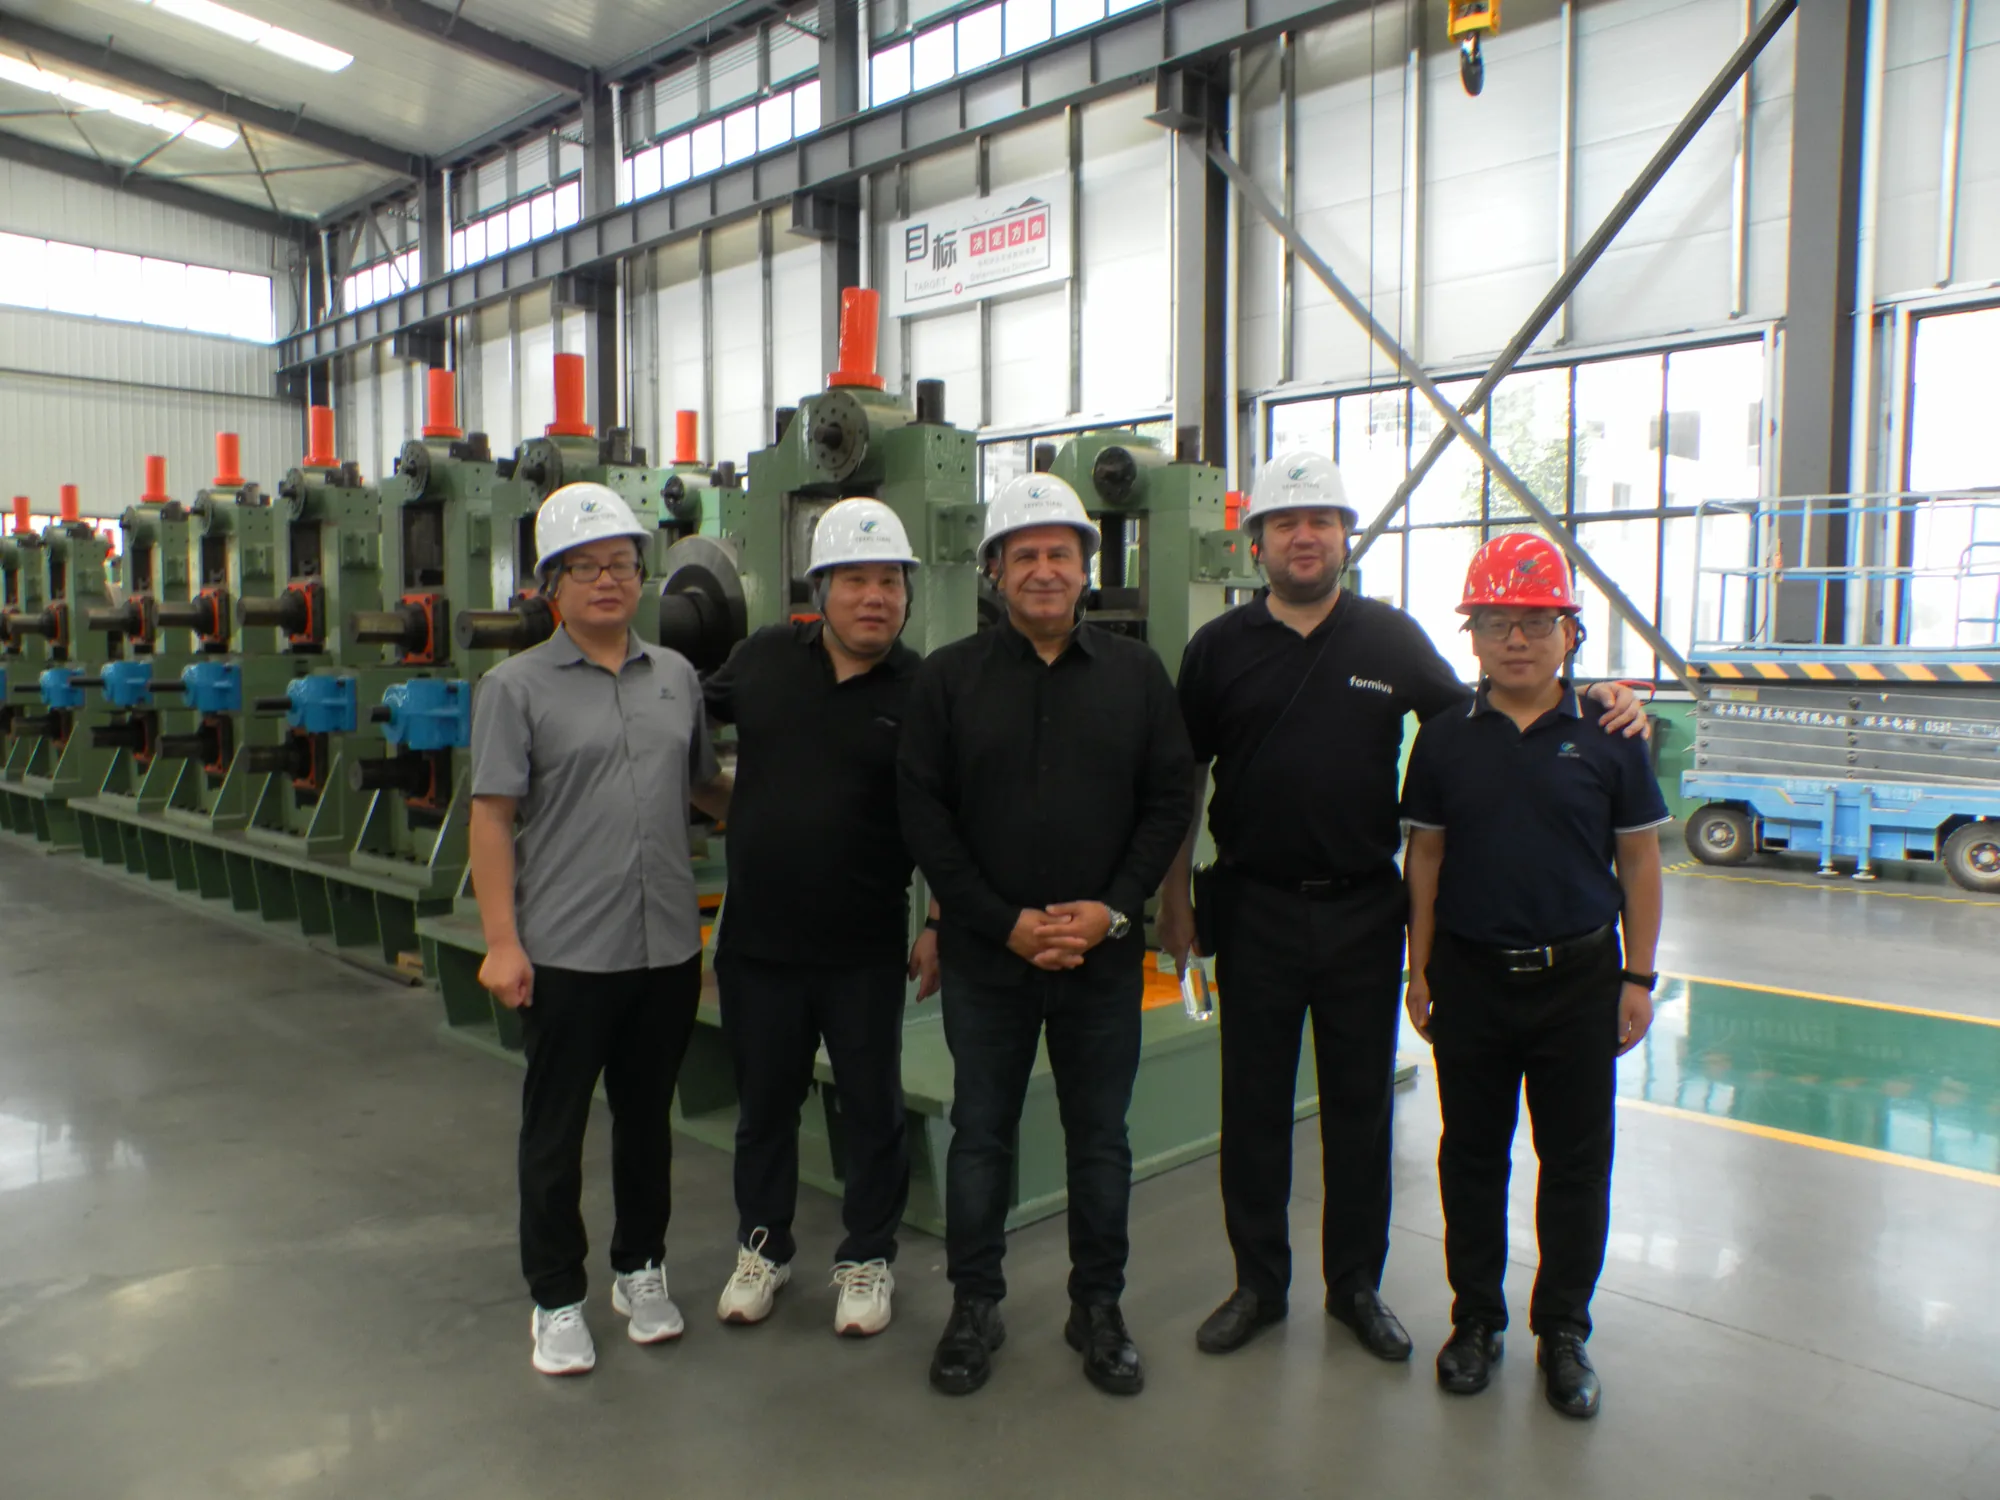
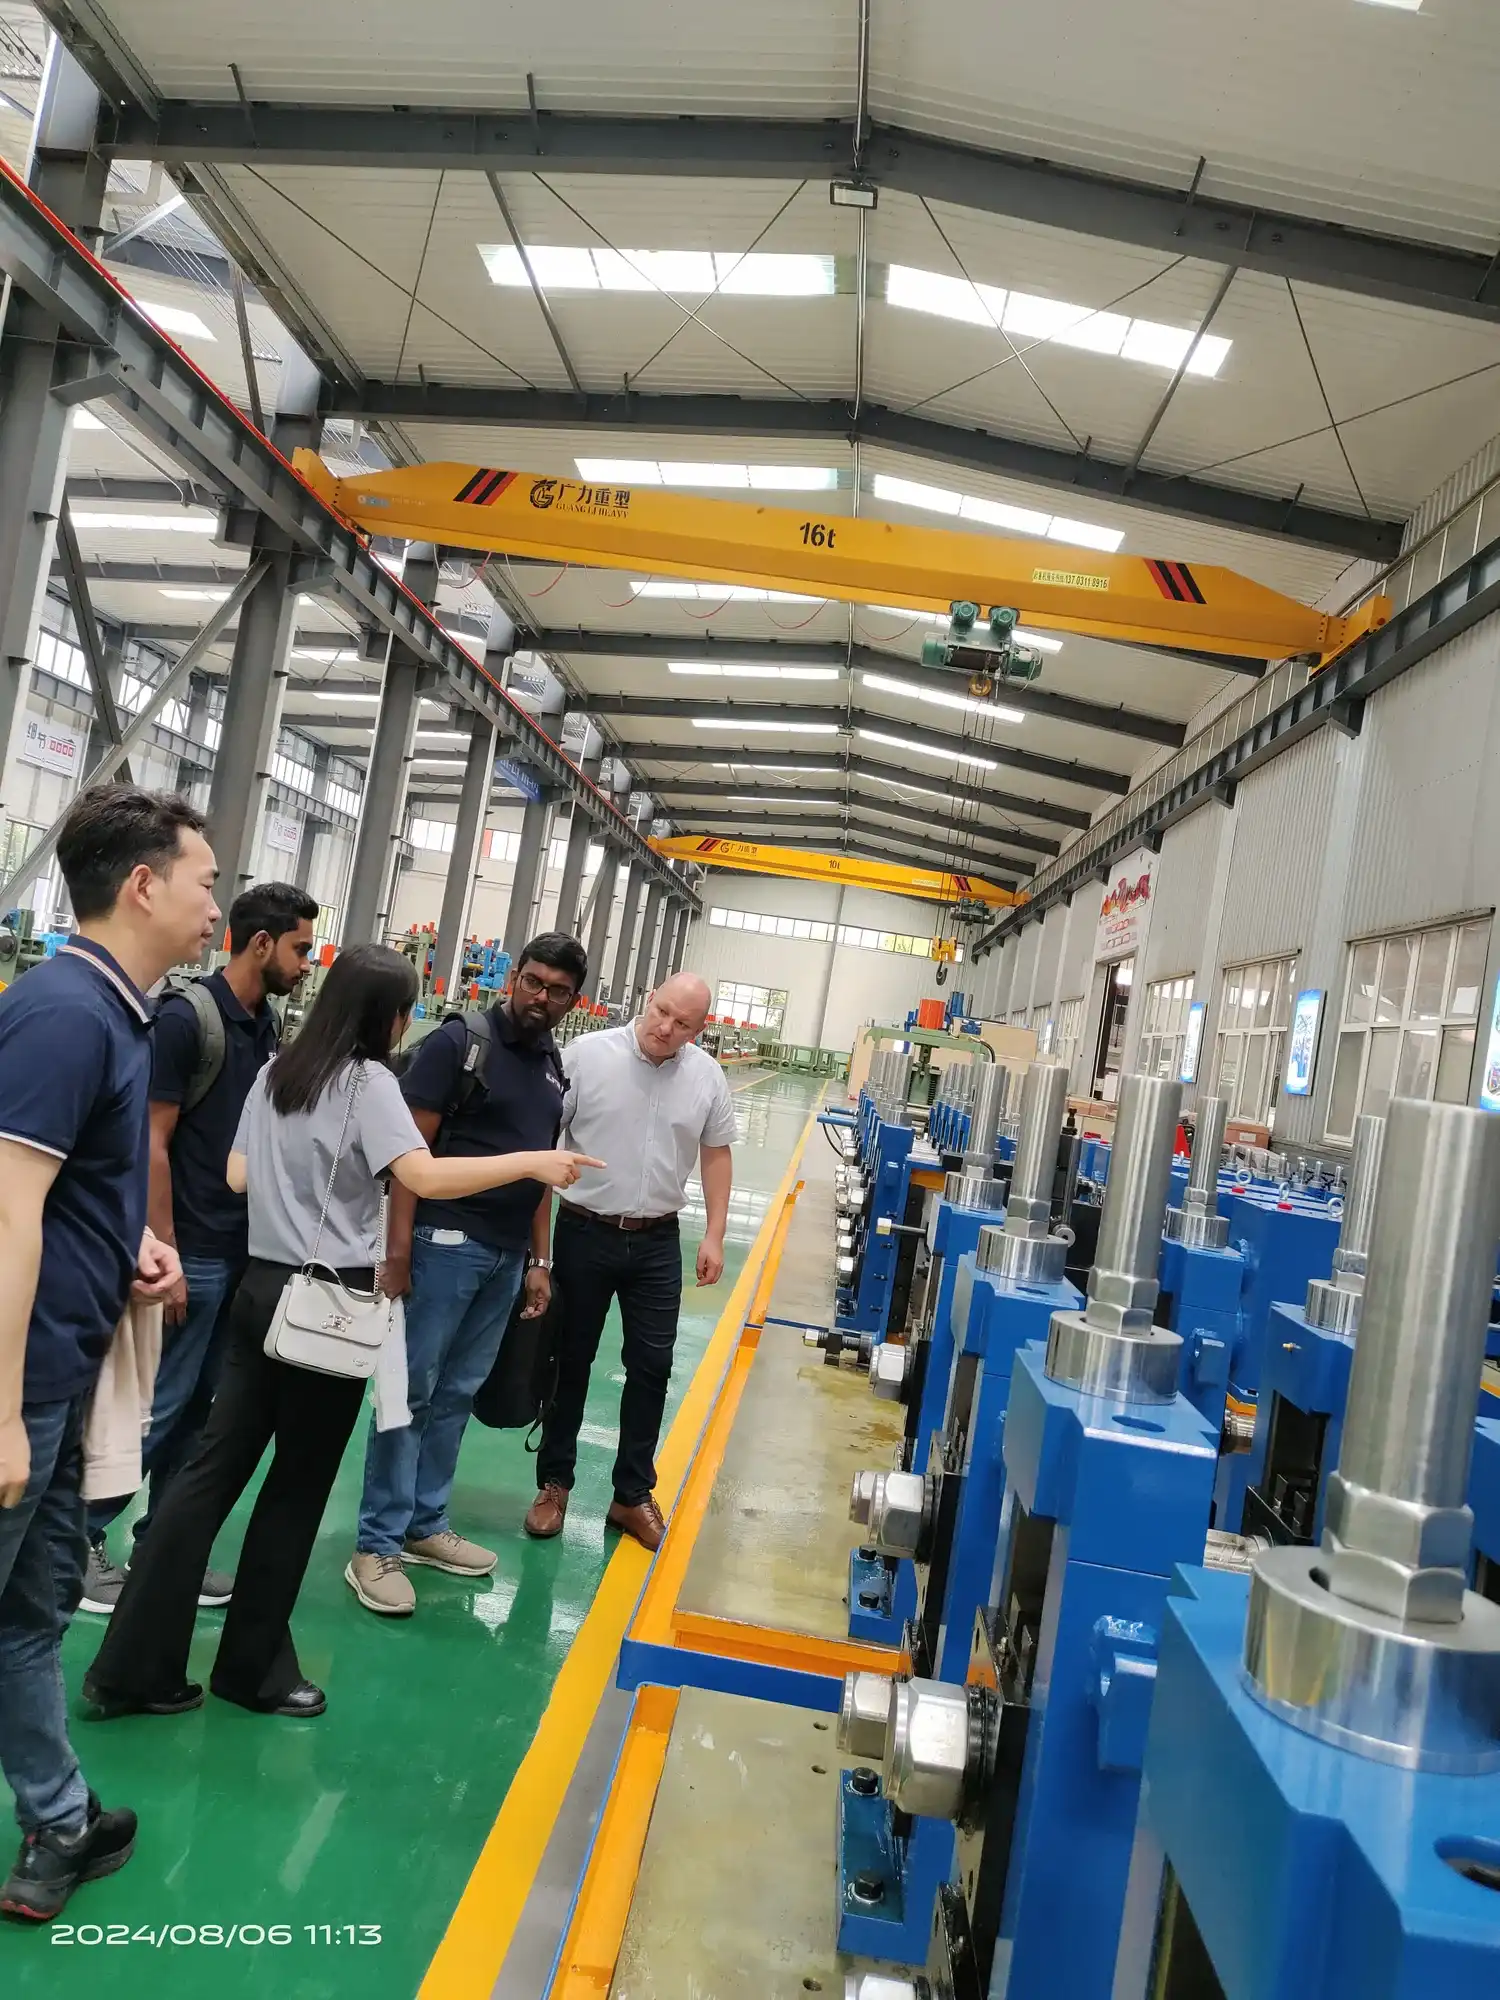
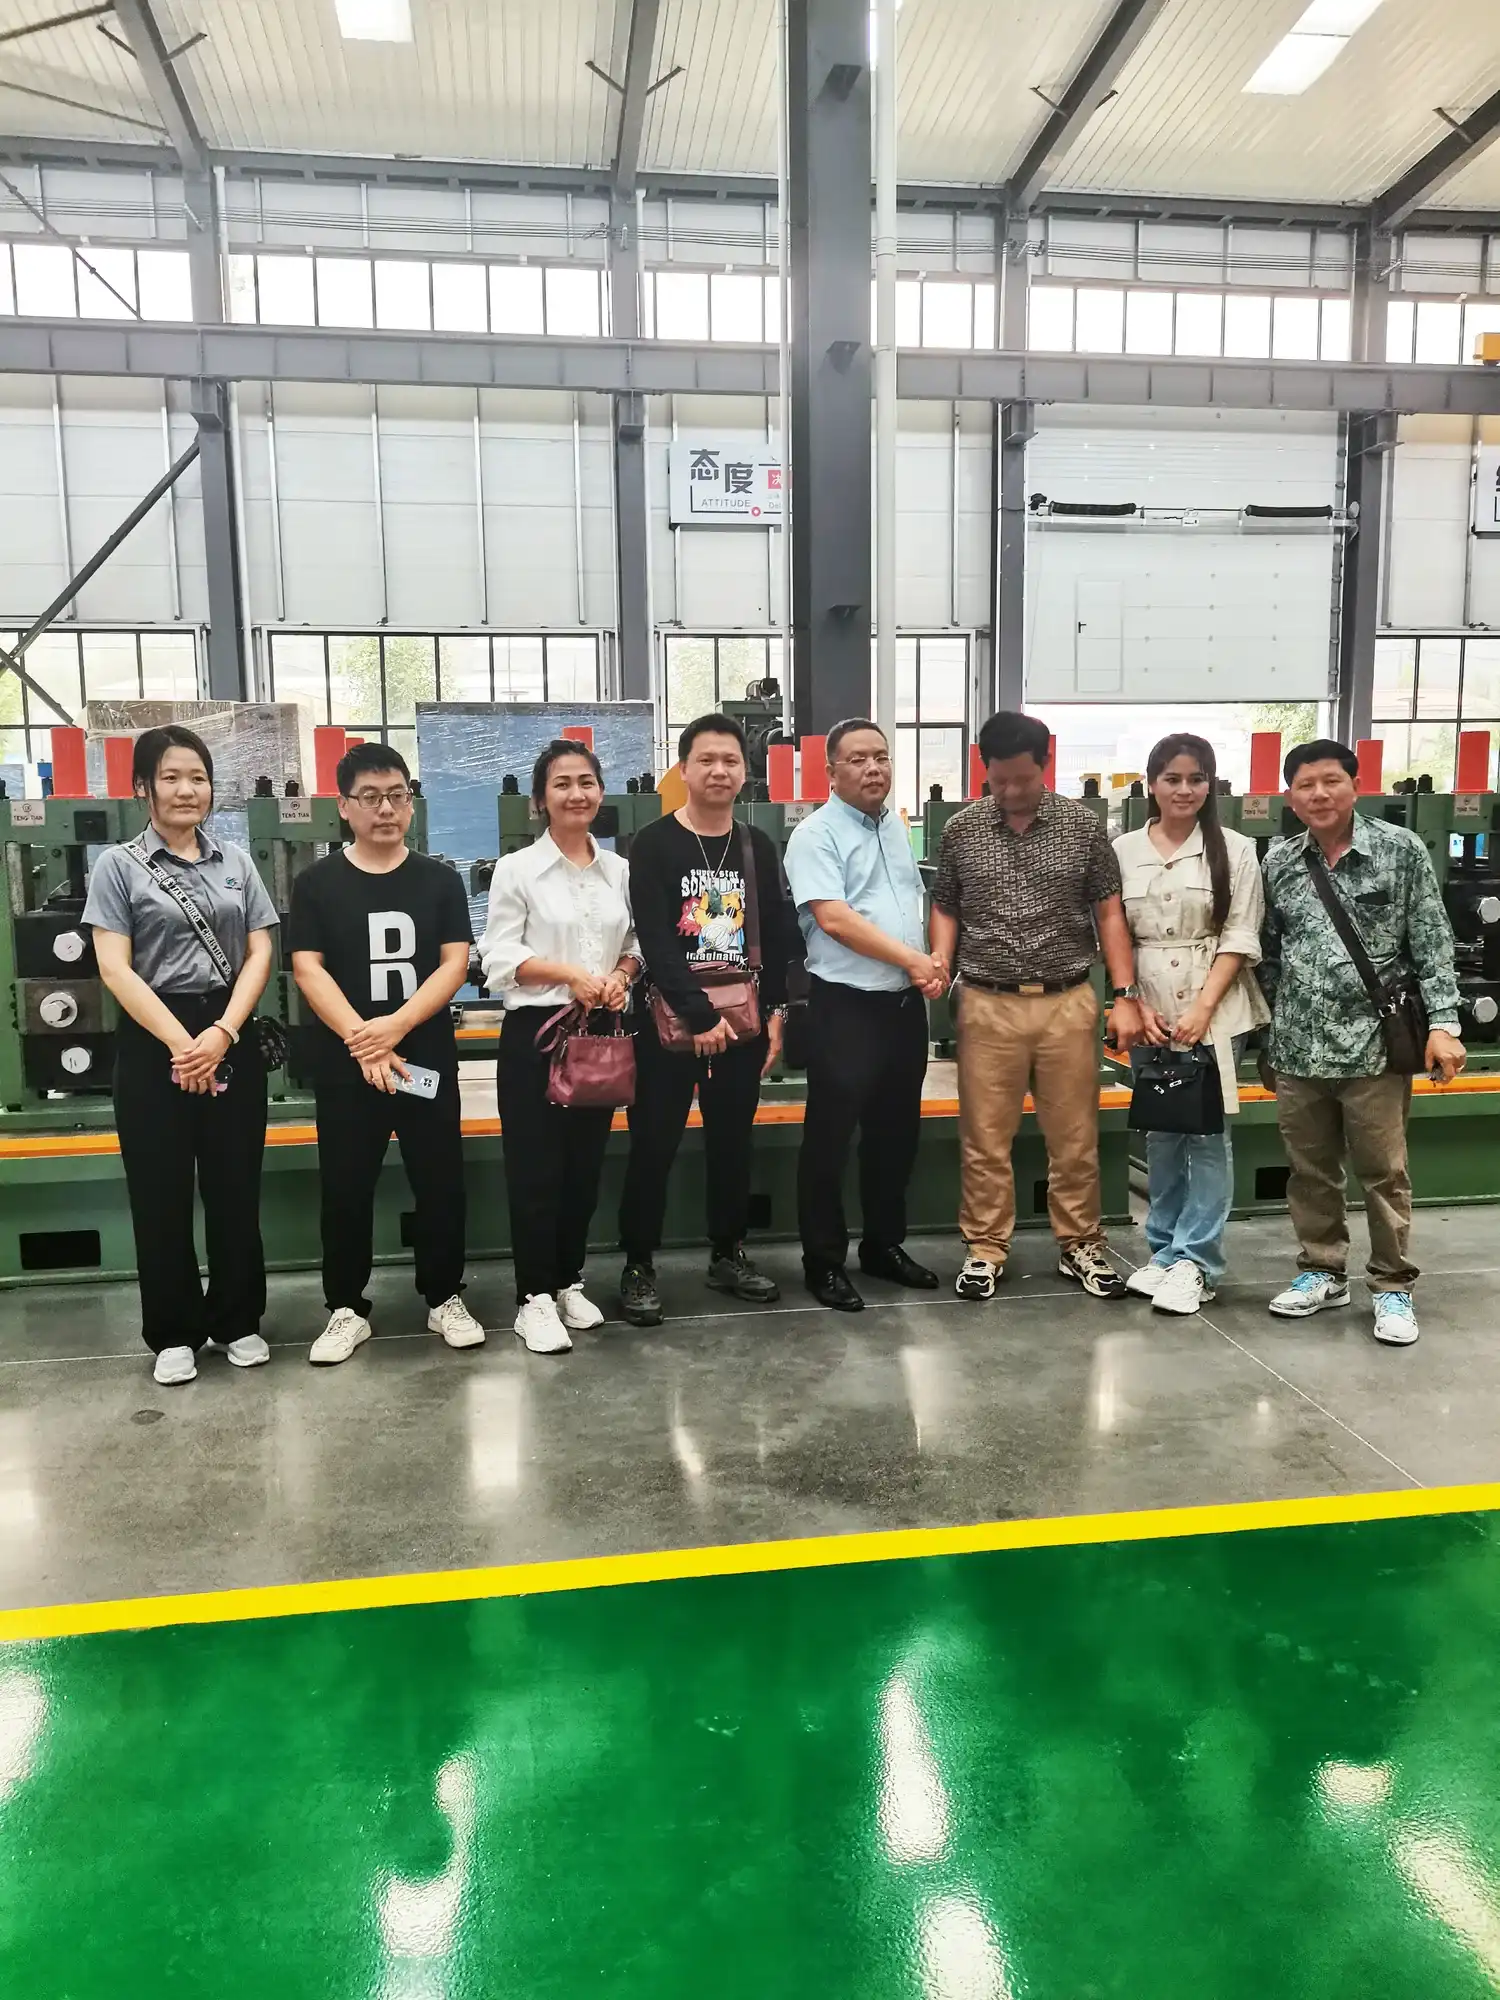
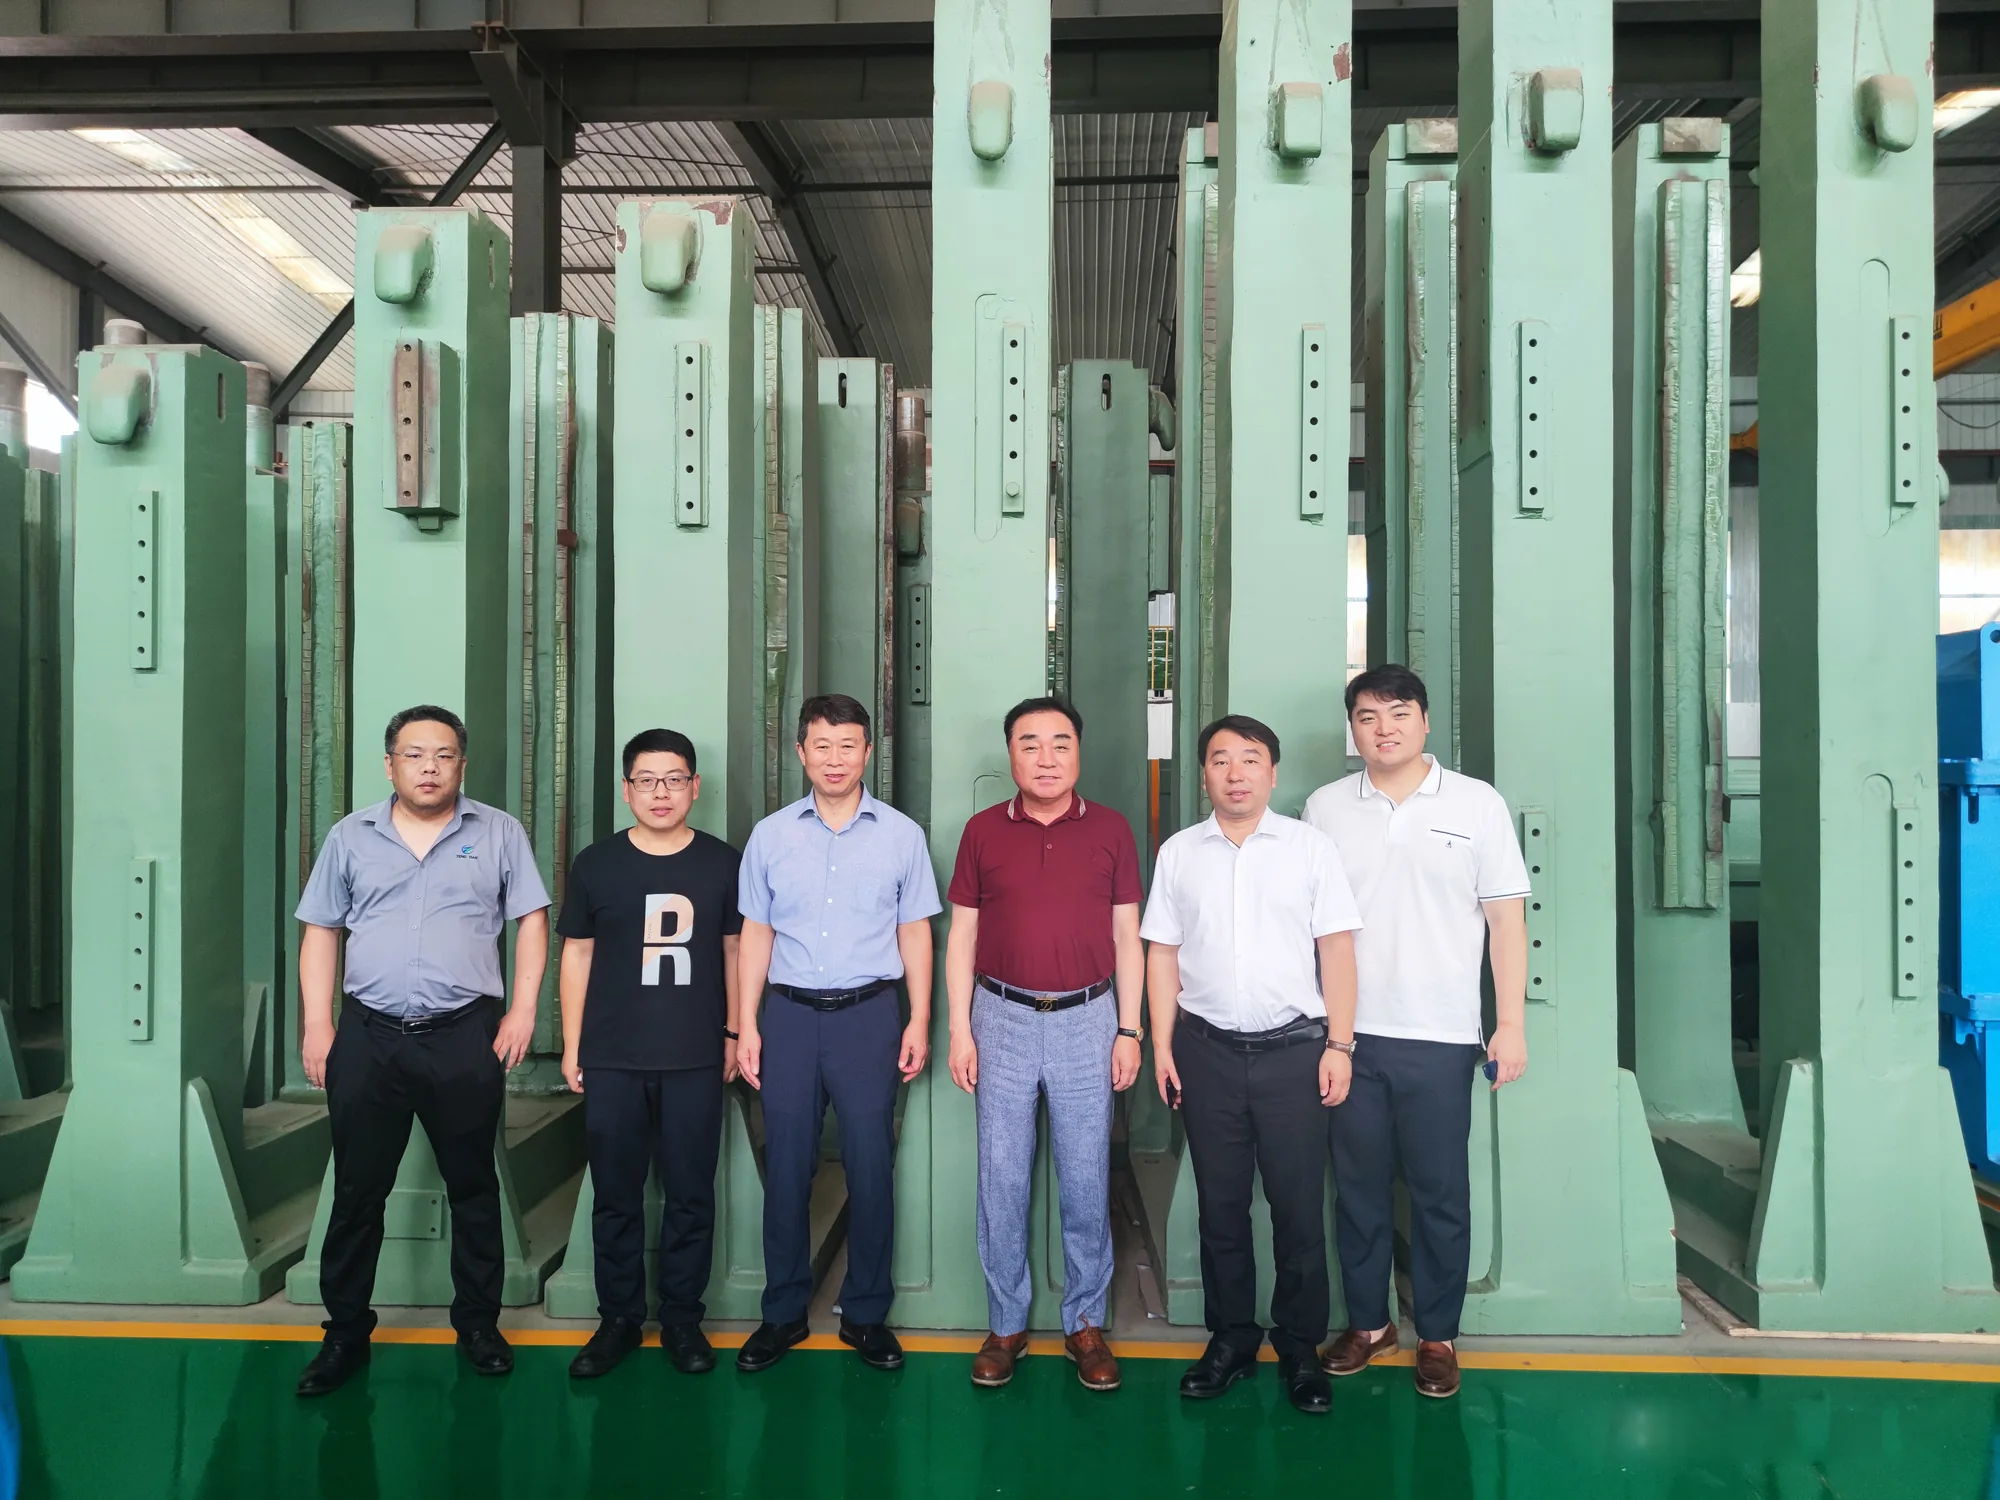
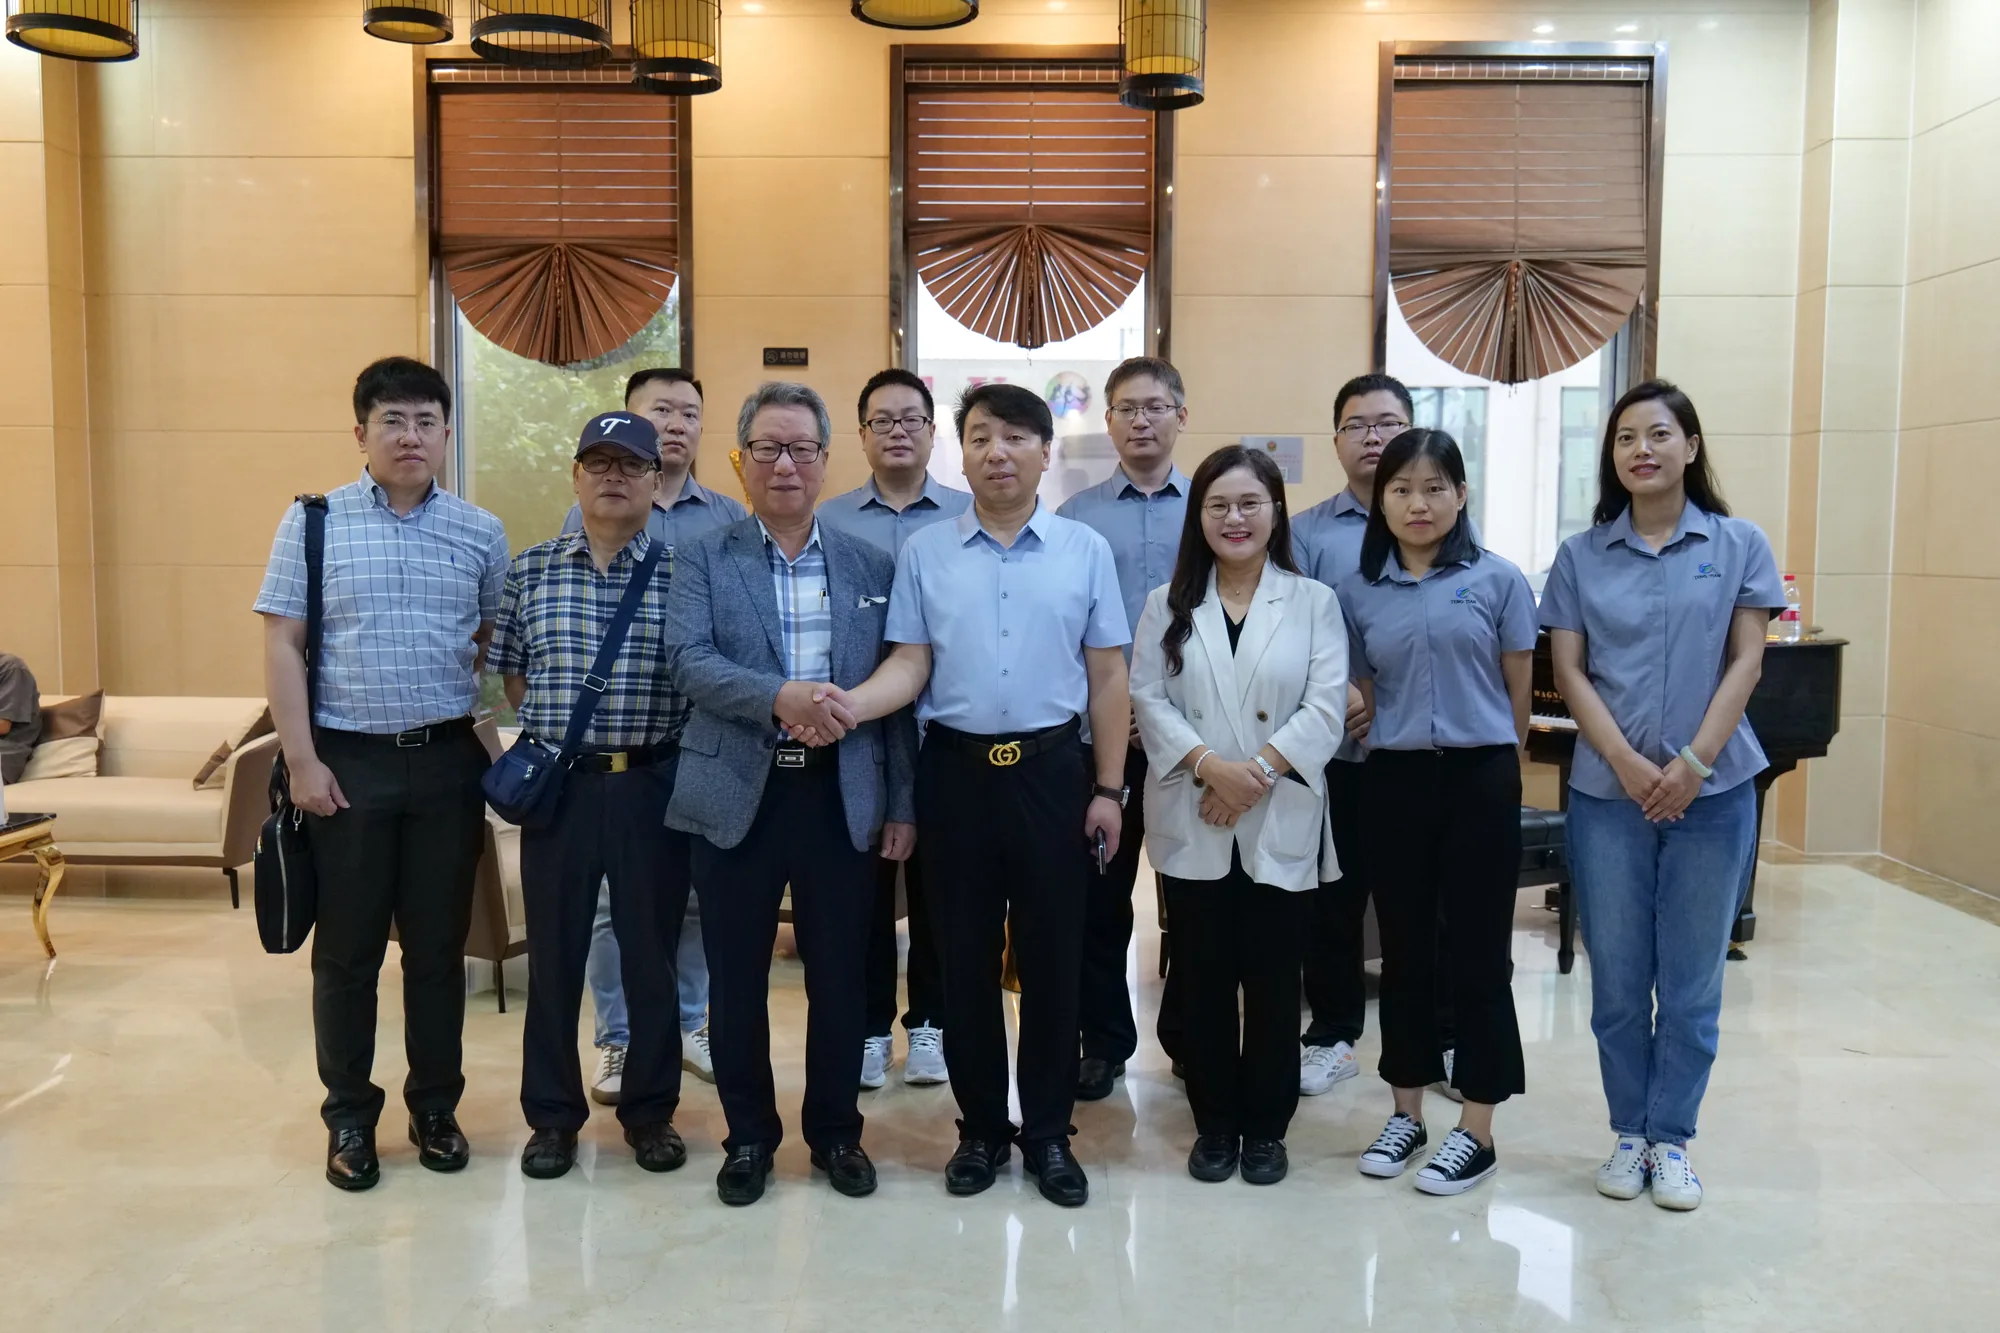
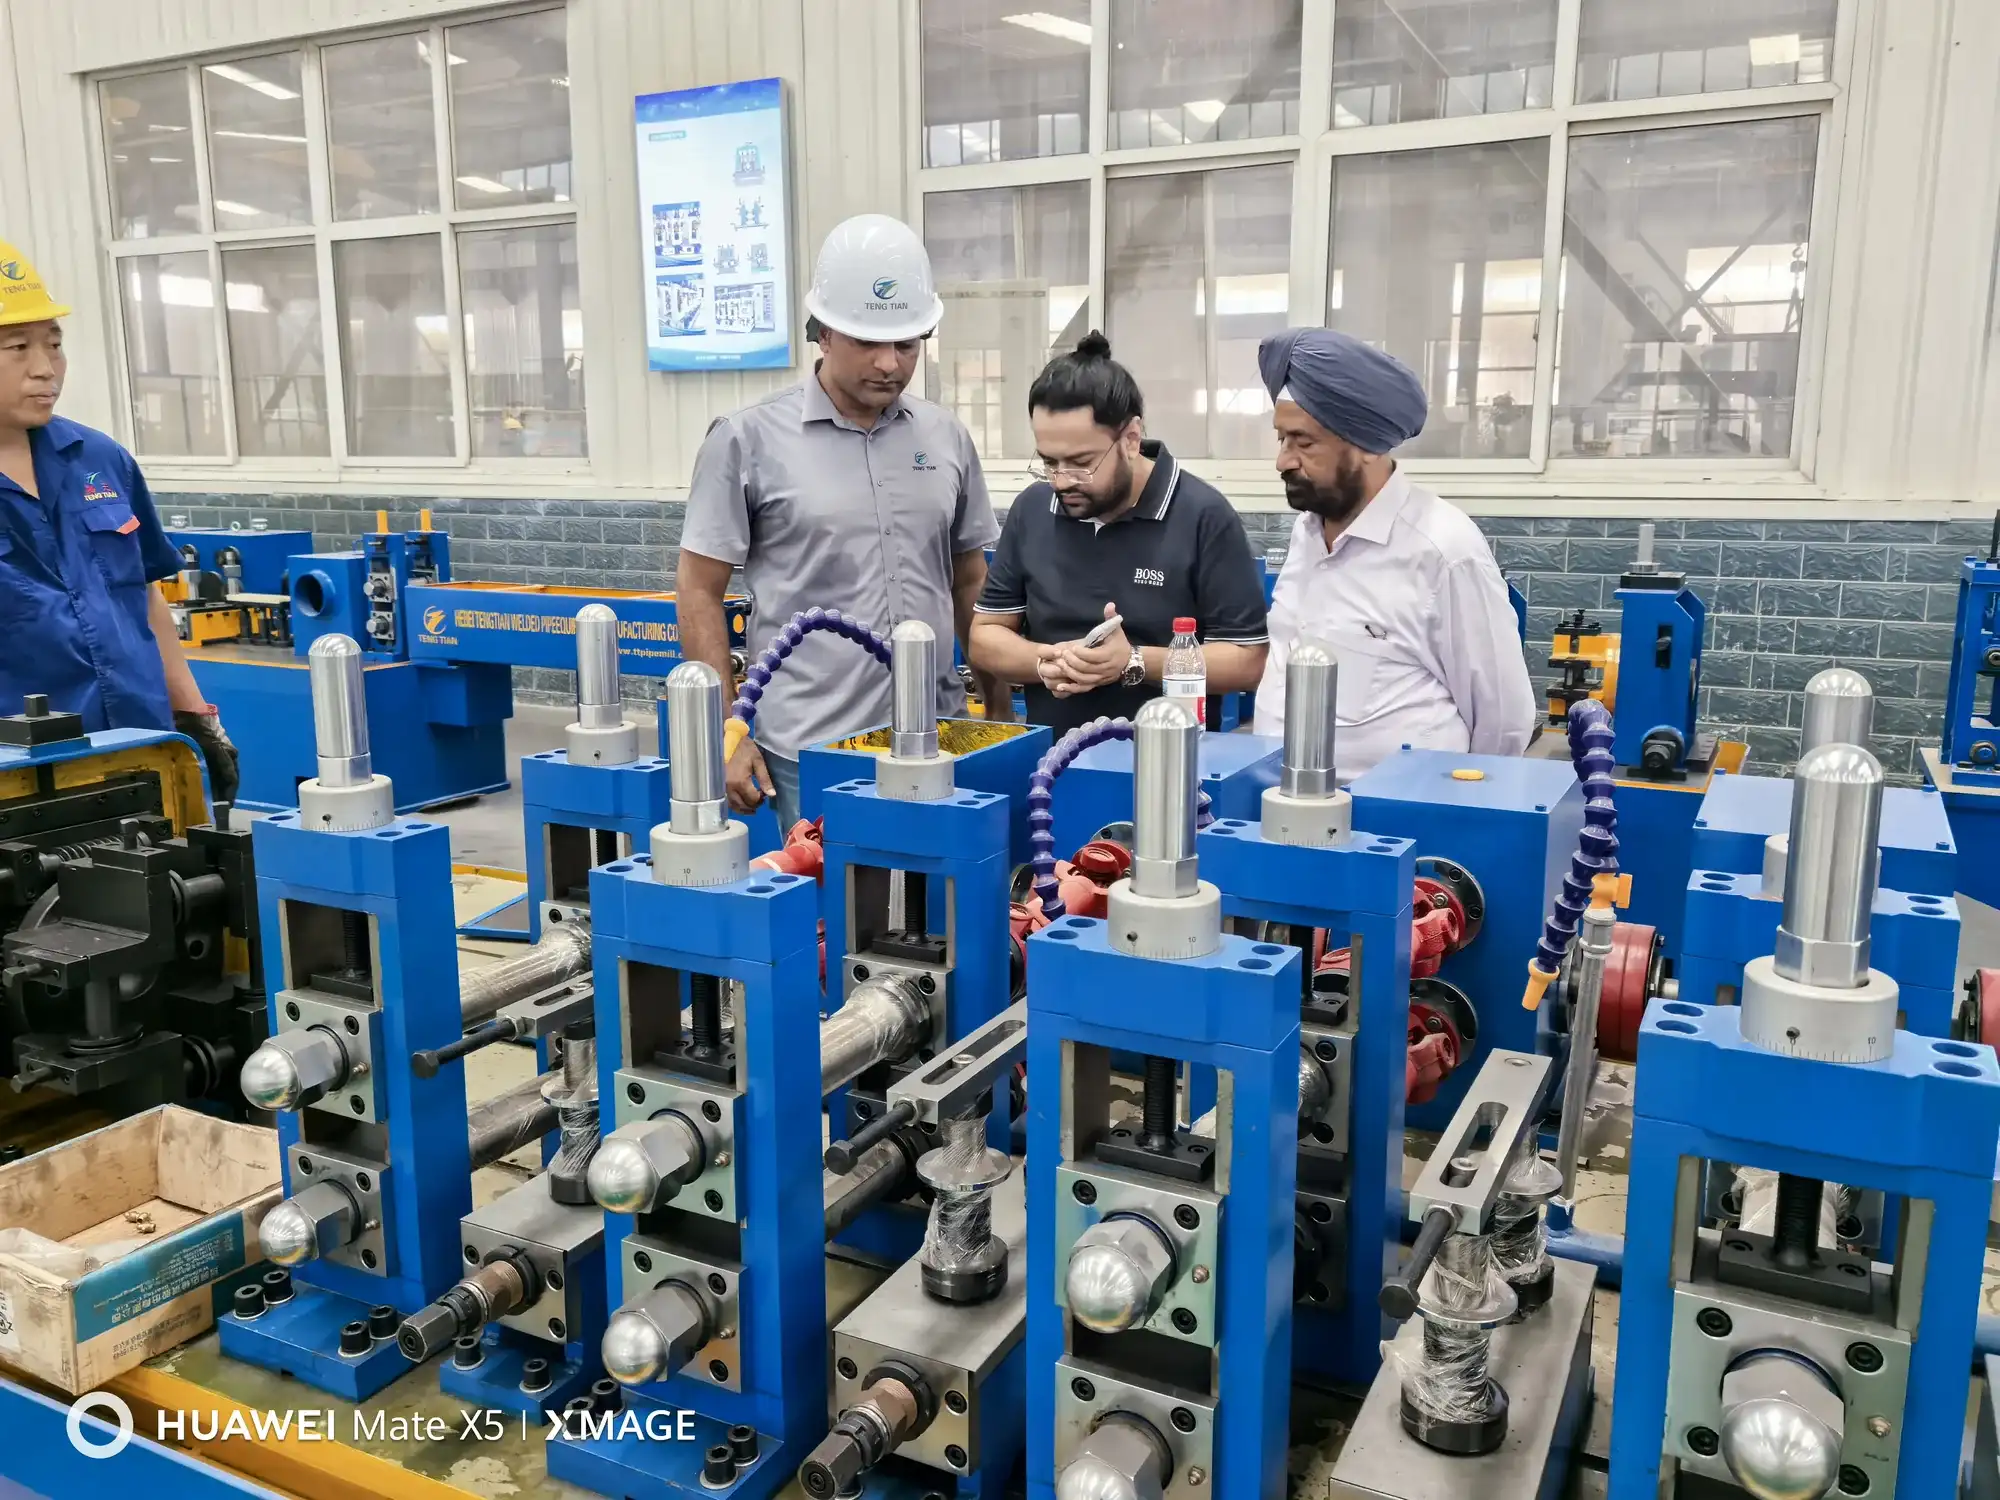
Customers at the Works
A 30-minute live video walk-through can be booked before any commercial discussion. Buyers walking the line during production and factory acceptance at our Zanhuang plant.
Find Your Line by Target Pipe Diameter (Φ10–1620 mm)
Above Φ630 mm the route changes: spiral submerged-arc (SSAW) covers Φ219–1620 mm on one machine, by changing the forming angle rather than the roll set.
Selection starts with one number: the largest outside diameter the plant intends to sell. Pick the step that covers it — each one opens the full specification for that line.
Two Welding Technologies, One Supplier: HFW Longitudinal and SSAW Spiral
Tengtian builds two families of welded pipe production lines: high-frequency longitudinal (HFW) mills covering Φ10–630 mm, and spiral submerged-arc (SSAW) mills covering Φ219–1620 mm. Together they span the full outside-diameter range a pipe plant needs, from furniture tube to large-diameter line pipe.
Most tube mill suppliers sell one welding technology and let the buyer solve the rest. A longitudinal-mill builder stops at the diameter where roll forming stops being practical; a spiral-mill builder has nothing to offer below Φ219 mm.
Tengtian manufactures both, so a plant that starts with small-diameter furniture tube and later moves into water and gas transmission pipe does not have to change supplier, re-learn a control philosophy, or maintain two separate spare-part relationships.
Welder power is matched to diameter in steps across the range 150–1500 kW, so the line is sized to the pipe rather than over-specified. The specific welder rating of each intermediate HG model (HG50 / HG76 / HG89 / HG114 / HG165 / HG219 / HG273 / HG325 / HG426 / HG508) is quoted per project. The two endpoints: HG32 = 150 kW and HG630 = 1500 kW.
Spiral submerged-arc welding takes a narrower coil and winds it helically at a set forming angle, then welds the seam inside and out by automatic submerged arc. Because diameter is changed by changing the forming angle rather than by changing rolls, one SSAW mill covers a wide diameter band: Φ219–820 mm × 3–12 mm on the smaller machine, Φ219–1620 mm × 5–16 mm on the larger.
Forming angle range is 39°–80°; delivery speed 0.5–3 m/min; welding speed 0.5–3 m/min.
The trade-off is honest and worth stating: SSAW is discontinuous and slower per metre, which suits large-diameter, medium-batch production; HFW is continuous and fast, which suits smaller diameter at volume.
The two technologies are not interchangeable. High-frequency welding forms strip through a roll set and closes a straight longitudinal seam by induction heating — fast, continuous, and economical for high volumes of small and medium diameter.
Built For: Distributors, Integrators, Line-Pipe Mills and Section Plants
Equipment for API 5L line pipe and for GOST R 58966-2020 H-beam is built to those inspection chains. Four buyer types account for most of what leaves this factory, and each one asks a different first question.
System integrators build a whole plant for an end user. They need the supplier to take responsibility across units, not just ship a mill: whole-line customisation, engineering cooperation, and a scope of supply that does not leave gaps between machines.
Large energy and infrastructure end users buy against a standard.
Regional pipe and section makers — the largest group by count — build or expand a plant and are sensitive to price, lead time, changeover speed, yield and energy use.
Seven objections come up in almost every enquiry, and they are worth answering here rather than three emails later.
Can a Chinese supplier keep spares coming?
Rolls and key wear parts are machined on the works’ own CNC equipment, so roll supply does not depend on a third-party shop that may stop quoting.
Will it meet API 5L or GOST?
The API line-pipe inspection chain and GOST R 58966-2020 H-beam capability are what those lines are designed around.
How long does a size change take?
On direct-square-forming lines, size is changed by combined dies instead of by changing rolls; roll consumption drops by more than 90%, and servo adjustment plus quick die change carries the rest. One exception is worth stating: making 100 × 100 mm tube needs the upper roll on the final open stand changed.
Is the lead time real?
50–90 days, with tiered supply and whole-plant scheduling against the works’ own capacity.
Can payment terms flex?
Staged payment, flexible deposit ratio and third-party escrow are all in use.
Why is your price different from the next quote?
Because the configurations are different. Tiered pricing maps to a written scope of supply, and the comparison only means something when both scopes are on the table.
Who commissions it, and can our operators run it?
Installation and commissioning are in the after-sales scope, engineers are dispatched to site, and support stays online after handover.
Buyers usually arrive through one of two doors. Either something is being built — a new mill, a capacity expansion, a move into square tube, API line pipe or H-beam, or a large downstream order that has to be covered — or something has failed at the incumbent supplier: spares dried up, size changes cost too much time, delivery slipped, or a new standard has to be met.
Distributors and regional agents resell into their own market. What they need is a tiered configuration they can quote at more than one price point, a delivery date that holds, and a factory that answers fast enough to keep their own customer calm. Response commitment is one hour, through a single named contact rather than a ticket queue.
Certificates, Patents and Delivery Records
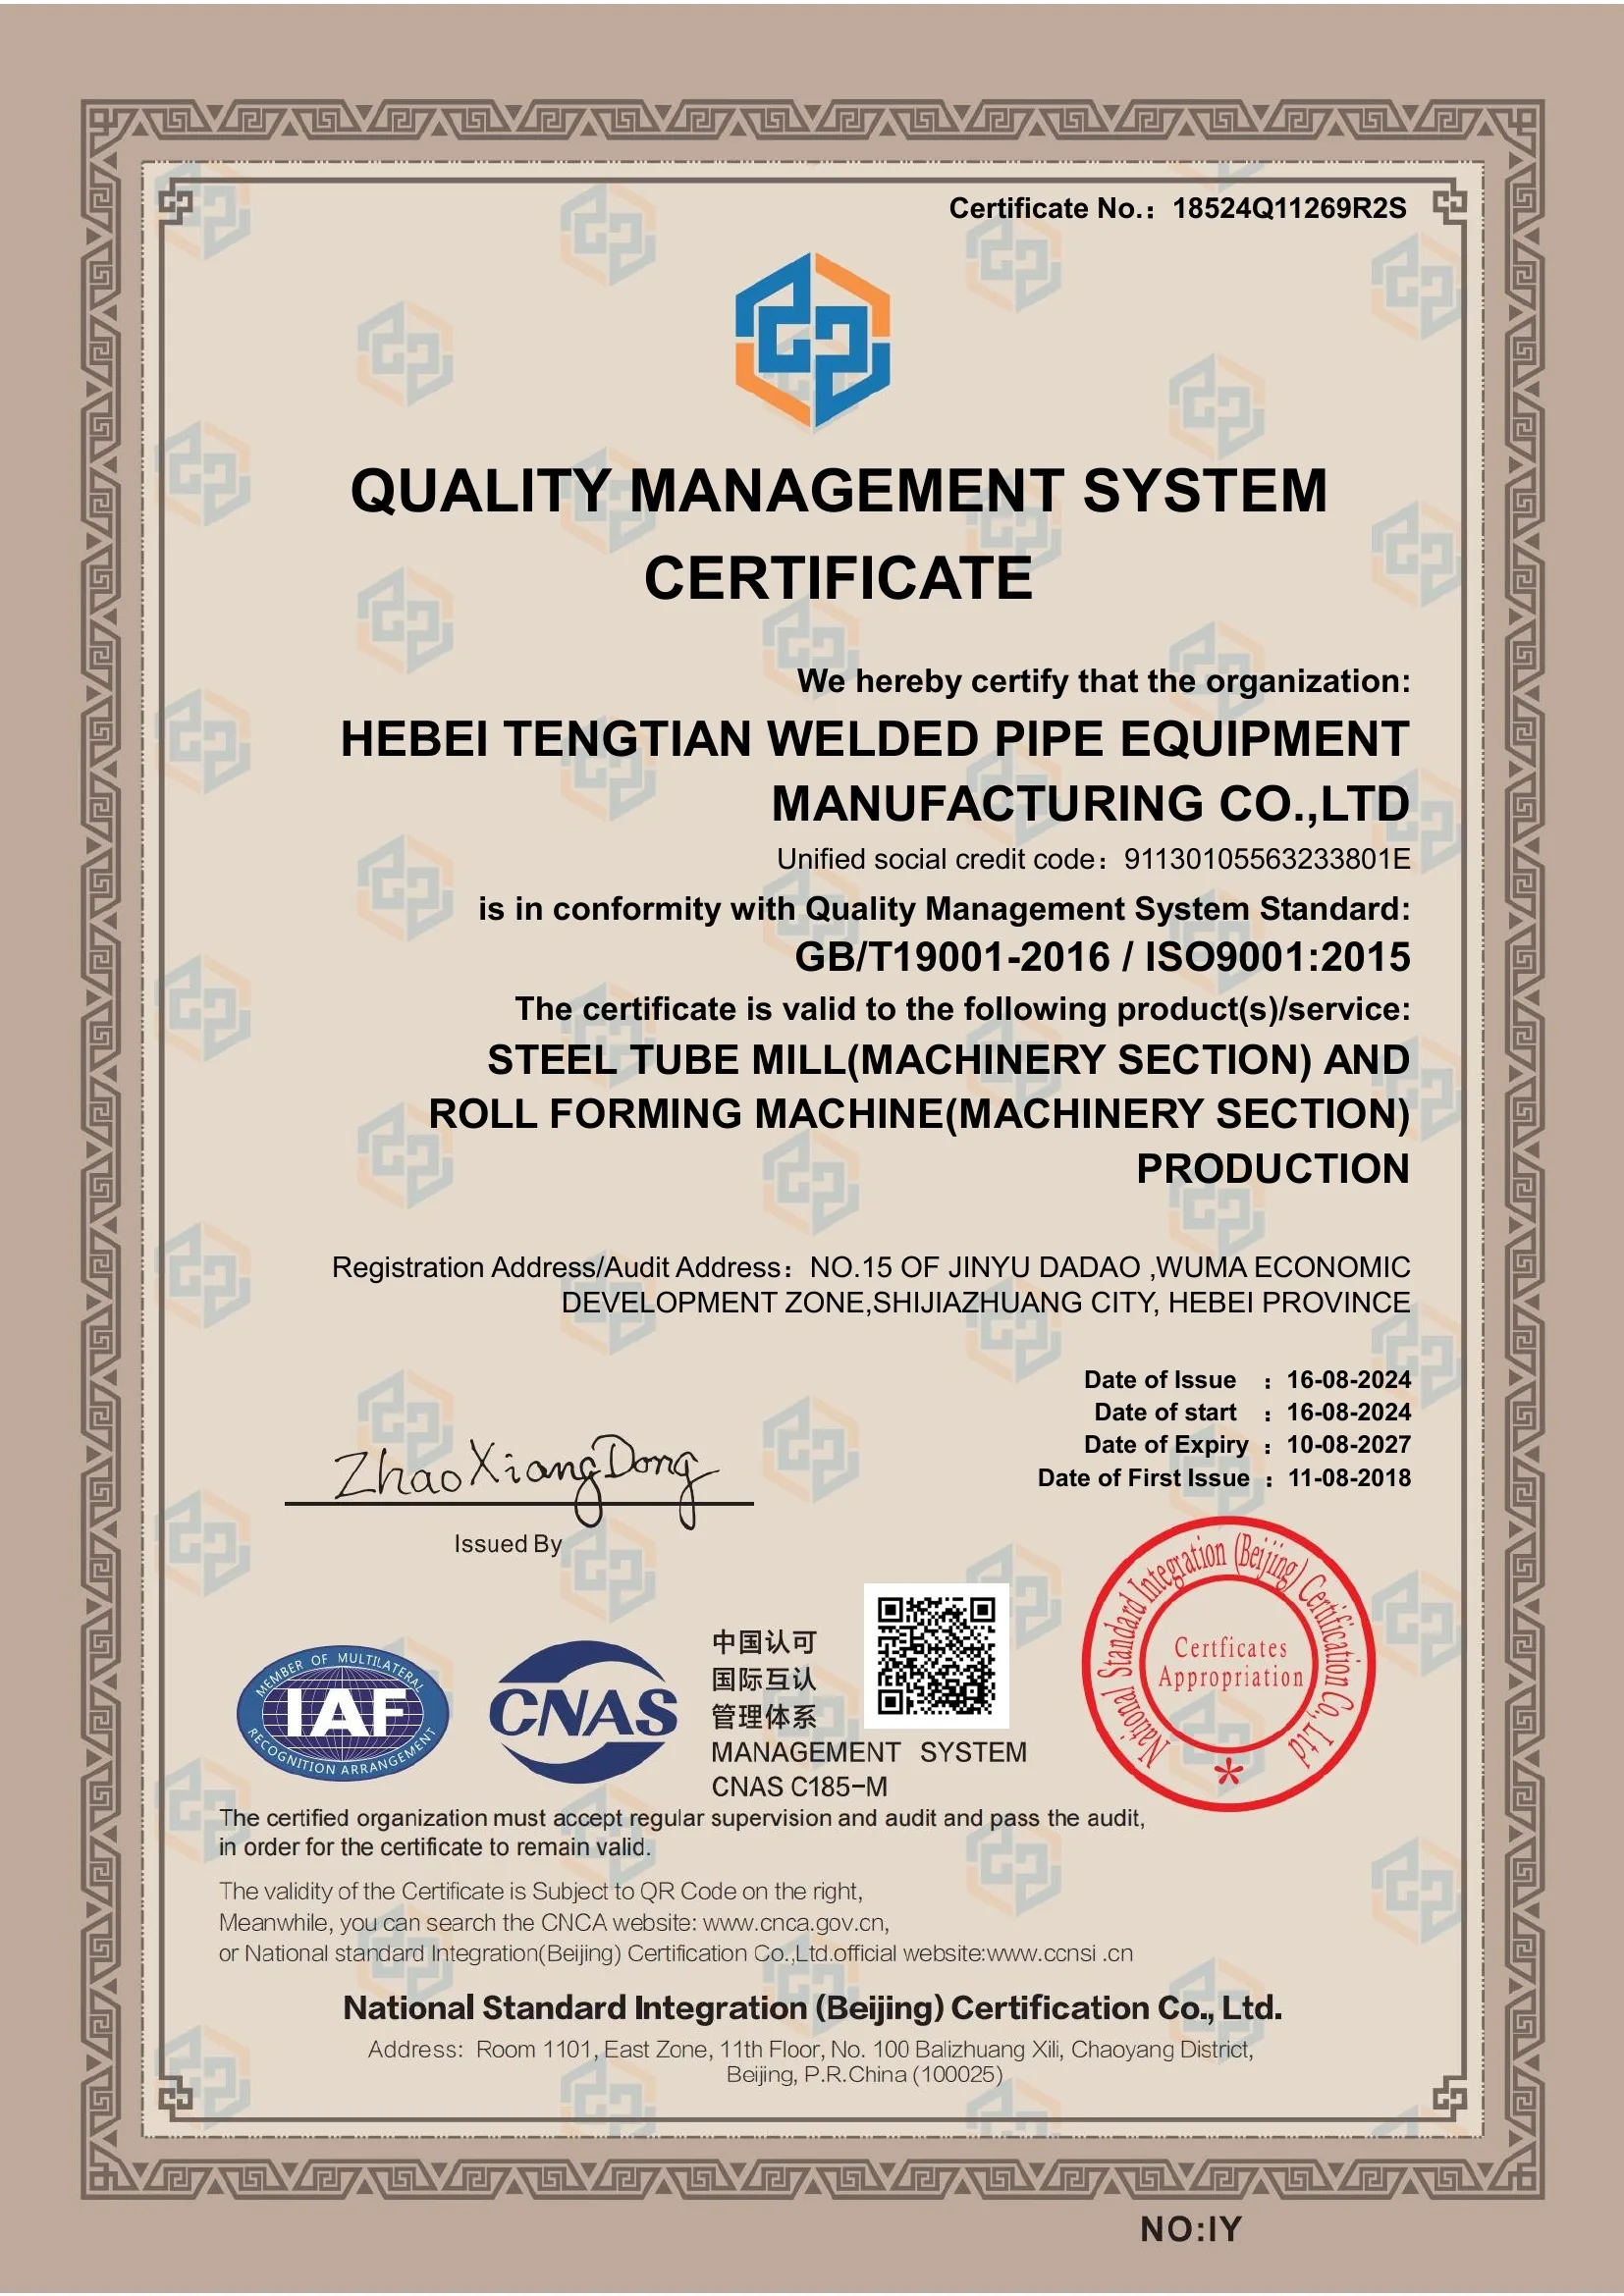
- ISO 9001 quality management system — certificate No. 18524Q11269R2S, GB/T 19001-2016 / ISO 9001:2015, issued by National Standard Integration (Beijing) Certification.
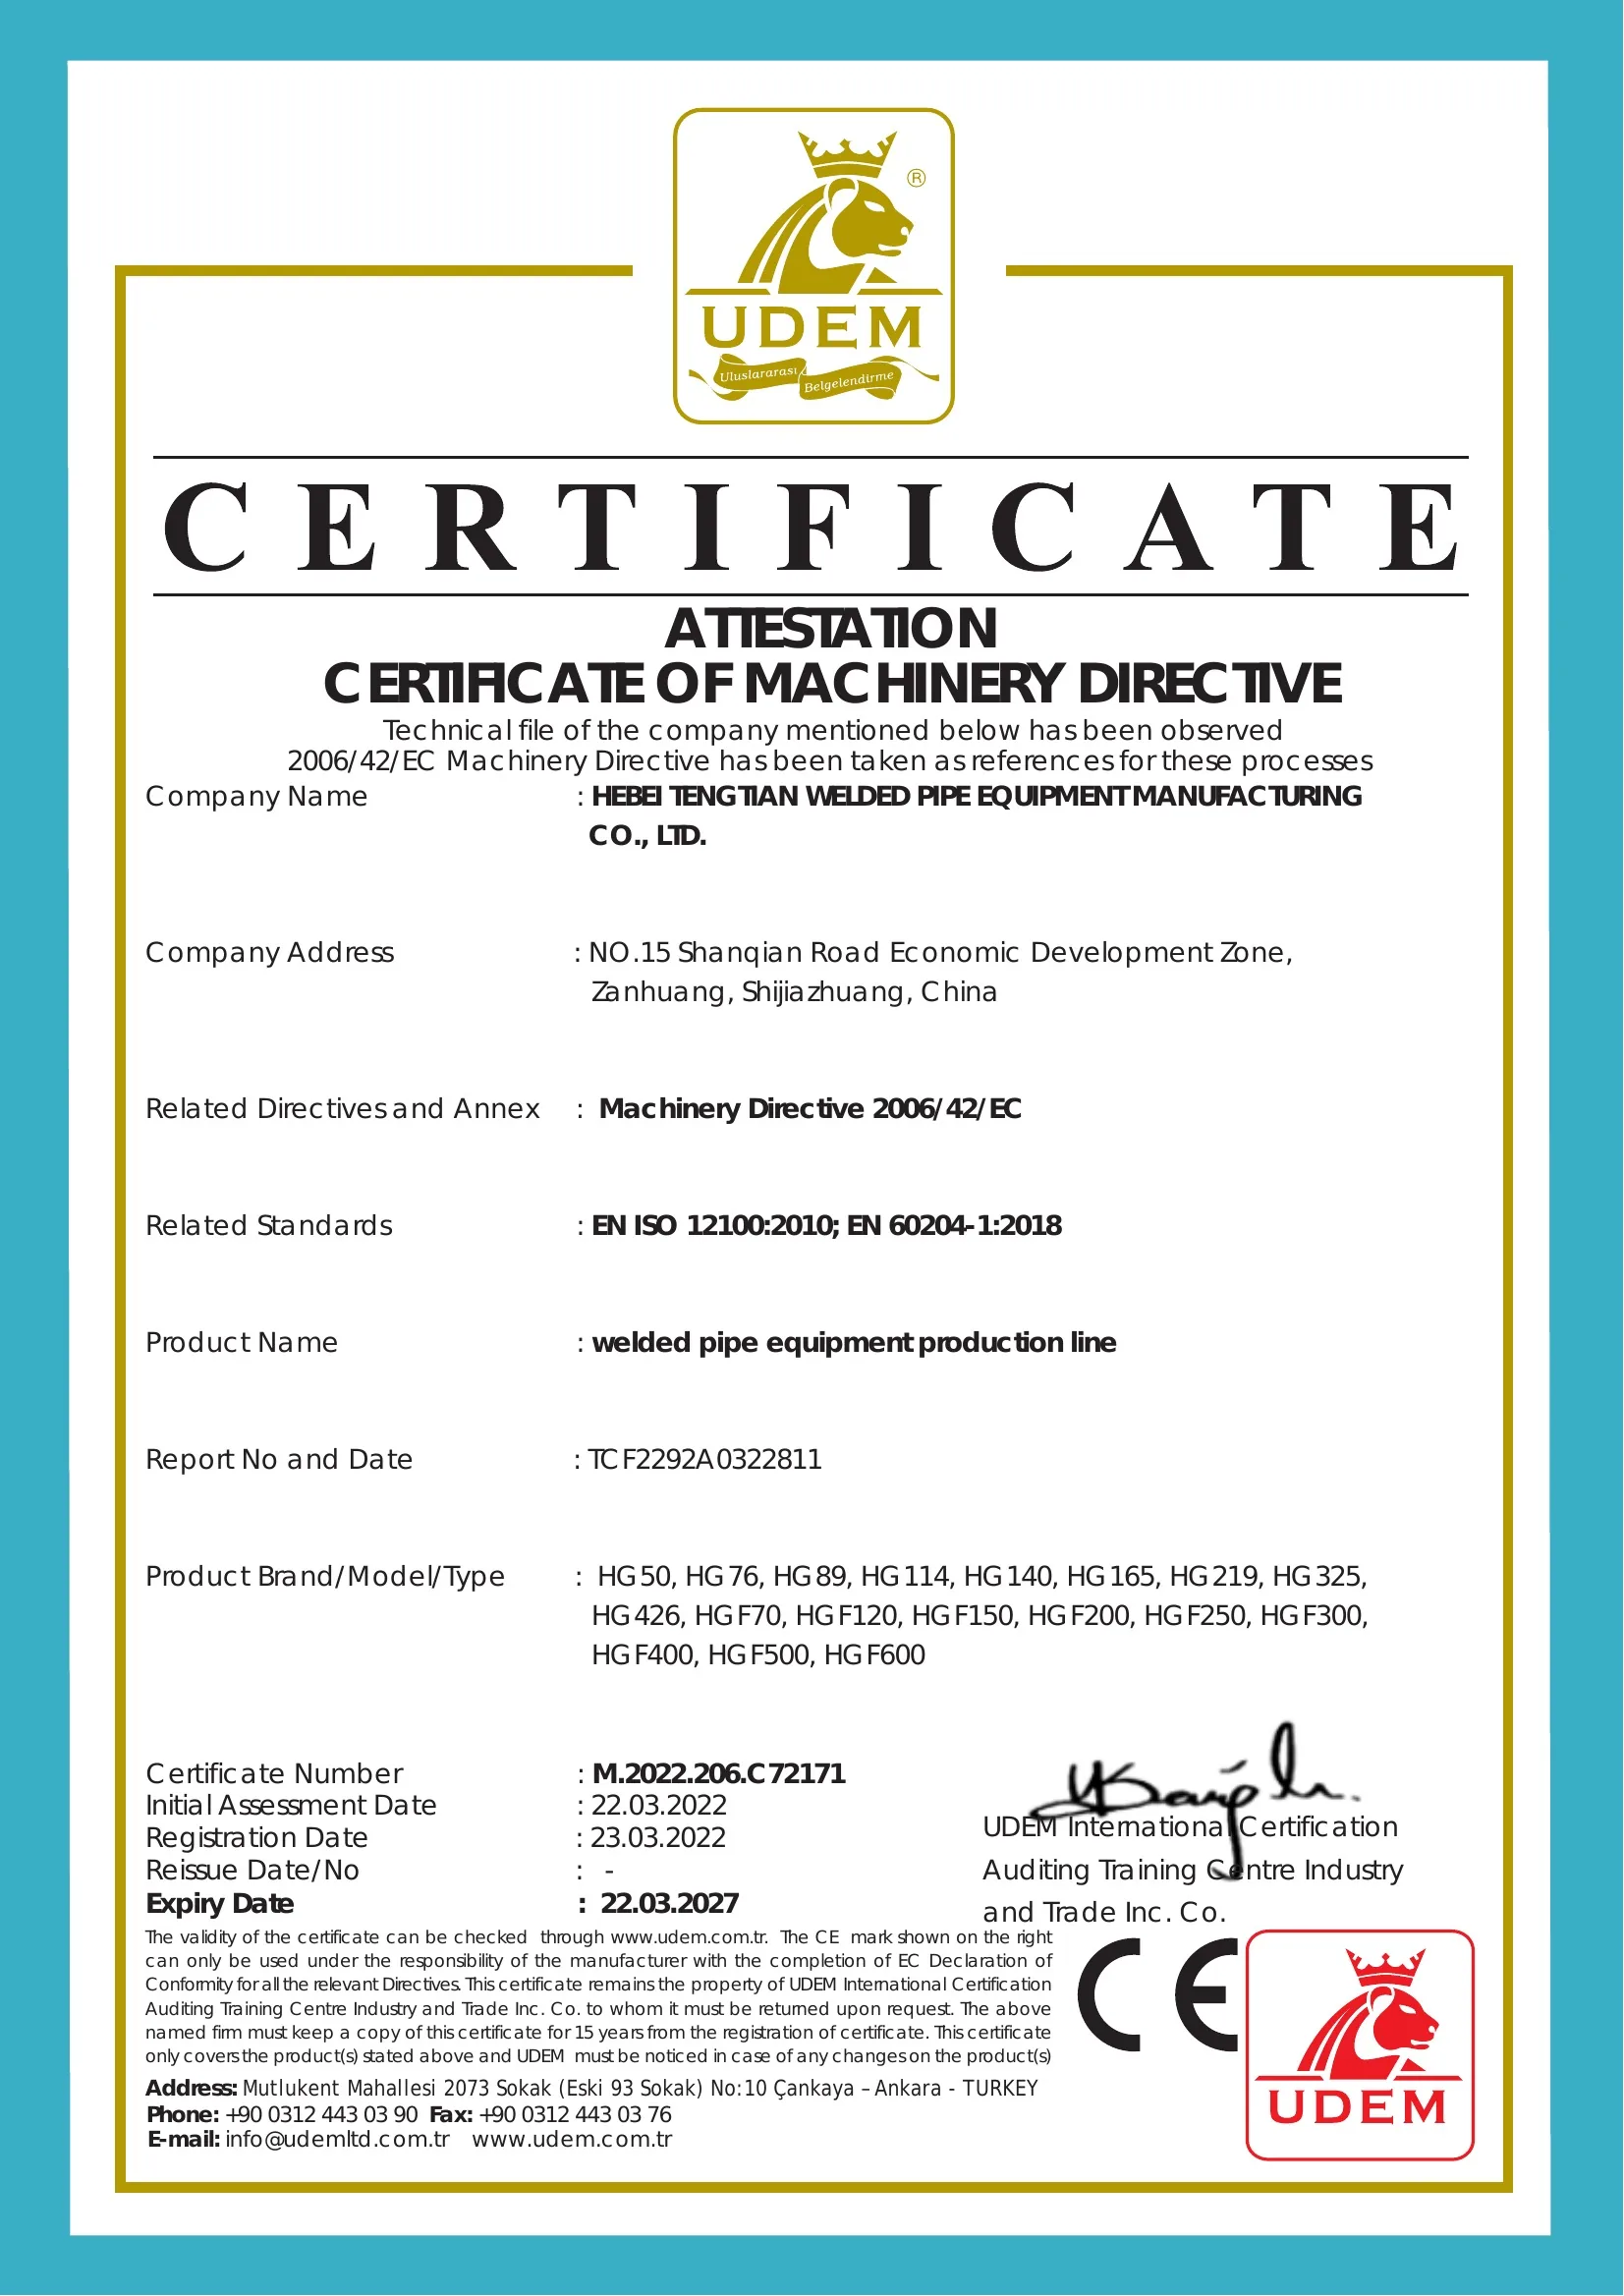
- CE — UDEM, welded pipe equipment, No. M.2022.206.C72171, report TCF2292A0322811.
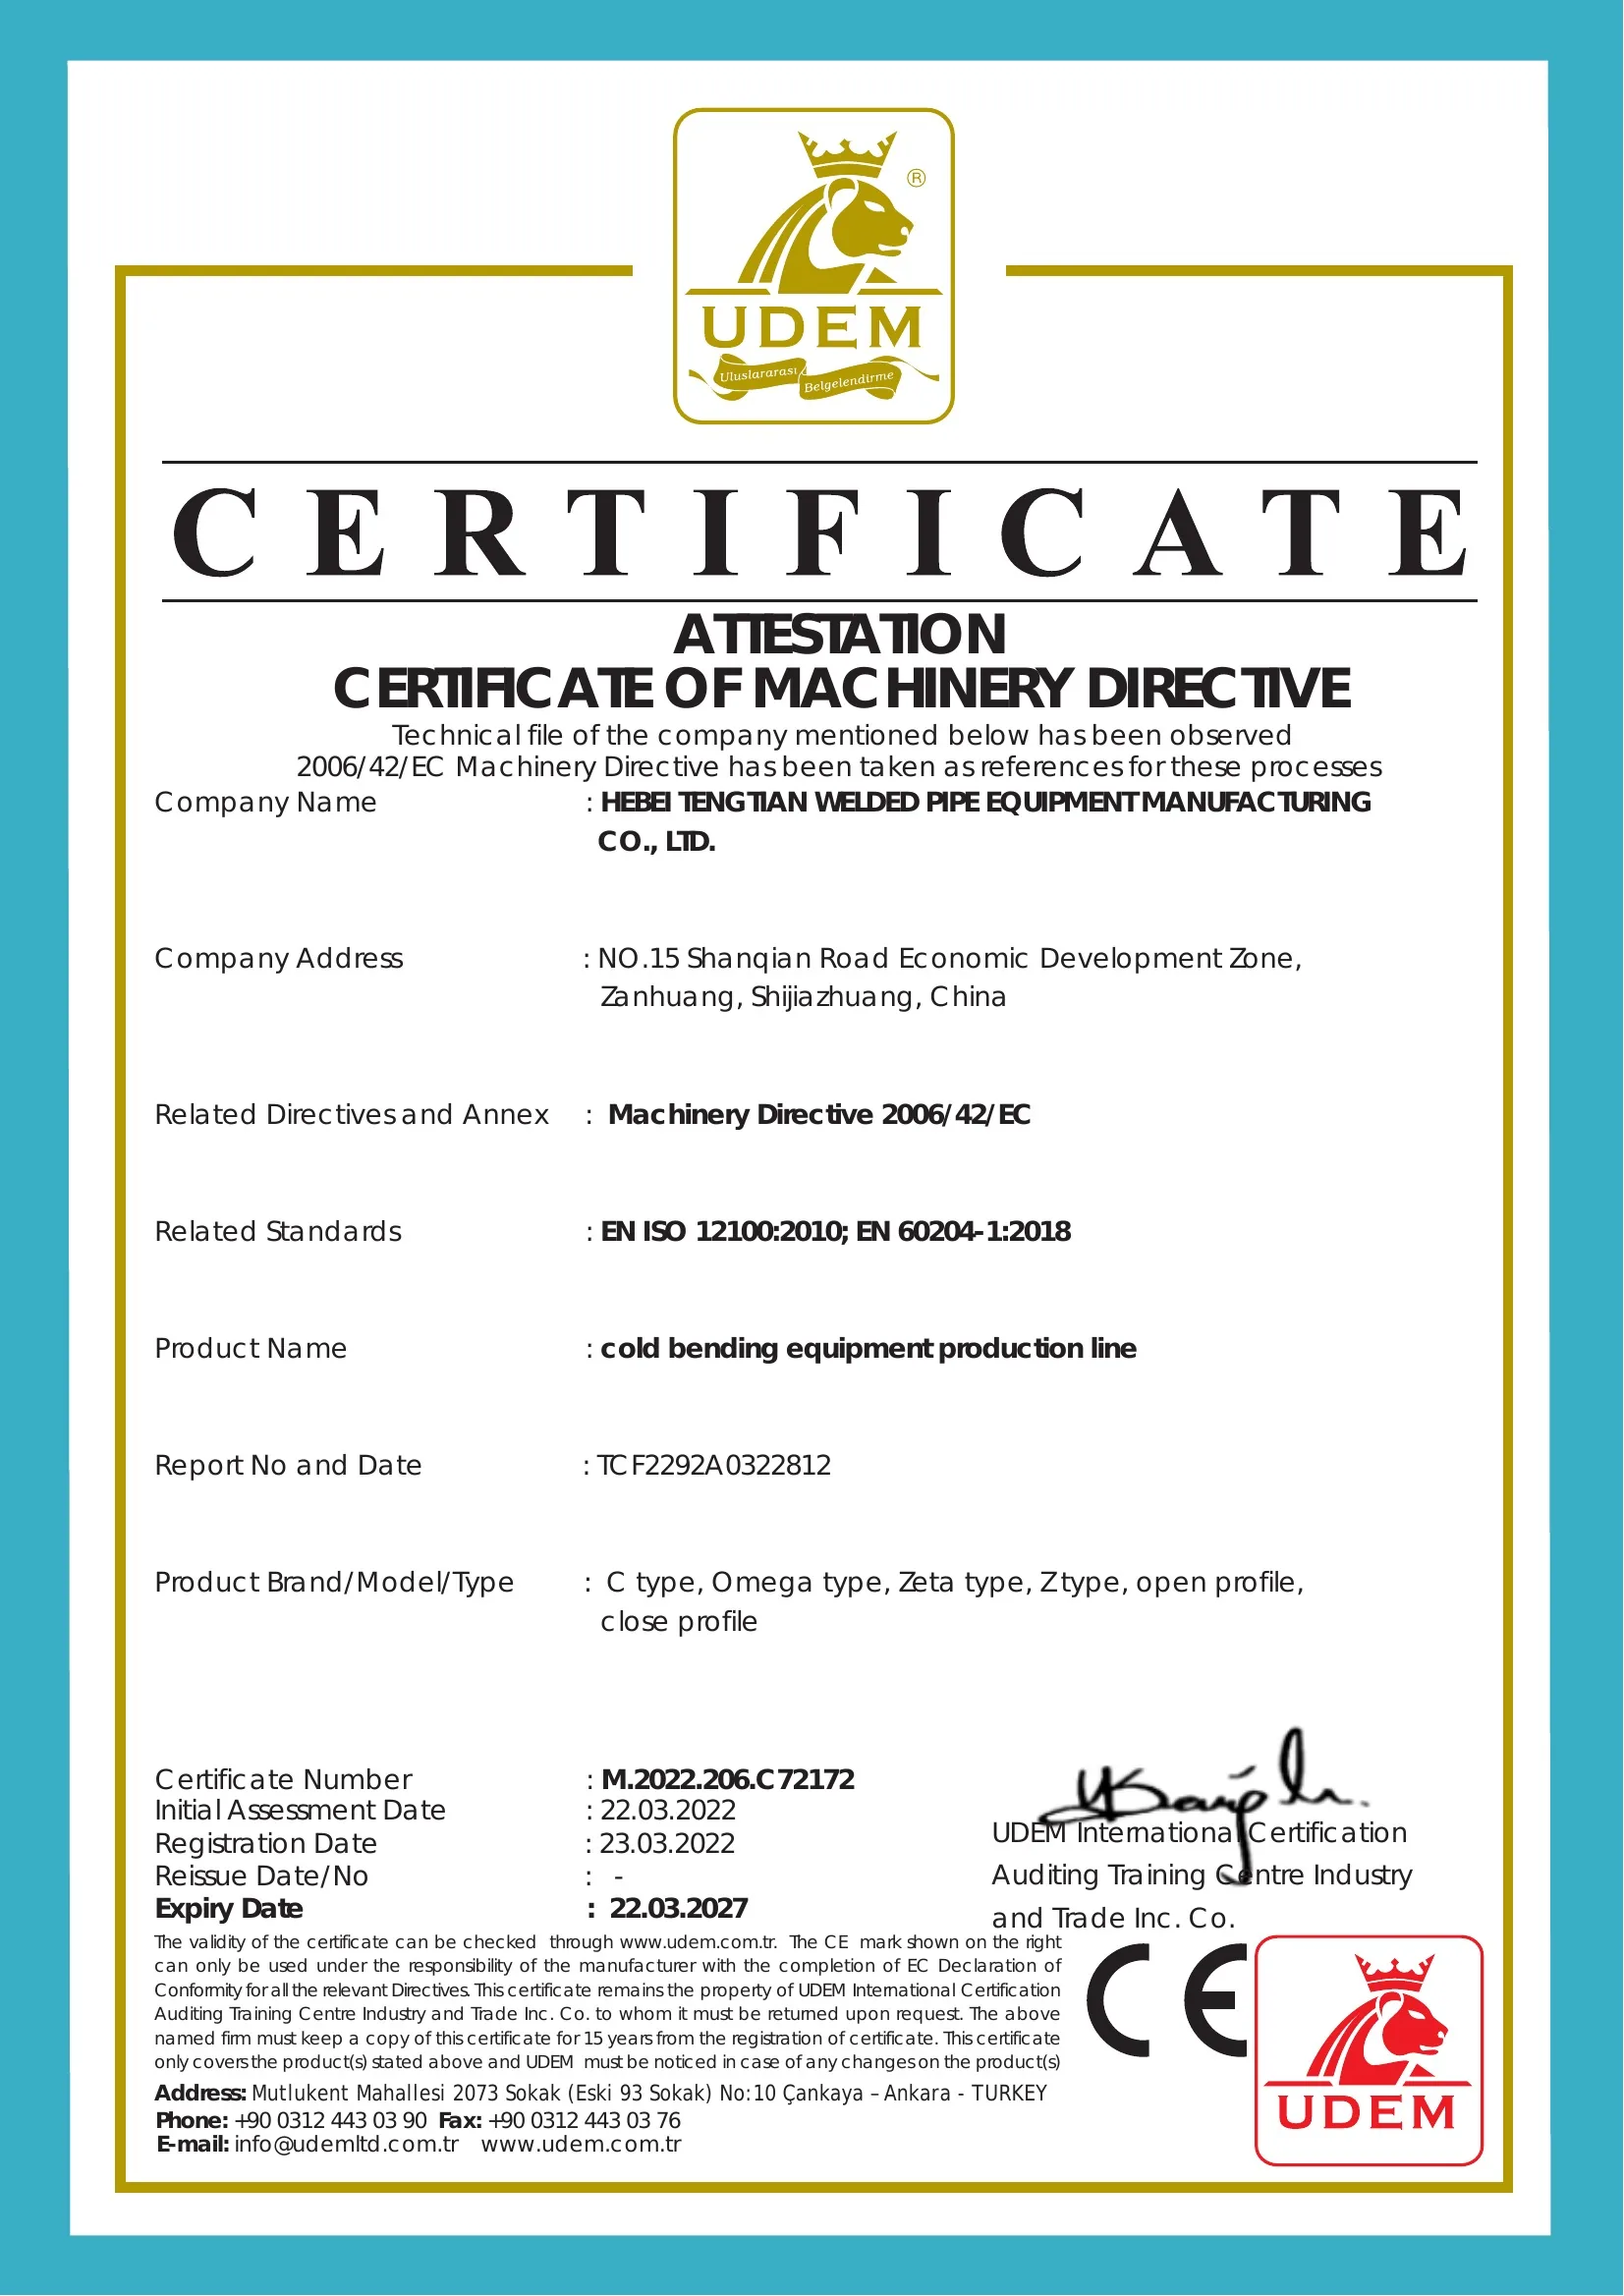
- CE — UDEM, cold roll forming equipment, No. M.2022.206.C72172.
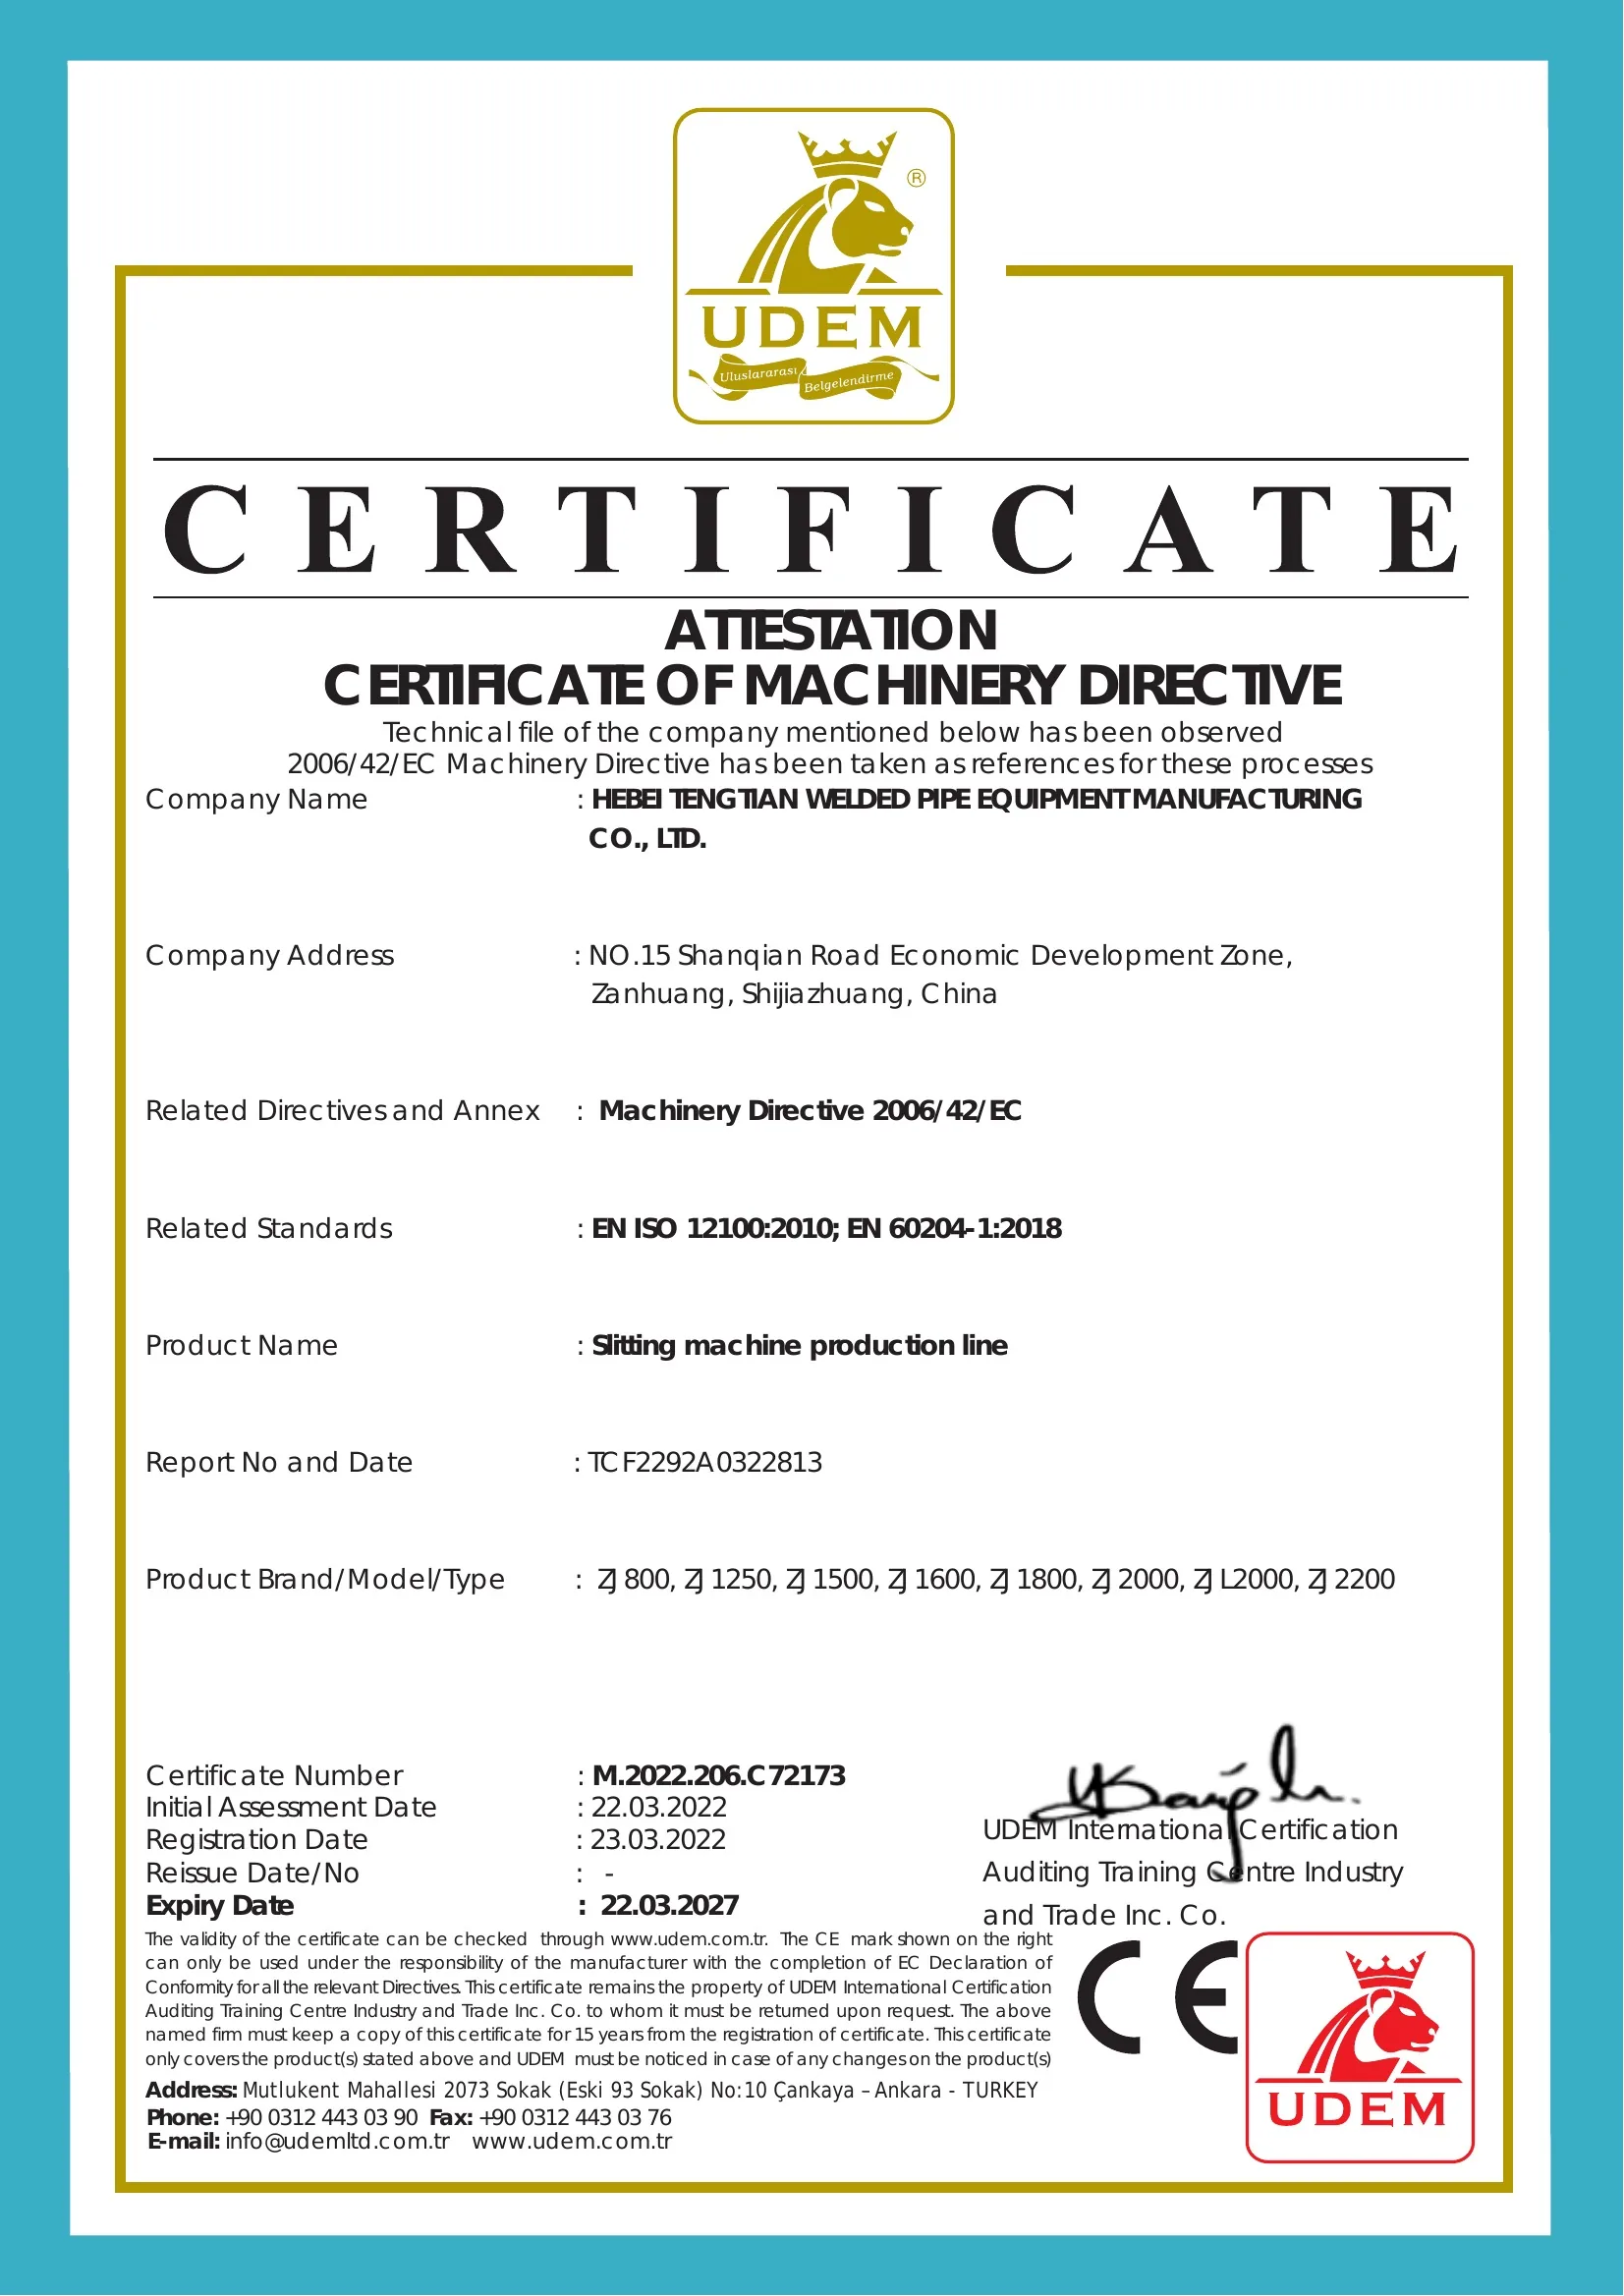
- CE — UDEM, slitting lines, No. M.2022.206.C72173.
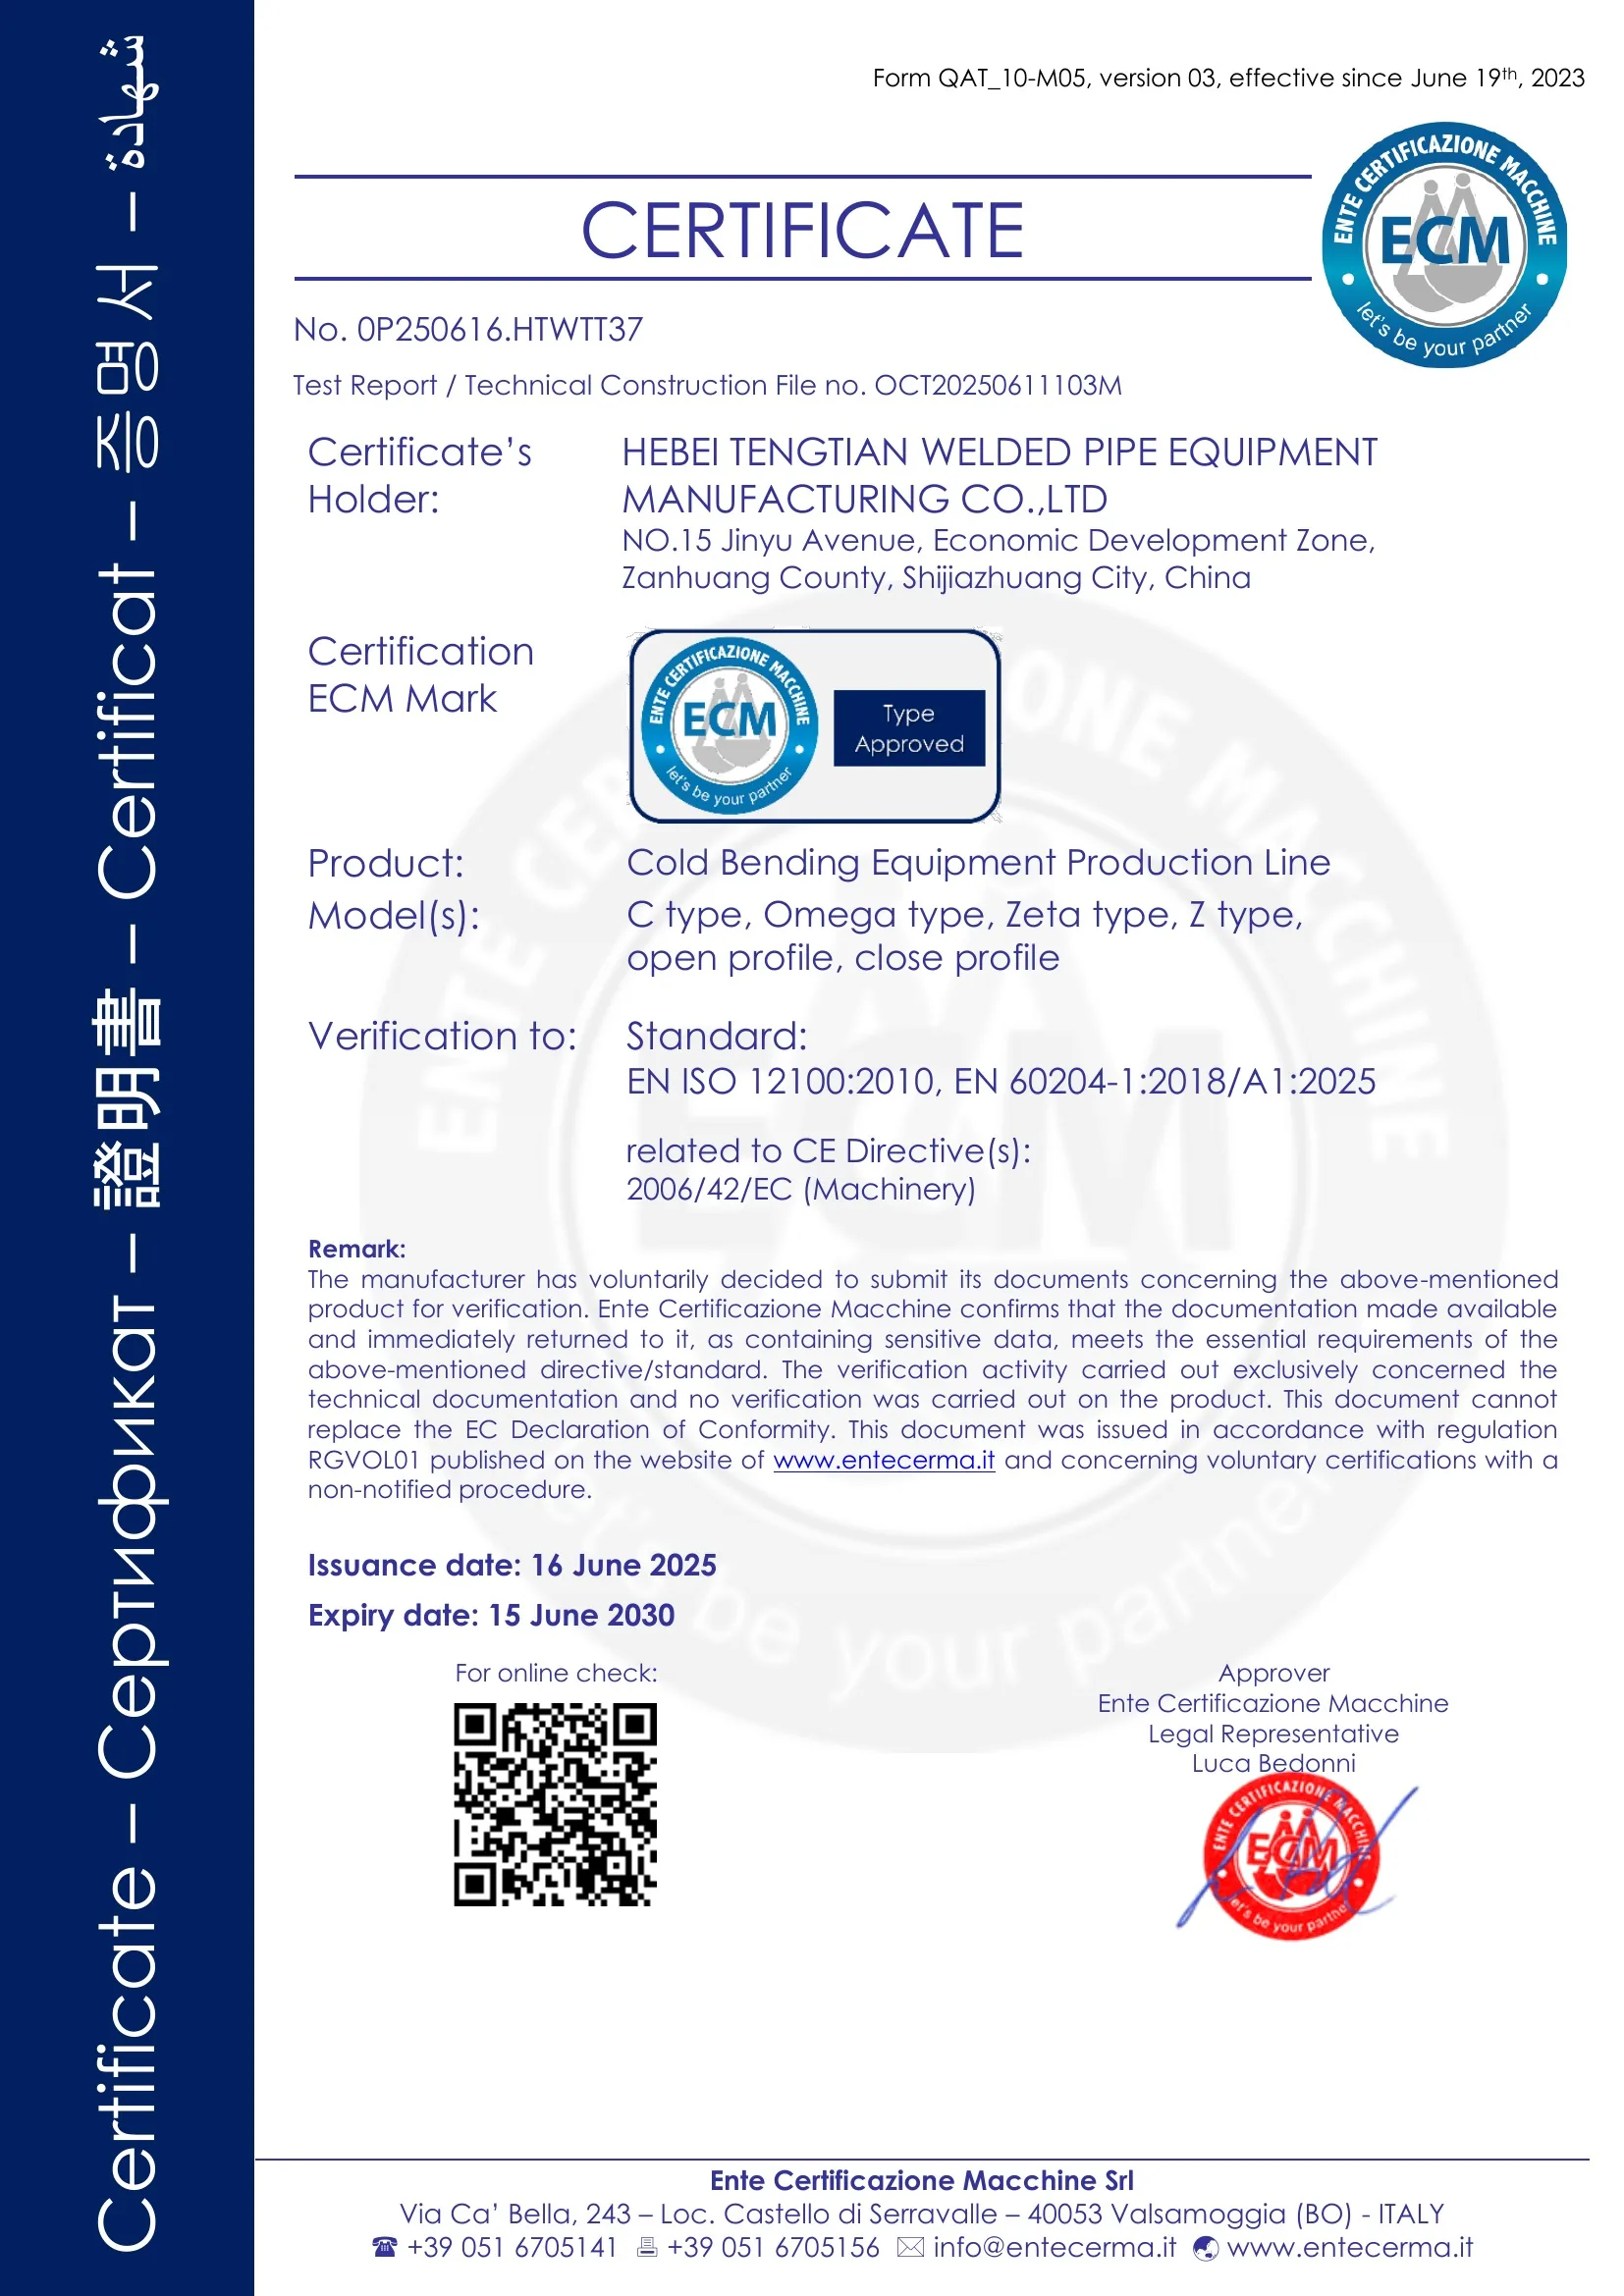
- Technical file verified by Ente Certificazione Macchine Srl (Italy), No. 0P250616.HTWTT37, TCF OCT20250611103M.
- Enterprise standard Q/GYLTT01-2023 “HGF150 High-Frequency Welded Pipe Equipment”, published on the national enterprise-standard platform.
- High-Tech Enterprise certificate GR202413001148.
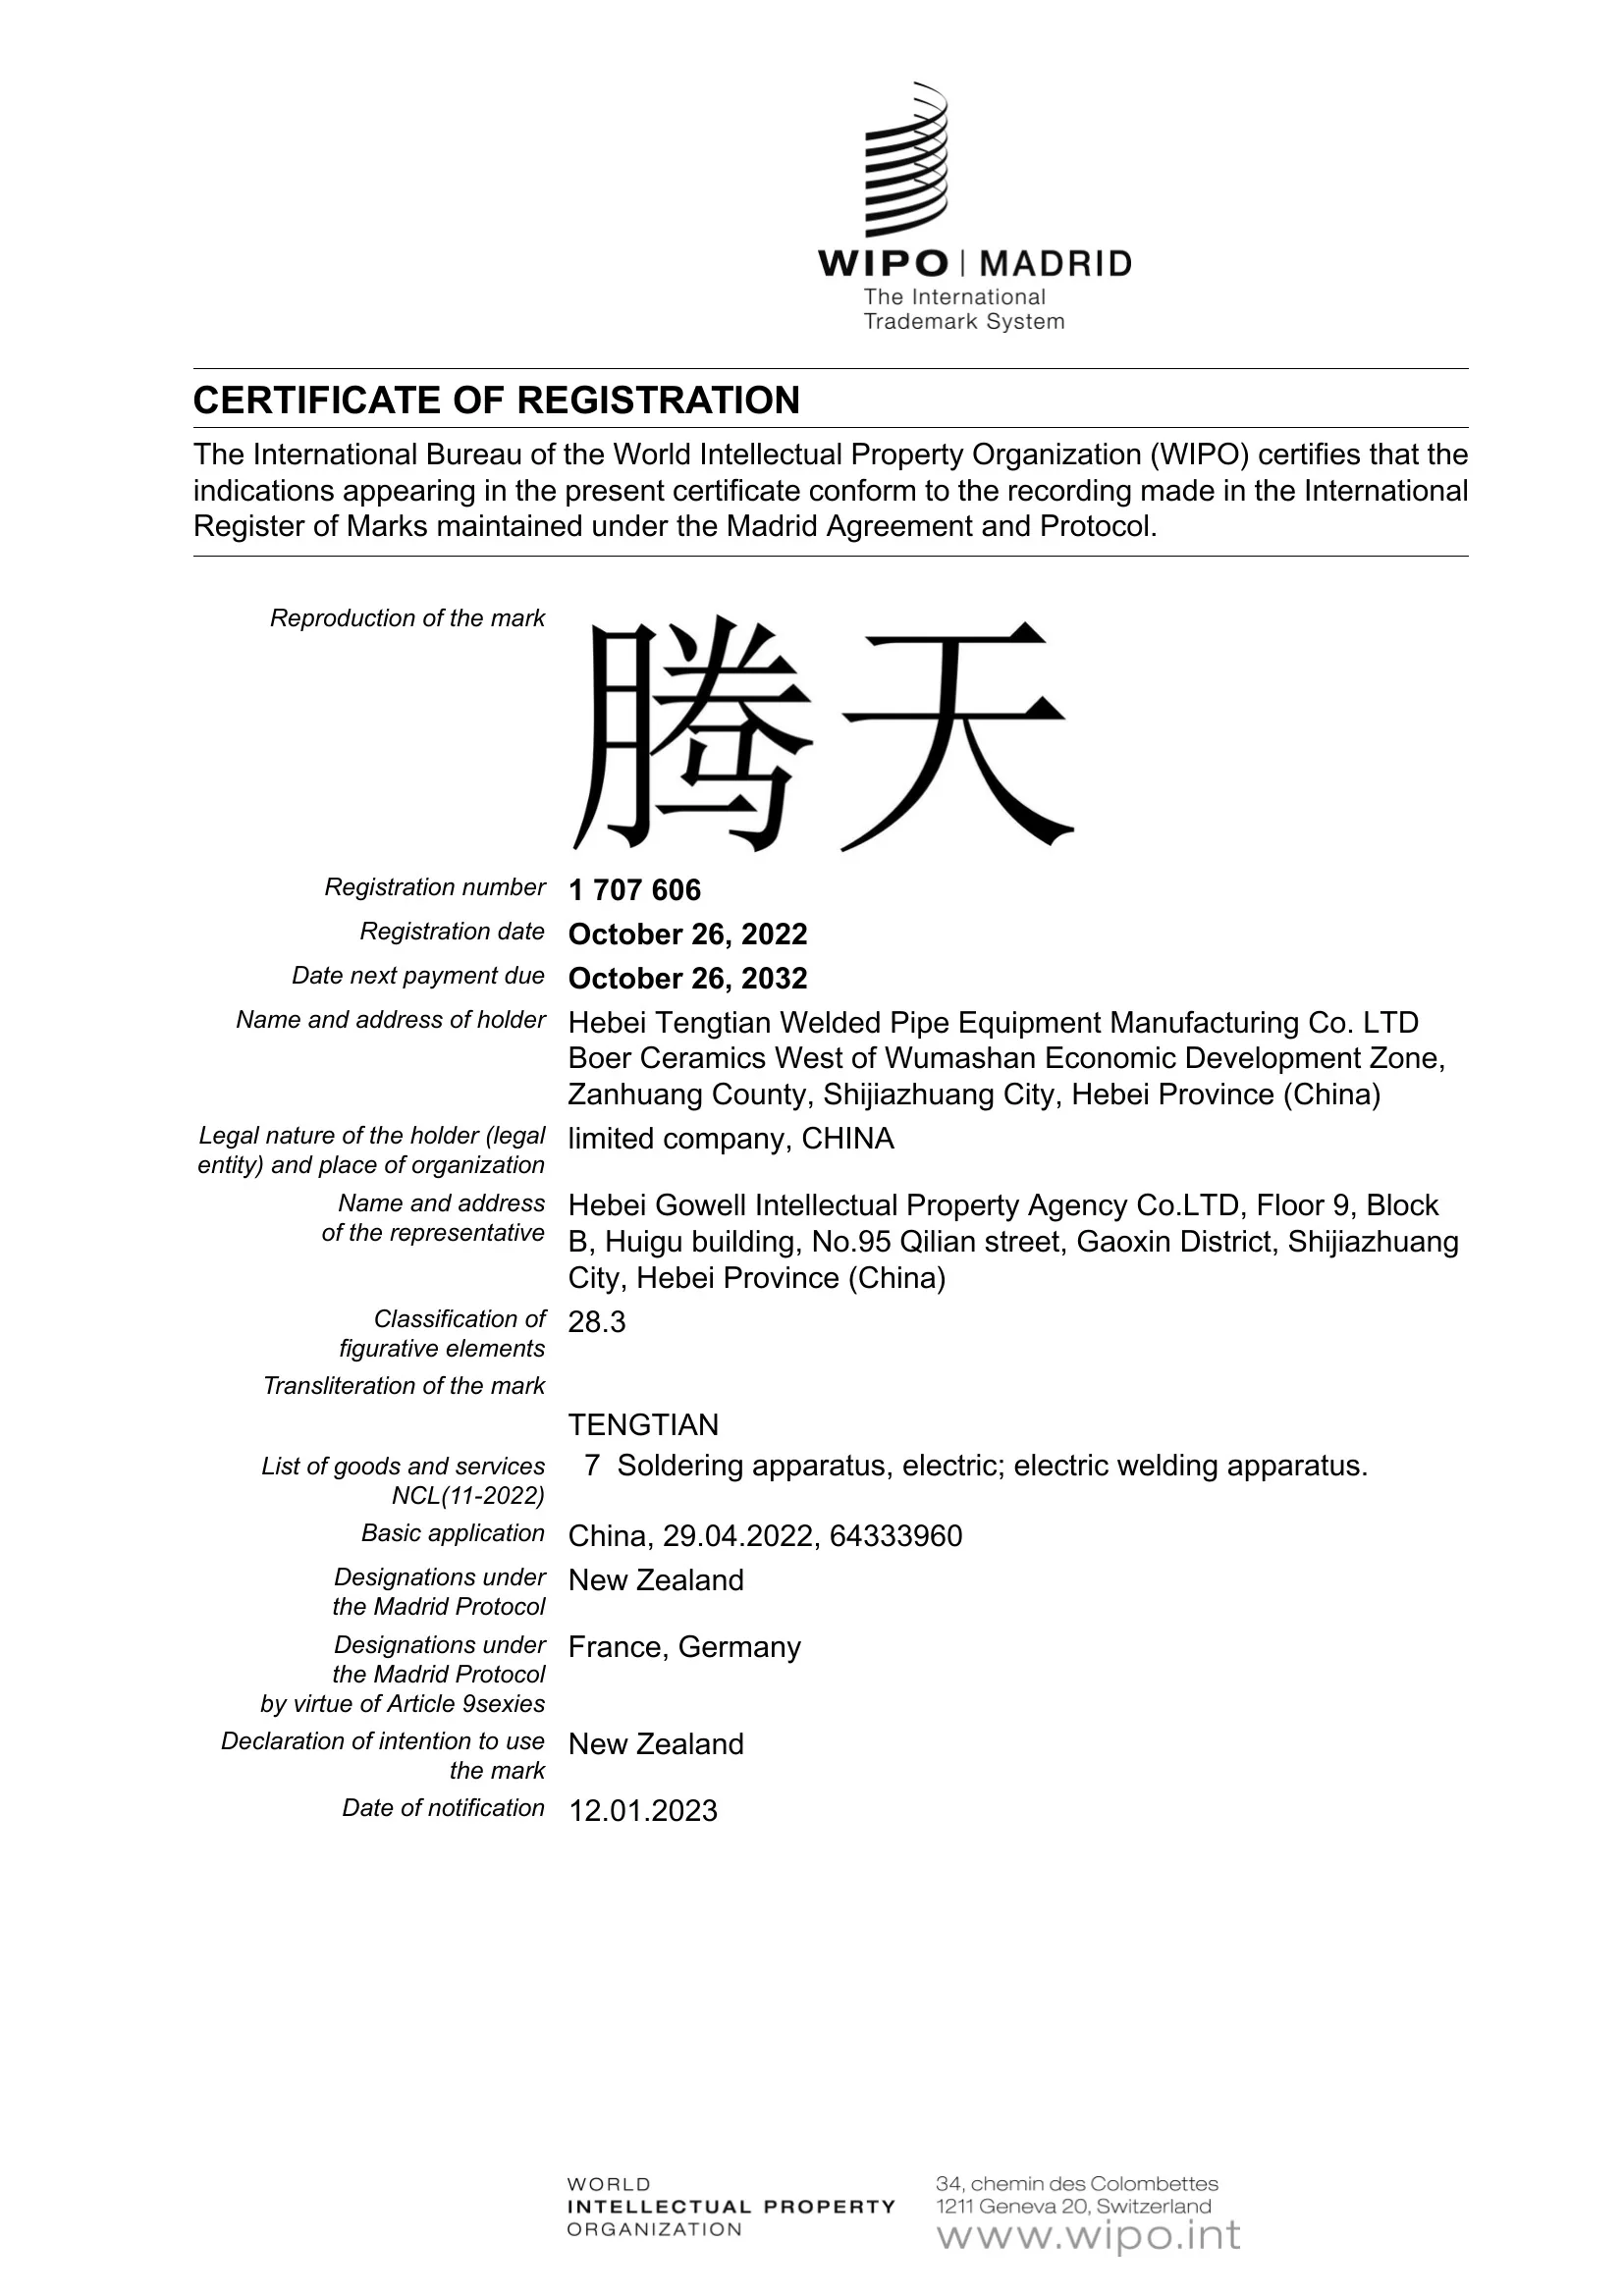
- Hebei Province first-set major technical equipment catalogue, item 33 — HGF150. No. 1 707 606, Nice class 7.
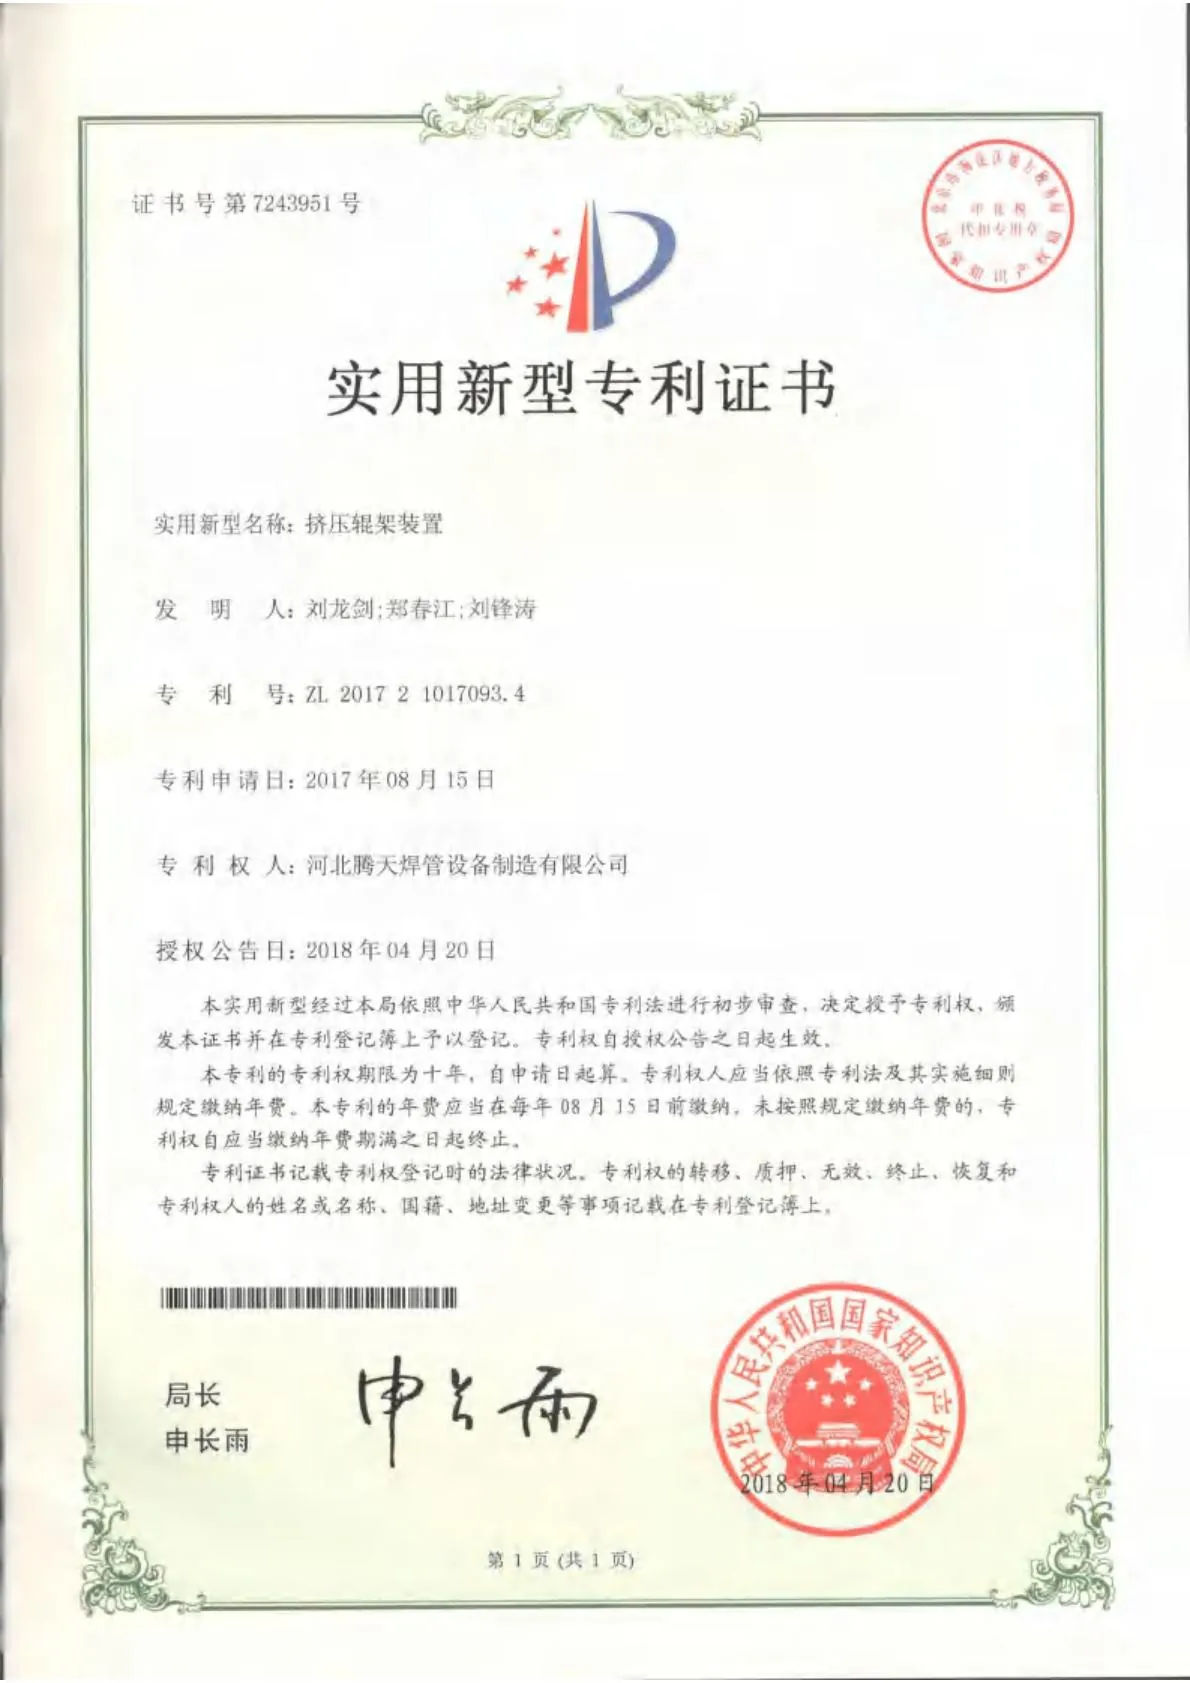
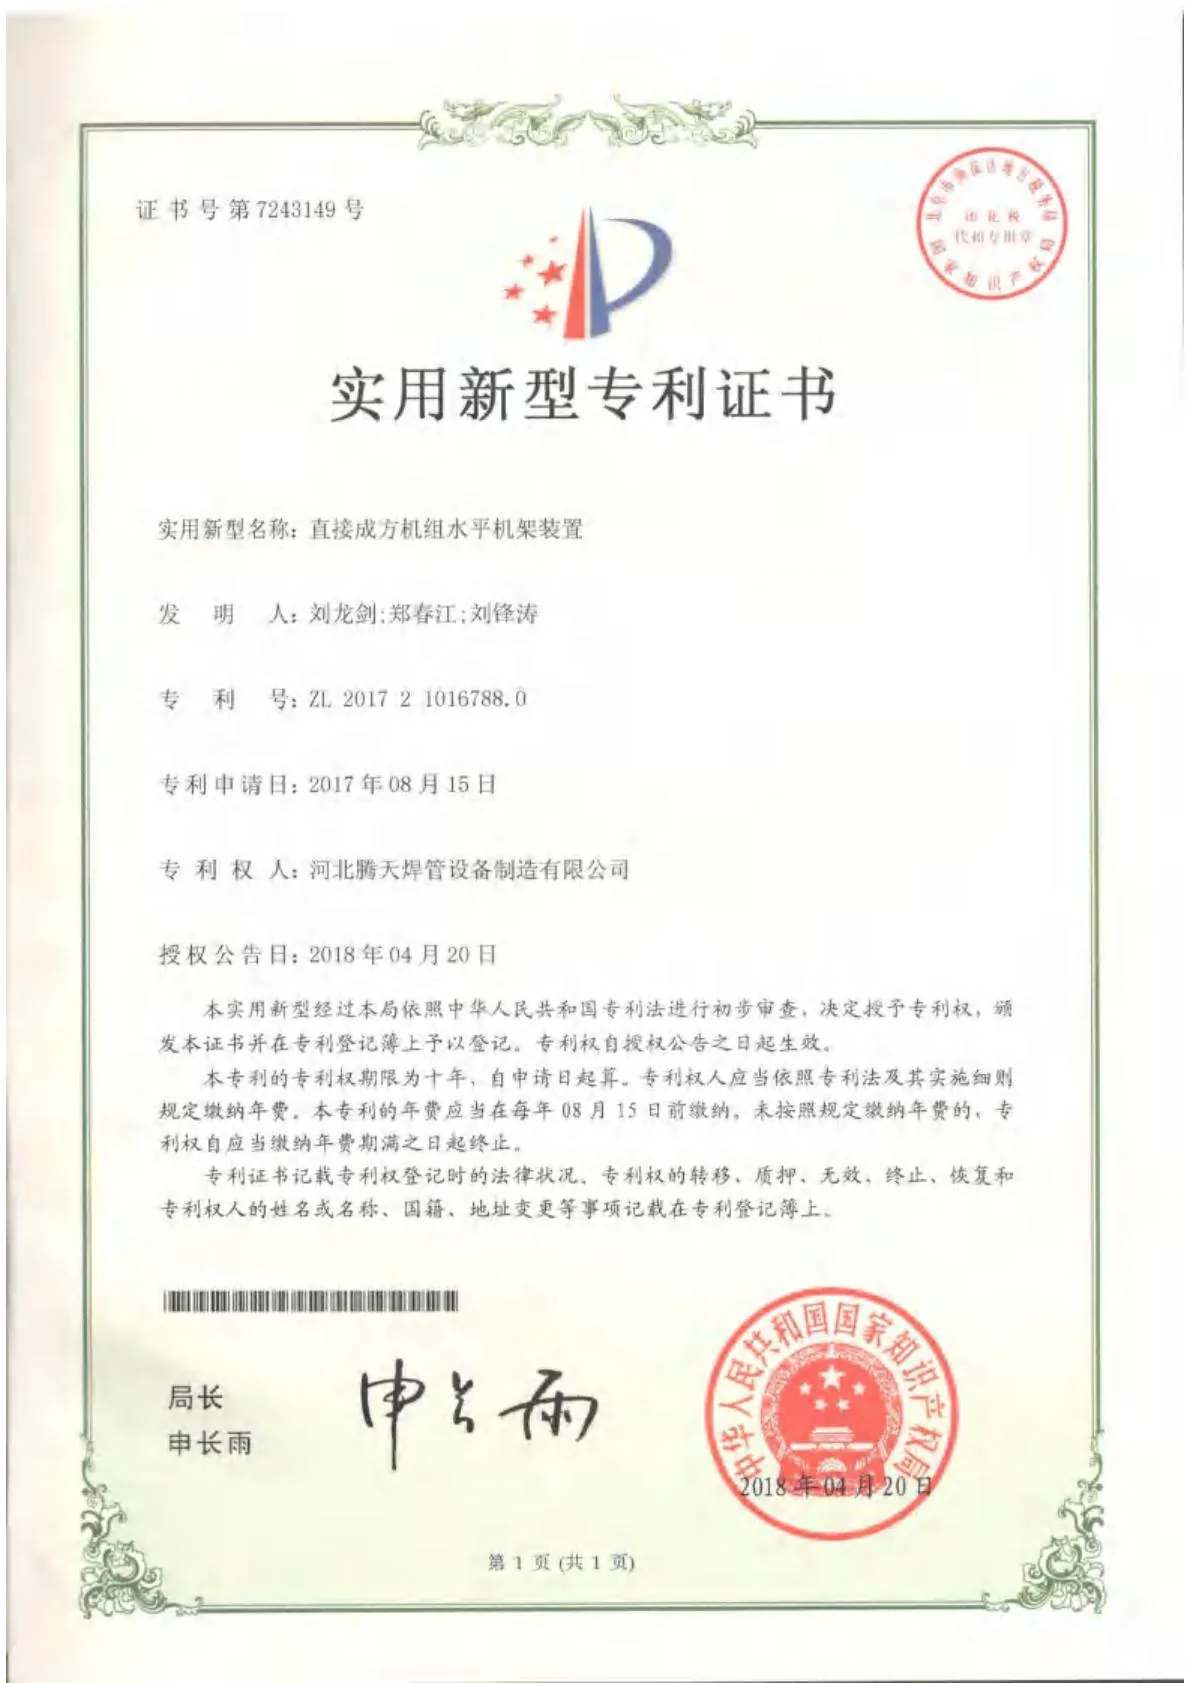
Patents — 30 granted utility model patents, with 7 invention patents applied for. Representative inventions: square tube production line (ZL 2019 1 0764631.3 / CN 110355611 B); H-beam assembly device (ZL 2022 1 1713036.5 / CN 115676238 B); steel pipe painting line (ZL 2024 1 0199417.9 / CN 117772471 B).
Delivery record — 20 documented deliveries across 15 countries (Afghanistan, Egypt, Pakistan, Russia, South Korea, Kyrgyzstan, Kenya, Malaysia, Mexico, Sri Lanka, Thailand, Türkiye, Uzbekistan, Italy, India), each with site photographs.
- Manufacturing and engineering:
- In-house CNC machining of forming rolls and key wear parts — the reason spare rolls stay available years after handover.
- Own production base, open to factory audit.
- Engineering team of 20, averaging 20 years’ experience.
- Export packing is specified per item, not generically: control cabinets, impeders and induction coils, forming rolls and cutting tools travel in moisture-protected wooden cases with a spare-parts pack, while heavy large-diameter frames ship bare, braced on cradles with designated lifting points and rust protection.
- Operating economics buyers ask about most:
- Yield ≥ 93%.
- Roll saving > 90% on direct-square-forming lines — size change by combined dies rather than by roll change.
- Lead time 50–90 days.
- Round-the-clock response, single point of contact, all-hours online support, on-site dispatch, direct spare-part shipment.
Certificates Held
ISO 9001, CE for welded pipe and cold roll forming equipment, and the patent and inspection records behind them. Full copies are available on request.
Before You Specify a Line
The reference material buyers ask for first — process, standards and the running numbers, written by the engineers who build and commission the lines.
Talk to an Engineer
Large-diameter heavy units (HG508–630 and API classes) ship bare on reinforced frames with lifting points designed in, which keeps packing cost down but requires professional lifting at the destination.
From there the process is: line sizing against those three numbers → tiered configuration with the scope of supply written out → delivery schedule → contract. Payment terms are flexible and third-party escrow is available; staged payment is used on larger projects.
Installation, commissioning and operator training are included in the after-sales scope; engineers are dispatched to site.
Shipping is planned as part of the scope, not left to the buyer.
A complete line is broken down into container-shippable units: bare machine frames strapped and fixed, precision and electrical items — control cabinets, induction coils and impeders, forming rolls, cutting tools — crated in moisture-protected wooden cases, with spare rolls and tooling travelling in the same shipment.
Once a line is running, what keeps a plant with one supplier is unglamorous: stable operation with low fault rates, spares that keep arriving, an answer round-the-clock when something stops, a delivery date that held the first time, and consistent equipment when the plant later adds a second line.
A 30-minute technical video call — or a live video walk-through of the works — can be booked before any commercial discussion.
Reply round-the-clock. One named contact stays with the enquiry from quotation through build and commissioning — the person who answers the first message is the person who follows the project through.
An enquiry does not need a full specification. Three numbers are enough to start: target outside diameter, wall thickness, and required output.
Get a Quote — Tell Us Three Things
Target outside diameter, wall thickness, required output — send those and you get a line sizing and a tiered configuration with the scope of supply written out. One named contact, reply from a single named contact.
Send Your Enquiry
Tell us the pipe outside-diameter range, the wall thickness and the output you need. An engineer reads every enquiry — it does not land in a general sales inbox.