
 Scan on WeChat
Home › Purlin Machine Lines › CZ Purlin Roll Forming Machine
In This Line
Quick Contact
Hebei TengtianYuanle@tentubemill.com
+86-311-83025332
WhatsApp +852 5425 3155
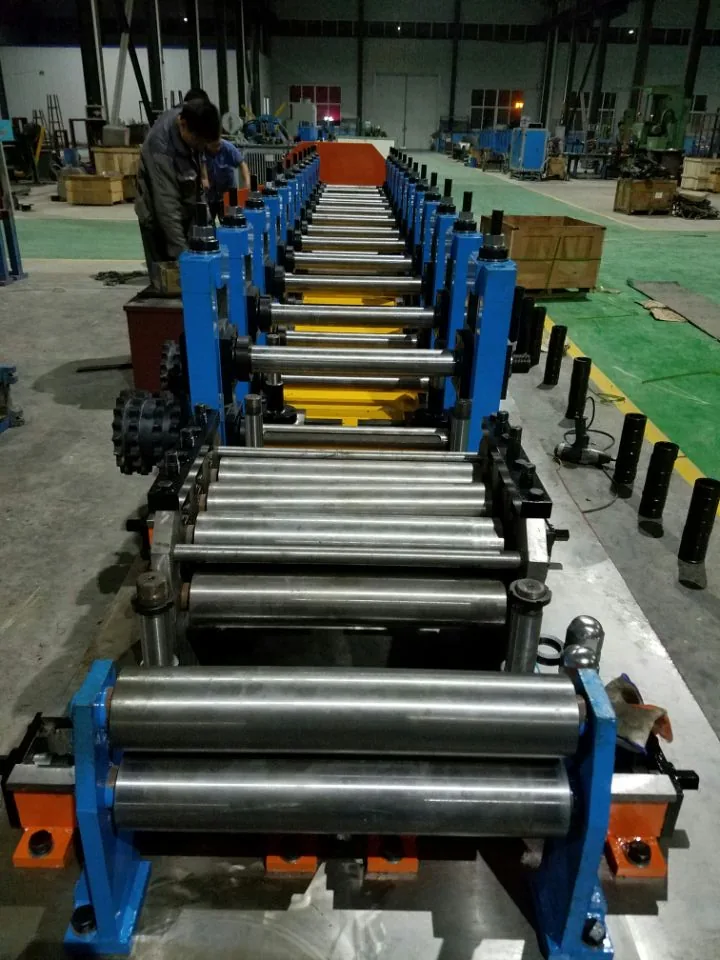
The C/Z/Ω purlin line cold-forms steel strip 2–4 mm thick into C, Z and Ω sections on one machine, at forming speeds up to 20 m/min, punching and cutting automatically from an entered length, hole pitch and quantity.
Technical Specification Table
| Parameter | Value |
|---|---|
| Line type | Semi-automatic C/Z interchangeable purlin line |
| Sections produced | C / Z / Ω on one machine |
| Strip thickness | 2–4 mm |
| Forming passes | 18 passes |
| Forming speed | up to 20 m/min |
| Size change | Stepless adjustment — no roll change |
| Punching & cut-off | Hydraulic, automatic from entered length / hole pitch / quantity |
| Forming roll material | Bearing steel, hardened after machining |
| Die & cutter material | Cr12, hardened |
| Forming principle | Room-temperature progressive bending; no phase change, purely plastic deformation |
| Tooling supplied | One set of dies and cutters with the line |
| Certified profile coverage | C / Omega / Zeta / Z / open / closed profile (CE) |
| Control | PLC industrial computer + variable-frequency / servo |
| Output (sections/h, t/shift) | available on request |
| Section dimension range (web / flange / lip) | available on request |
| Manufacturing lead time (this line) | available on request |
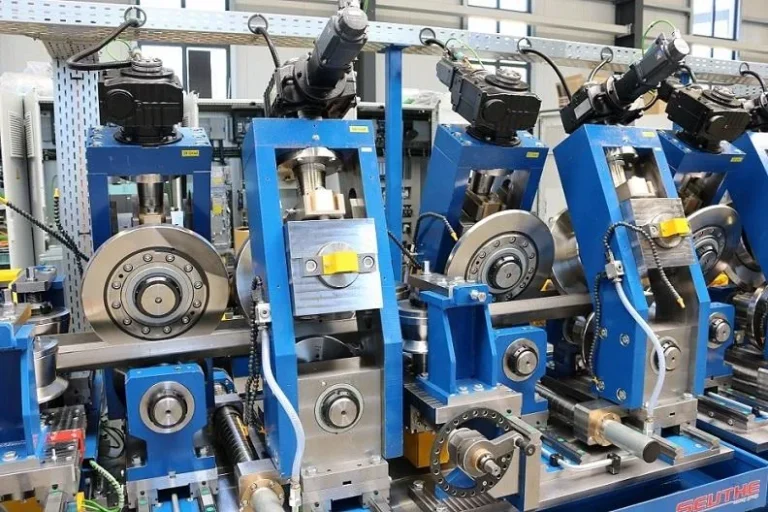
Line Configuration and Scope of Supply
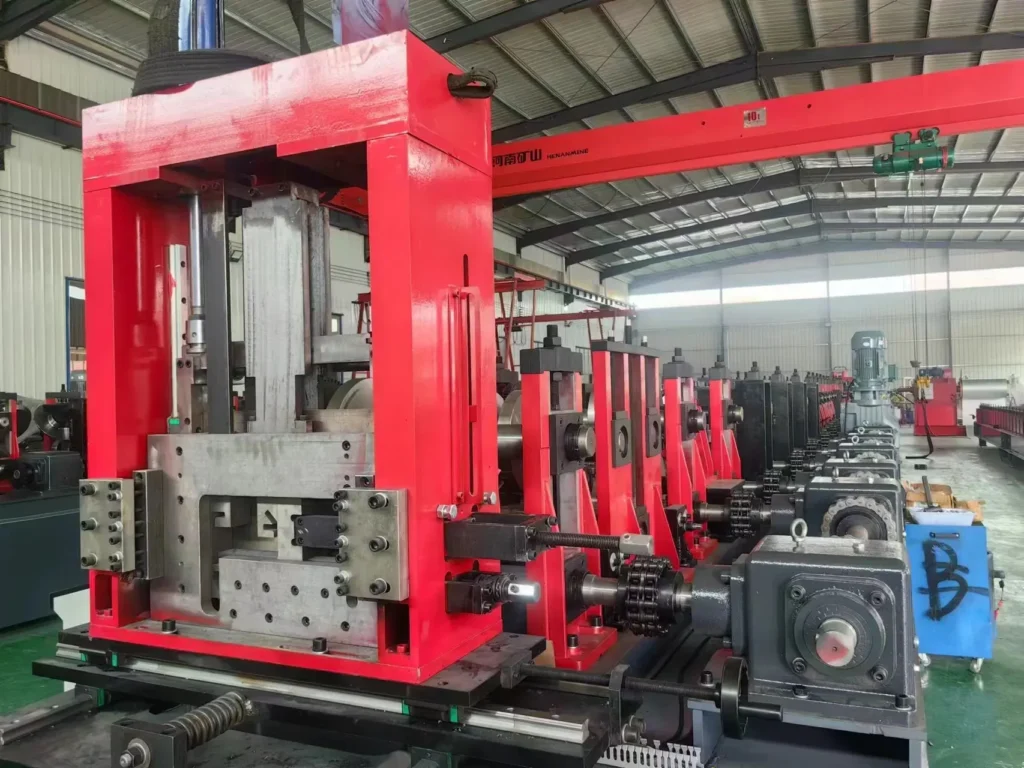
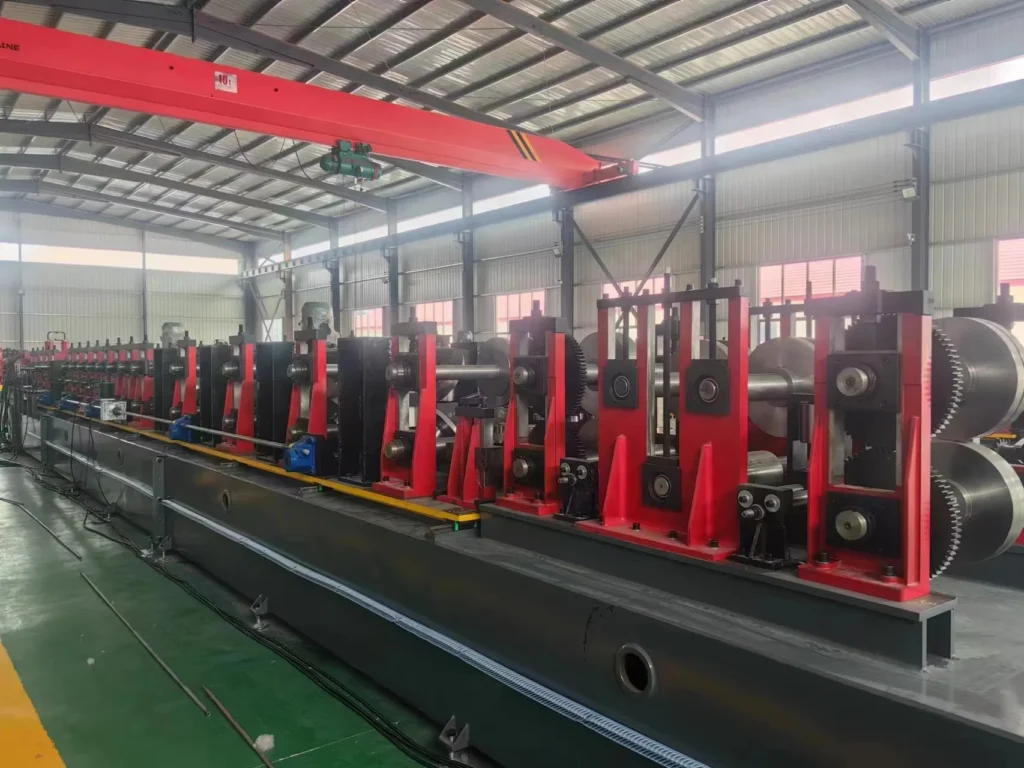
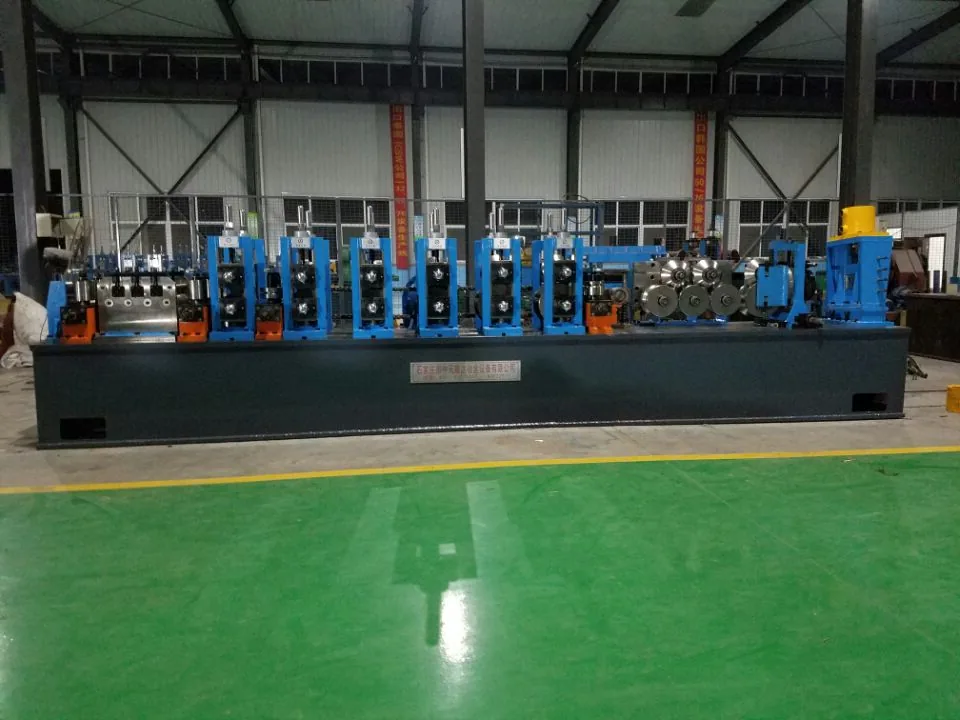
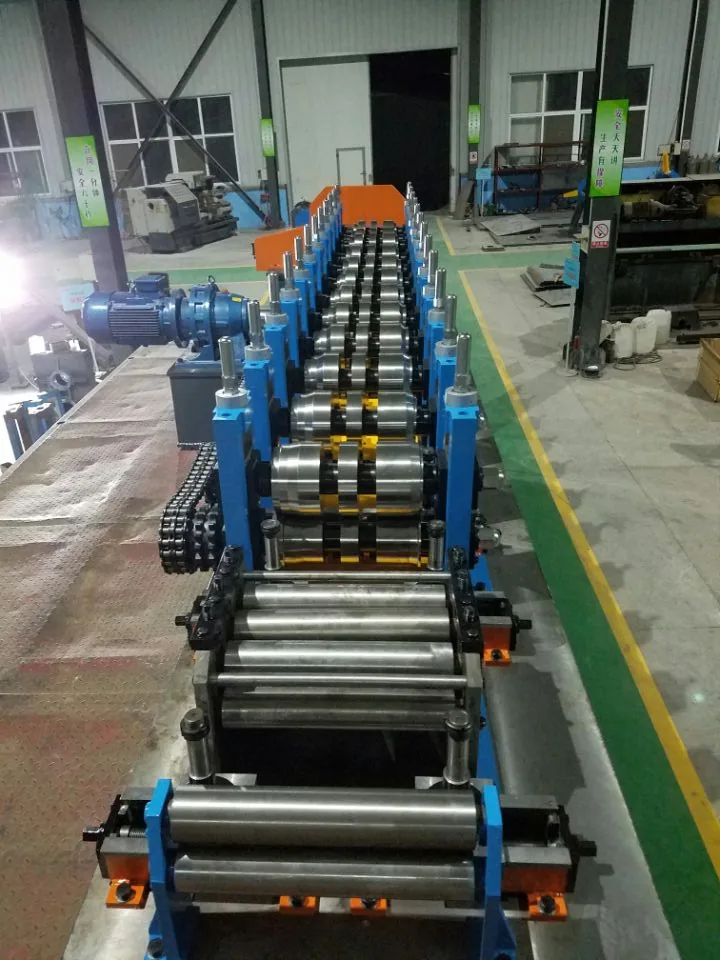
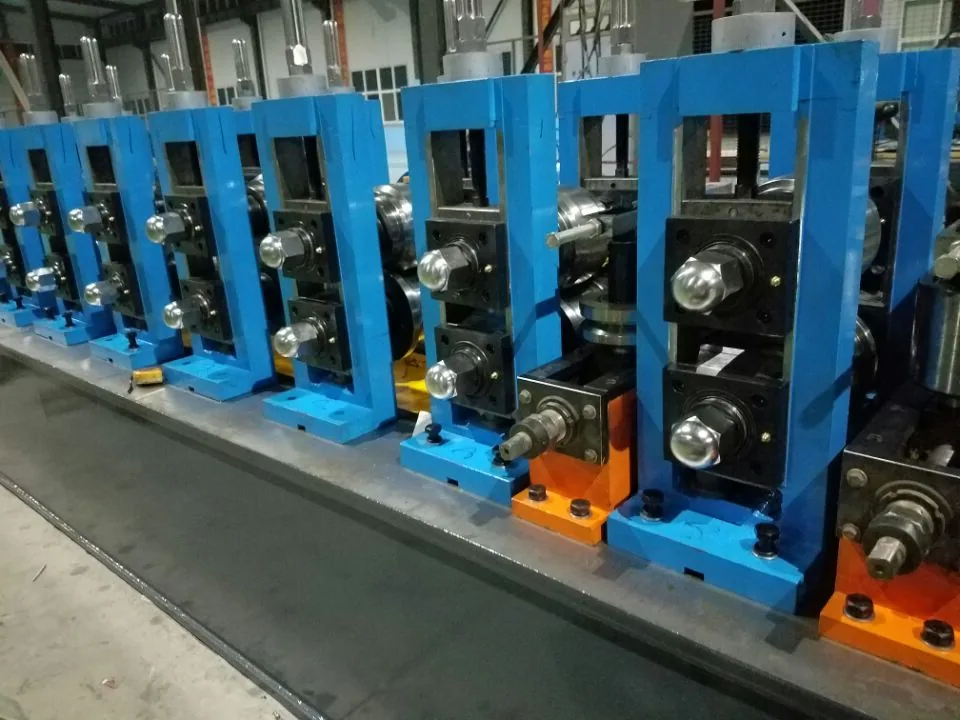
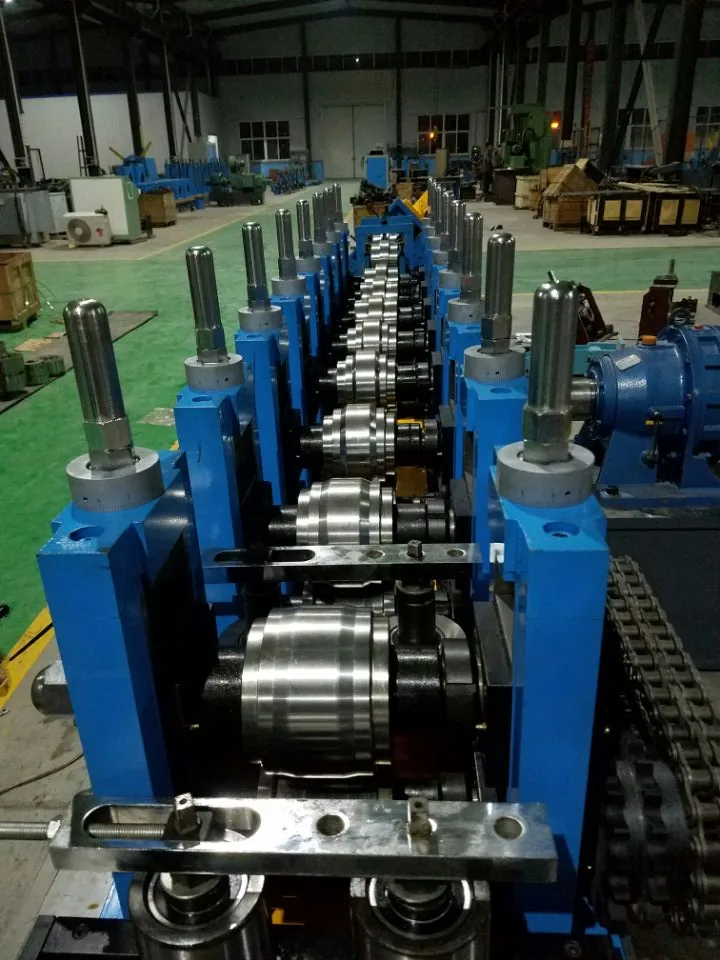
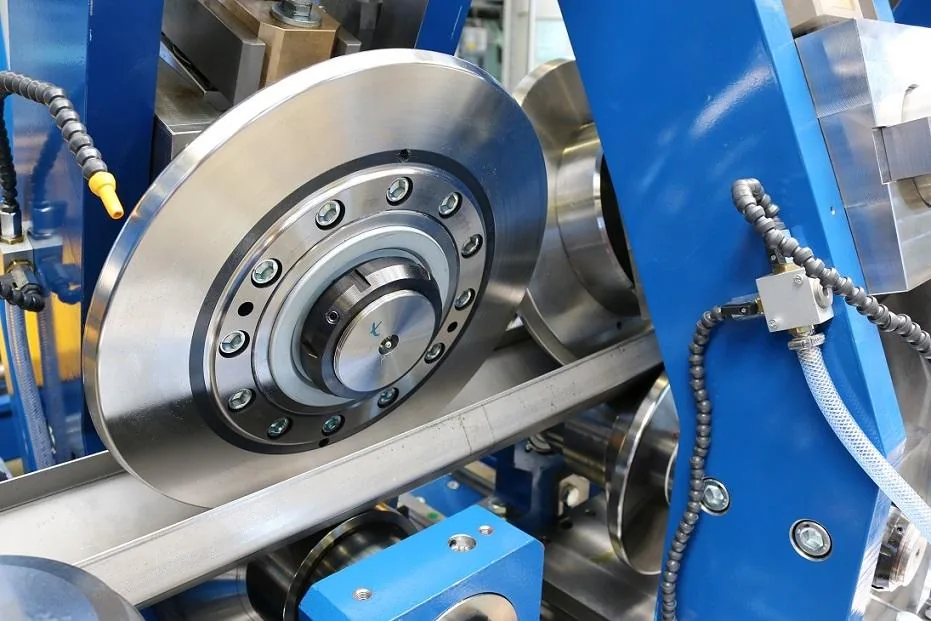
Forming rolls. Eighteen passes bend the flat strip progressively into the C, Z or Ω section. The rolls are bearing steel, hardened after machining — hardness here is not a spec sheet detail but the thing that stands between the line and poor corner definition, twisted section or early roll wear.
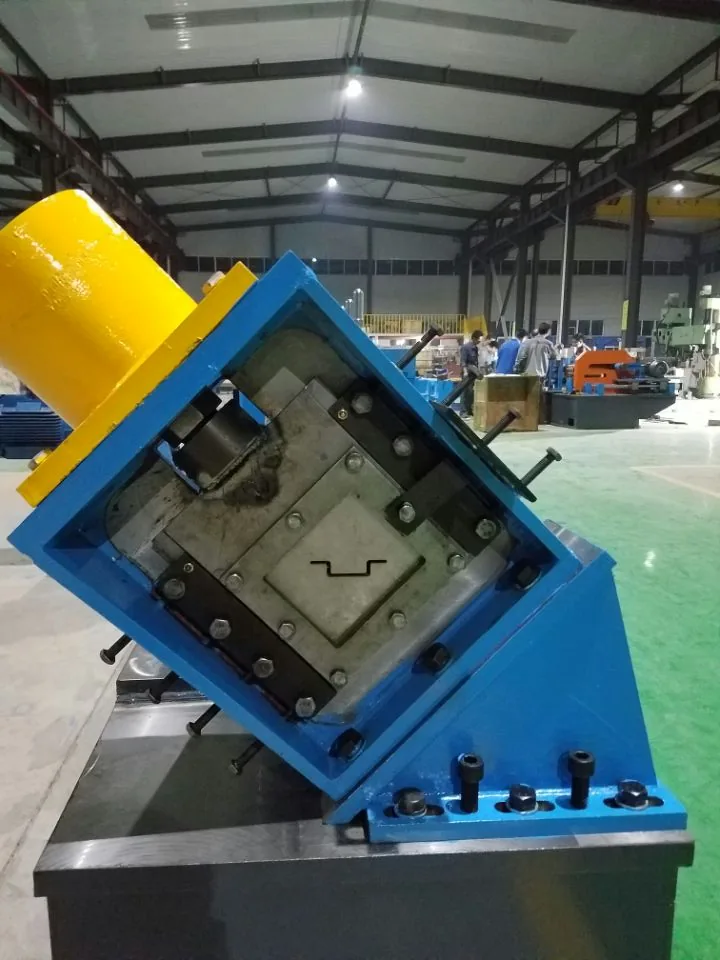
Hydraulic punching dies and cutters. Cr12, hardened. These punch the hole pattern and cut the section to length. Blunt or under-hardened tooling shows as hole-position drift and a ragged cut edge before it shows as anything else.
Parameter entry and control. Length, hole pitch and quantity are entered; the line then punches, forms and cuts without further intervention. Underneath sits a PLC industrial computer with variable-frequency and servo control, common across Tengtian’s families.
One set of dies and cutters travels with the line, so the plant is not sourcing tooling during commissioning.
Why eighteen passes rather than fewer. Cold roll forming works by bending the strip a little at a time: each pass takes the section closer to its final shape without exceeding what the material will accept in one step.
Pass count, roll profile and the yield strength of the strip together decide the geometric accuracy of the finished section and how much springback has to be designed out. Fewer passes means more deformation per stand, and that surfaces as poor corner definition and a section that will not hold tolerance.
Why there is no welder on this line. The section is open, so nothing has to be closed. That removes an entire class of equipment and an entire class of failure — no induction welder, no impeder or coil as wear items, no post-weld cooling, and no weld to inspect.
It also removes the recovery mechanisms: a tube mill has a sizing stand after the weld that pulls dimension back, and a forming line does not. What comes off the last pass is the product.
Scope of supply is quoted two ways across all Tengtian families — a turnkey line delivered complete, or individual machines and units where the plant already has part of the chain — and automation level is selectable, semi-automatic through fully automatic.
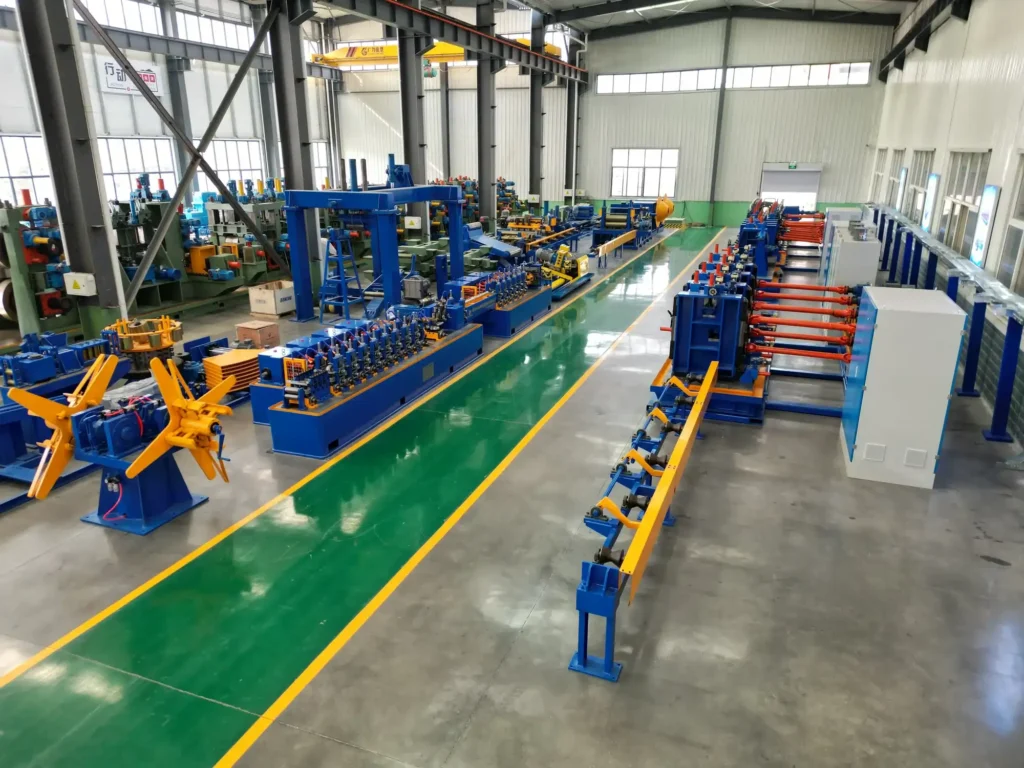
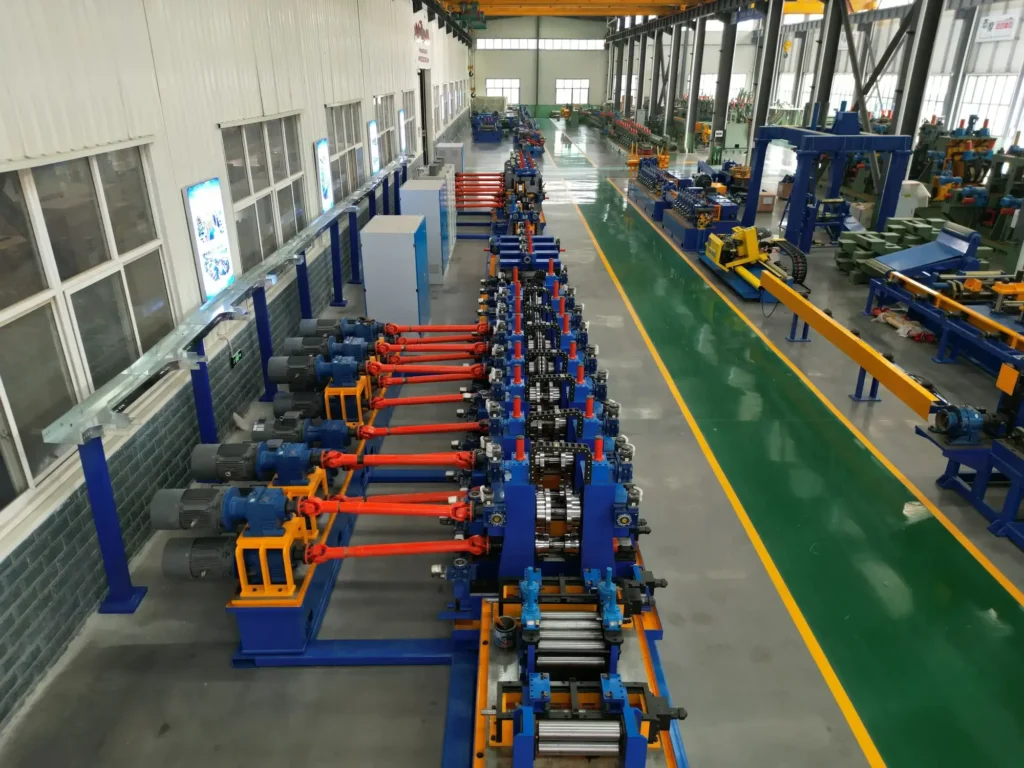
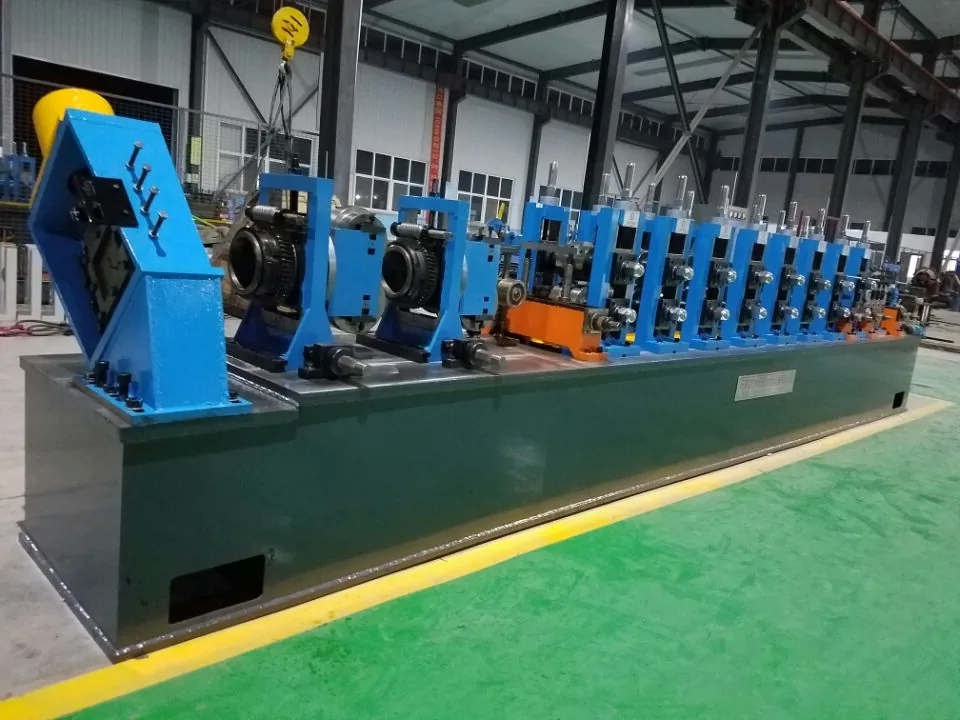
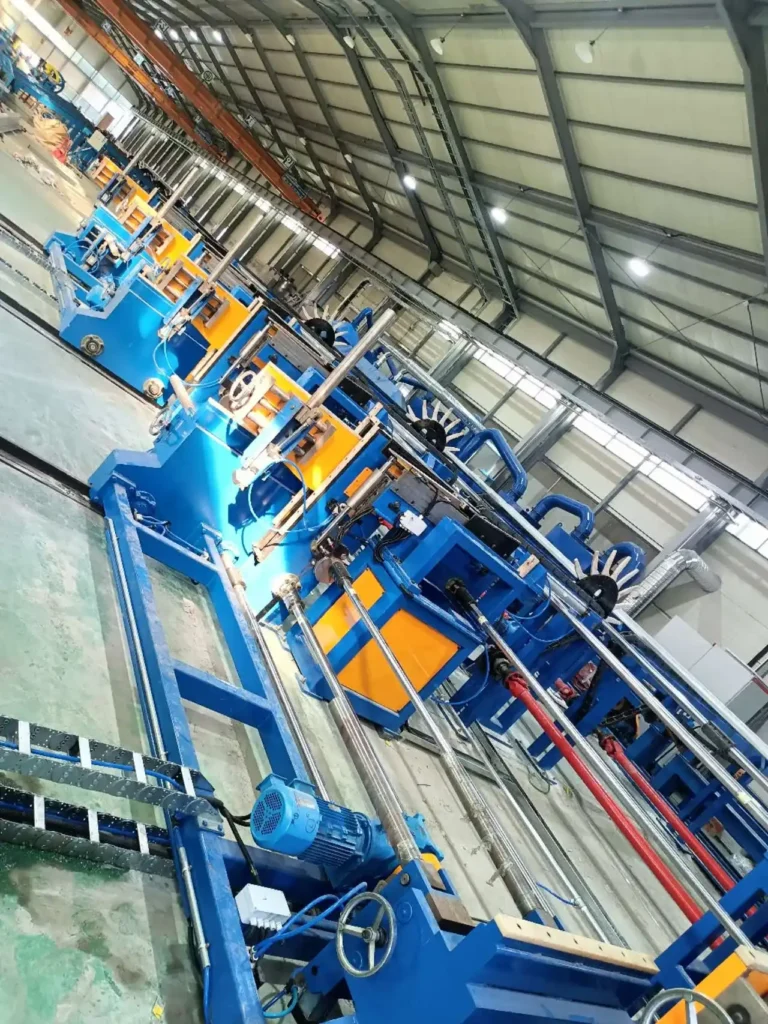
The line is short compared with a tube mill, and three assemblies carry it:
Size Change, Roll Wear and Running Cost
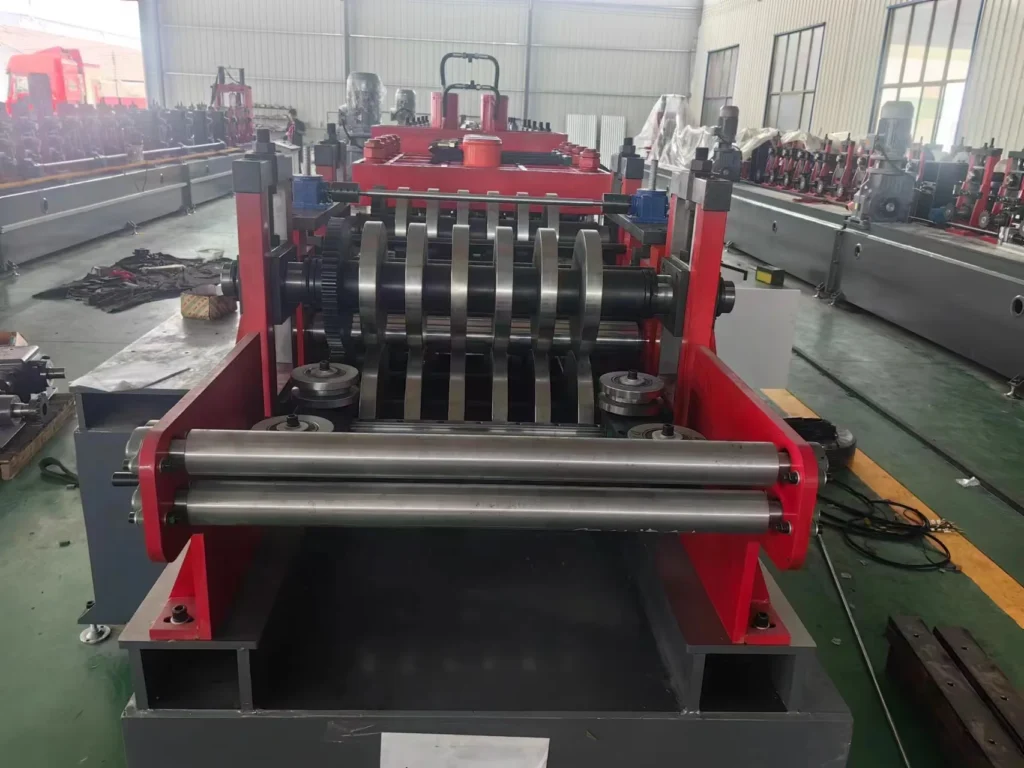
The controls that prevent it are unglamorous — hardened tooling, accurate hydraulic punch positioning, disciplined parameter entry — and they are the reason die material is specified as Cr12 rather than left open. Size change is the selling point of this line. Multiple purlin sizes come off the same machine by stepless adjustment — no roll change. For a fabricator running C and Z sections in several depths against different building contracts, that is the difference between a tooling change and a setting change.
It is worth being precise about what “no roll change” does and does not mean, because the phrase is used loosely across this industry. On this line it means the C and Z sections are interchangeable on one machine and multiple sizes within them are reached by adjusting the stand positions steplessly.
It does not mean any section can be produced without tooling: the roll pass sequence is what defines the profile family, and a profile outside that family is a tooling question rather than an adjustment question. Material thickness, line speed and output are confirmed against your profile section, steel grade and finished length at quotation.
Send us those three and we will state the figures.
- What wears, and on what clock:
- Forming rolls — replacement wear parts, consumed by output volume. Machined at the works on its own CNC equipment, so a replacement set years later matches the set delivered with the line.
- Punching dies and cutters (Cr12) — both wear parts and consumables, re-ground or replaced by punch count. This is the clock that actually runs on a purlin line: a tube mill counts welding hours, a forming line counts punches.
Where quality is decided, in order: roll, die and cutter hardness; the entered parameters; and the stepless-adjustment alignment at setup. Failure shows as hole-position offset, twisted section, or a blunt cut edge — and all three surface downstream as assembly problems rather than as visible machine faults.
That last point is the one worth carrying into a purchase decision. On a tube mill a bad weld fails a pressure test at the works; on a purlin line a hole four millimetres out of position passes every check the fabricator runs and fails on the building site, in someone else’s hands, weeks later.
- What Tengtian supplies around the machine, common to all four equipment families and unchanged here:
- Forming rolls and key wear parts machined in-house on the works’ own CNC equipment rather than bought from an outside shop — on a forming line, where tooling is the capability, that matters more than on a tube mill.
- Own production base, open to factory audit in person or by live video walk-through.
- An engineering team of 20 averaging 20 years each, doing the line sizing.
- Tiered configuration mapped to a written scope of supply; staged payment, adjustable deposit ratio, third-party escrow and several workable Incoterms.
Who buys a purlin line. Two doors, as across the range. Either capacity is being built — a new fabrication shop, an expansion, or a move into PV mounting sections — or an incumbent supplier has failed: tooling stopped arriving, changeover cost too much time, or delivery slipped against a construction date.
The second group asks a narrower question than the first, and it is usually about Cr12 die supply rather than about the machine.
Responsibility boundary. The equipment controls hydraulic punch positioning and roll profile accuracy; the plant controls the entered parameters and the setup. Hole position and section geometry on the finished purlin depend on both.
Incoming strip grade and flatness remain the buyer’s responsibility, as on every Tengtian line; on a forming line there is no welding stage to absorb a material defect and no sizing pass to pull the section back, so what the rolls produce is what ships.
Operator training is a stated requirement for this line, not an optional extra.
Applications and Output Examples
Buyers judge the line on three points, and it answers each — stepless adjustment without roll change, hydraulic punch positioning with Cr12 tooling, and up to 20 m/min. Two user groups buy this line: steel-structure fabricators making building purlins, and photovoltaic mounting fabricators making bracket sections. Both feed the same machine with an entered length, hole pitch and quantity and take C, Z or Ω sections off it.
Both measure the line against the same short list: whether a size change needs a roll change, hole-position accuracy, and forming speed.
That is why we lead with stepless adjustment and 20 m/min rather than with a section catalogue — those are the two points buyers ask about.
The Ω section is worth a line of its own, because it is the section PV fabricators come for. It comes off the same machine as C and Z, under the same stepless adjustment, and it is named explicitly in the CE certificate’s covered profiles alongside C, Zeta and Z.
Cold roll forming also sits inside a wider works. Tengtian organises its business into four equipment families — welded pipe production lines, slitting and cut-to-length lines, cold roll forming lines, and H-beam production lines, with an automatic spray-painting line as a companion unit.
For a purlin fabricator the practical consequence is upstream: a forming line runs from strip of a defined width, and slitting a wide coil down to that width is a separate line that can come from the same works, with the same spare-parts channel and the same contact.
The beneficiaries sit one step further out — steel-structure projects and PV plant construction — which is why lead time on a purlin line tends to be tied to a construction schedule rather than to a production plan.
Delivery, Installation and Training
Certification for this equipment class is verifiable by number: CE — UDEM, cold roll forming equipment, M.2022.206.C72172, covering C, Omega, Zeta, Z, open and closed profile; and a technical file verified by Ente Certificazione Macchine Srl (Italy), 0P250616.HTWTT37 (TCF OCT20250611103M).
A single named point of contact carries the enquiry through delivery and after-sales, with a first reply committed round-the-clock and all-hours online support; the same person later holds the tooling re-order history, which on this line is what matters most over the working life of the machine.
Shipment: precision items — control cabinet, forming rolls, dies and cutters — crate in moisture-protected wooden cases with the spare tooling set travelling in the same consignment; machine frames ship strapped on reinforced supports with lifting points designed in.
The general 50–90 day delivery figure is an all-lines figure; the schedule for a specific roll-forming line is confirmed with the quotation.
Installation, commissioning and operator training sit inside the after-sales scope; engineers are dispatched to site and support continues online after handover. On this line training is load-bearing rather than courtesy — parameter setup and stepless-adjustment alignment are where hole position and section geometry are won or lost.
PV bracket purlin machine
CZ purlin making machine
Line Photos from the Works
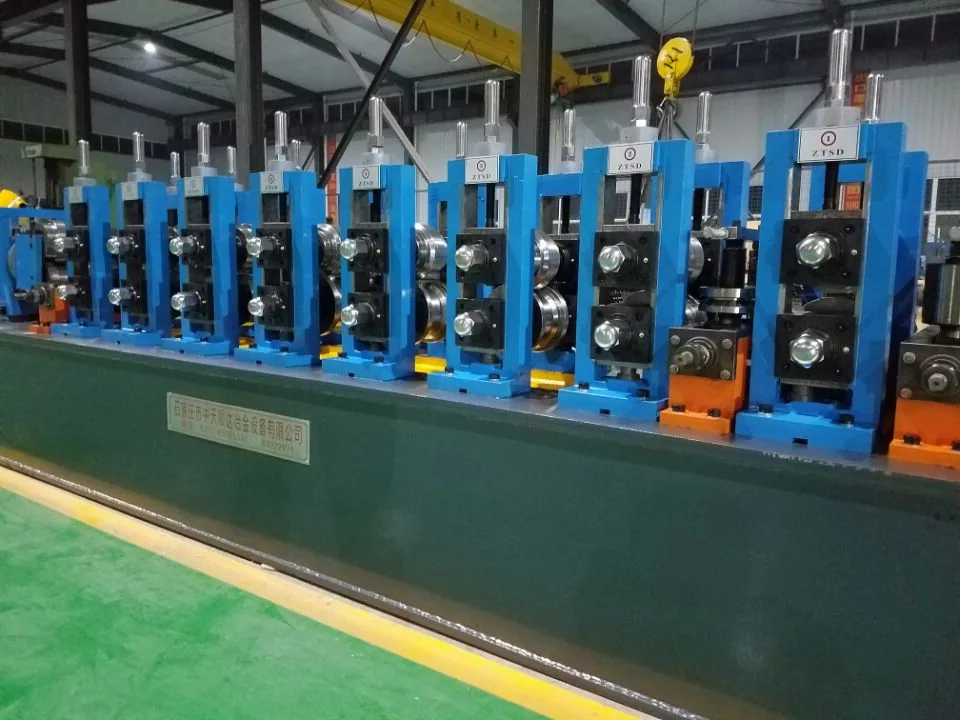
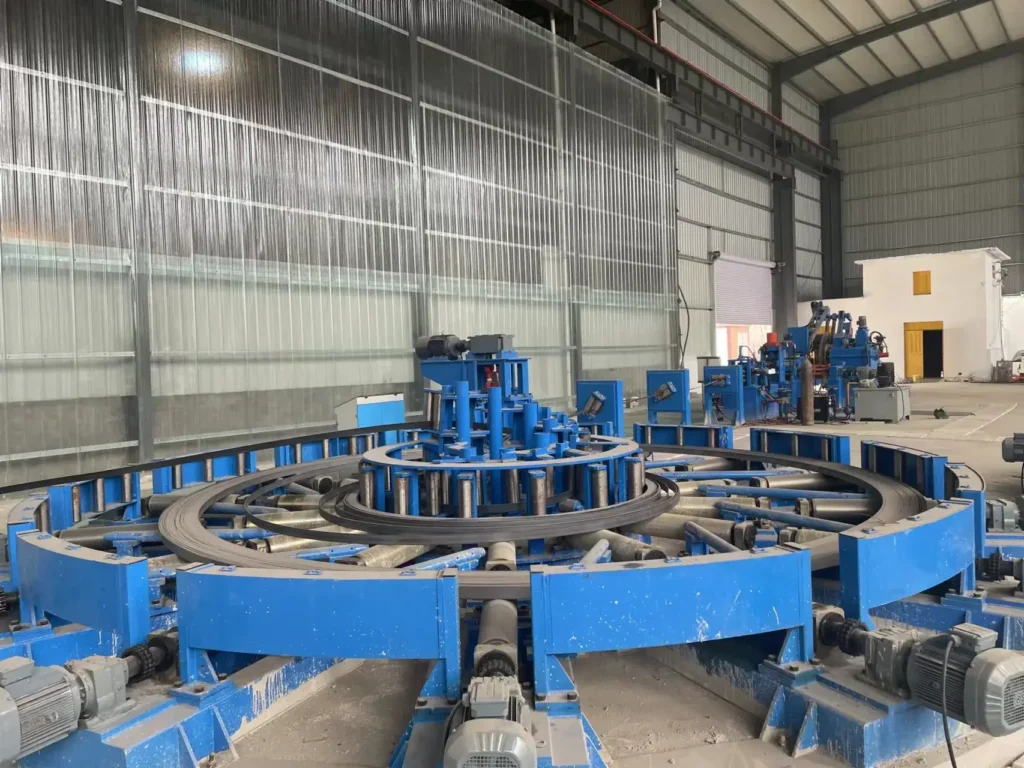
Eight photographs of this line, taken in our own workshop. Click any photo for the full-size image.
Watch This Line Running
C/Z/Ω Purlin Roll Forming Machine — 18-Pass, 20 m/min
 Changing Section Size on a Purlin Roll Forming Machine
 The API Pipe Mill Inspection Chain
 Pipe Coating Line Configuration
 H Beam Welding Line
Send Your Enquiry
Tell us the pipe outside-diameter range, the wall thickness and the output you need. An engineer reads every enquiry — it does not land in a general sales inbox.