
 Scan on WeChat
In This Line
Quick Contact
Hebei TengtianYuanle@tentubemill.com
+86-311-83025332
WhatsApp +852 5425 3155
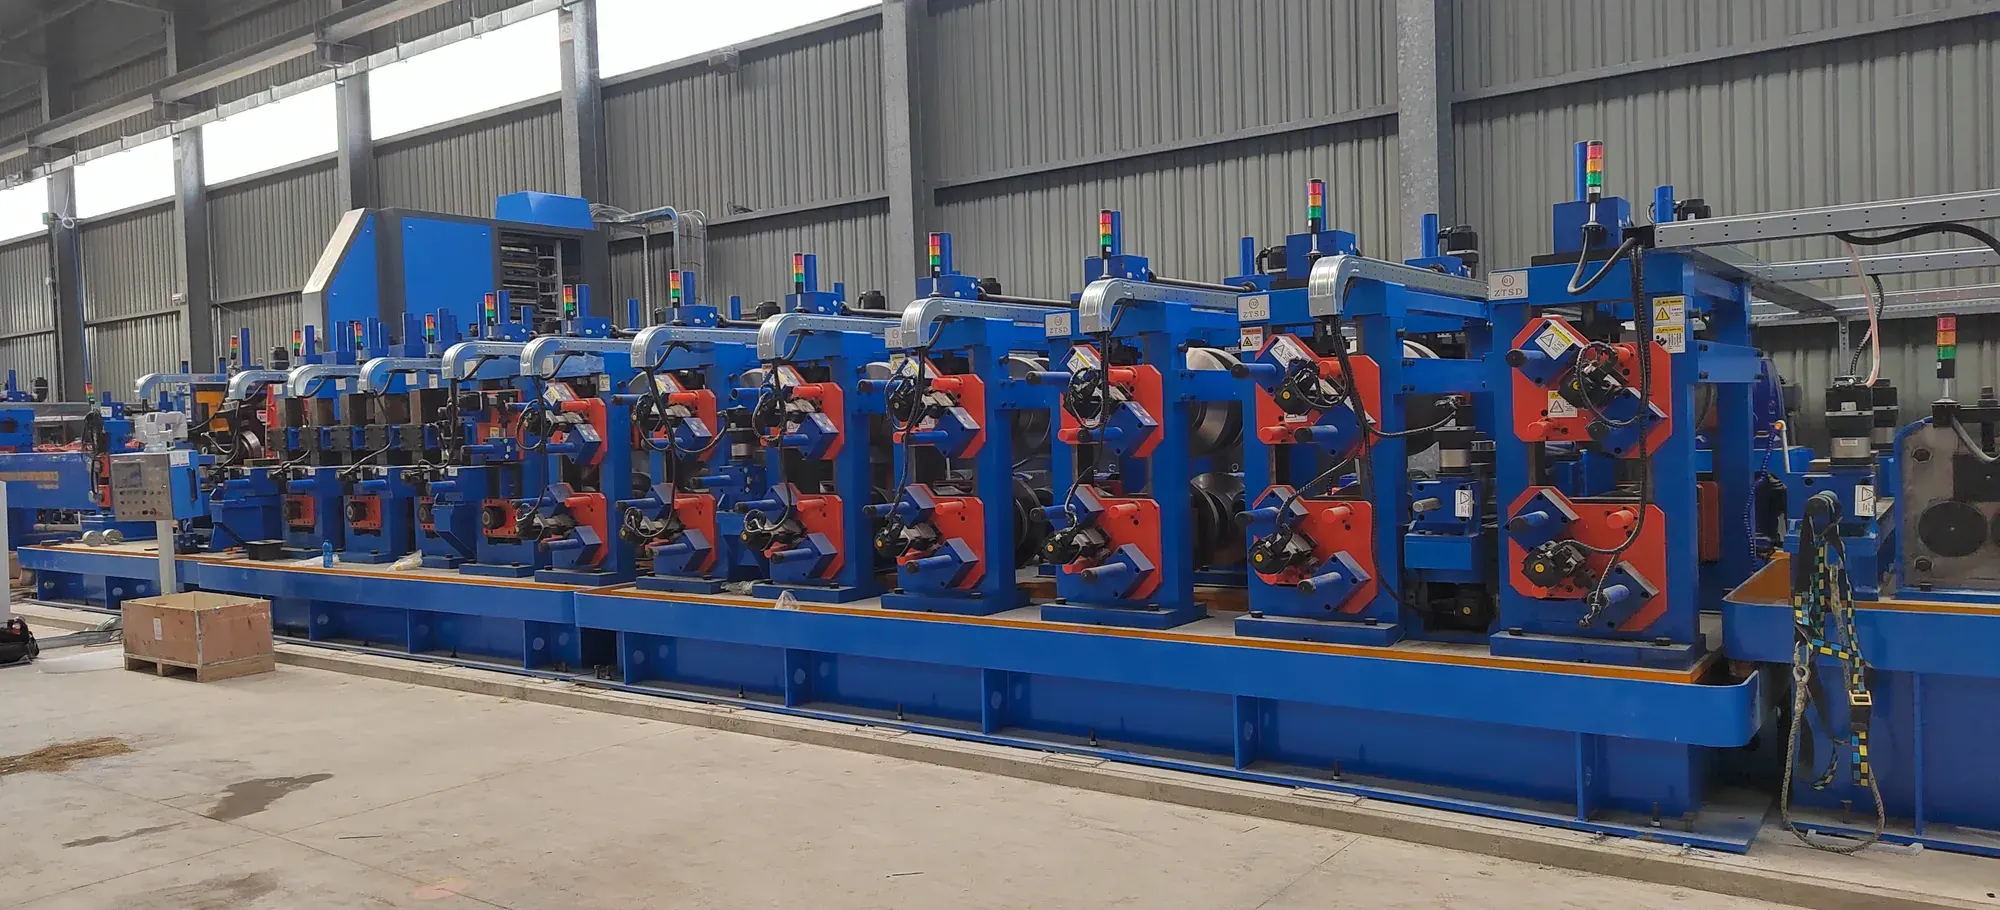
Twelve model steps cover Φ10–630 mm in round, square and rectangular section.
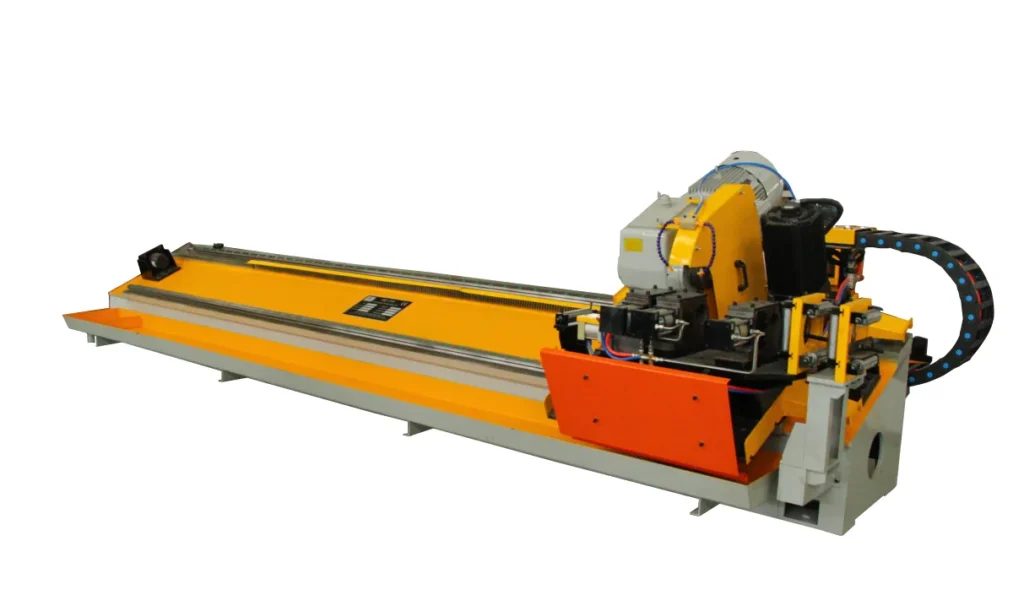
Technical Specification Table
Finished pipe — outside diameter: Φ10–630 mm, covered by twelve model steps (HG32 Φ10–32 · HG50 Φ16–50.8 · HG76 Φ12.7–76 · HG89 Φ32–89 · HG114 Φ45–114 · HG165 Φ60–165 · HG219 Φ114–219 · HG273 Φ114–273 · HG325 Φ165–325 · HG426 Φ165–426 · HG508 Φ219–508 · HG630 Φ325–630) Finished pipe — wall thickness: 0.5–16 mm across the series Finished pipe — section shape:
The table is organised by what comes off the line rather than by machine designation, for buyers who have not yet chosen a model step.
round, square, rectangular; most model steps run all three Welding process: high-frequency induction welding, whole series Forming technology: conventional roll forming, or direct forming square Automation: semi-automatic, or full-automatic under PLC control Welder power: stepped with diameter across 150–1500 kW Material yield: 93% or better by line design
HG32 = 150 kW and HG630 = 1500 kW. Intermediate steps (HG50 / HG76 / HG89 / HG114 / HG165 / HG219 / HG273 / HG325 / HG426 / HG508) are quoted per project rather than derived from the diameter band.
The pipe produced on these lines is carbon steel, including pipe for fluid transport.
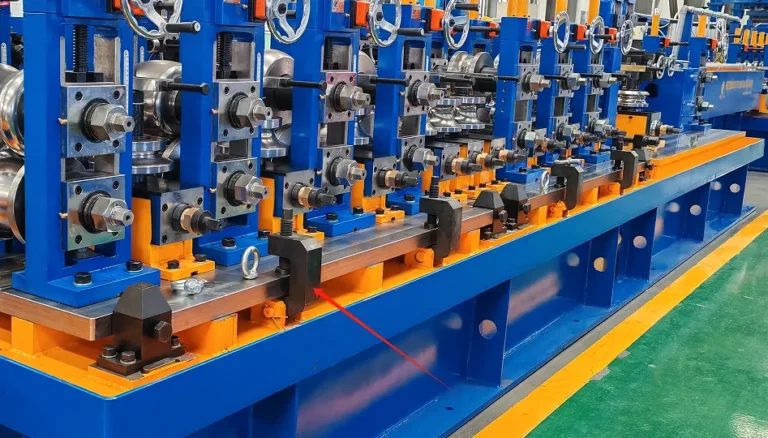
Line Configuration and Scope of Supply
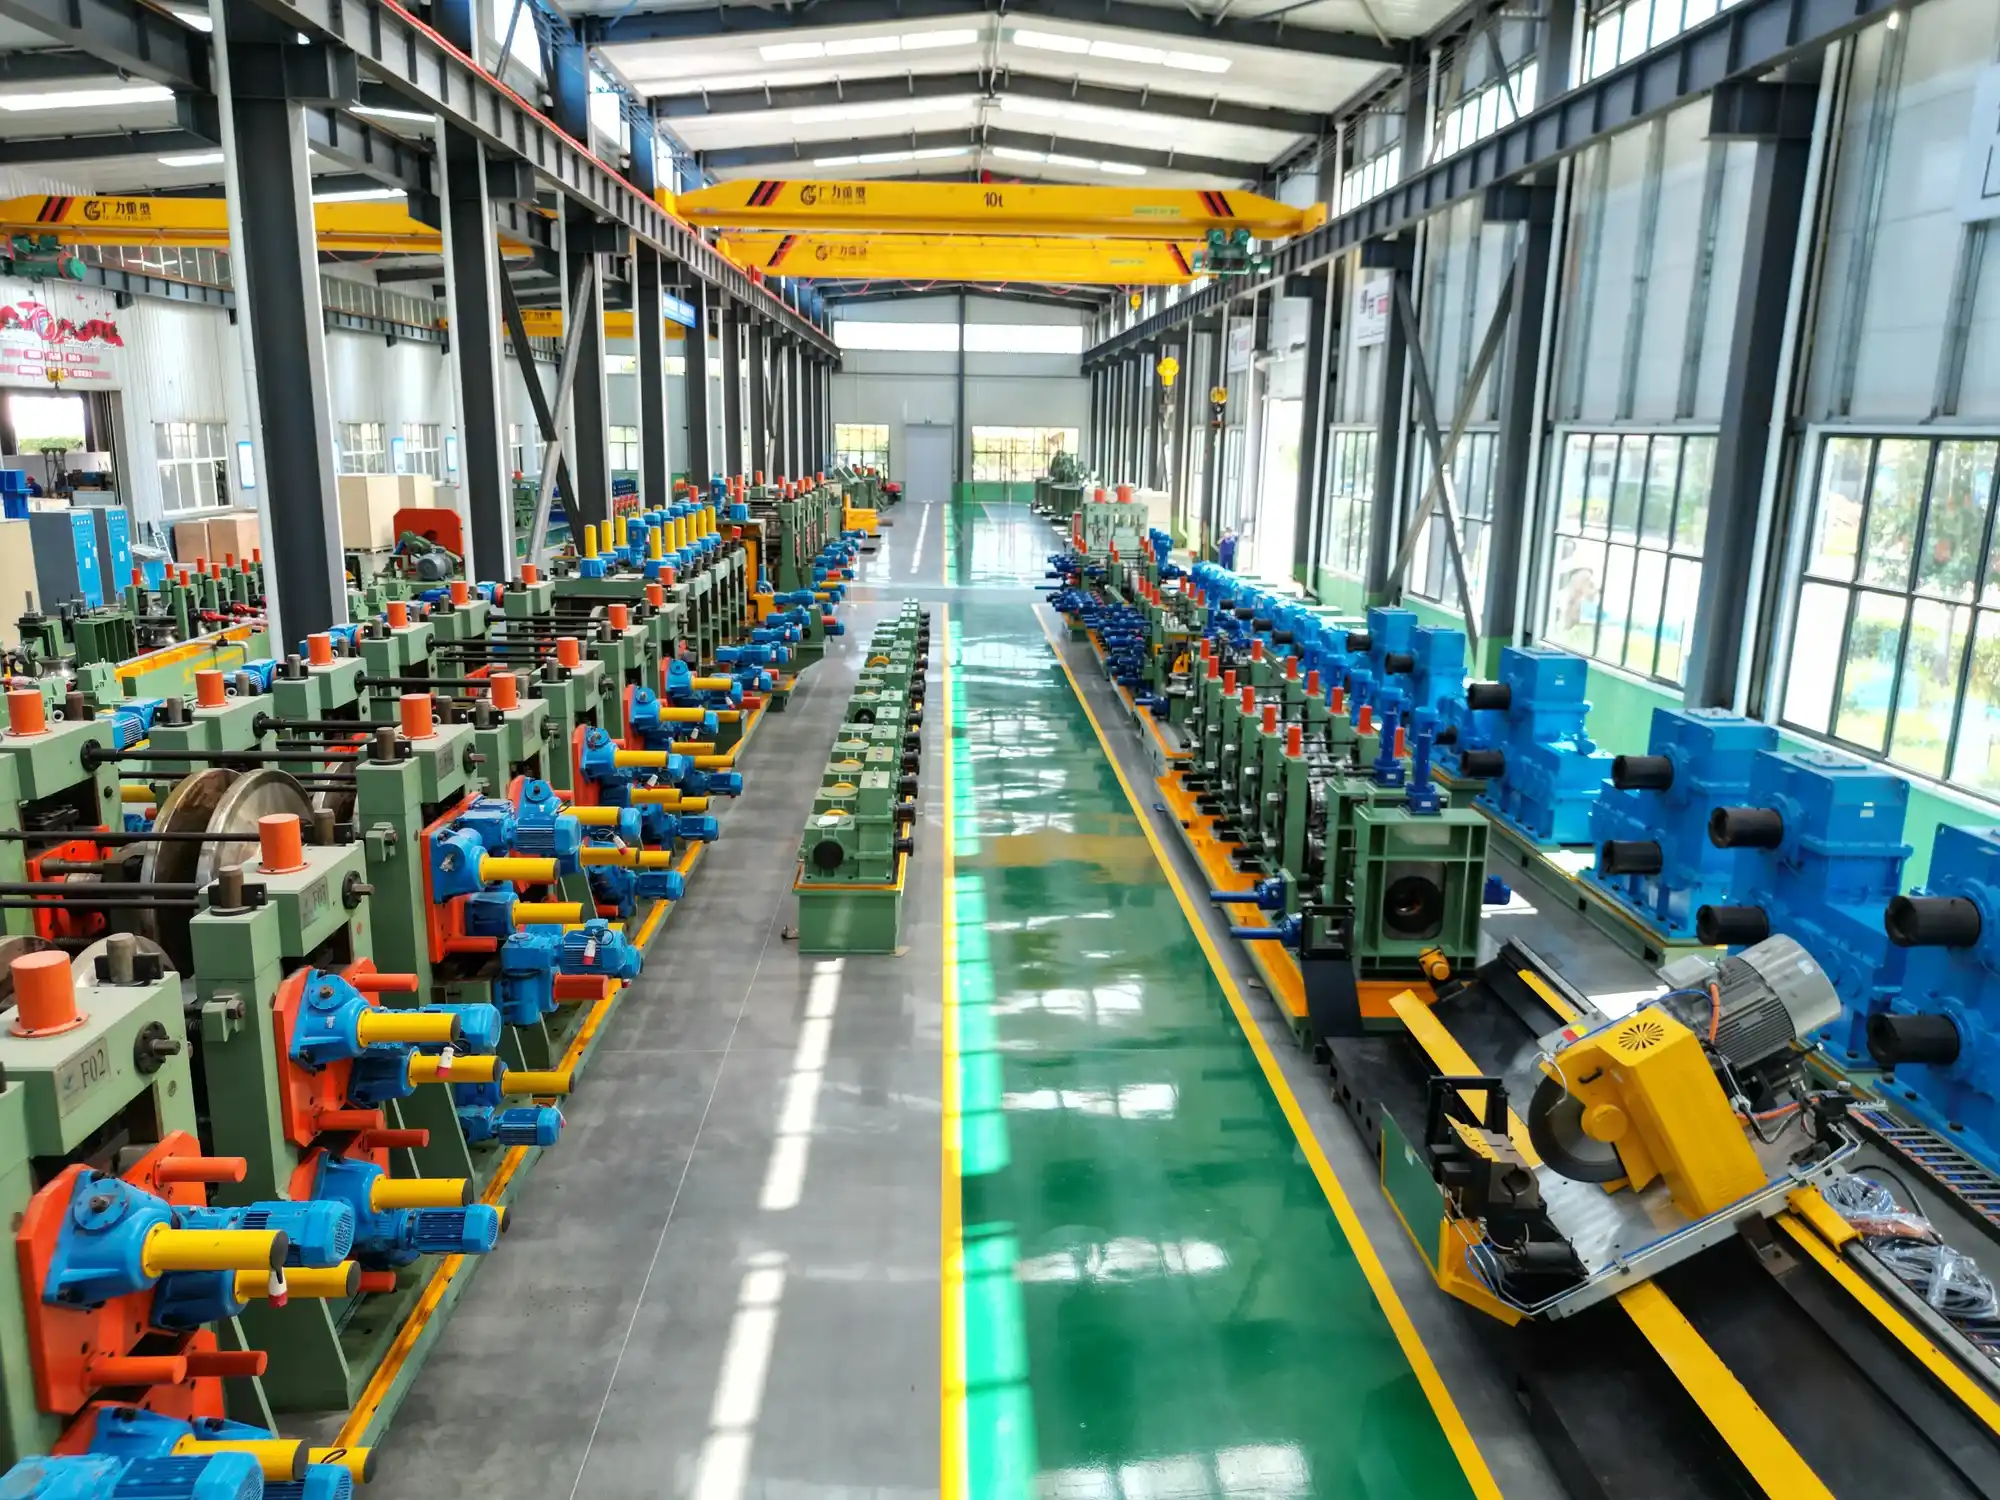
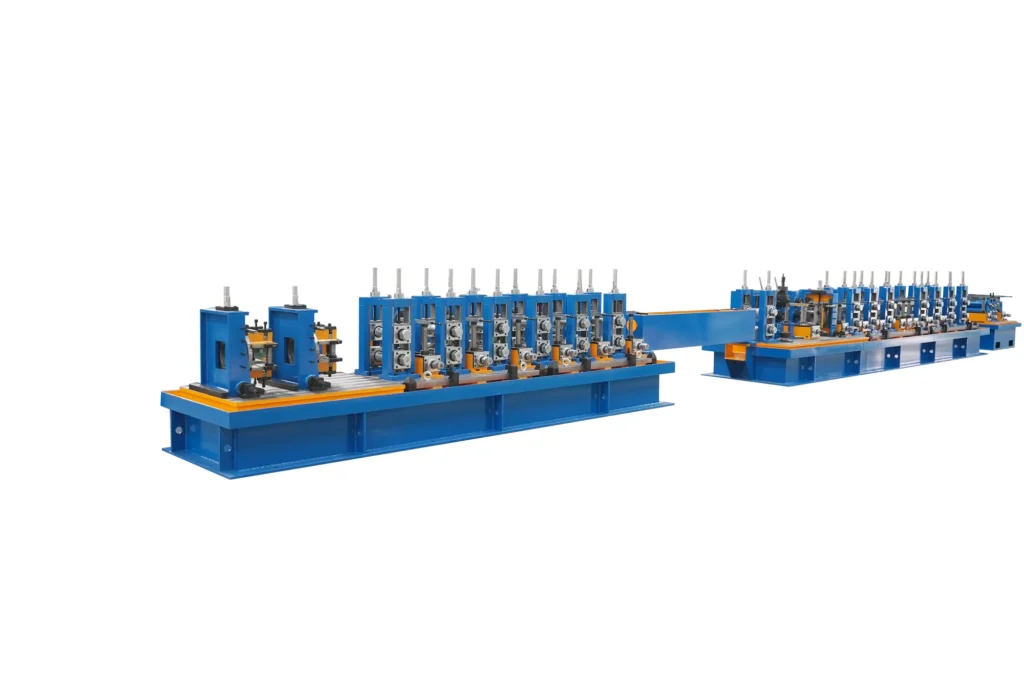
The shear-welder and the accumulator are the two units that turn a batch machine into a continuous one. What a buyer is actually purchasing is a sequence, and the value of the sequence is that it does not stop. Eight units make it up, and two of them exist purely to protect continuity.
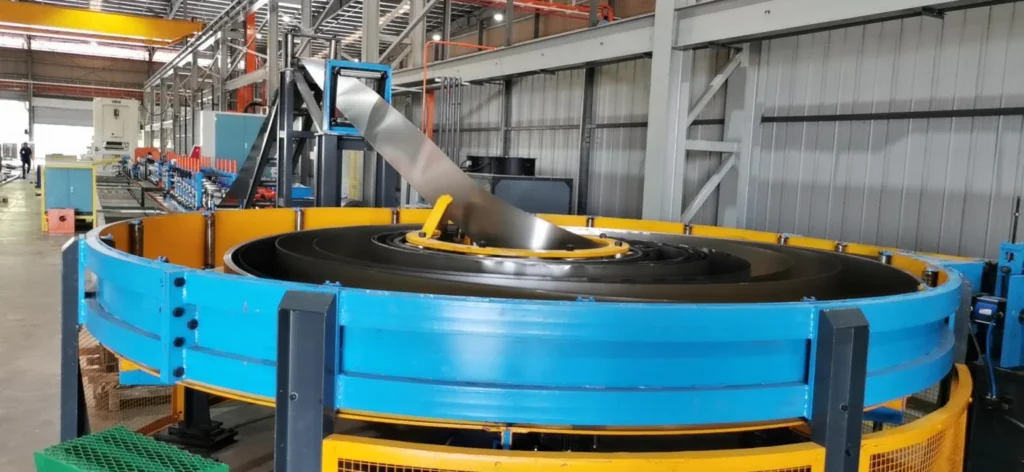
- Coil car and uncoiler — a pneumatically expanding four-link mandrel tensions the coil so it neither wanders nor slackens on the way in.
- Five-roller leveller — flattens the head and body of the strip. Residual curvature here becomes seam wander later, so this is a precondition rather than a refinement.
- Automatic shear-welder — crops the irregular head and tail of each coil and butt welds one coil to the next.
- Spiral accumulator — stores strip so the forming mill keeps running while the next coil is being joined.
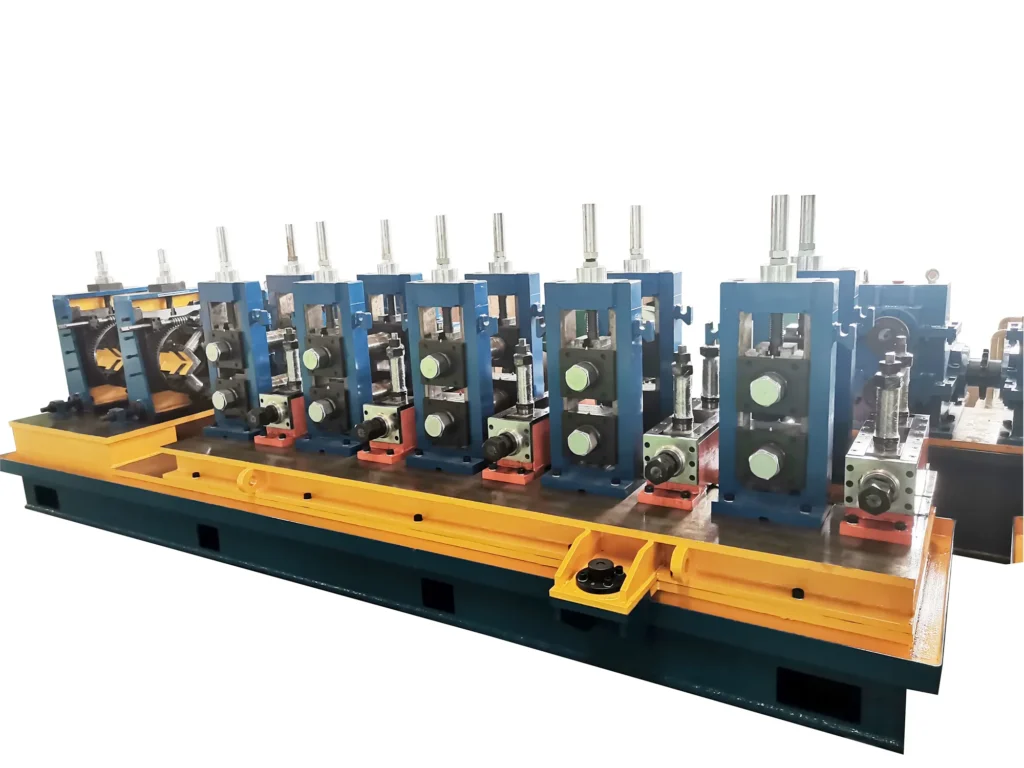
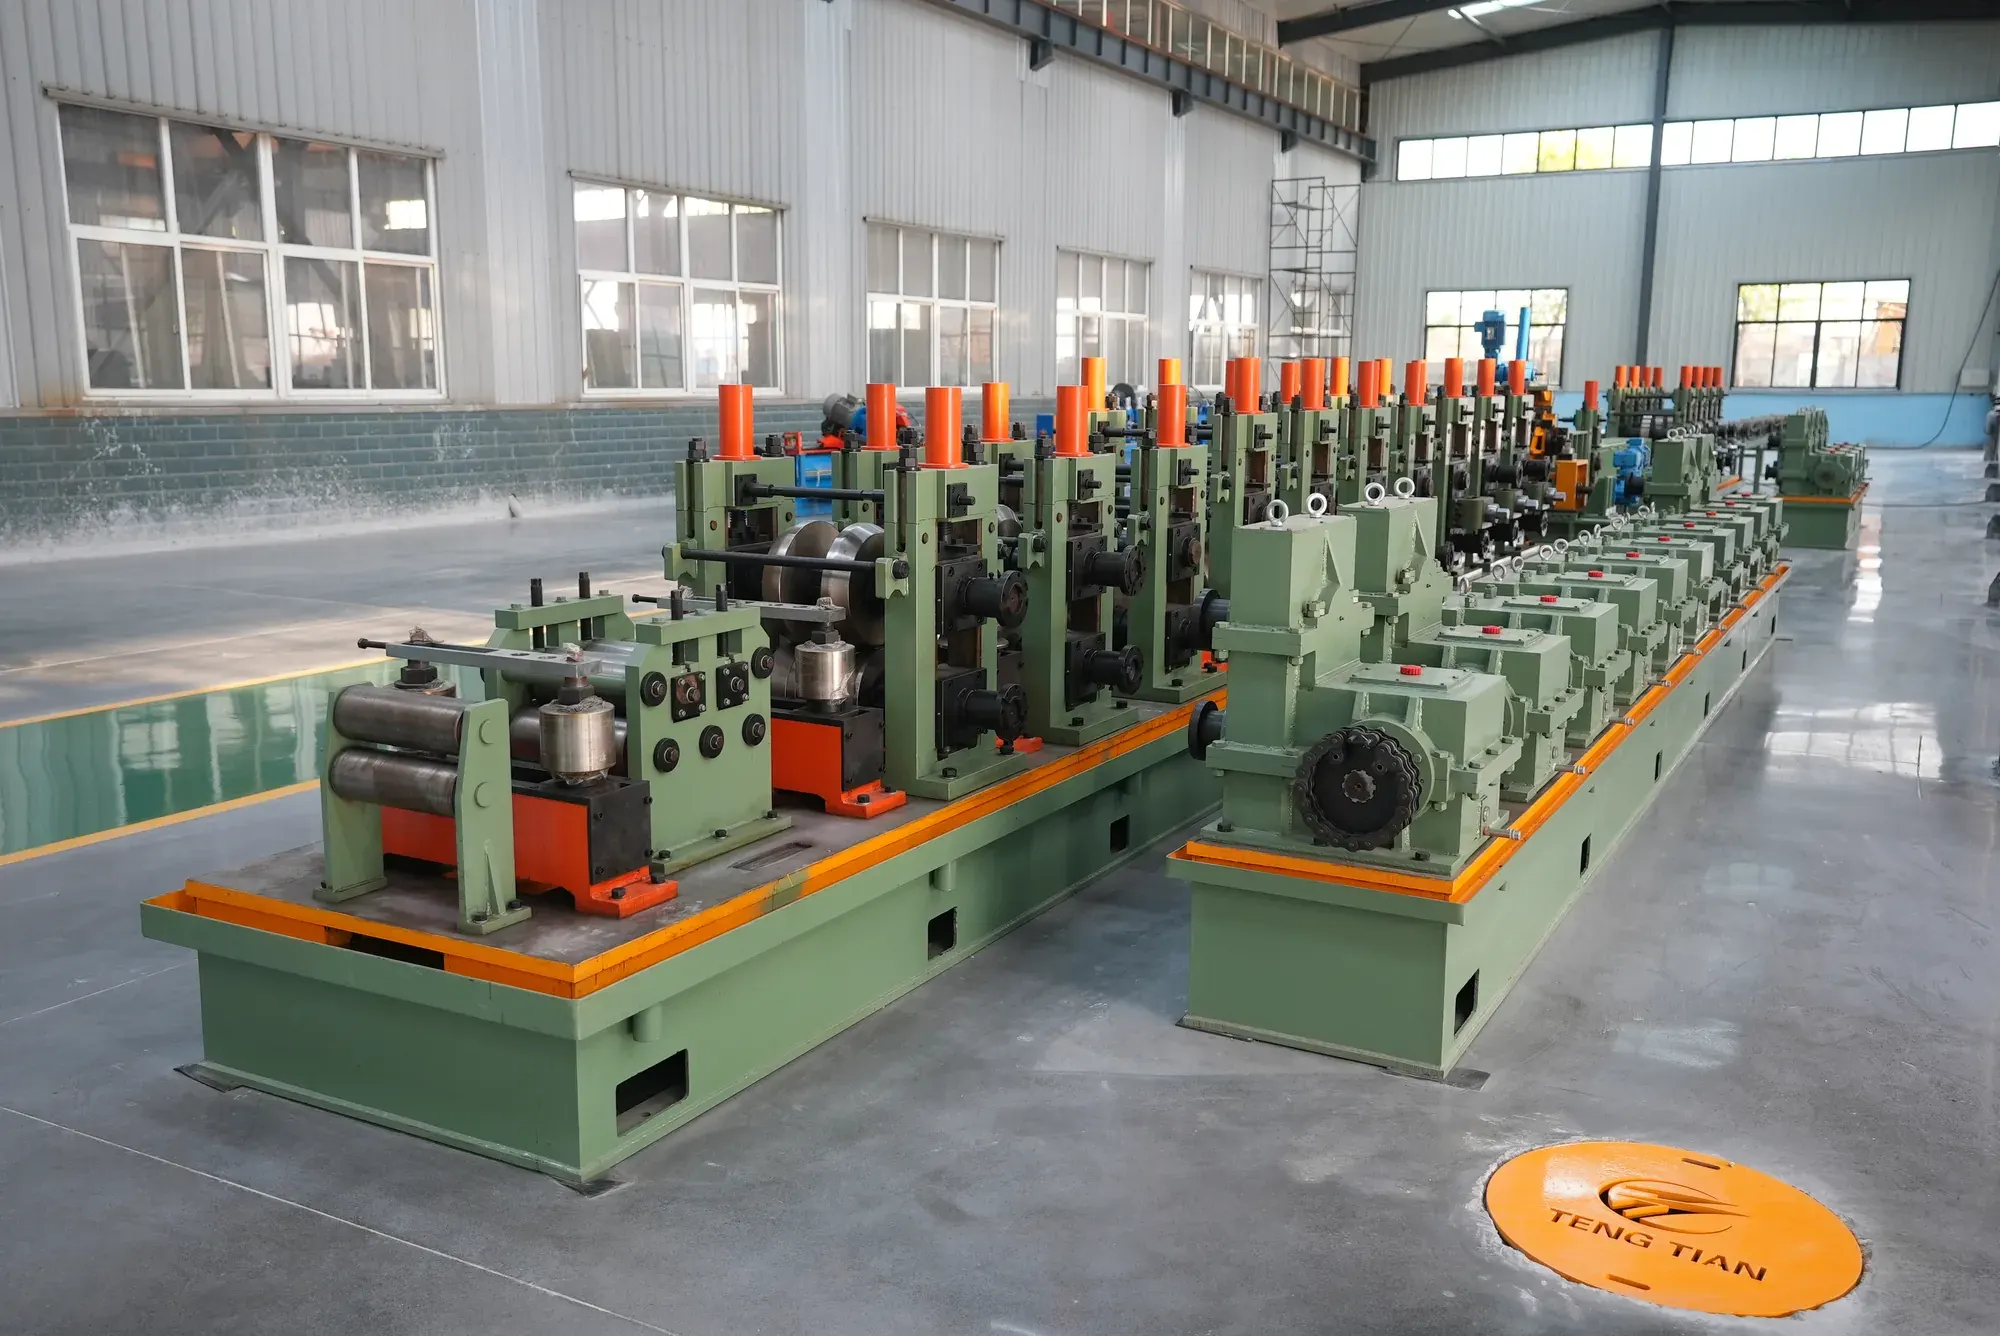
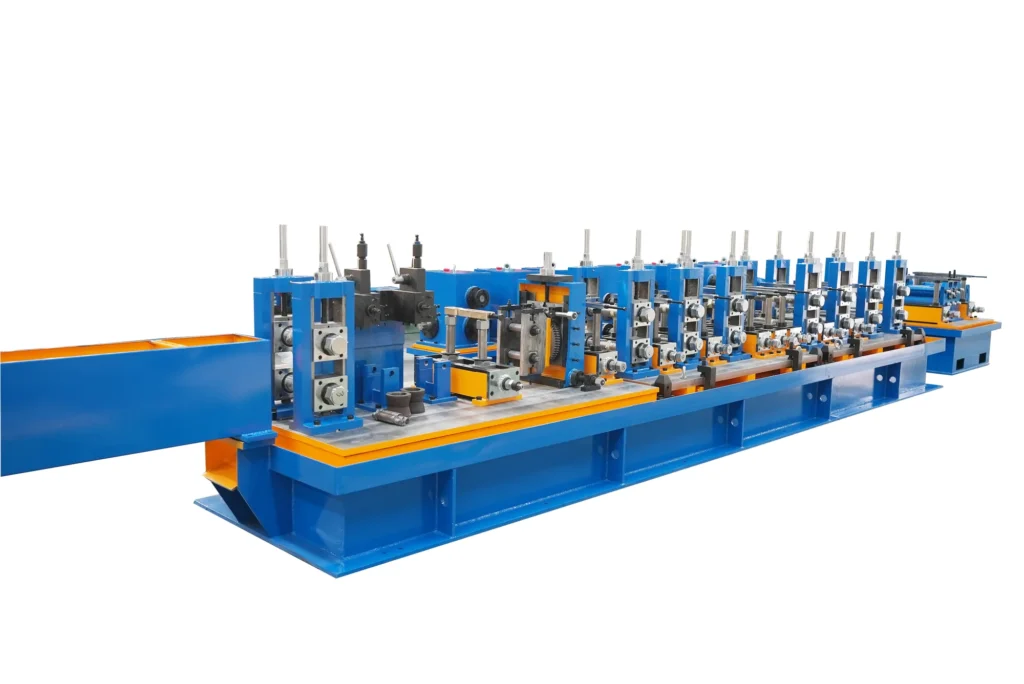
- Forming and sizing mill — the core unit, where rolls bend flat strip progressively into an open tube and, after welding, sizing stands bring it to final diameter.
- High-frequency induction welder — supplies the welding energy, matched to the pipe range.
- Flying saw — cuts to length while pipe is still being delivered at speed.
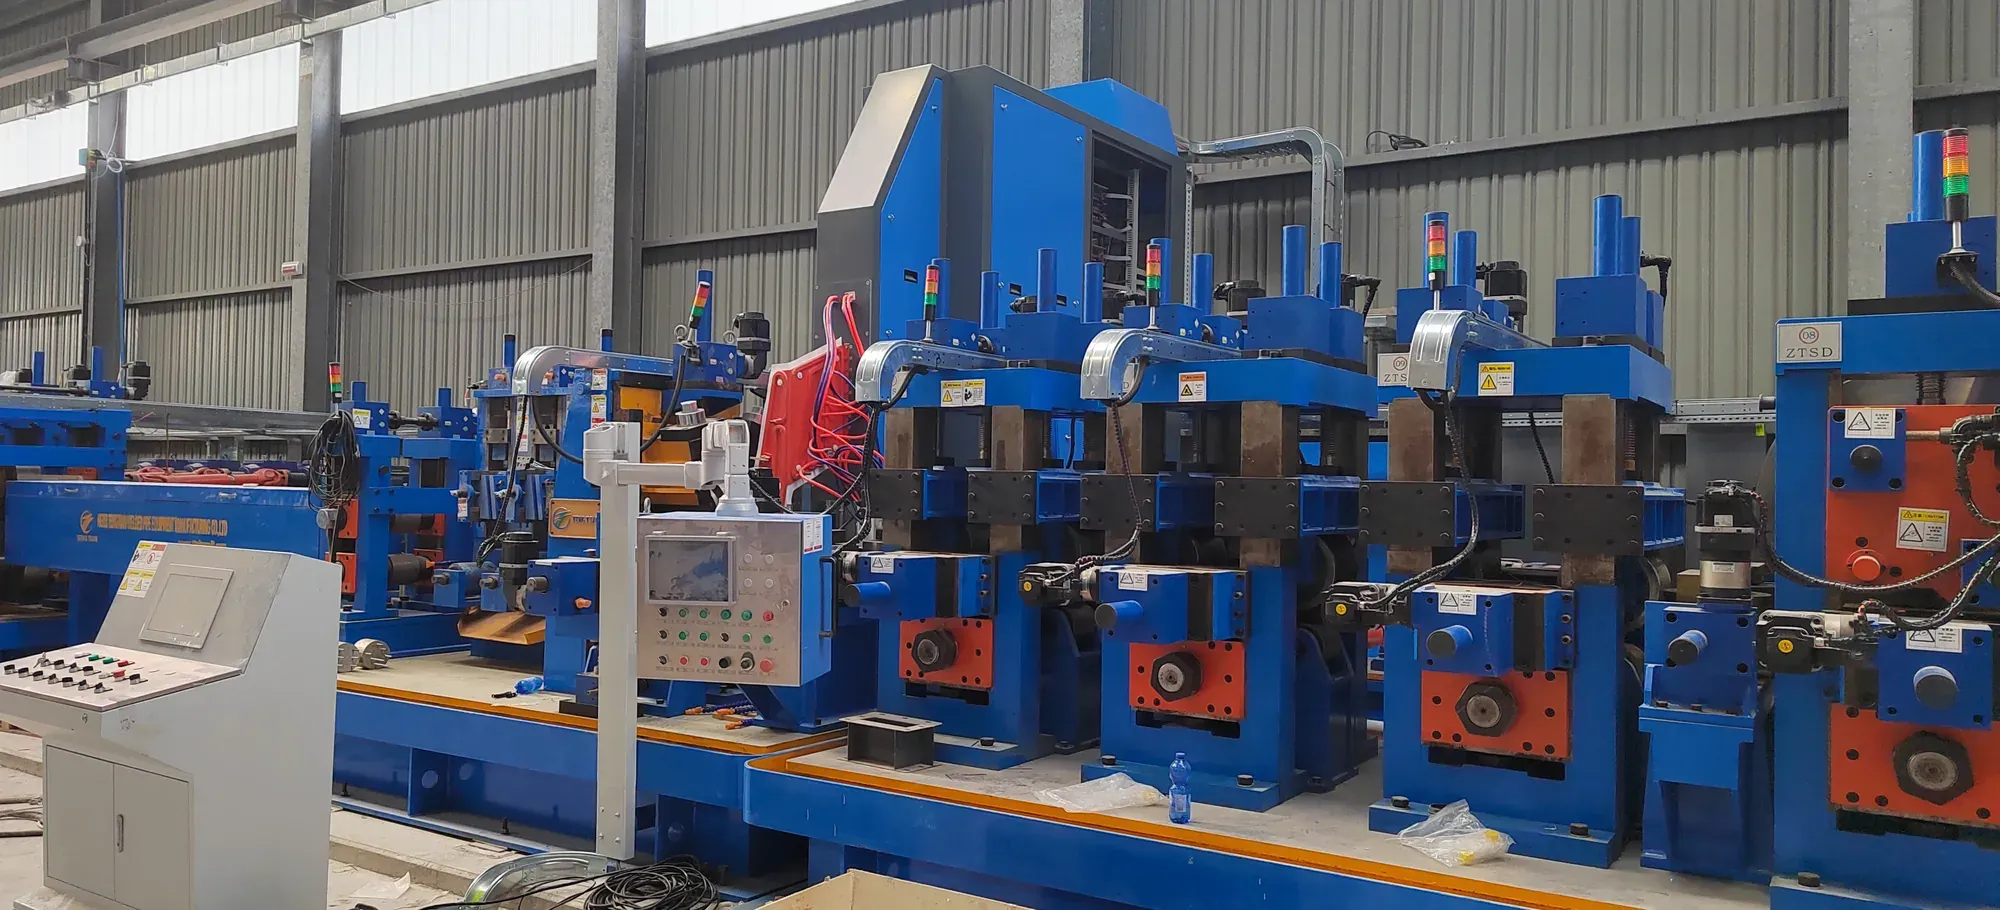
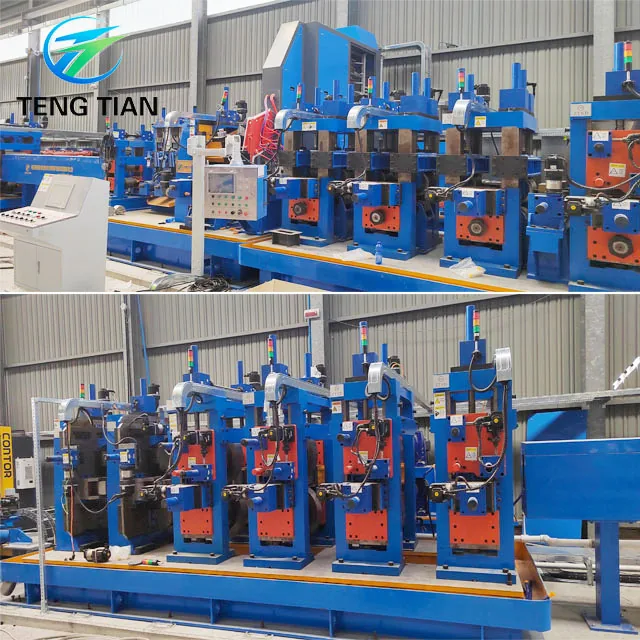
- PLC and variable-frequency control — ties line speed, sequence timing and cut length into one controller.
Underneath the unit list, the physics is short enough to state plainly. Rolls form the strip step by step into an open tube. High-frequency current, concentrated at the open edges by skin and proximity effect, heats them to welding temperature. Squeeze rolls press the two heated edges together, forming a continuous seam by pressure.
The tube is then cooled, sized and straightened to its final dimension.
Within those units, five parts do the actual work, and a quotation comparison usually turns on these five rather than on the unit count.
- Forming and sizing rolls — the first determinant of shape accuracy, roundness and squareness, edge definition and dimensional consistency. Roll material and heat treatment decide how long that holds; a direct-forming build uses combined rolls whose point contact reduces wear.
- High-frequency induction welder — supplies the welding energy and so governs fusion quality and welding speed, with power stepped to diameter. Unstable power or frequency shows up as lack of fusion, cold welds or burn-through, and the pipe then fails pressure testing and inspection.
- Induction coil and impeder — concentrate the high-frequency current at the seam through skin and proximity effect. Both are wear parts; as they degrade, welding energy spreads, seam quality fluctuates and energy consumption rises.
- PLC and variable-frequency control — holds the timing and speed of forming, welding, sizing and cutting together. Unstable control produces speed fluctuation, cut-length error and higher downtime.
- Cutting saw — cuts to length accurately while pipe is still being delivered at speed. Blade wear or length-setting drift shows as length error, end burr and skewed cuts.
Of the five, two are consumed in normal running (coil and impeder), one is a wear item (rolls), and two are capital items expected to last the life of the line (welder and control system). Which of the five a supplier makes itself, and which it buys in, is a fair question to put to any quotation.
Without them the mill stops at every coil change; with them the join is made off-line while buffered strip keeps the forming stands fed. That is why they appear in the standard train rather than as options.
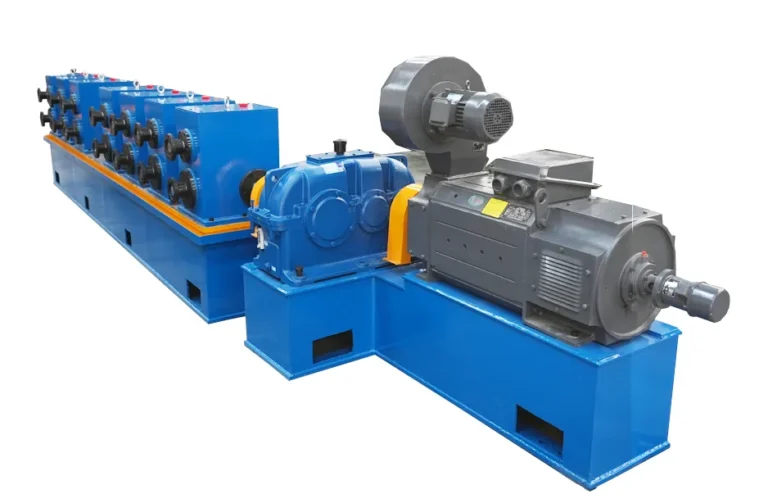
Size Change, Roll Wear and Running Cost
A direct-forming square build adjusts a combined die set by servo instead, with a roll saving above 90%, because contact between die and strip is point contact rather than full face. Two questions decide the running cost of a pipe making machine, and neither is answered by the specification table: what a size change costs in time, and what the rolls cost over a year. There is one exception: making 100 × 100 mm tube needs the upper roll on the final open stand changed.
Our rolls are machined in-house on our own CNC equipment. The practical consequence for a buyer is not a quality claim but an availability one: replacement rolls remain obtainable years after handover instead of becoming an obsolescence problem.
Changeover cost depends on which forming technology is quoted. A conventional roll-forming build changes size by changing rolls.
Operator practice is the third variable: quick changeover and a trained change crew are what keep scrap during a size change down, which is why changeover training is treated as a separate requirement, not taken for granted.
Forming and sizing rolls determine shape accuracy, roundness and squareness, corner definition and dimensional consistency — they are the first determinant of pipe quality. Roll material and heat treatment decide how long that accuracy survives; when they are wrong the line shows early wear, diameter drift, uneven corner lines and repeated re-machining.
- Consumables and wear parts divide into four groups. · Saw blades and cutting tools, consumed against cutting volume.
- Impeders and induction coils, wear parts replaced against welding hours; their condition governs how tightly weld energy stays focused at the seam.
- Cooling water and emulsion, plus hydraulic oil and grease — specifications from us, purchased locally.
- Forming and sizing rolls as replacement wear items. Wall thickness, line speed and shift output are confirmed against your pipe size, material grade and cut length at quotation. Send us those three and we will state the figures.
Applications and Output Examples
The measures that matter to those buyers are weld pass rate, diameter and wall coverage, non-stop coil change, and energy and yield per tonne. Two application families carry most of the demand for these lines, and two lower-volume applications sit alongside them.
Structural and scaffolding tube. Structural plants produce square, rectangular and round sections for load-bearing steelwork, scaffolding and general machinery components. Here the measures shift to corner definition and straightness on square and rectangular section, changeover efficiency, and electricity per unit produced.
Electrical conduit and agricultural pipe are two further applications. Both are round carbon-steel sections inside the same diameter range, produced on the same train — which matters, because buyers asking about either often expect a dedicated machine and do not need one.
Where responsibility sits is best made clear before a line is quoted, not after a dispute. The mill controls welding power, seam alignment and squeeze. Sizing and straightening set dimensional accuracy and straightness. Line design supports material yield of 93% or better, though achieved yield also depends on scheduling and operating practice.
Incoming strip grade, thickness tolerance and flatness stay on the buyer’s side: the line offers levelling and incoming checks, but levelling cannot rescue out-of-tolerance strip.
Fluid transport pipe. Pipe plants run these lines continuously to produce carbon-steel welded pipe for oil and gas transport, municipal water and drainage, gas distribution, and chemical and heating pipework.
Delivery, Installation and Training
Lead time is 50–90 days.
Commissioning a pipe making machine is a training exercise as much as an installation one, and training needs differ across the five operating steps. Coil loading and strip threading need operator training. Shear-welding a coil join in time with the accumulator needs operator training. Setting a new size needs a trained change crew.
Setting welder power, welding speed and squeeze, then running and watching the process, needs process-level training. Cutting and collecting is routine.
After handover, support is a first reply through a single named point of contact, all-hours online support, on-site dispatch when required, and direct spare-part shipment. Behind that sits an engineering team of twenty averaging twenty years each, and an owned production base open to factory audit.
Certification: GB/T 19001-2016 / ISO 9001:2015 (quality management system, certificate No. 18524Q11269R2S). The product standard the finished pipe is made to depends on the destination market and the buyer’s specification; the equipment itself follows destination-market machinery-safety rules and that product standard.
Export packing is specified per item. Control cabinets, impeders and induction coils, forming rolls and cutting tools travel in moisture-protected wooden cases with a spare-parts pack; heavy large-diameter frames ship bare, braced on cradles with designated lifting points and rust protection.
Electrical wiring pipe manufacturing machine
Agriculture pipe manufacturing machine
From the Workshop

 Tube Mill Output, Material Yield and Roll-Change Cost in the Cold Forming Steel Process
 What Is an ERW Tube Mill
 PLC Automatic Tube Mill for Round and Square Pipe
 The API Pipe Mill Inspection Chain
Send Your Enquiry
Tell us the pipe outside-diameter range, the wall thickness and the output you need. An engineer reads every enquiry — it does not land in a general sales inbox.