
 Scan on WeChat
In This Line
Quick Contact
Hebei TengtianYuanle@tentubemill.com
+86-311-83025332
WhatsApp +852 5425 3155
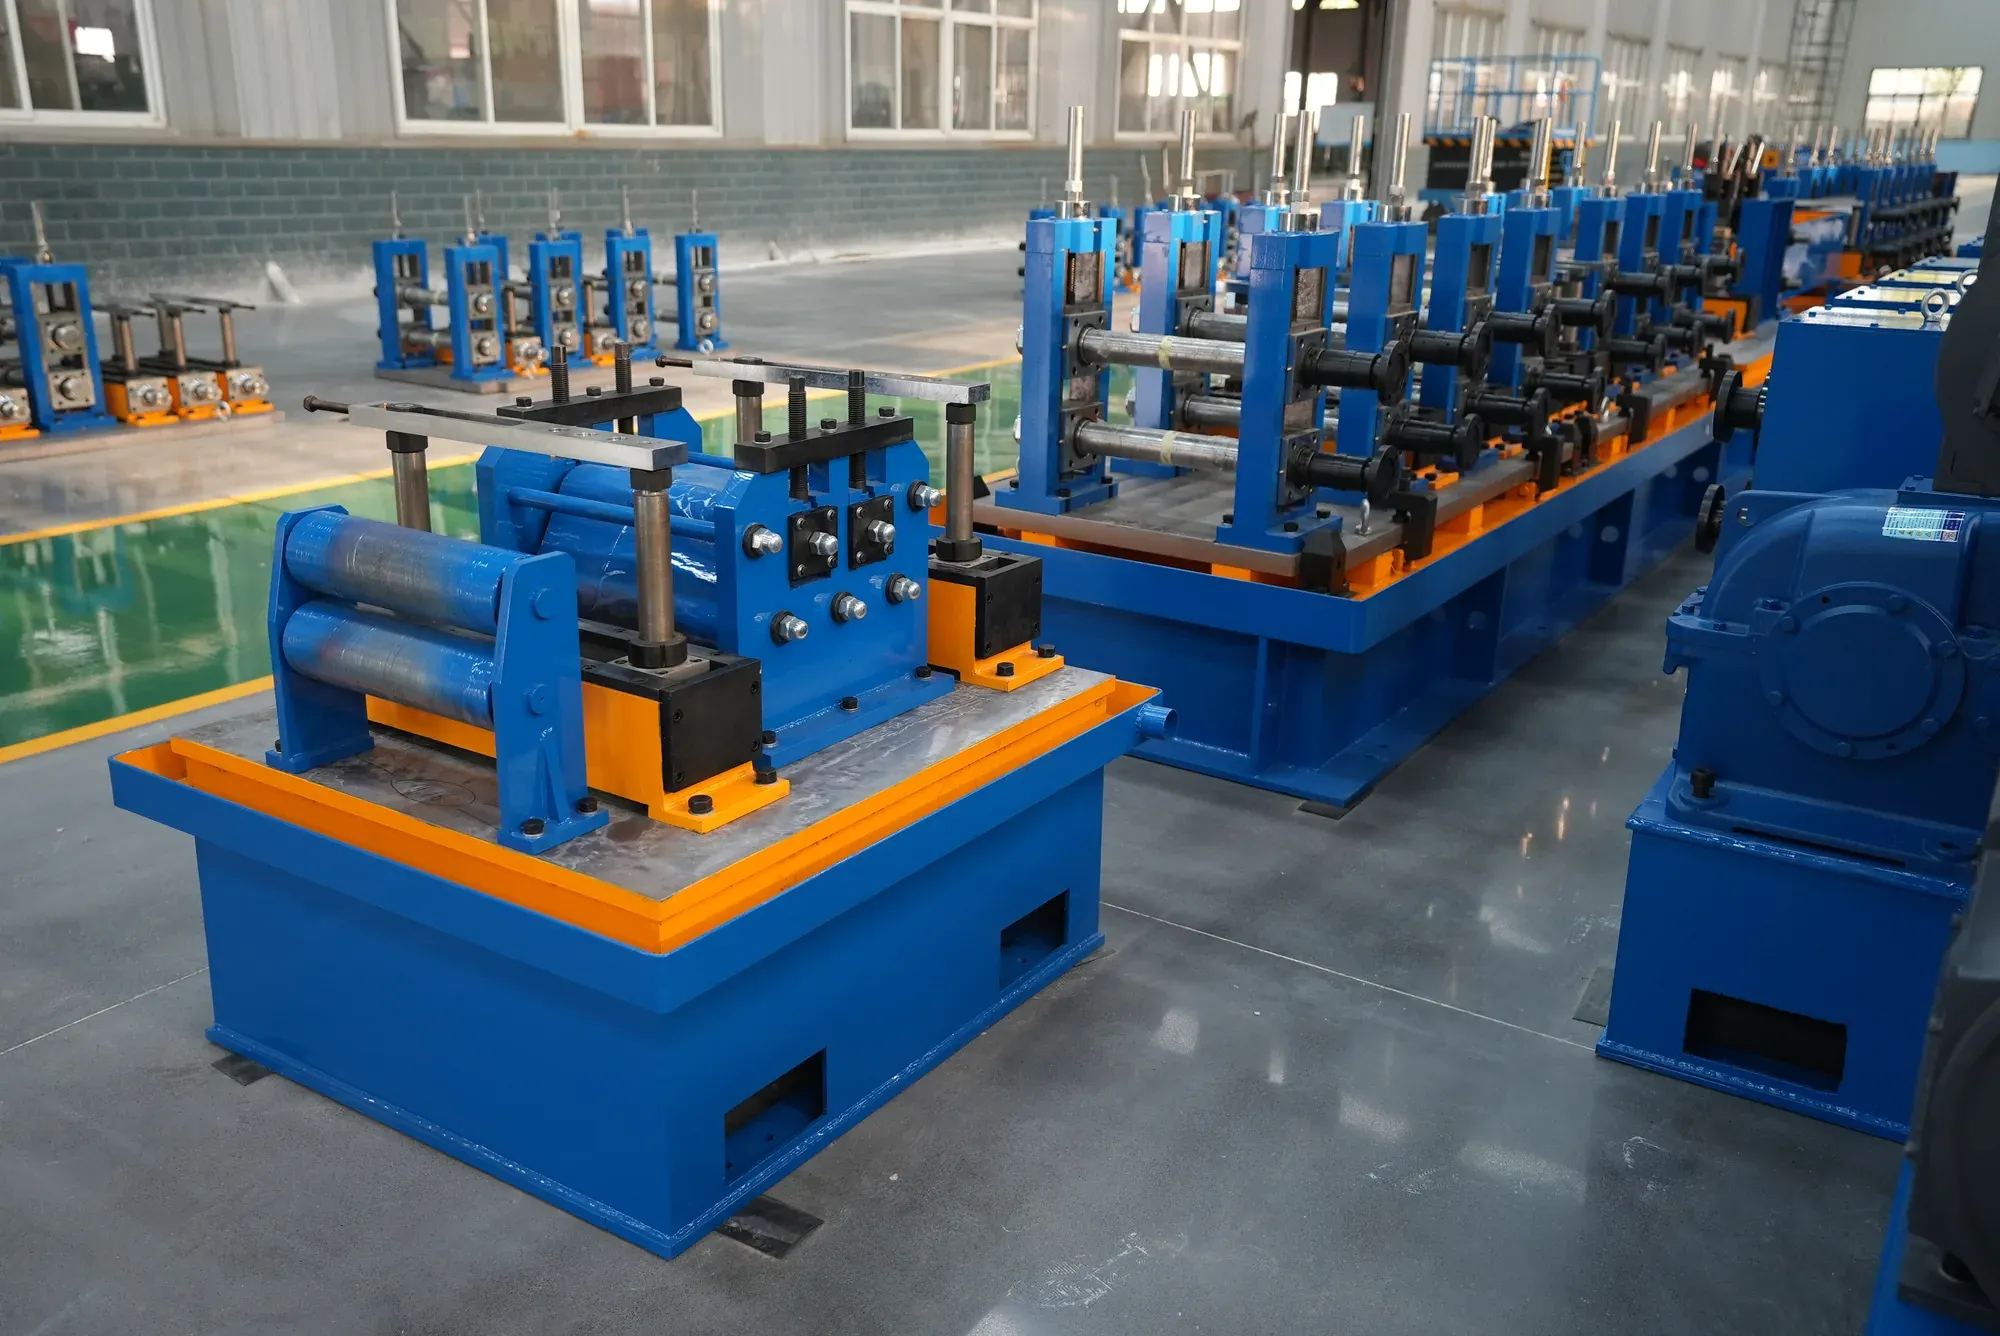
Roll-change cost is best shown as a comparison: the direct-forming square route saves more than ninety per cent of roll consumption because a size change needs no roll change.
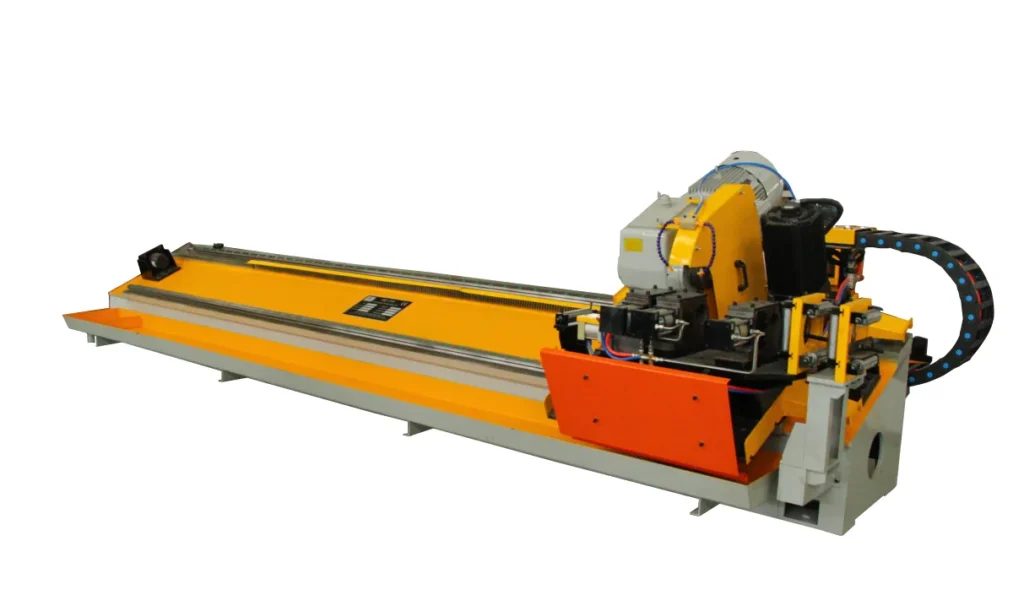
What Sets Yield, and What a Size Change Costs
- Material yield: line design supports not less than 93 per cent.
- Actual yield also depends on the buyer’s operation.
- Direct forming square saves more than ninety per cent of roll consumption — no roll change on a size change.
- A conventional line changes rolls for a size change; direct forming adjusts servos instead.
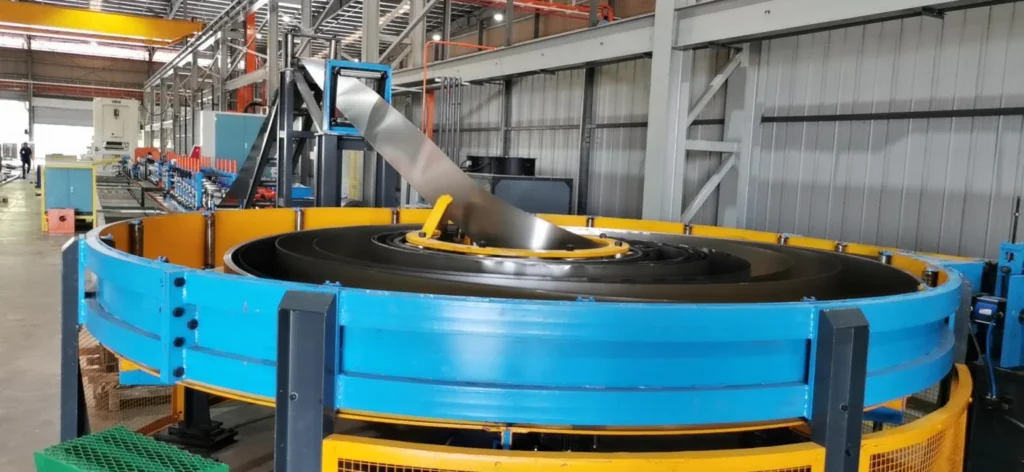
- A spiral accumulator keeps the mill running through a coil change.
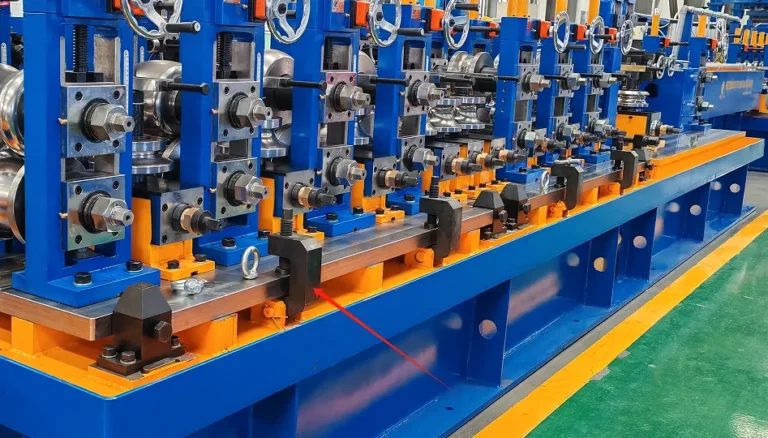
What Is Tube Mill Output, Material Yield & Roll-Change Cost
Material yield is a design-level figure with a caveat: line design supports a material yield of not less than 93 per cent, and actual yield also depends on the buyer’s operation. Three numbers decide whether a tube mill pays for itself, and buyers usually ask for them together: how much pipe comes off the line in a shift, how much of the incoming coil ends up as saleable pipe, and what it costs in tooling and downtime every time the size changes.
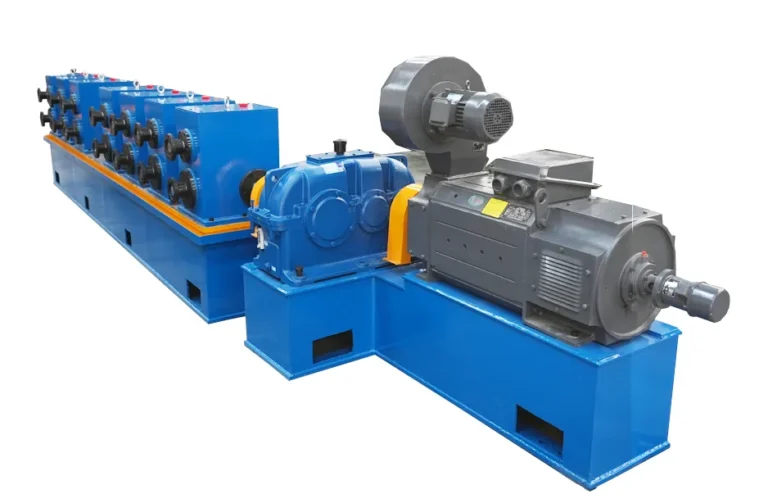
Tube mill output
Wall thickness, line speed and shift output are confirmed against your pipe size, material grade and cut length at quotation. Send us those three and we will state the figures.
The key point about output is its mechanism rather than its magnitude. Continuous running is the main answer to what buyers are up against: production that does not stop, one line covering several sizes, stable yield and weld quality, and quick size changes.
The specific device that delivers the first of those is the spiral accumulator, which stores strip between the shear-welder and the mill so that the mill keeps forming while the next coil is prepared and joined.
The failure mode for that buffer is worth knowing when comparing lines: if accumulator storage or tension control is poor, the mill starves or judders, and the consequence is weld-seam fluctuation and downtime.
Yield depends on the forming and welding process and on automation on the equipment side, and on scheduling and operator skill on the customer side.
Tube Mill Output, Material Yield & Roll-Change Cost — Method and Measured Values
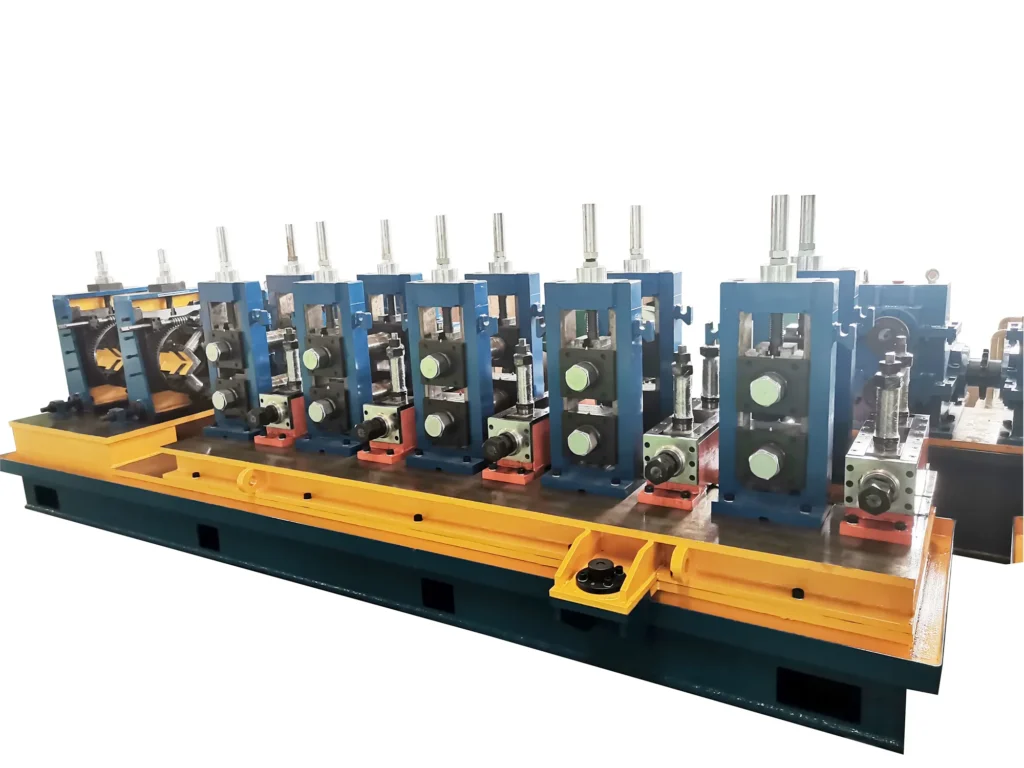
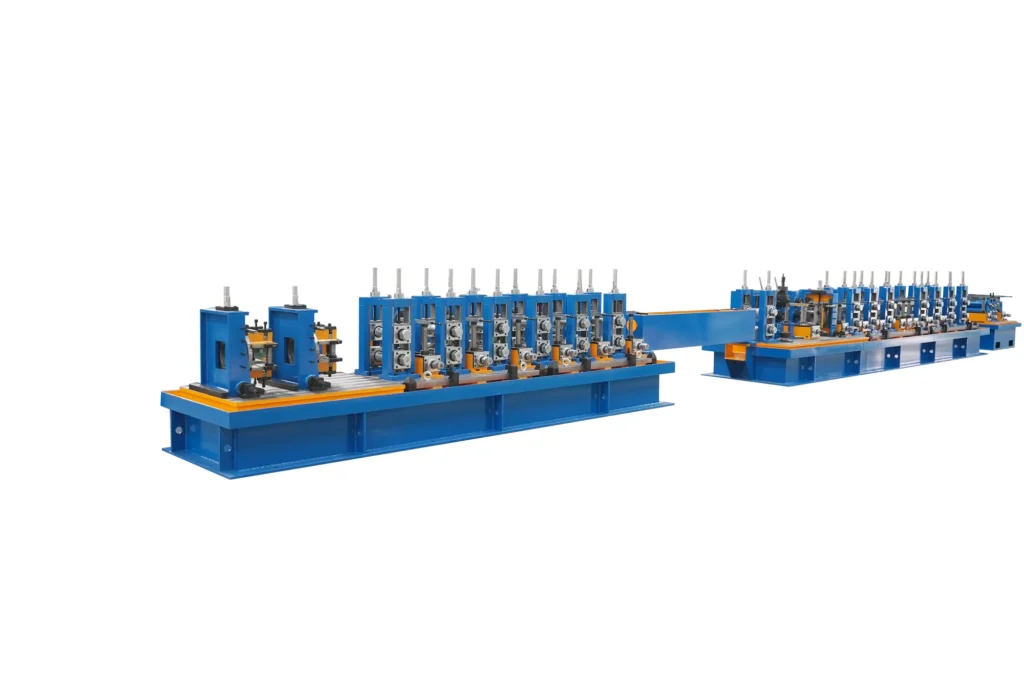
On the direct-forming square route one combined mould covers the range and the change is a servo adjustment with no roll change at all.
The saving on the second route is more than ninety per cent of roll consumption, together with longer roll life, and the mechanism is point contact in the combined-roll design.
The cost of a size change also has a human component. Operator setup and quick roll change are among the ten quality-influencing factors, under personnel, and the consequence of getting them wrong is shape drift after the change and scrap pipe while the new size is dialled in; the mitigations are change-over training and quick die change.
Roll change cost
Where roll-change cost shows up in the buyer’s own words is on the persona side.
For the regional pipe and section maker — a small or medium mill building or expanding capacity, sensitive to price and lead time — the concerns are value for money, delivery, quick size change, material yield and energy consumption, and the decision drivers are return on investment, change-over efficiency, and tooling and energy cost.
That list is why output per shift, yield and changeover cost matter more to a buyer than a specification sheet.
Consumables fall into four classes: saw blades and cutting tools, consumed in proportion to cutting volume and replaced periodically; the induction coil and impeder, as wear parts; cooling water and emulsion as process media; and hydraulic oil and grease. Continuous supply is offered for the first two.
Roll-change cost is best understood as a comparison between two routes. On a conventional mill the operating step for a size change is to set the line to the target diameter and change rolls, after which roll gap, servo parameters and alignment are reset.
Standards Behind the Output and Yield Figures
The applicable standards — GB/T 9711 and GB/T 5037 on the spiral bands, API 5L on the API line pipe family, GOST R 58966-2020 on the H-beam line, and the enterprise standard Q/GYLTT01-2023 covering HGF150 high-frequency welded pipe equipment — govern product classes and equipment, not yield or changeover economics.
No product-level standard applies to output, yield or roll-change cost for this family.
Step-by-Step Procedure
The flying saw cuts to the set length automatically and the run-out table collects finished pipe. For a size change, the operator sets the line to the target pipe diameter; on a conventional line that means changing rolls, on the direct-forming square line it means a servo adjustment only. Roll gap, servo parameters and alignment are then set.
Coil changes are handled without stopping: before the running coil is exhausted, the head and tail are sheared and butt welded to join the next coil, and the accumulator supplies the mill during the join.
Welding power and weld speed are set, the continuous forming–welding–sizing sequence is started, and the process is monitored.
Worked Example — Yield on an HG Line
If a mill feeds coil into an HG line and the line performs to its design figure, not less than 93 per cent of the input mass leaves as saleable pipe.
These levers pull the same way: low roll wear, high yield and quick changeover are what keep long-run running cost under control — as a value proposition with its two supporting figures, roll saving of more than ninety per cent and yield of not less than 93 per cent.
Where yield is actually won or lost
Yield is not decided at one machine. The list of quality-influencing factors spreads across raw material, process, equipment, personnel and inspection, and each carries the defect it produces when it drifts.
Incoming strip is checked for grade, thickness tolerance and flatness, because poor material shows up as forming wander, seam inclusions and uneven wall thickness — all of which become scrap rather than saleable pipe.
The five-roll pre-leveller flattens the strip before forming, and the consequence of leaving residual curvature in the band is a poor corner line and weld-seam misalignment downstream.
Further down the line the same logic repeats. Sizing and straightening set final dimension and straightness, with out-of-tolerance outside diameter, bend and ovality as the failure modes.
PLC and servo stability keep line speed and cut length repeatable, and when they drift the symptoms are speed fluctuation and length error — both of which turn finished pipe into off-cut. Final inspection is the last catch, with ultrasonic and eddy-current testing on API lines.
Read as a set, that list tells a buyer where yield losses come from, without attaching a percentage to any single cause.
The two routes compared
For roll-change cost, the comparison that matters is between the conventional and direct-forming routes.
On a conventional line, a change of finished diameter is a change of rolls. Roll gap, servo parameters and alignment have to be reset afterwards, and the risks are shape drift and scrap pipe while the new size is dialled in. The mitigation is training and quick die change rather than a claim that the problem disappears.
On the direct-forming square line, one combined mould covers finished sizes from 30 by 30 to 500 by 500 mm at 1.5 to 13 mm wall by band, and a size change is a servo adjustment. The consequence is a roll saving of more than ninety per cent and longer roll life, with point contact in the combined-roll design as the mechanism.
The target buyers are square-tube mills that switch frequently between sizes in the 30 by 30 to 500 by 500 range, whose pain is exactly roll consumption cost and downtime at every change.
What continuity is worth, and how it is achieved
Output on a continuous line is as much about not stopping as about speed. Two mechanisms carry that. The shear and butt welder joins the tail of the running coil to the head of the next one so a coil change does not halt production, and the spiral accumulator holds enough strip to feed the mill while that joint is made.
The control layer holds the rest together. The PLC and variable-frequency drive system unifies the cycle and speed of forming, welding, sizing and cutting, and determines line stability and the level of automation; configurations run from semi-automatic to fully automatic PLC control.
Around the equipment, two commercial facts bear on when output actually starts. Delivery is set at 50 to 90 days with plant-level customisation from the manufacturer’s own base, and installation and commissioning are included, with on-site dispatch and round-the-clock online support.
What to ask the factory for
Three requests turn a general enquiry into a business case. Ask for line speed and shift output for the specific band and wall thickness. Ask for the roll-change time on the configuration offered, in minutes, not as a percentage saving.
And ask for the yield figure to be restated against your own coil grade and thickness — the 93 per cent is a design-level figure for the equipment side.
Actual yield also depends on the buyer’s operation, so the design figure is a ceiling condition on the equipment side rather than a promise about any particular plant.
Resource Downloads
From the Workshop

 Tube Mill Machine for Steel Pipe Production
 What Is an ERW Tube Mill
 PLC Automatic Tube Mill for Round and Square Pipe
 The API Pipe Mill Inspection Chain
Send Your Enquiry
Tell us the pipe outside-diameter range, the wall thickness and the output you need. An engineer reads every enquiry — it does not land in a general sales inbox.