
 Scan on WeChat
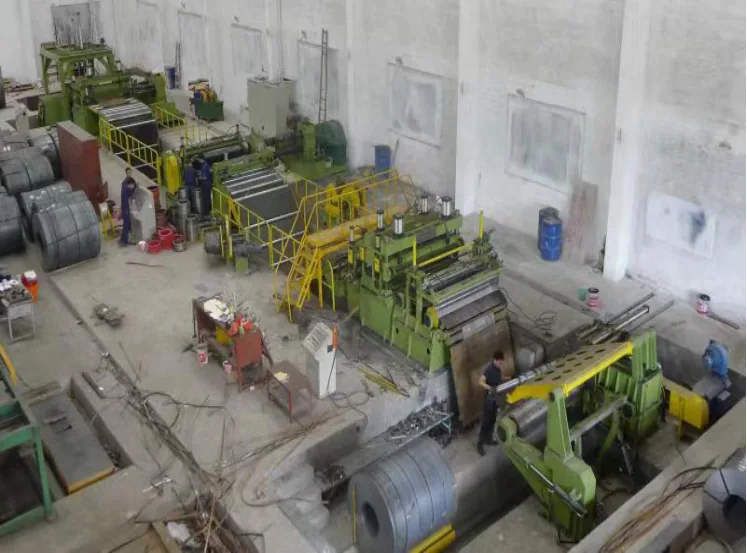
Steel Coil Slitting Line
A slitting line is upstream equipment.
In This Line
Quick Contact
Hebei TengtianYuanle@tentubemill.com
+86-311-83025332
WhatsApp +852 5425 3155
It does not make a product a buyer sells — it makes the strip that a tube mill or forming line can actually run. This range covers the CNC uncoiling, slitting and recoiling line and its cut-to-length mode.
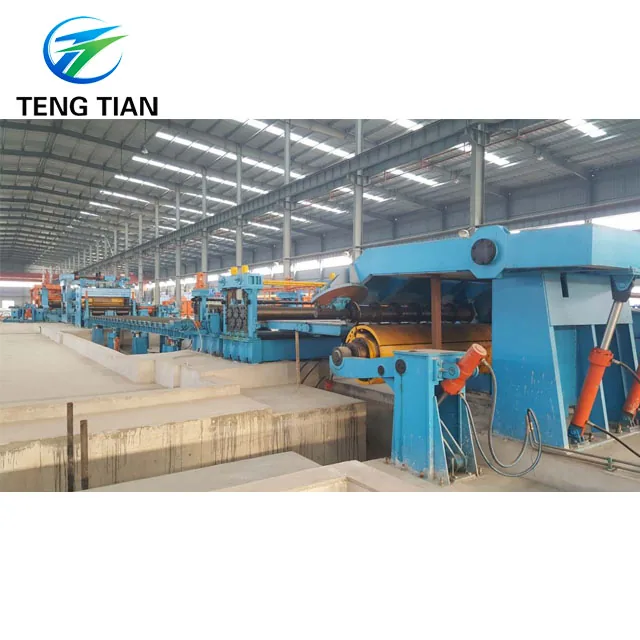
What Is a Steel Coil Slitting Line?
Slit width accuracy is ±0.2 mm and camber is held to ≤0.5 mm per 1000 mm. The line uncoils a wide coil, levels it, slits it lengthways into narrower strips or cuts it to length, and recoils the result — producing compliant narrow coil or cut sheet for downstream pipe and forming lines. It handles 1–12 mm thickness, 800–2000 mm width, and coils up to 32 tonnes.
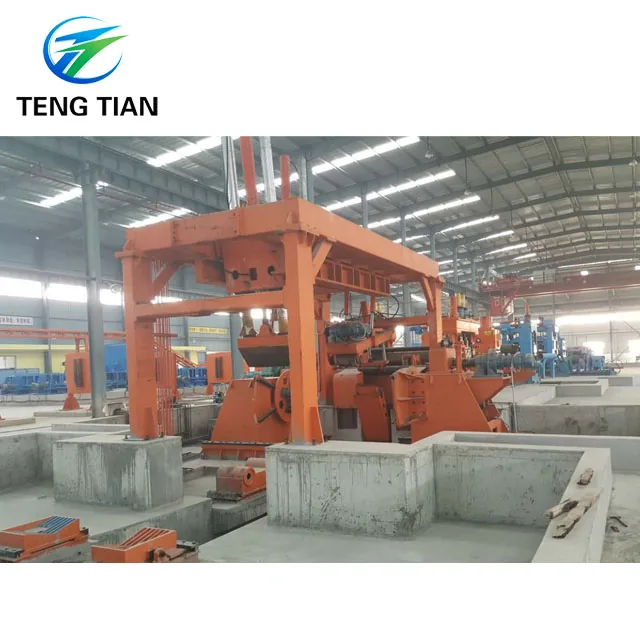 Steel Coil Slitting MachineStrip 1–12 mm thick, 800–2000 mm wide, coils up to 32 tonnes.See the line →
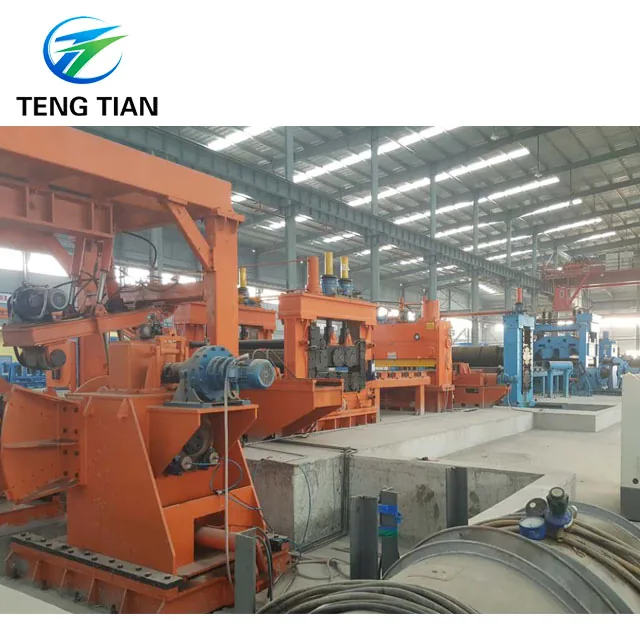 Slitting Line Running CostWhat a knife change actually consists of is a configuration decision keyed to strip thickness.See the line →
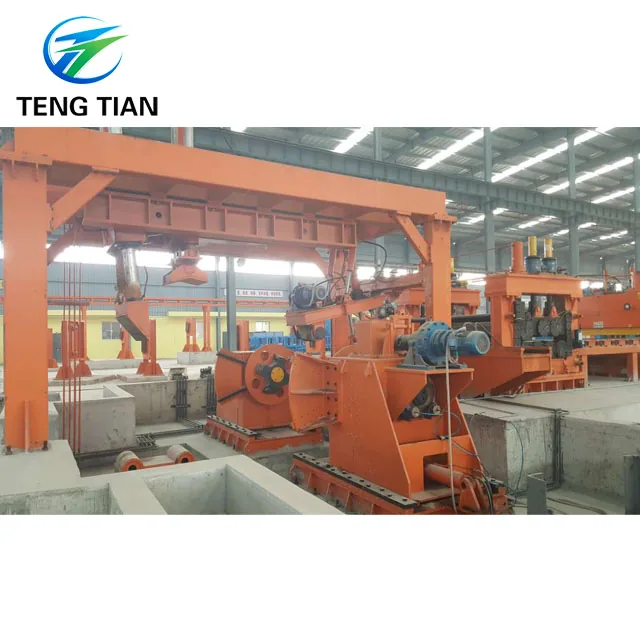 Slitting PrecisionPrecision on such a line is not one number.See the line →
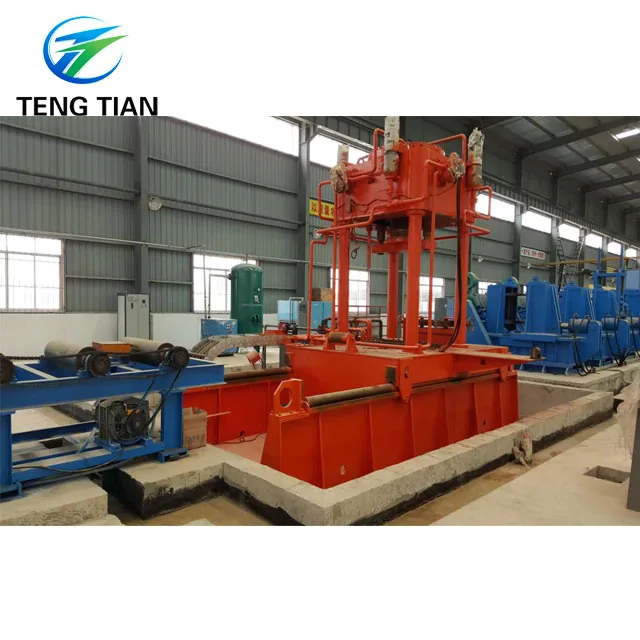 Slitting vs Cut-to-LengthThe envelope is 1 to 12 mm thick, 800 to 2000 mm wide, with coil weight up to 32 tonnes.See the line →
It addresses a problem rather than a feature: incoming coil that is the wrong width, has bad edges, or is not cut to length.
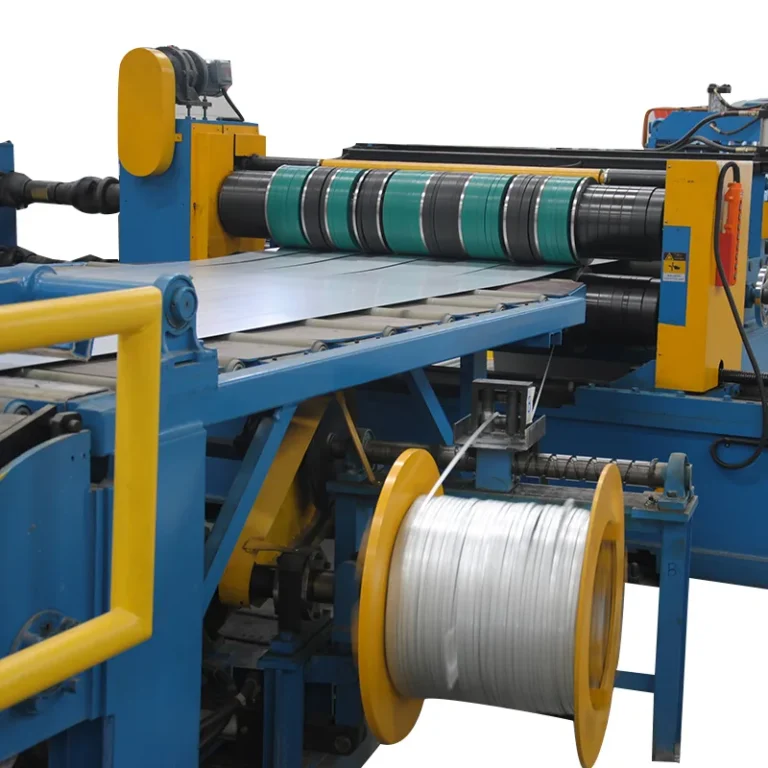
Steel Coil Slitting Line — Range, Configuration and Output
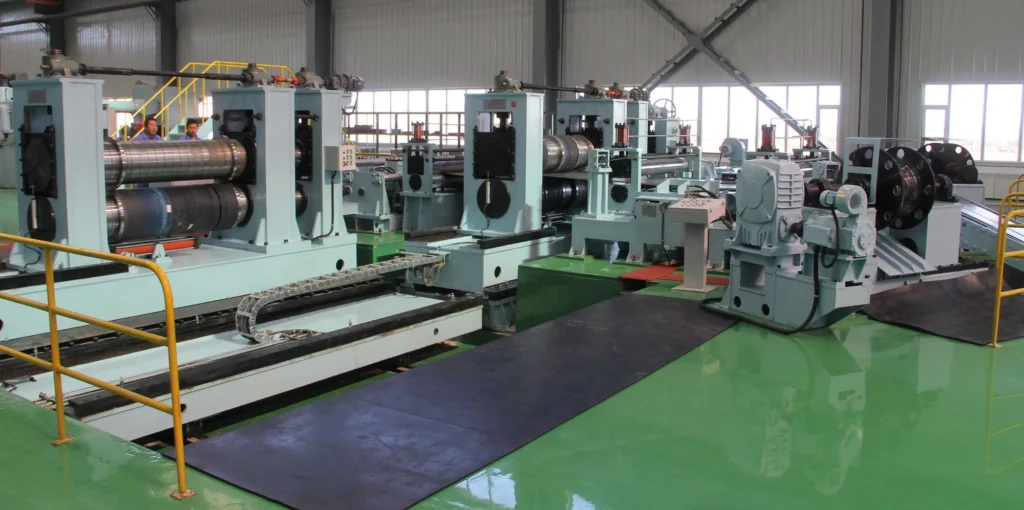
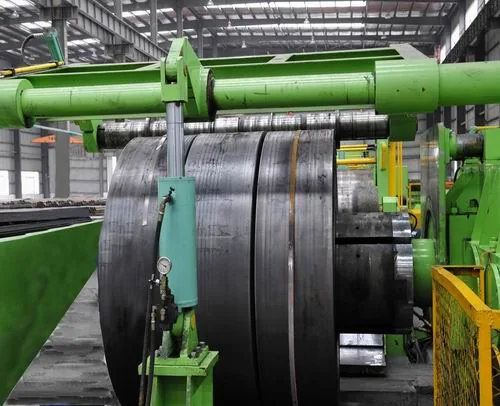
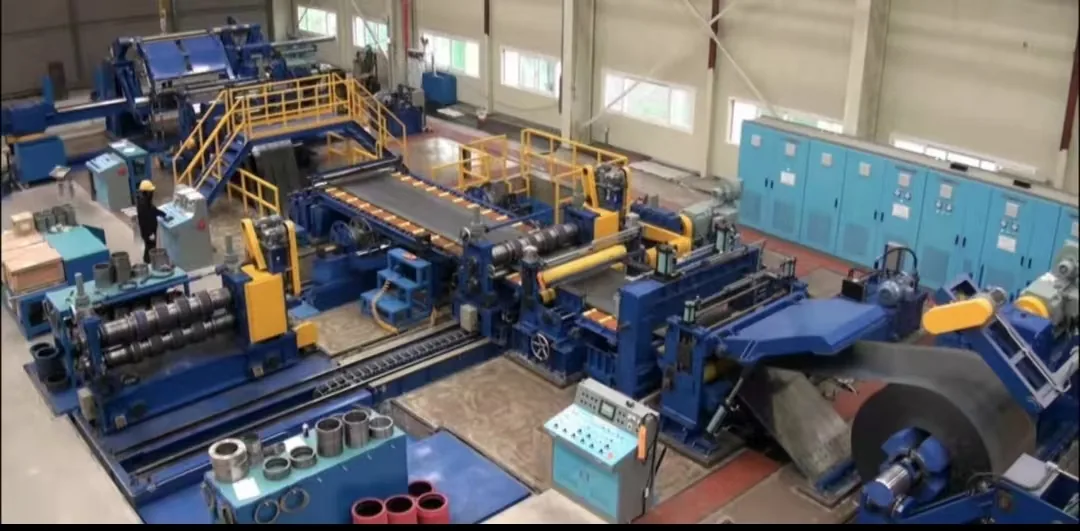
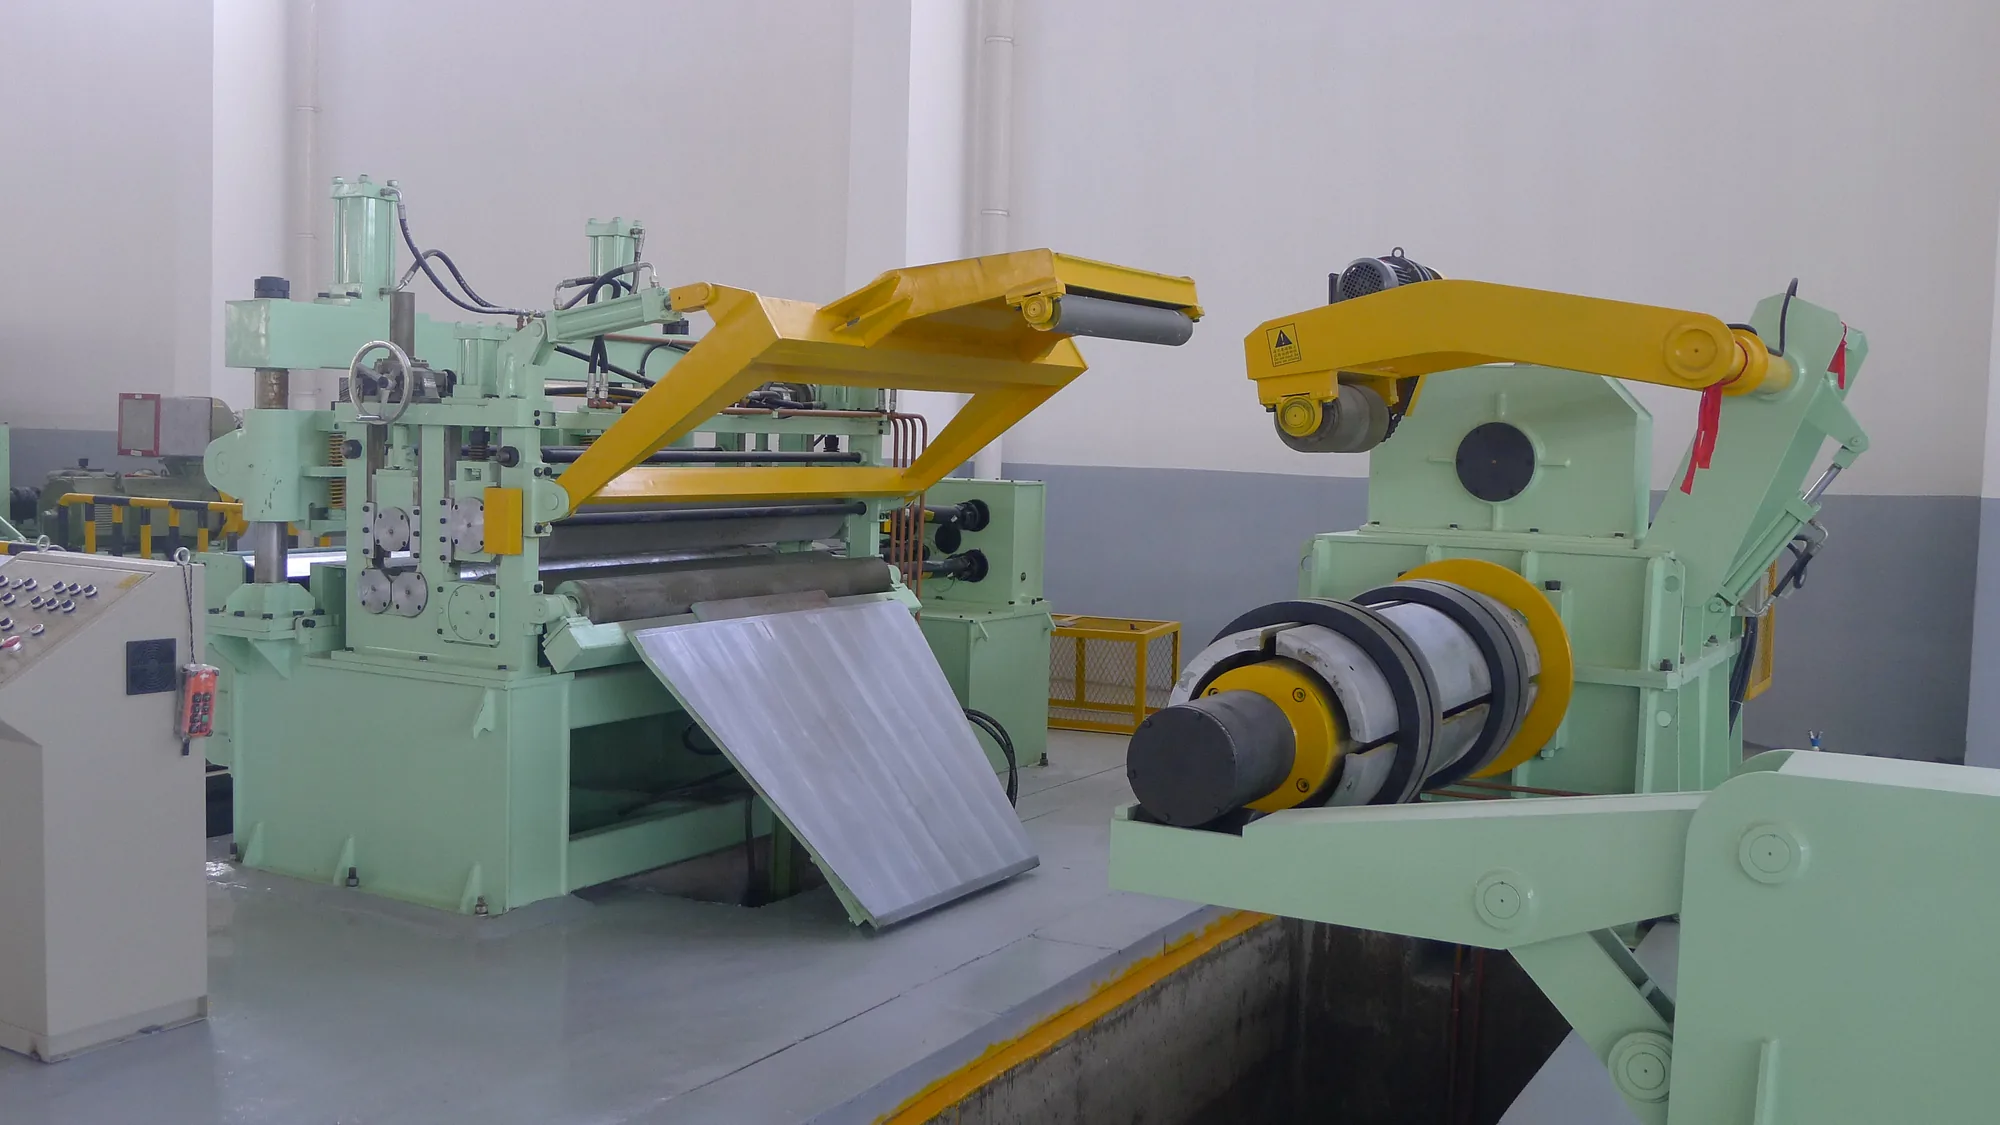
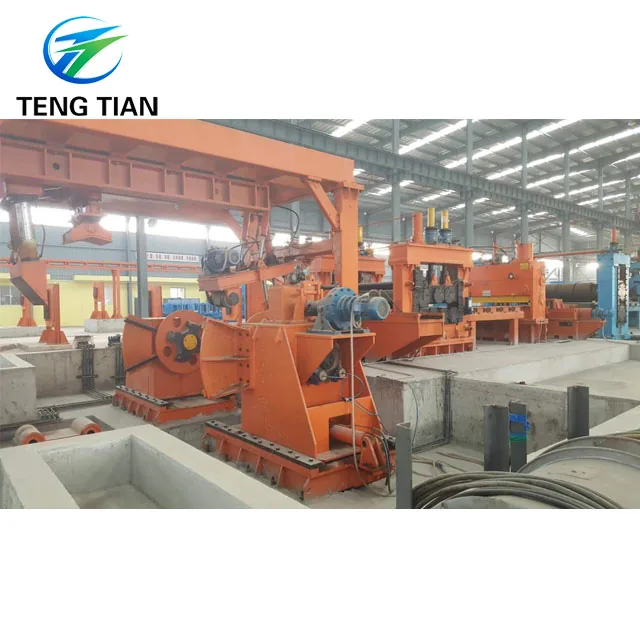
The main units are a double-head uncoiler, the slitter and a recoiler rated for 32-tonne coils, with a hydraulic shear, looper and tension unit handling the strip between them.
Two operating modes are on the same line: slitting into strips, and cut-to-length into sheet.
The flow is stage by stage: coil car and uncoiling, levelling, hydraulic shear, slitting or cross-cutting, scrap-edge winding, looper, separation, tensioning and recoiling.
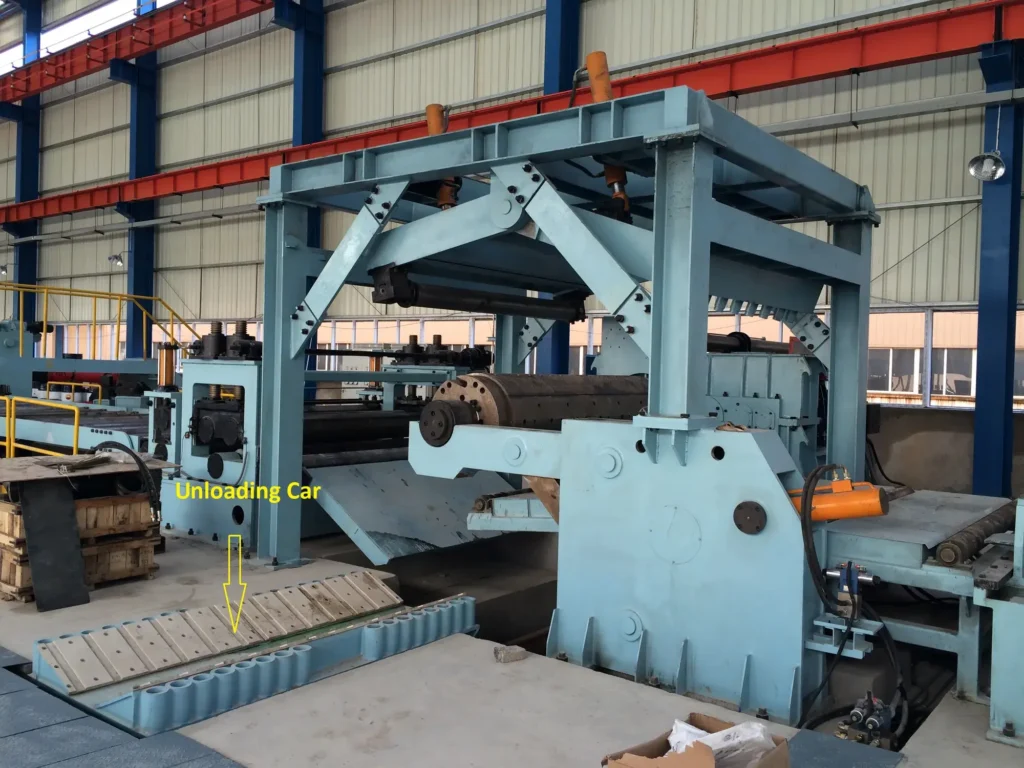
Key Parameters: Coil Width, Strip Thickness, Line Speed
Main parameters:
- Thickness handled: 1–12 mm.
- Width handled: 800–2000 mm.
- Coil weight: up to 32 t.
- Slit width tolerance: ±0.2 mm.
- Camber: ≤0.5 mm / 1000 mm (coil width ≥200 mm).
- Burr: ≤4 % of material thickness.
- Telescoping on the recoil: ≤±10 mm.
Line speed and output are confirmed against your coil width, material thickness and target strip width at quotation. Send us those three and we will state the figures.
Line speed and shift output are available on request.
Line Specification — SL-12×2000
| Equipment name | CNC Coil Uncoiling Slitting Recoiling Line |
|---|---|
| Model | SL-12×2000 |
| Coil material | HR. Steel Coil (YS. ≤250 MPa, TS. ≤480 MPa) |
| Coil thickness | 1 mm – 12 mm (Leveling + Shear) |
| Coil width | 800 mm – 2000 mm |
| Coil inner diameter | Φ610 mm |
| Coil outer diameter | Φ1300 mm – Φ2200 mm |
| Coil weight | Max. 32000 Kg |
| Recoil ID | Φ610 mm |
| Recoil OD | Φ1300 mm – Φ2200 mm |
| Recoil weight | Max. 32000 Kg |
| Strip slitting capacity | Max. 15 strips (coil thickness 2 mm); Max. 10 strips (coil thickness 4 mm); Max. 6 strips (coil thickness 6 mm); Max. 4 strips (coil thickness 8 mm) |
| Slitting width | Min. 80 mm |
| Width accuracy | ±0.2 mm |
| Sickle curve | ≤0.5 mm/1000 mm (coil width ≥200 mm) |
| Shear burr | ≤4% × thickness |
| Scrap width | 5 – 15 mm |
| Coiling tolerance | Pyramid ≤±10 mm |
| Line speed | 30/100 mpm |
| Machine list | 20 units: coil saddle; loading car; double-heads uncoiler; gantry feeding device; pre-leveler (2+5 rollers); hydraulic shear + scrap car; roller table; hydraulic side guide; slitter; scrap winder; looper; separation device; tension and feeding mechanism; recoiler + separating; unloading car; oil hydraulic system; pneumatic system; electrical control system; unit protection facilities; accessories (slitting knives, spacer bushing, rubber sleeve, separation disk, etc.) |
How to Choose the Right Model
Three inputs decide the configuration, and all three are on the coil rather than on the finished product: incoming thickness, incoming width, and coil weight. Those map straight onto the 1–12 mm, 800–2000 mm and 32 t window.
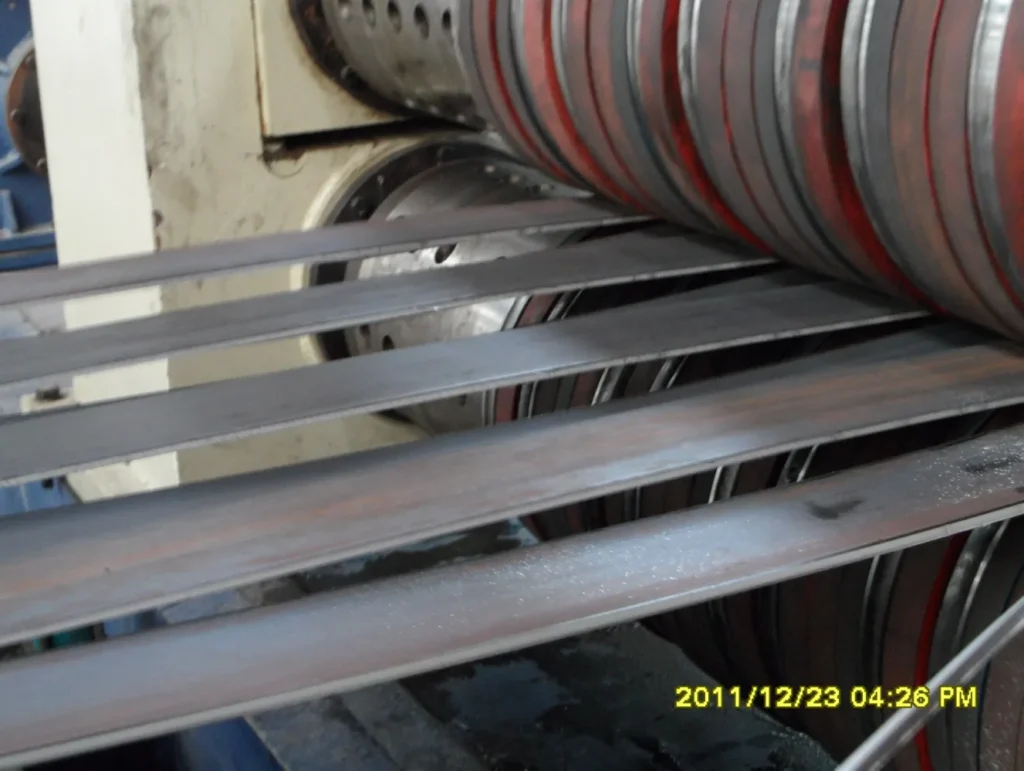
Knife and spacer configuration then follows from thickness, and it is the item that most often needs revisiting: worn or wrongly configured knives show up as width out of tolerance, heavy burr and camber.
The fourth input is what the downstream line needs. If it feeds a tube mill, the number that matters is slit width tolerance, because strip width error becomes diameter error after forming. If it feeds a forming line making open sections, camber and edge quality matter more, because a cambered strip forms a twisted profile.
Scope of Supply, Installation and Commissioning
Slitting knives, spacers, rubber sleeves and separator discs are supplied as a matched set and can be resupplied — they are the wear items that hold the ±0.2 mm tolerance. Knife service life in tonnes or hours is available on request.
Export packing is specified per item, with control cabinets and precision components in moisture-protected wooden cases and heavy frames braced bare on cradles with designated lifting points. CE certification for slitting lines is held from UDEM under its own certificate number.
What the downstream line needs from this one
A slitting line is bought for what it hands over, so the specification that matters is the one the next machine reads.
For a tube mill, slit width is what becomes diameter: strip width error propagates through forming into finished outside diameter, which is why the ±0.2 mm width tolerance is the headline number rather than throughput.
For a forming line making open sections, camber matters most: a cambered strip forms a twisted profile, and the limit is ≤0.5 mm per 1000 mm.
For both, burr and telescoping decide whether the coil can be run at all — burr at ≤4 per cent of material thickness, telescoping on the recoil at ≤±10 mm.
Where those numbers come from mechanically
The knife set is what holds width: slitting knives, spacers, rubber sleeves and separator discs, configured per strip thickness. Worn knives or a wrong configuration show up as width out of tolerance, heavy burr and camber. The configuration pattern is direct — about 15 strips at 2 mm material, about 4 at 8 mm.
Tension, looper and recoil control is what holds camber and telescoping once the strip is cut. Main unit precision — double-head uncoiler, slitter, 32-tonne recoiler — is what holds both when coil weight goes up.
Who buys upstream equipment
The buyer is a steel processing or pipe plant, and the beneficiaries are downstream: pipe mills, forming plants and steel service centres.
That makes the purchase trigger a plant-flow question rather than a product one. A new plant sizing its whole line, or an existing plant that keeps hitting incoming-coil problems, buys coil preparation to stop paying for them at the tube mill.
Certification, and what each certificate actually covers
ISO 9001 is held under certificate number 18524Q11269R2S, issued by National Standard Integration (Beijing) Certification Co., Ltd. under IAF MLA and CNAS accreditation.
CE certificates are held from UDEM under three separate numbers, and each covers a different line type: welded pipe equipment under M.2022.206.C72171, cold roll forming equipment under M.2022.206.C72172, and slitting lines under M.2022.206.C72173. A fourth CE certificate for cold forming is held from Ente Certificazione Macchine in Italy under 0P250616.HTWTT37.
Each number can be checked at the issuing body rather than taken on trust, which is why we publish numbers and verification routes instead of certificate images.
An enterprise standard, Q/GYLTT01-2023 for HGF150 high-frequency welded pipe equipment, is published on the national enterprise-standard platform. High-Tech Enterprise certificate GR202413001148 is held. The Madrid international trademark for TENGTIAN is registered under number 1 707 606. The patent portfolio is 30 granted utility model patents, with 7 invention patents applied for.
Delivery, payment and after-sales
Lines are dismantled into units and shipped in containers: heavy frames braced bare on cradles with designated lifting points and rust protection, precision and wear items in moisture-protected wooden cases with a spare-parts pack. Delivery takes 50 to 90 days.
Installation and commissioning are part of the supply rather than a separate quotation, backed by on-site dispatch and round-the-clock online support. There is a single point of contact, with a response time of under one hour. Payment is staged — 30 per cent deposit, 70 per cent before shipment — with third-party escrow and multiple trade terms available.
Anonymised reference deliveries
Our lines are running in more than a dozen countries — mostly on construction tube, and also on fire-extinguisher tube, furniture tube and other sections. Delivery cards show region and model or size; commissioning dates are available on request.
The line stage by stage
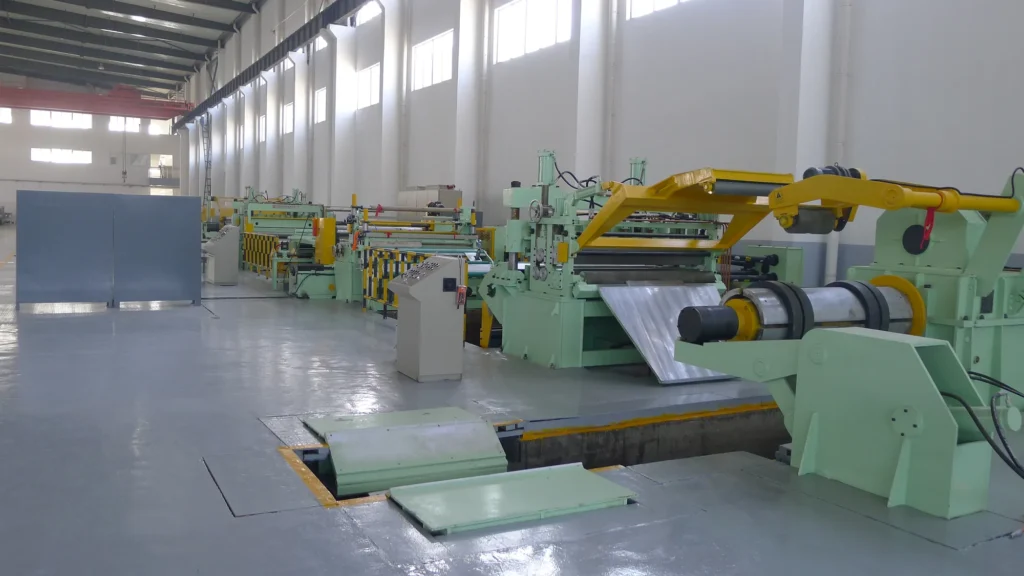
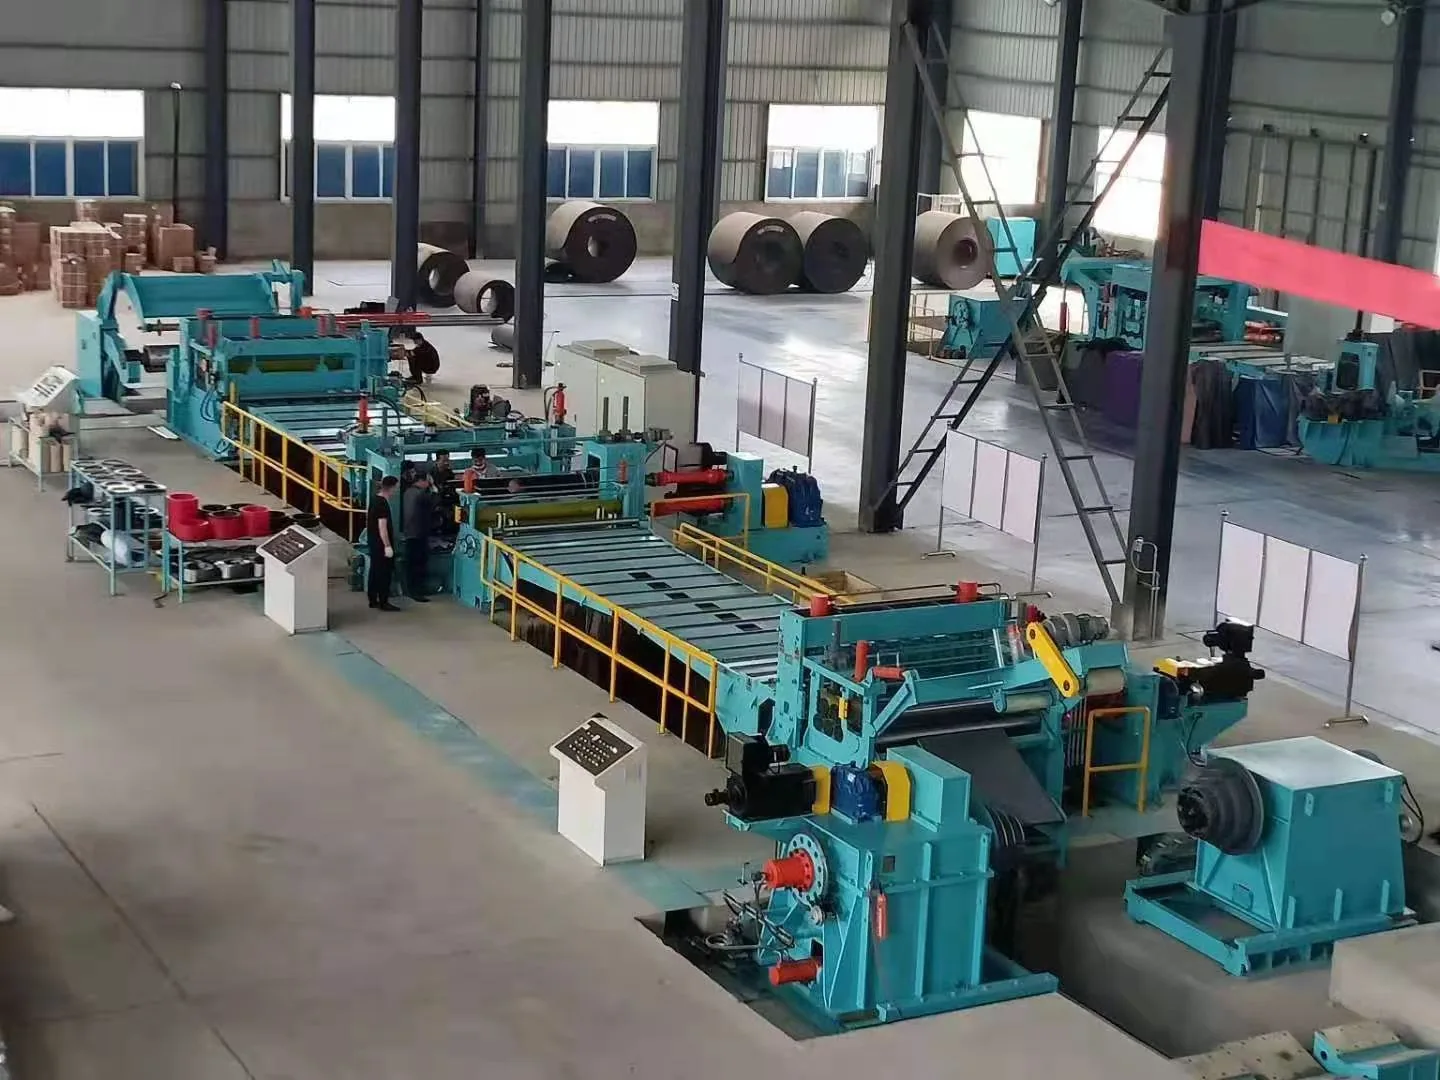
The line runs station by station: coil car and loading, uncoiling, levelling, hydraulic shear, slitting or cross cutting, scrap-edge winding, looper, separation, tensioning, and recoiling.
Three of those exist only to protect strip quality after the cut, and they are the ones a buyer tends to under-specify. Scrap-edge winding removes the trimmed edge cleanly so it does not foul the line. The looper absorbs speed differences between slitting and recoiling. The separation and tension unit keeps each strip under its own controlled tension so the rebuilt coil does not telescope.
The failure chain is clear: knife-set configuration, tension or looper control that is not right produces width out of tolerance, camber and telescoping, and the consequence is downstream — the material does not suit the next line.
Two modes, one line
Slitting and cut-to-length are two operating modes of the same line. For slitting, the specification covers width tolerance ±0.2 mm, camber ≤0.5 mm per 1000 mm, burr ≤4 per cent of material thickness, telescoping ≤±10 mm, knife configuration by thickness.
What this line is not
It does not correct incoming grade. The division is that the line offers levelling and incoming inspection capability, while strip grade and flatness remain the buyer’s responsibility.
It does not weld. The whole flow is uncoil, level, shear, slit or cut, recoil — no welding station appears anywhere in it.
It is not sized by finished-product diameter. Its window is defined by the incoming coil — 1–12 mm thick, 800–2000 mm wide, up to 32 tonnes — and the finished pipe diameter belongs to the machine downstream.
What to send with an enquiry
Incoming coil thickness, width and weight; the number and width of strips you need out; and what the strip feeds downstream. Those map directly onto the 1–12 mm, 800–2000 mm and 32-tonne window and onto the knife-set configuration, which is set by thickness.
If the line will also run in cut-to-length mode, say so in the enquiry, because cut-to-length parameters are configured to order.
Correct line sizing is its own risk item — a line matched wrongly to the need produces capacity and quality that do not fit.
The two knife-related numbers, read together
Two numbers govern the cut edge and they are read together rather than separately: width tolerance ±0.2 mm, and burr no more than 4 per cent of material thickness.
Width is set by the knife and spacer stack, so it drifts when the stack is worn or configured for a different thickness. Burr is set by the clearance between the knives, so it grows when clearance is wrong for the material even if width is still inside tolerance. A line that holds width but throws burr is telling you about clearance, not about the stack width.
That is why knife configuration is a per-thickness setting with a pattern attached — about 15 strips at 2 mm, about 4 at 8 mm — rather than as a fixed arrangement.
The third number, telescoping at ≤±10 mm on the recoil, comes from somewhere else entirely: tension and looper control, not the knives.
Tension, looper and recoil control is what limits camber and telescoping in service.
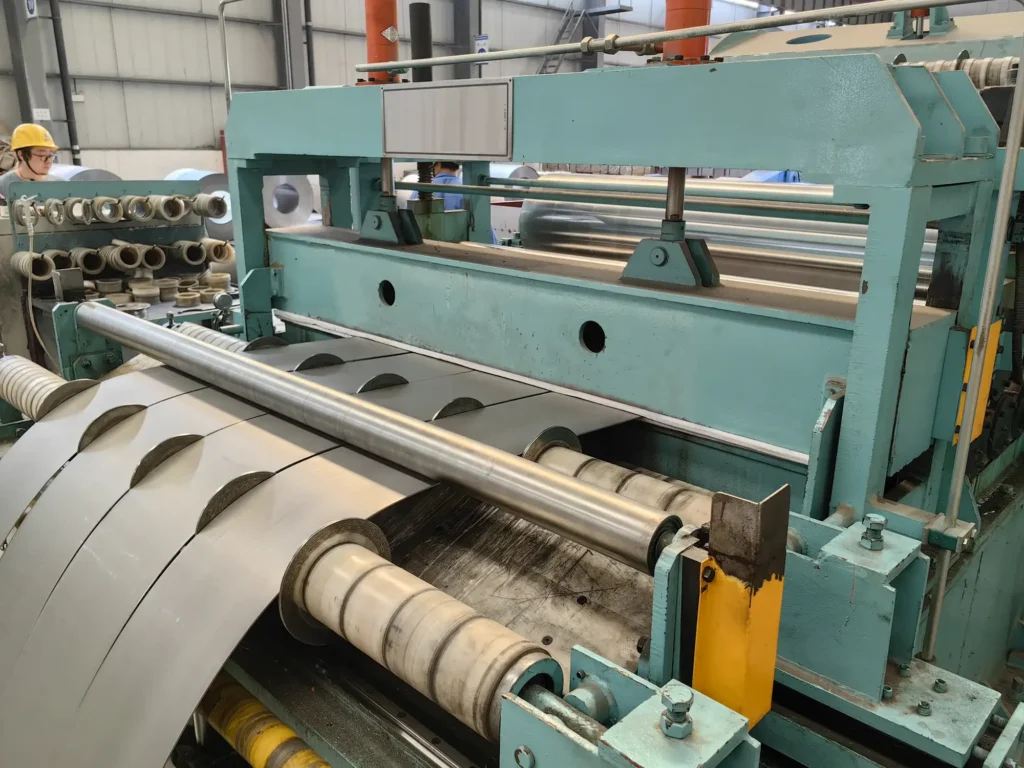
Line Photos from the Works
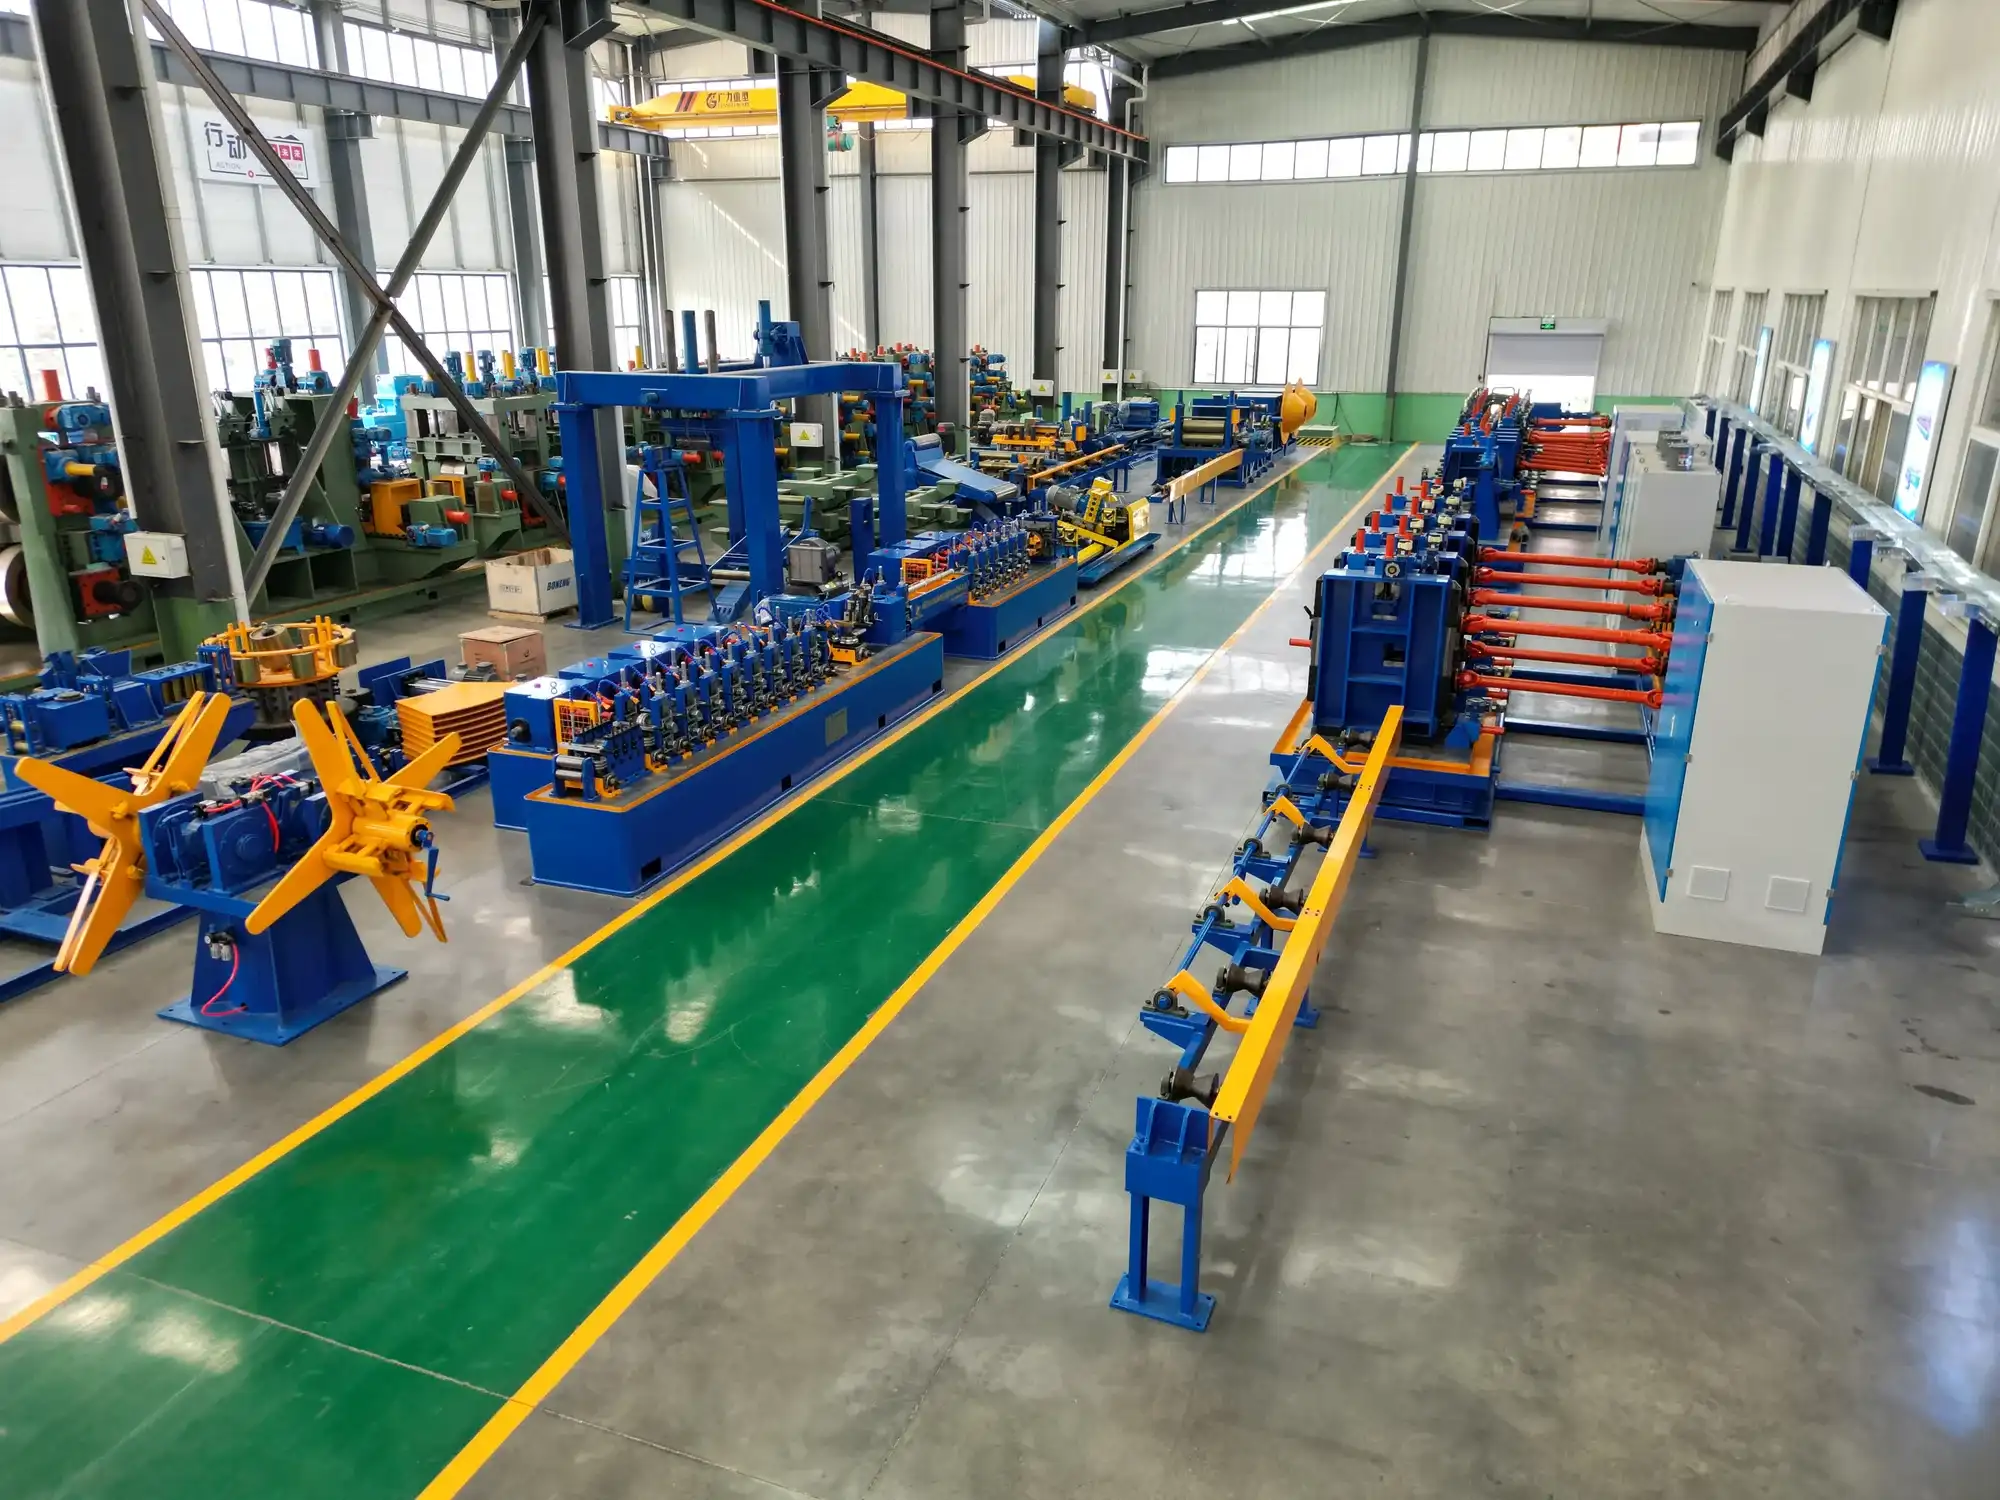
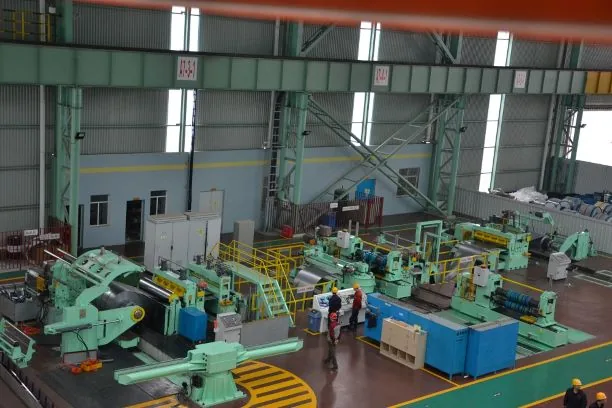
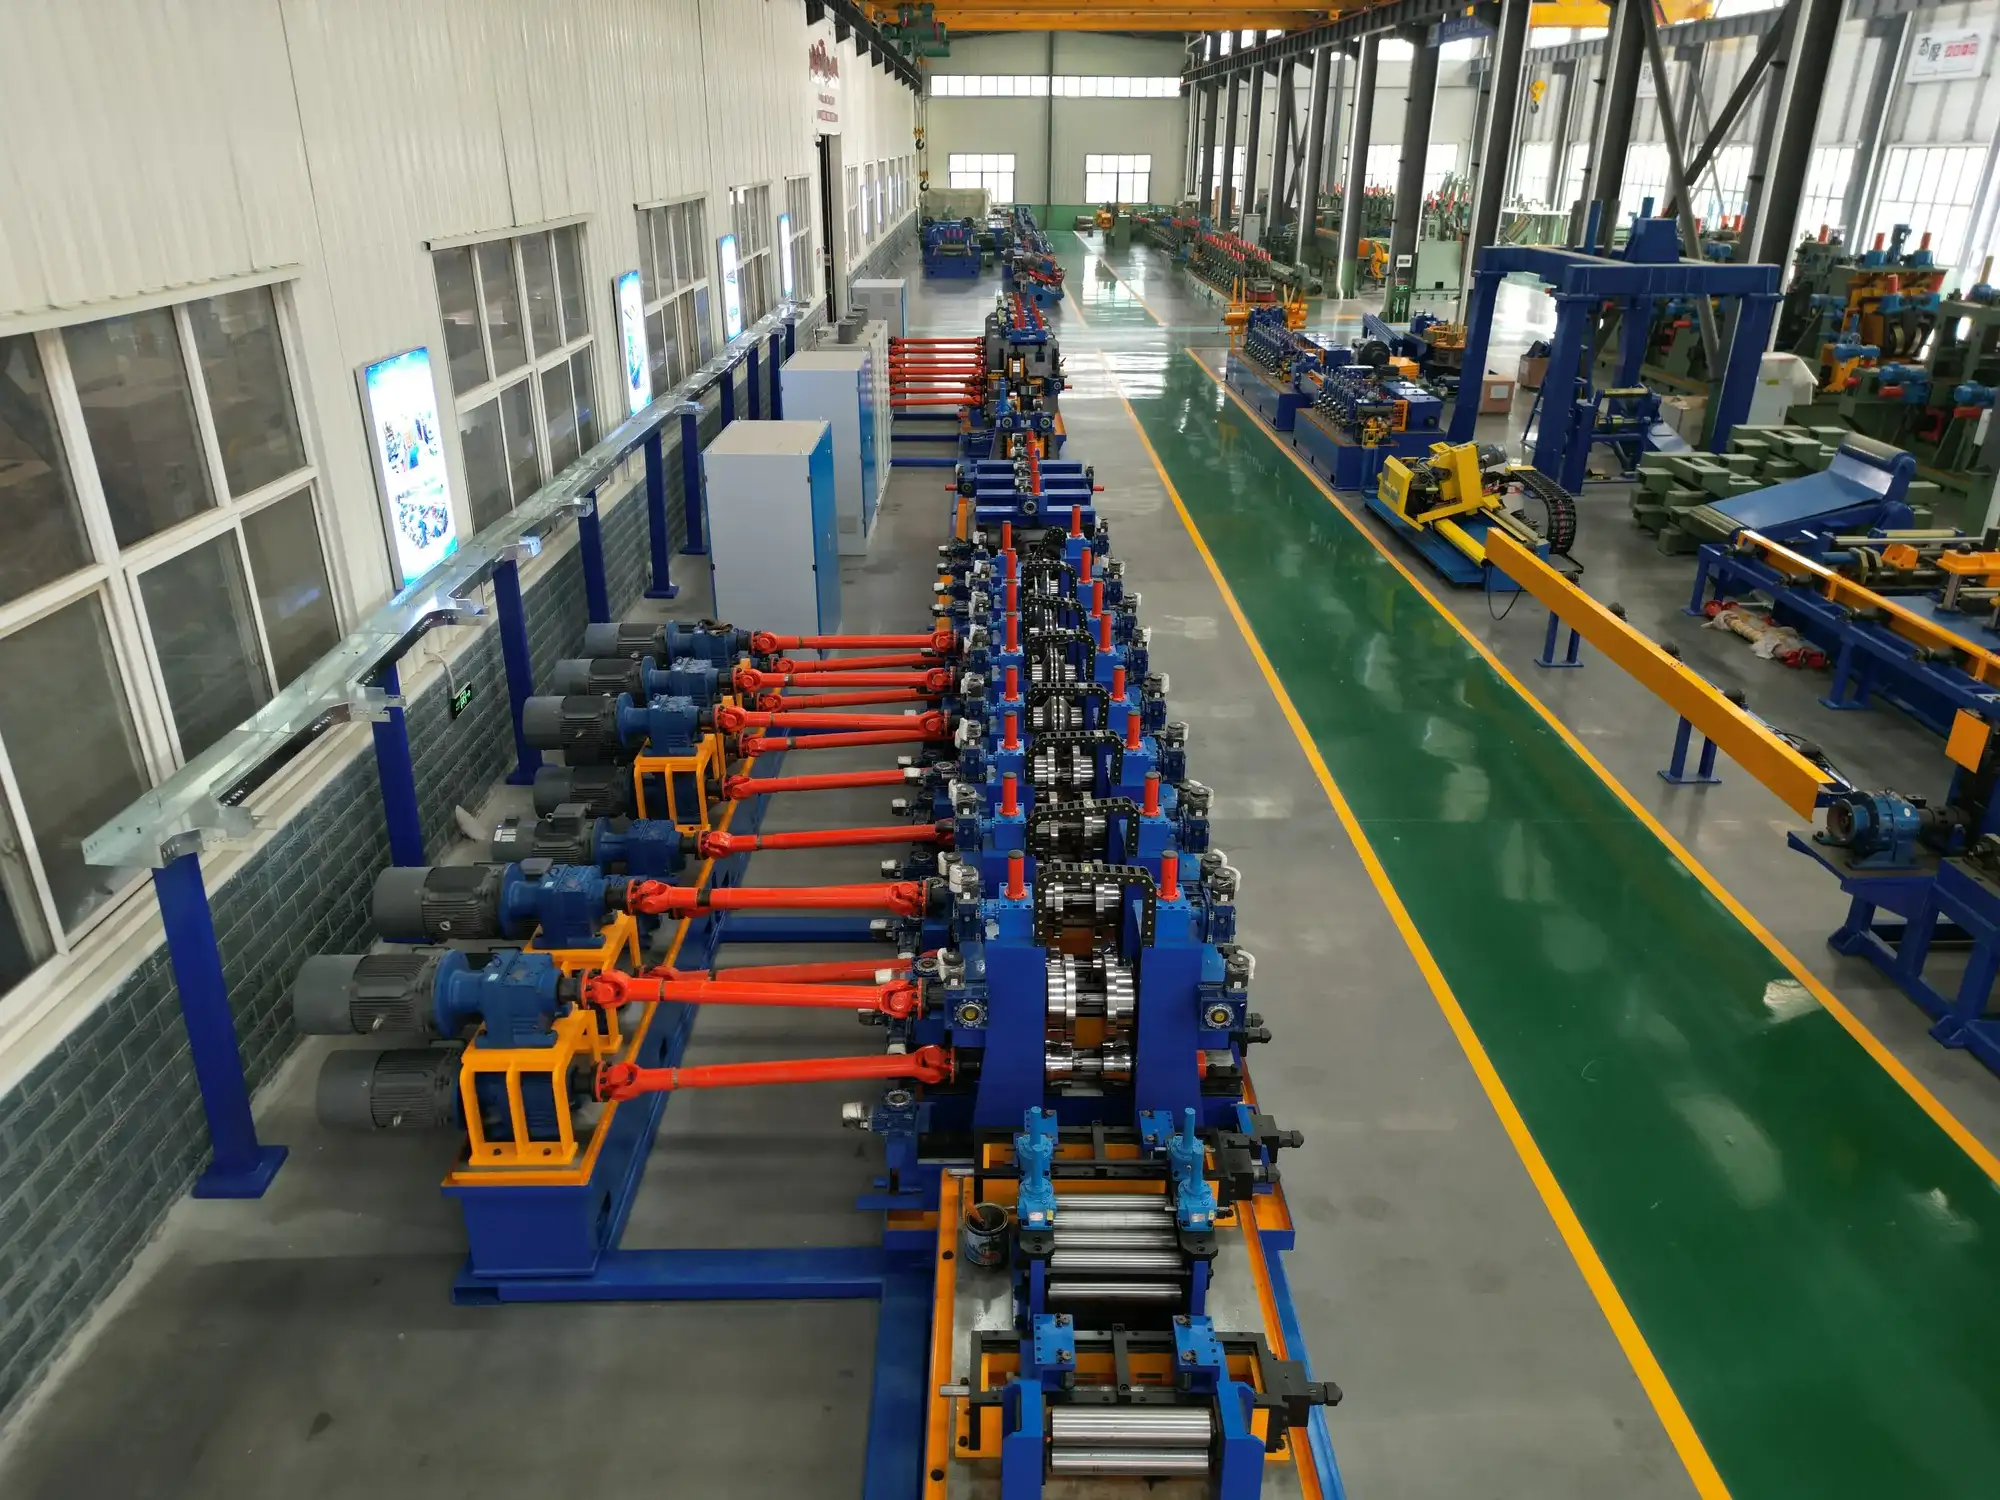
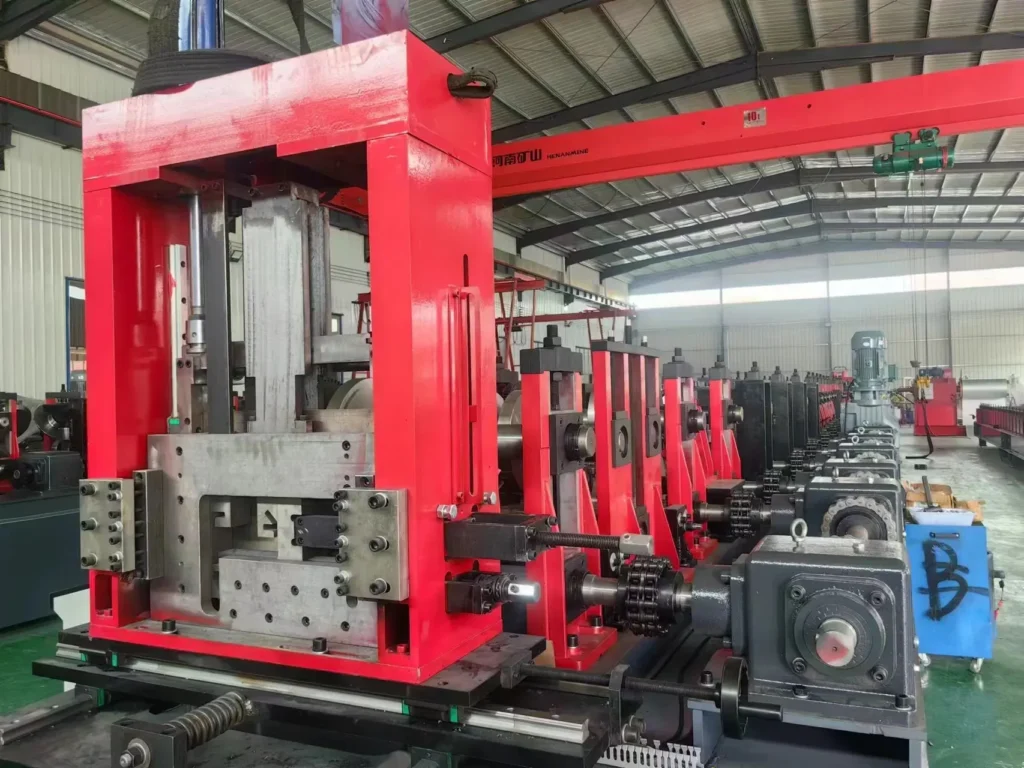
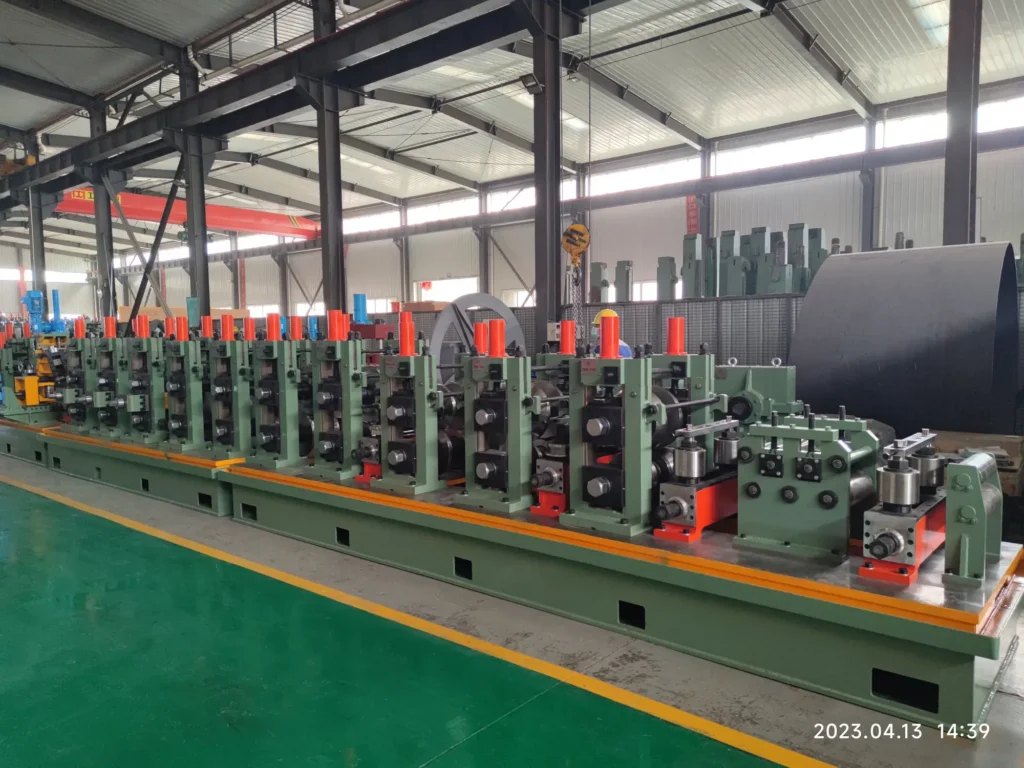
Eight photographs of this line, taken in our own workshop. Click any photo for the full-size image.
More from this line
More on this line — specifications, model steps and photographs.
 Roll Forming Machine
 Purlin Machine Lines
 Pipe Production Applications
 Large Diameter Tube Mill
Send Your Enquiry
Tell us the pipe outside-diameter range, the wall thickness and the output you need. An engineer reads every enquiry — it does not land in a general sales inbox.