
 Scan on WeChat
Home › Tube Mill › Small-Diameter Tube Mill › HG89
The fourth of the twelve model steps — Φ32 – Φ89 mm round pipe and 25×25 – 70×70 mm square section, on a 300 kW high-frequency welder.
Model Steps
In This Line
Quick Contact
Hebei TengtianYuanle@tentubemill.com
+86-311-83025332
WhatsApp +852 5425 3155
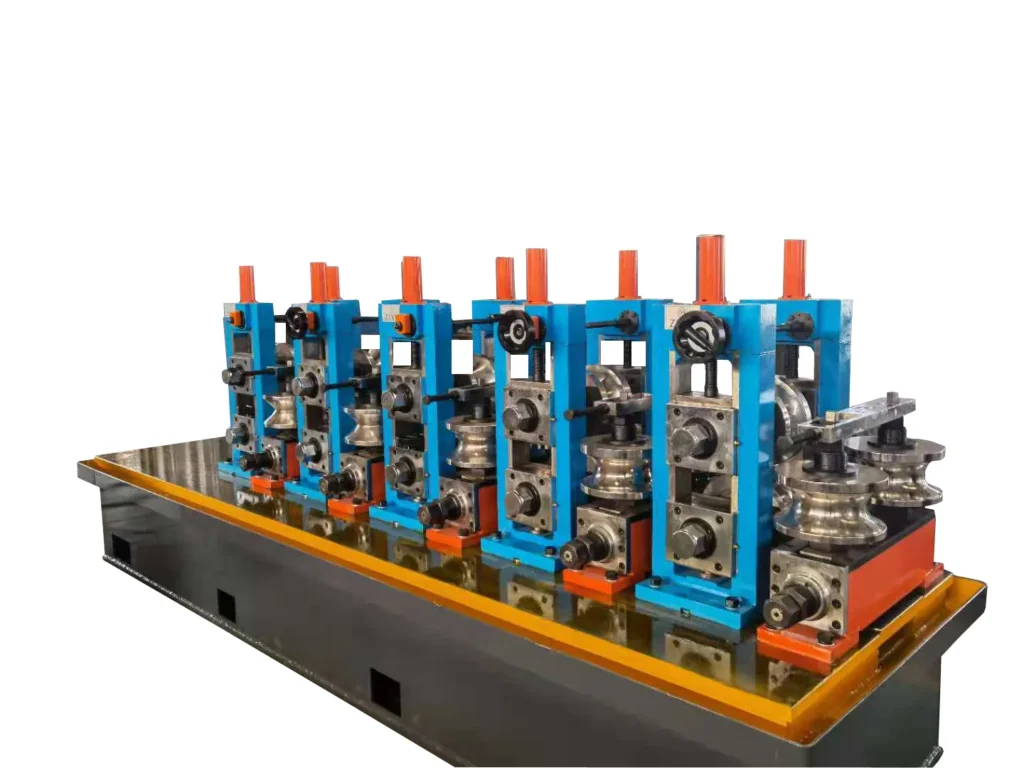
HG89 is the fourth of the twelve steps, covering Φ32–89 mm. Its lower bound is where HG32 stops, which makes it the natural step for a plant that already runs small tube and wants to move up into scaffolding and light structural section without leaving the same process chain.
Line Specification — HG89×4.0
| Round tube outside diameter | Φ32 – Φ89 mm |
|---|---|
| Wall thickness | 1.0 – 4.0 mm |
| High-frequency welder | 300 kW |
| Square / rectangular tube | Square 25×25 – 70×70 mm; wall 1.0 – 3.5 mm |
Watch This Line Running
HG89 High-Frequency Welded Pipe Mill — O.D. 32-89 mm
Technical Specification Table
- Outside diameter range: Φ32–89 mm, the fourth of twelve steps.
- Section shapes: round, square and rectangular.
- Forming: conventional roll forming.
- Welding: high-frequency induction.
- Automation: semi-automatic or full PLC.
- Welder power for this step: 300 kW
Line Configuration and Scope of Supply
- Expanding-mandrel uncoiler.
- Five-roller leveller.
- Automatic shear-welder.
- Spiral accumulator.
- Forming and sizing mill.
- HF induction welder.
- Flying saw.
- PLC and VFD control.
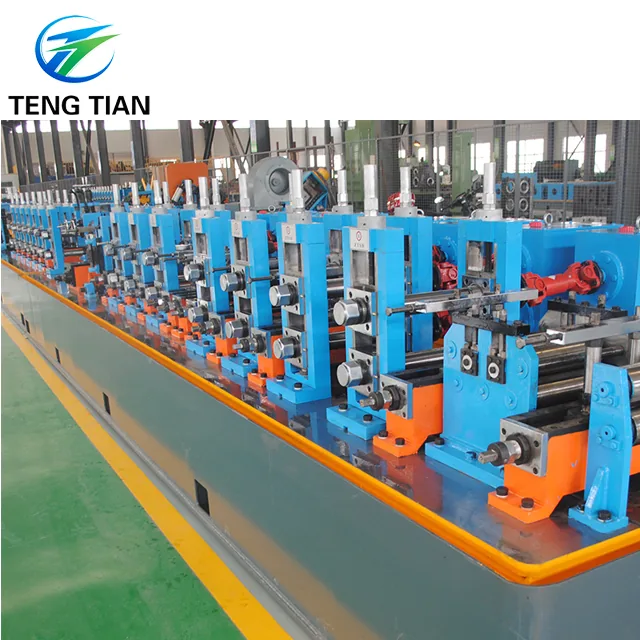
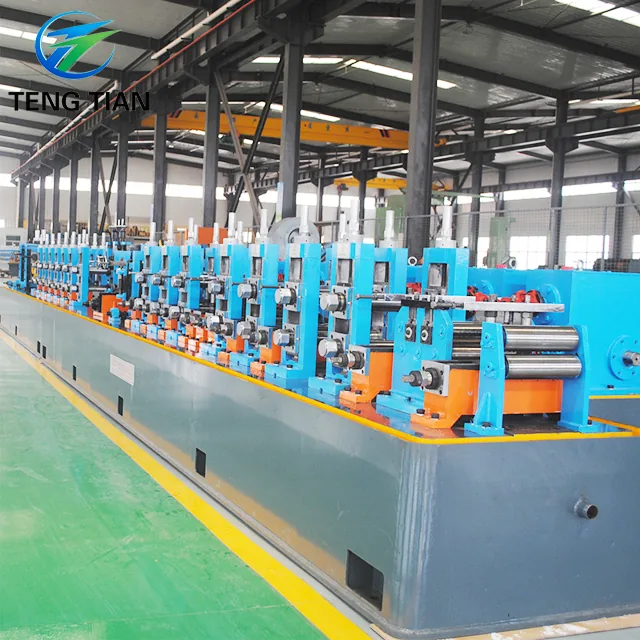
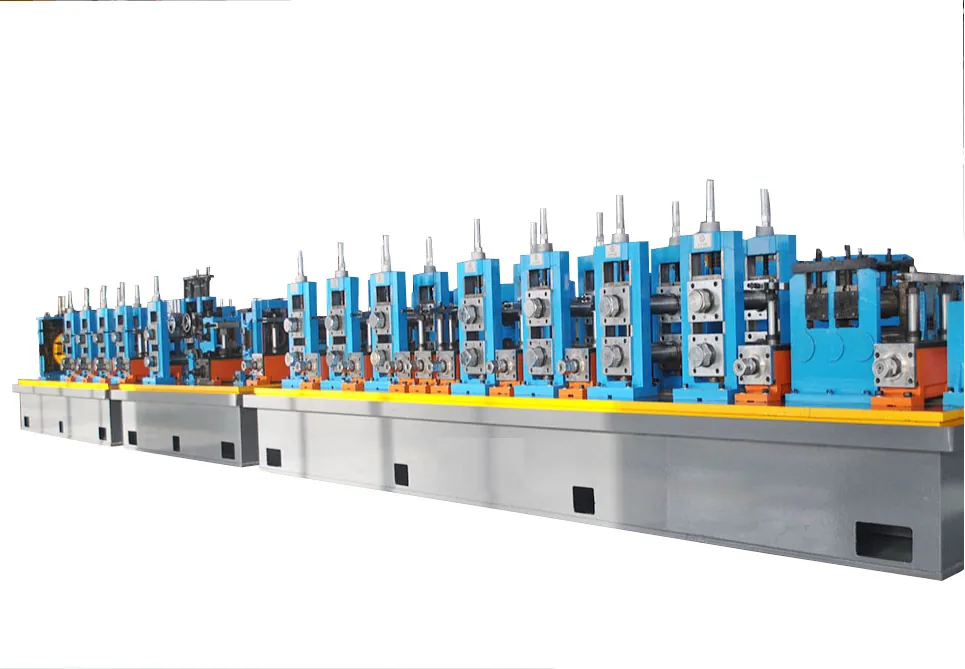
Tube mill for 89mm pipe
At Φ32–89 mm the second family is the usual one, and its acceptance criteria are different: what a scaffolding buyer checks is squareness and straightness of the section, edge line quality and how quickly the mill can switch size — not pressure rating.
Wear Parts and Consumables
Saw blades by cutting volume; impeders and induction coils by welding hours; forming and sizing rolls on wear, machined in-house.
Two application families apply to this process. The first is fluid transport — carbon steel welded pipe for oil and gas lines, municipal water and gas, and chemical or heating lines. The second is structural and scaffolding tube: load-bearing building sections, scaffolding and general mechanical square and rectangular tube.
Size Change, Roll Wear and Running Cost
Yield above 93 per cent is supported by line design and also depends on the plant’s own scheduling. A size change inside this band is a roll change. Roll material and heat treatment set how long that set lasts before diameter starts to drift, and under-specified rolls show up as early wear, drift and repeated regrinding rather than as an immediate failure.
Send your section mix, wall and target output and we will size the step and list the open items rather than filling them.
Where this step sits in the twelve
HG89 is the fourth rung. Below it are HG32, HG50 and HG76; above it HG114 and the large-diameter group.
Anonymised delivery record
Deliveries in this band: Egypt at HG76 × 3 and HG89 × 5, Sri Lanka at 89 × 5, India at 76 × 3, and Malaysia at HG60 × 3.
The buyer for this band
At Φ32–89 mm the usual buyer is a regional pipe and section maker producing scaffolding and light structural tube. Their acceptance criteria are return on investment, how fast a size change can be made, roll cost and energy per tonne.
Two purchase triggers apply directly. A new plant sizing its first line to a target diameter, and an existing plant expanding capacity or upgrading to full automation. For the second, automation is a grade of the same series rather than a different mill, which is why an upgrade does not mean replacing the process.
Delivery, installation and support
Shipped dismantled in containers with heavy frames braced and precision items cased; delivery 50 to 90 days; installation and commissioning included with on-site dispatch and round-the-clock support; single contact replying round-the-clock. Payment is 30 per cent deposit and 70 per cent before shipment, with third-party escrow and multiple trade terms.
Operating steps that need training
Four of the five operating procedures are marked as requiring training: loading and threading the strip; shear-welding the coil join; setting specification and changing tooling; and setting and running the weld parameters. Only cutting and collecting is routine operation.
That matters for a first-line buyer, and it is why installation and commissioning are part of the supply rather than as an extra, with on-site dispatch and round-the-clock support behind them.
Quality factors at this diameter
The ten split into material, tooling, process, people-and-control, and inspection. The two that most often explain a rejected batch on structural tube are squeeze amount with seam alignment, and sizing with straightening — the first shows as weld offset and burr, the second as diameter out of tolerance, bend or ovality.
What to send with an enquiry
Section shape and size, wall, target output, and the standard the finished section is written against.
One more boundary on this step
Post-weld cooling is its own quality factor, stabilising seam structure and needing to be matched to welding speed; the medium is specified by us and sourced locally. Final inspection is the last quality factor, with ultrasonic and eddy current named for API lines specifically rather than for this configuration.
Two divisions worth repeating here
Weld fusion is on the equipment side — power matching, seam alignment, squeeze control — while strip quality and operating practice are on the buyer’s. Dimensional accuracy divides the same way: sizing and straightening on the equipment side, incoming strip thickness tolerance on the buyer’s.
Consistency after a size change is on the equipment side through servo setup, with tooling-change practice on the operator’s.
The application families at this size, read carefully
Two families apply to this process, and at Φ32–89 mm both are plausible, which is why the enquiry matters more here than on the narrow steps.
Fluid transport takes carbon steel welded pipe for oil and gas, municipal water and gas, and chemical and heating lines; what that buyer checks is weld pass rate, diameter and wall coverage, non-stop coil change, and energy and yield.
Structural and scaffolding takes load-bearing building sections, scaffolding and general mechanical square and rectangular tube; what that buyer checks is squareness and straightness, edge line quality, changeover efficiency and unit energy.
Batch-to-batch consistency after a change is held by servo setup; speed and cut length are held by PLC and variable-frequency control. Dimensional accuracy is split: sizing and straightening on the equipment side, incoming strip tolerance on the buyer’s.
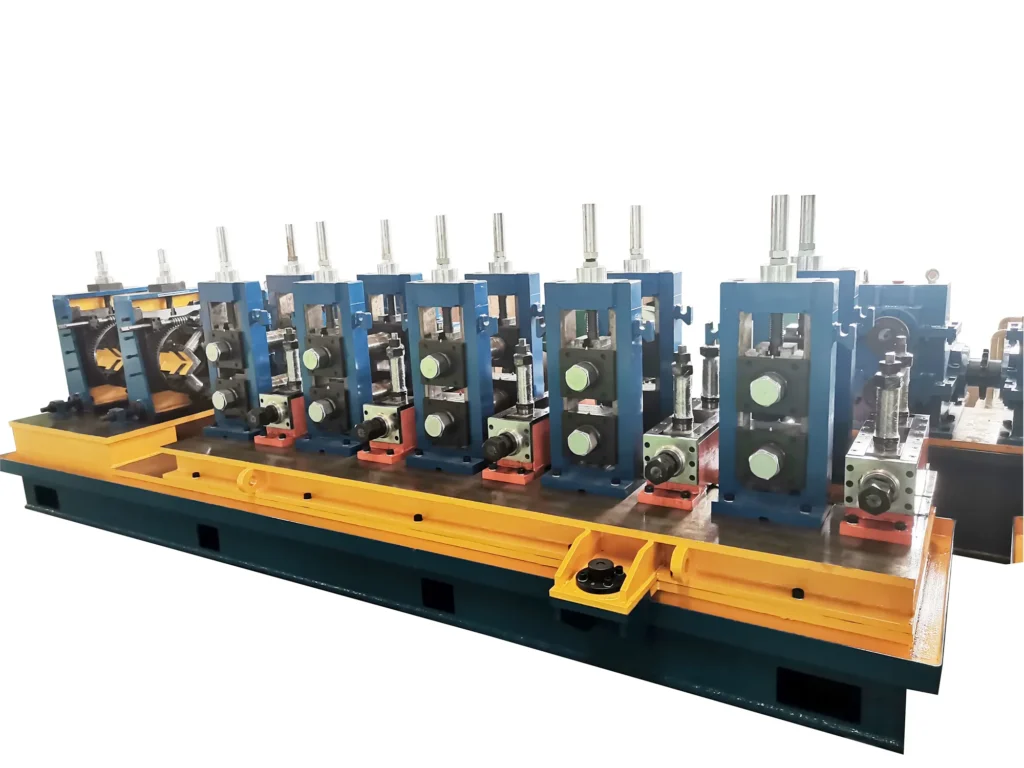
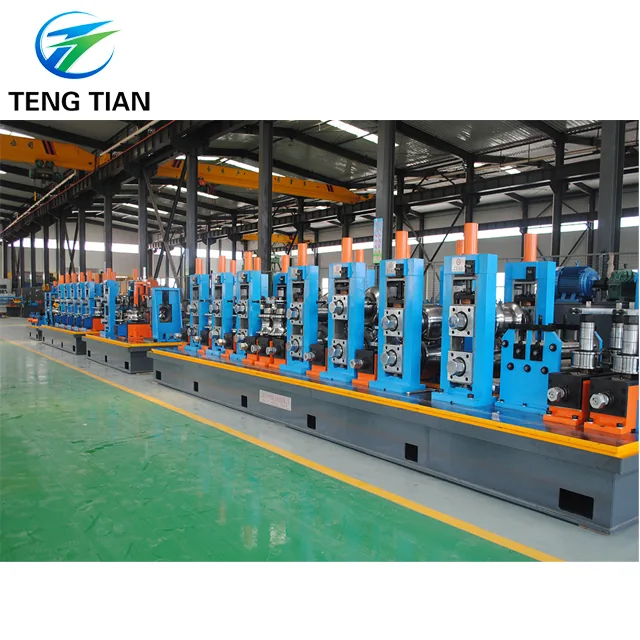
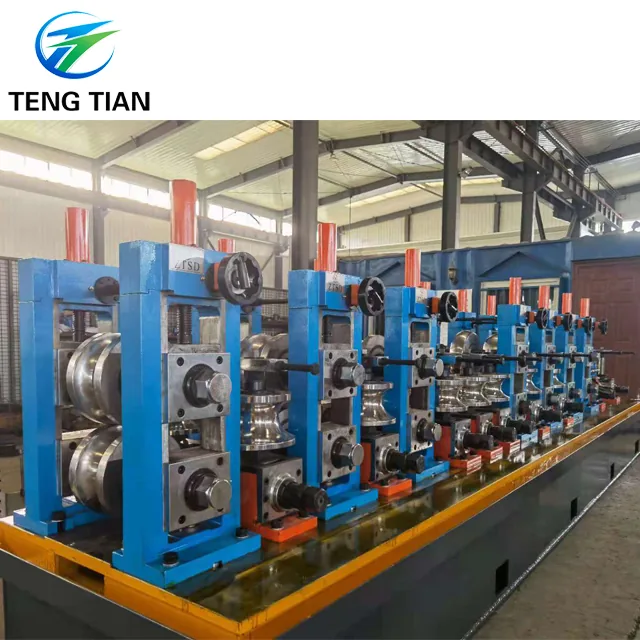
Line Photos from the Works
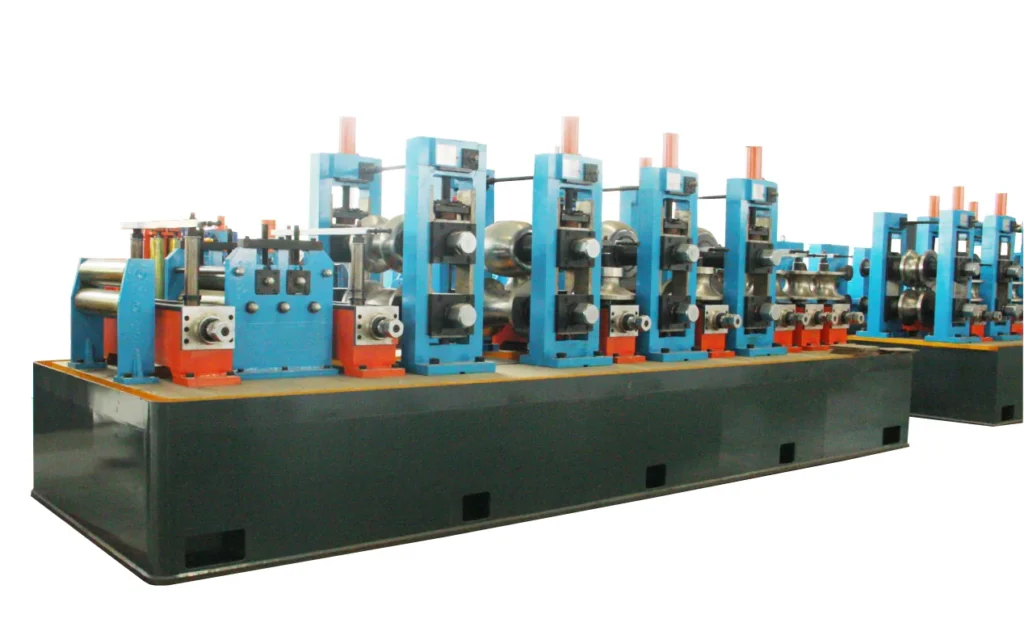
Four photographs of this line, taken in our own workshop. Click any photo for the full-size image.
More from this line
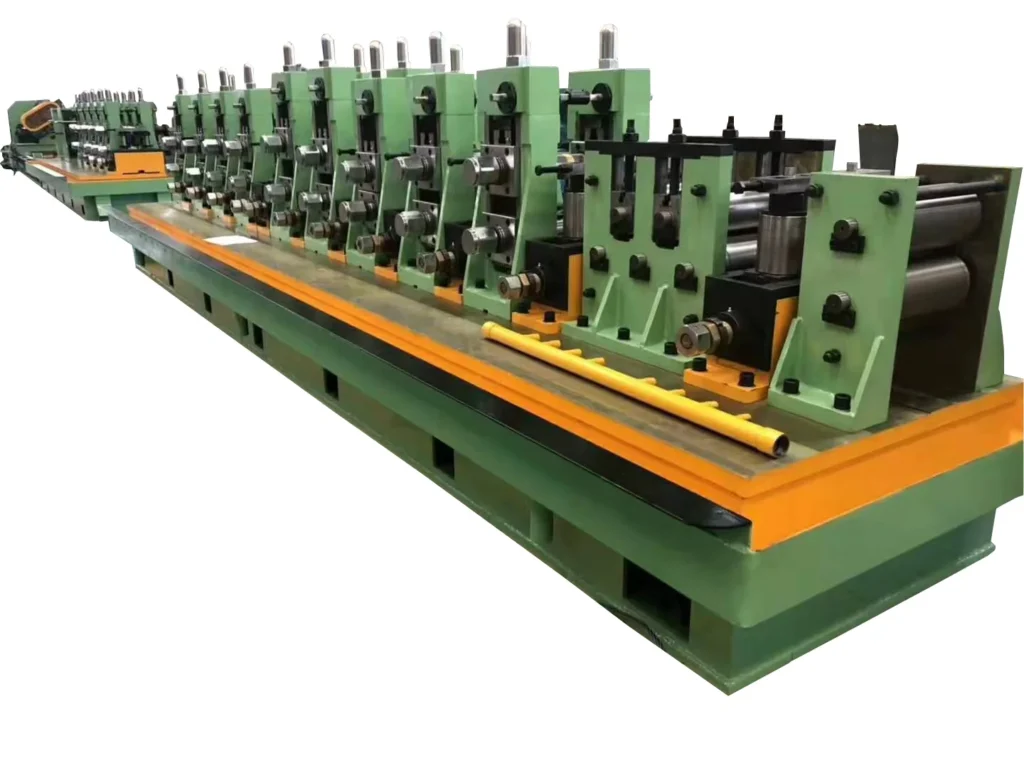 HG50
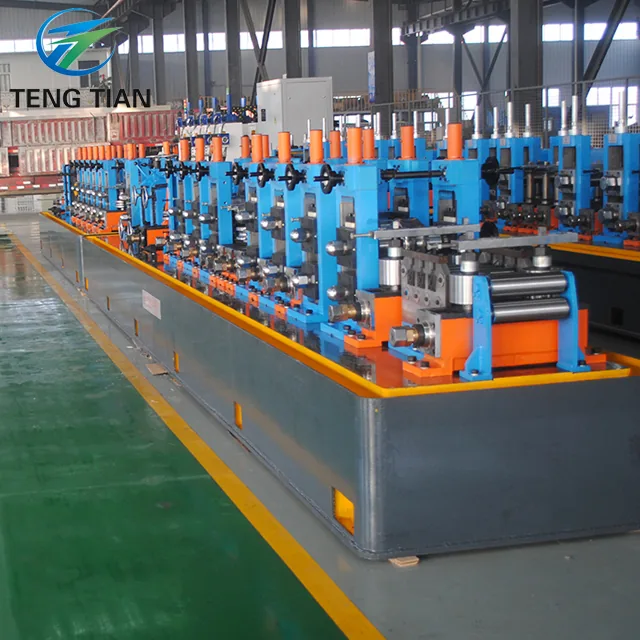 HG76
 HG114
 HG165
Send Your Enquiry
Tell us the pipe outside-diameter range, the wall thickness and the output you need. An engineer reads every enquiry — it does not land in a general sales inbox.