
 Scan on WeChat
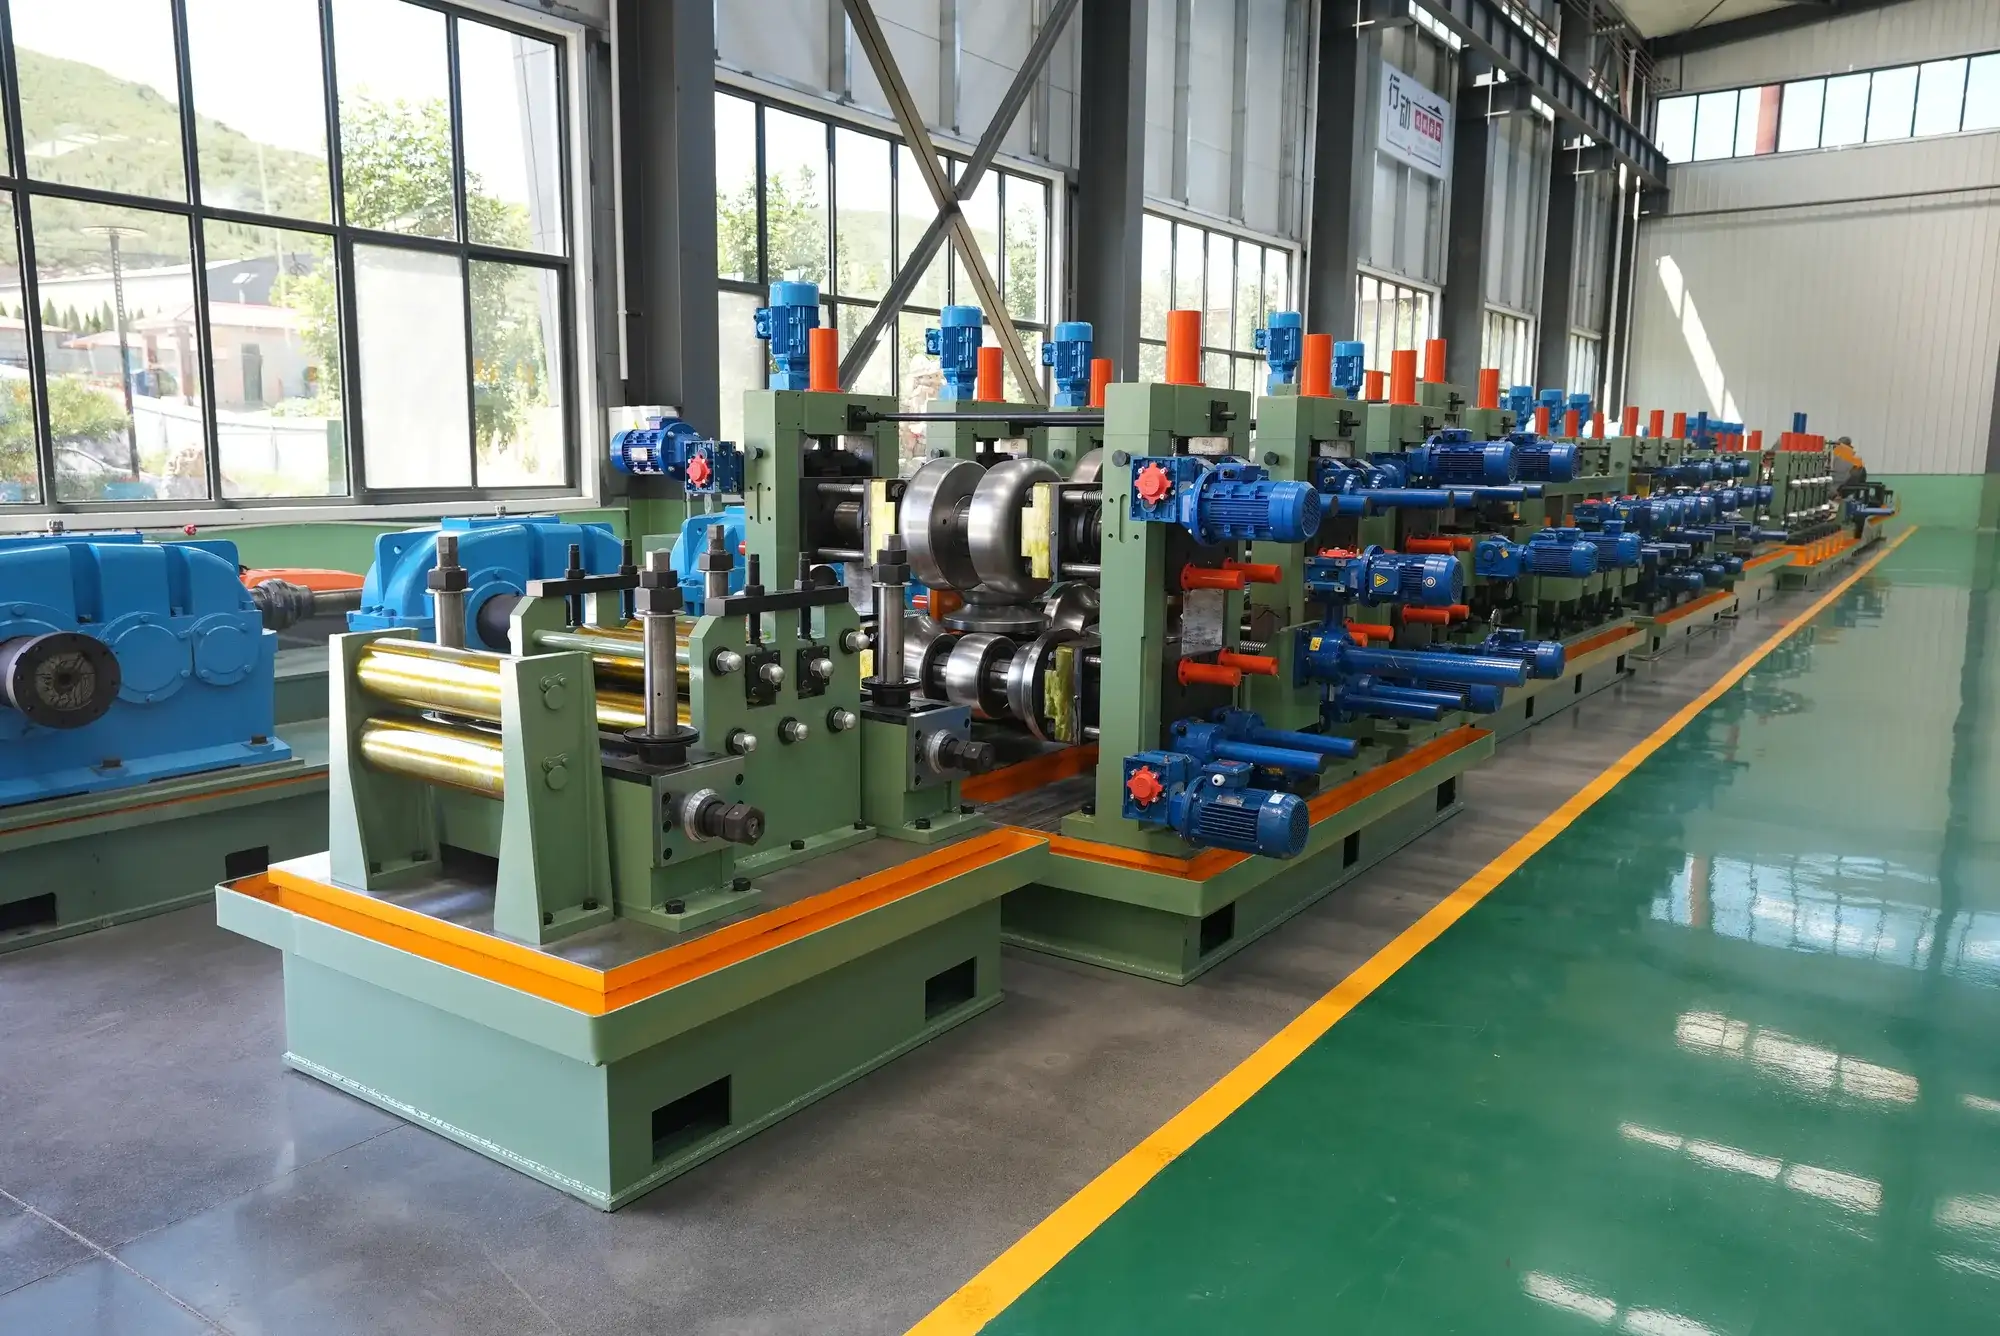
Tengtian builds welded pipe lines, not seamless mills. Below, the welded side is covered in full — two welding routes, twelve size classes plus two spiral classes, and the standards each is tested to — while seamless appears only in a single comparison.
Which Welded Route, and How It Compares With Seamless
- The one comparison against seamless: high-frequency longitudinal welding is lower in investment and running cost, more continuous, and suited to mid and small diameters in volume.
- The welded side is in two routes: high-frequency longitudinal (HFW/ERW) and spiral submerged-arc (SSAW).
- Diameter coverage: Φ10–630 mm across twelve HFW size classes, and Φ219–1620 mm on the spiral line.
- Standards differ by line and class: GB/T 9711 and GB/T 5037 on the Φ820 spiral class, GB/T 9711 and API 5L on the Φ1620 class.
- Tengtian builds welded pipe lines; seamless pipe is a different process — no process data, no cost figure, no standard, no performance value. available on request
What Is Seamless Pipe vs Welded Pipe
Yield is set at not less than 93%, although actual yield also depends on the buyer’s own operation. The distinction is about how the pipe body is closed. A welded pipe starts as flat strip that is formed into a shell and then joined along a seam; a seamless pipe has no such seam. Tengtian builds only the first of these: welded pipe lines.
Uses are set out in detail for both welded routes. For the spiral line, four downstream uses apply: oil and gas line pipe, low-pressure fluid and urban gas pipe, water supply and drainage pipe, and industrial structural pipe.
For the high-frequency lines the uses are fluid transport pipe — oil and gas, municipal water and gas, chemical and heating pipework — and structural and scaffolding tube.
Erw pipe vs seamless cost
The answer is one of direction, not magnitude: the high-frequency welded route carries lower investment and lower running cost than seamless rolling. Wall thickness, line speed and shift output are confirmed against your pipe size, material grade and cut length at quotation. Send us those three and we will state the figures.
On the welded side, running cost over time comes down to: low roll wear, high yield and quick changeover.
One comparison places the two side by side. Against seamless rolling and against UOE/JCOE, the high-frequency longitudinal welded route is lower in investment and running cost, higher in continuity, and suited to mid and small diameters produced in volume.
Seamless Pipe vs Welded Pipe Explained
Tengtian currently builds lines for both routes: high-frequency longitudinal welding (HFW/ERW) and spiral submerged-arc welding.
The welded side is two distinct processes, not one.
The two are separated by more than seam direction. Against high-frequency longitudinal welding, the spiral route is substituting a spiral seam and submerged-arc welding for a longitudinal seam and high-frequency welding, and as changing diameter by changing the forming angle rather than by changing rolls.
That gives one machine a wide diameter span and the ability to make large-diameter heavy wall — up to Φ1620 × 16 mm at 7.5 tonnes per pipe — but at a lower welding speed of 0.5 to 3 m/min and in discontinuous production, which suits large diameters in small to medium batches.
There is a hard boundary between the two welded routes, and it is the reason the spiral line exists at all. The high-frequency line is bounded at Φ630 mm.
A buyer who needs line pipe, water pipe or structural pipe above that diameter has to move to spiral submerged-arc; and because one spiral machine covers Φ219–1620 mm by changing the forming angle, that buyer does not have to build a separate line for each diameter class.
The high-frequency side has its own reason for existing, and it is about continuity rather than diameter. The core need it answers is continuous production without stopping — the spiral accumulator keeps the mill fed while coils are changed — plus one line covering multiple sizes, stable yield and weld quality, and changeover efficiency.
The spiral route is also compared against UOE/JCOE, which is the other seamless-adjacent alternative buyers raise. Compared with those, the spiral line forms continuously from strip coil, with lower equipment investment and floor area and more flexible size switching.
Erw vs lsaw pipe
Against UOE/JCOE longitudinal submerged-arc, the spiral route is lower in equipment investment and floor area and more flexible in size switching, because it forms continuously from strip coil. Against the same alternative, the high-frequency route is lower in investment and running cost and more continuous. These comparisons are qualitative.
Put the other way round, the high-frequency route is the faster one: higher welding speed, a longitudinal seam, and a fit with structural and ordinary fluid pipe.
HFW, SSAW and Seamless — How They Compare
Tengtian builds the two welded routes, and the comparisons above are drawn from lines we have built. Seamless is hot-worked on entirely different plant; for seamless-side figures, the builders of those mills are the right source.
How to Decide: Target Diameter, Application and Volume
The HFW range spans twelve classes: Φ10–32, 16–50.8, 12.7–76, 32–89, 45–114, 60–165, 114–219, 114–273, 165–325, 165–426, 219–508 and 325–630 mm. Target diameter is the first cut and the primary selection dimension. The spiral line comes in two classes, Φ219–820 × 3–12 mm and Φ219–1620 × 5–16 mm.
Application is the second cut, defined by downstream use. For the spiral line the uses are oil and gas line pipe, low-pressure fluid and urban gas pipe, water supply and drainage pipe, and industrial structural pipe. For the HFW lines the uses are fluid transport pipe and structural and scaffolding tube.
Standards are the third cut, and each line is tested to specific standards. The Φ820 spiral class is built to GB/T 9711 and GB/T 5037; the Φ1620 class is built to GB/T 9711 and API 5L, with GB/T 9711-2017 and API SPEC 5L (46th edition) cited at the X-ray and ultrasonic stages.
Volume is the fourth cut. The spiral line’s output is quoted with its basis: about 62 tonnes per 8-hour shift on the Φ820 class, on 1050 mm strip at 12 mm wall making Φ820 × 12 m pipe, roughly 21 pipes at 3 tonnes each; and about 120 tonnes per shift on the Φ1620 class, on 1250 mm strip at 16 mm wall making Φ1620 × 12 m pipe, roughly 15 pipes at 7.5 tonnes each.
Two-shift annual output on the Φ820 class is set at 10,000 to 20,000 tonnes.
Inspection is the fifth cut, and it is the one large-diameter buyers are most sensitive to. The spiral line can be supplied with a complete inspection chain: a 225 kVA X-ray unit, a 1200-tonne hydrostatic tester and offline ultrasonic.
The coverage is defined in numbers — 100% of the weld, 25 mm either side of the heat-affected zone, and not less than 35% of the pipe body — accepted to GB/T 9711-2017 and API SPEC 5L (46th ed.), with laser image capture used for weld tracking.
That matters because large-diameter pipe makers work to project orders and are sensitive to standards and to the inspection chain: what they are checking is whether the diameter and wall coverage reach far enough, whether the chain is complete enough to deliver compliant pipe, and whether output matches the project milestones.
On the spiral line the maximum wall thickness is not a single number: a capacity table sets the maximum wall per steel grade and diameter across Q235, Q355 and L360, and exceeding it has known consequences — forming force falls short, the strip will not roll, or the pipe shape comes out wrong.
The order of decision is therefore grade first, then wall.
One constraint sits underneath all of the above and is easy to miss.
Frequently Asked Questions
In practice, how do seamless and welded pipe differ? The comparison is qualitative and runs one way only. Against seamless rolling and UOE/JCOE, the high-frequency welded route is lower in investment and running cost, more continuous in operation, and suited to mid and small diameters made in volume.
Which one suits my diameter and what I am making? Diameter decides first. The HFW range is Φ10–630 mm across twelve size classes; the spiral range is Φ219–1620 mm across two classes.
Above Φ630 mm the reason is plain: the high-frequency line is bounded at Φ630, so large-diameter line pipe, water and structural pipe have to go to spiral submerged-arc. Application then narrows it further, with the spiral line for line pipe, gas, water and structural use.
How do the running costs of the two compare? The high-frequency route is lower in investment and running cost than seamless rolling and UOE/JCOE, and the spiral route is lower in equipment investment and floor area than UOE/JCOE. On the welded side, the factors that keep running cost down are low roll wear, yield of not less than 93% and quick changeover. The comparison is qualitative; no cost figures are quoted for any route.
Which standards apply to seamless and to welded pipe? For the welded lines the applicable standards are specified line by line: GB/T 9711 and GB/T 5037 on the Φ820 spiral class, GB/T 9711 and API 5L on the Φ1620 class, with GB/T 9711-2017 and API SPEC 5L (46th ed.) cited at the inspection stages.
For the machinery itself no single mandatory certification applies: what governs is the destination’s machinery-safety rules plus the standard the finished pipe must meet.
Which line ships and gets commissioned faster? One delivery range applies at line level: 50 to 90 days, with plant-level customised scheduling from the company’s own manufacturing base. That range is not broken down by welding route, and commissioning time is confirmed per project.
Can one supplier give me both routes? Both welded routes, yes — one supplier covers high-frequency longitudinal and spiral submerged-arc in the same plant, with diameters running from Φ10 all the way to Φ1620 mm, so a buyer does not need a second supplier for large diameter.
Seamless is a different answer: Tengtian builds welded pipe lines, not seamless equipment of any kind, so a seamless mill is not something we supply.
From the Workshop
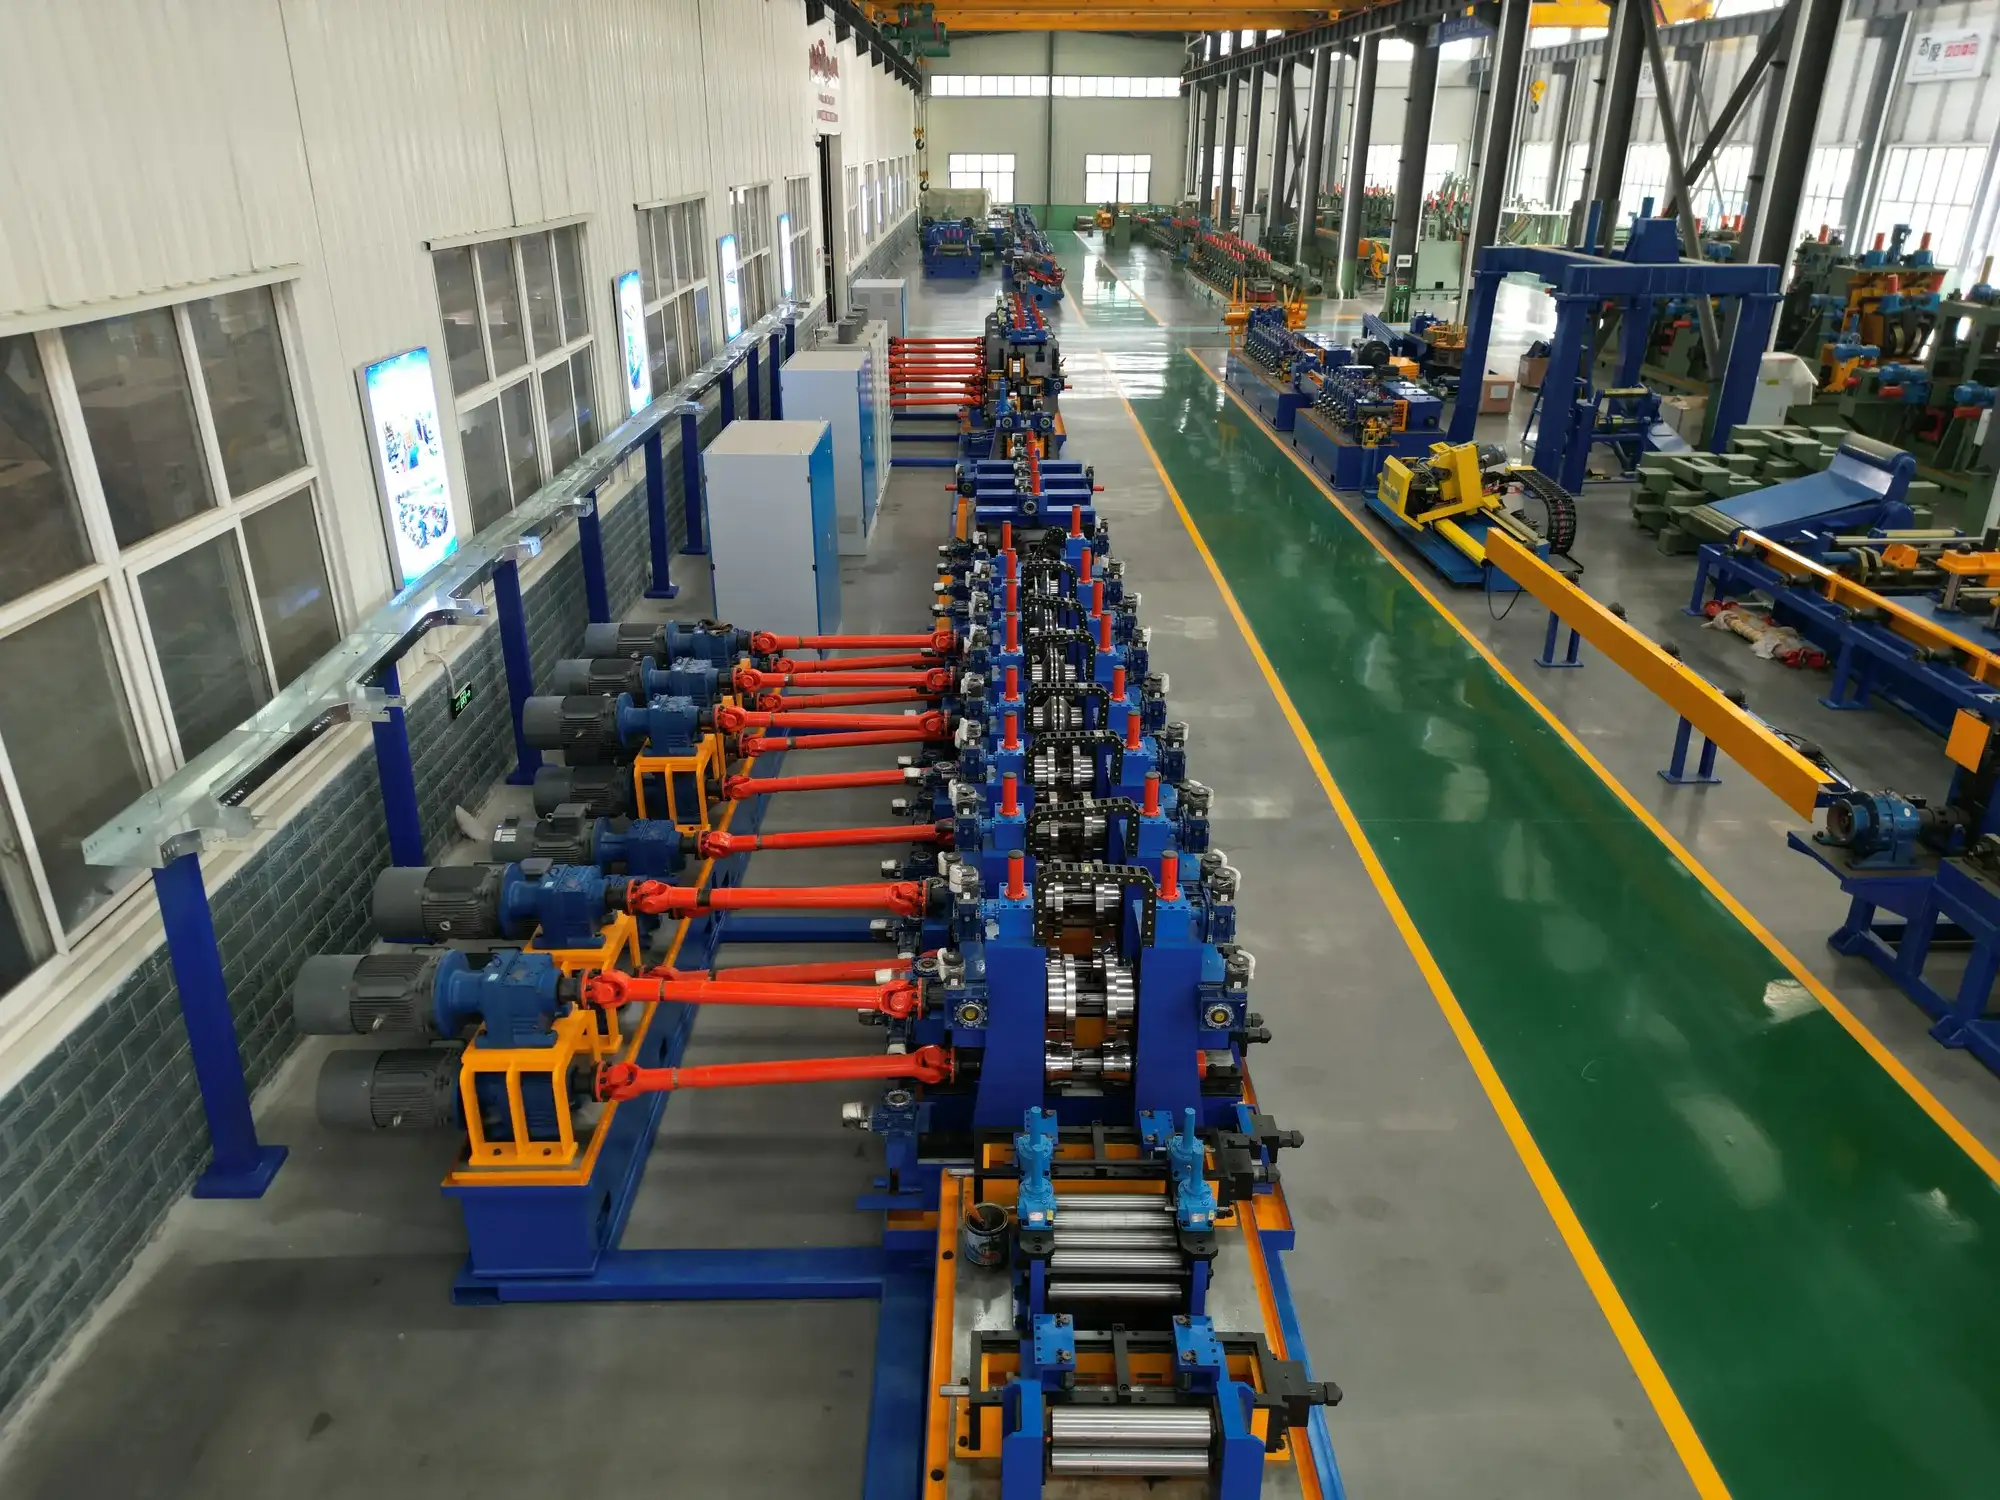
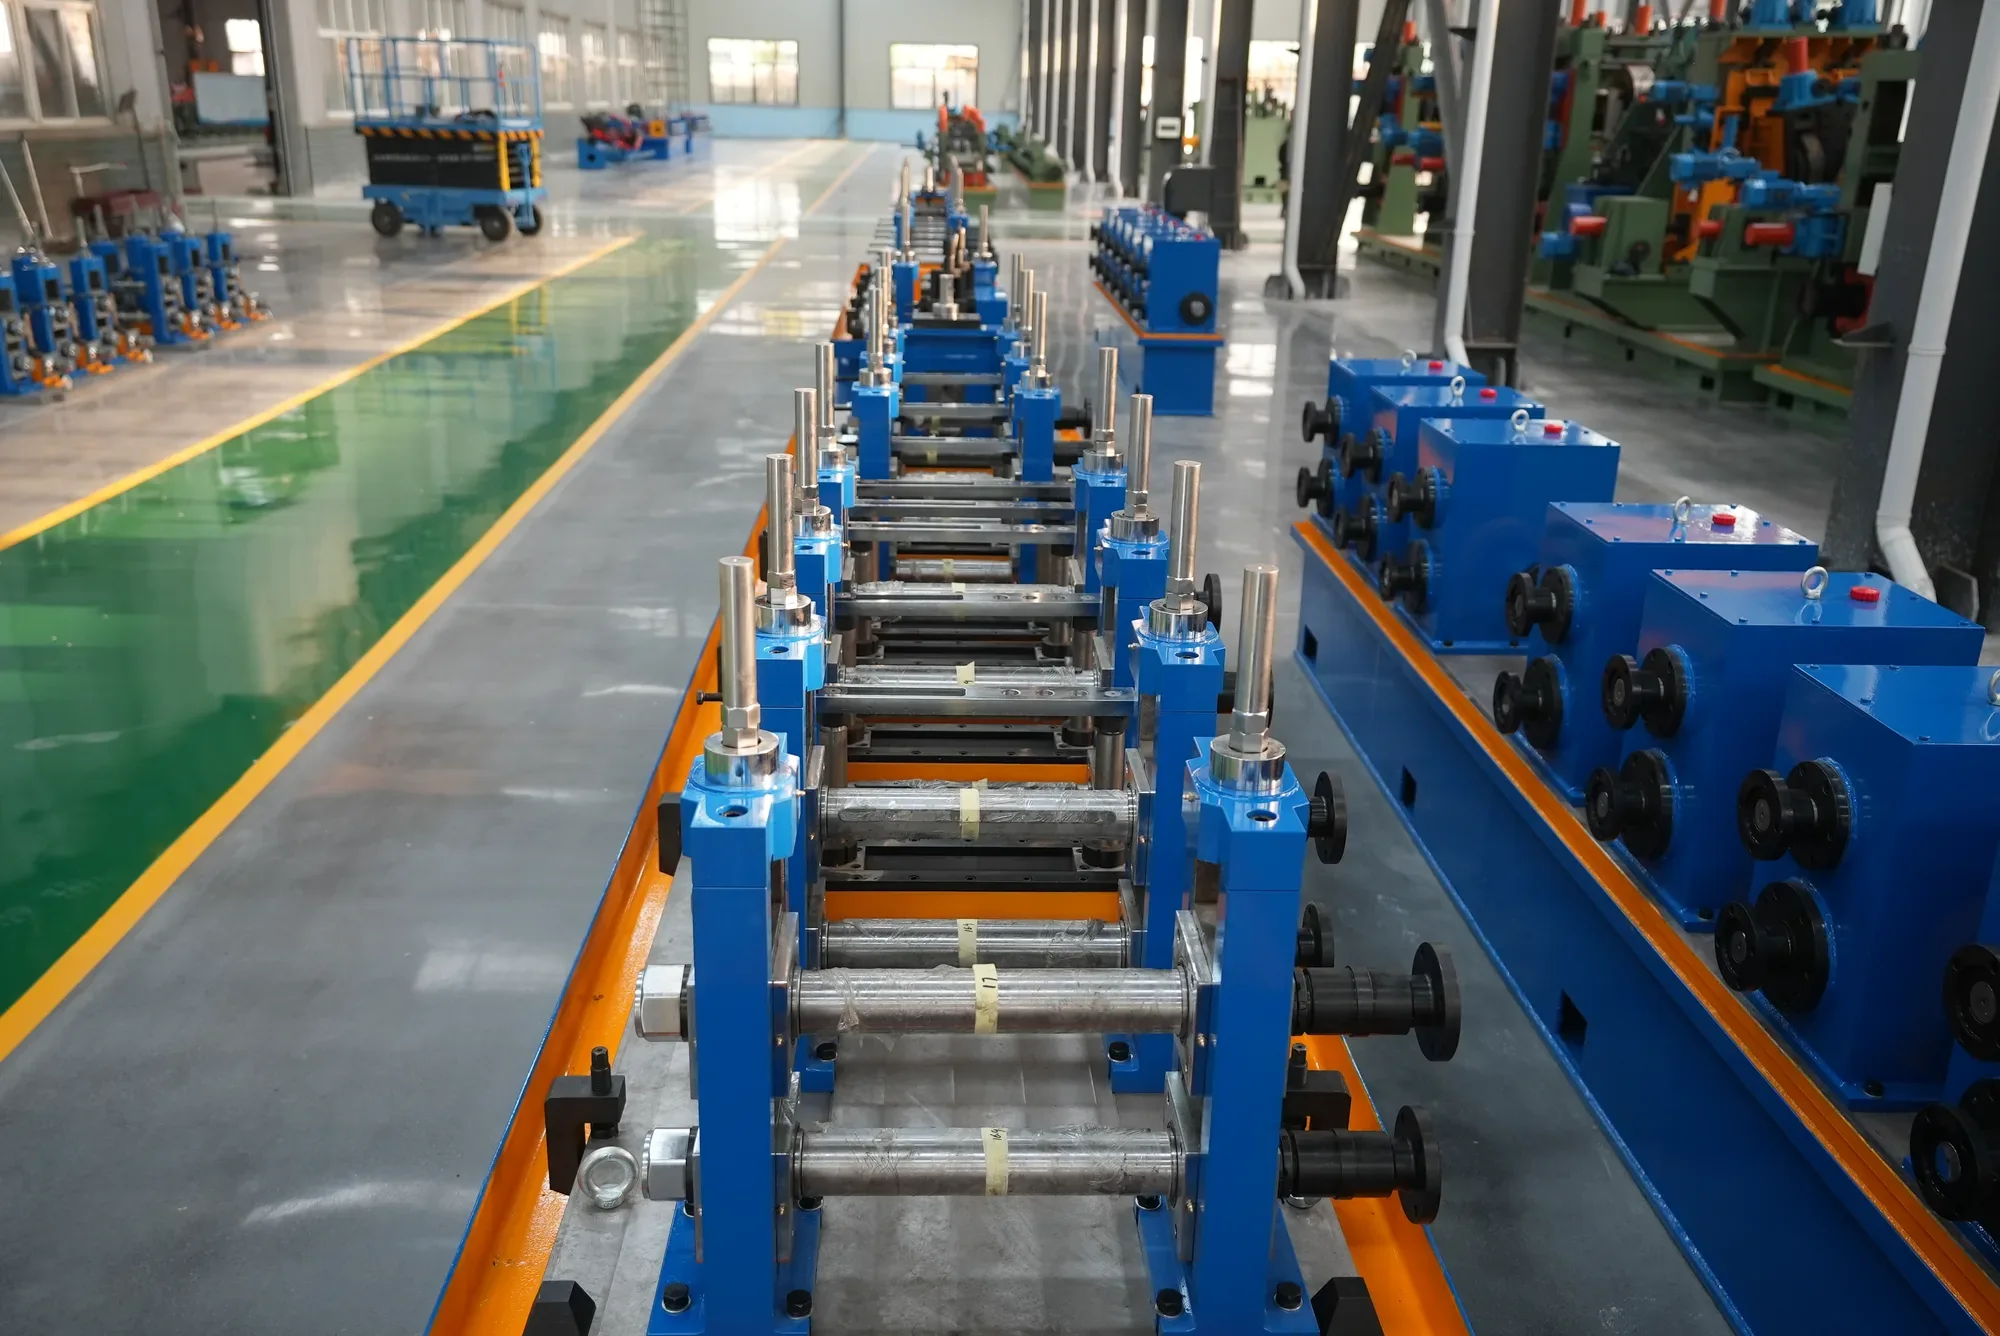
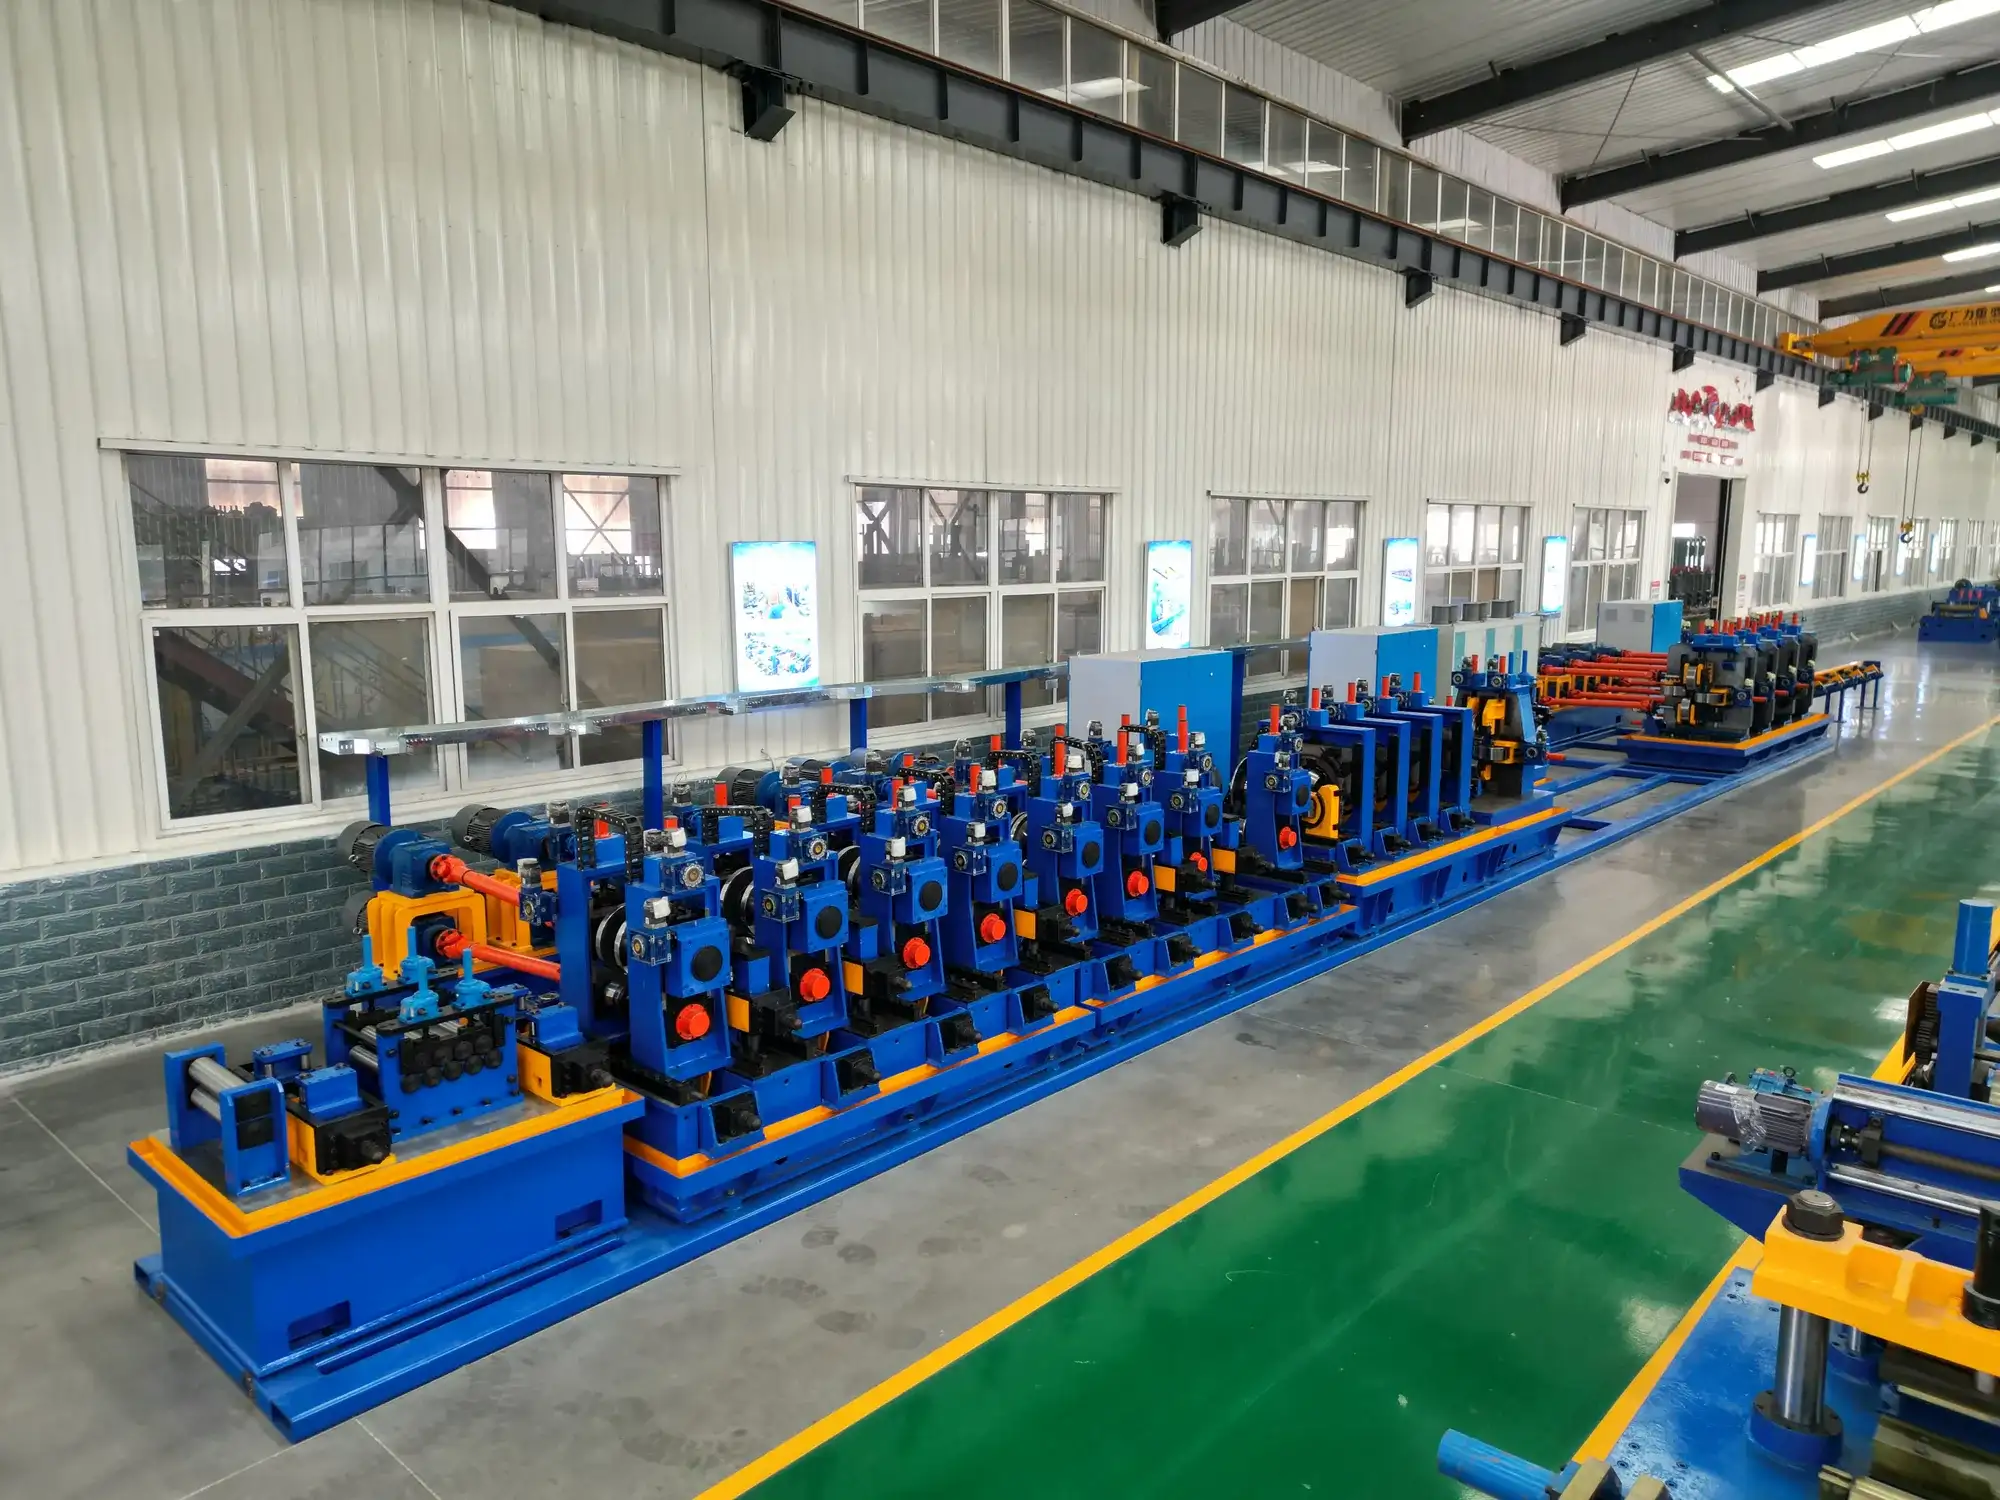
Send Your Enquiry
Tell us the pipe outside-diameter range, the wall thickness and the output you need. An engineer reads every enquiry — it does not land in a general sales inbox.