
 Scan on WeChat
Compare the Mill Types Side by Side
Smallest HFW step, largest HFW step, and the spiral route.
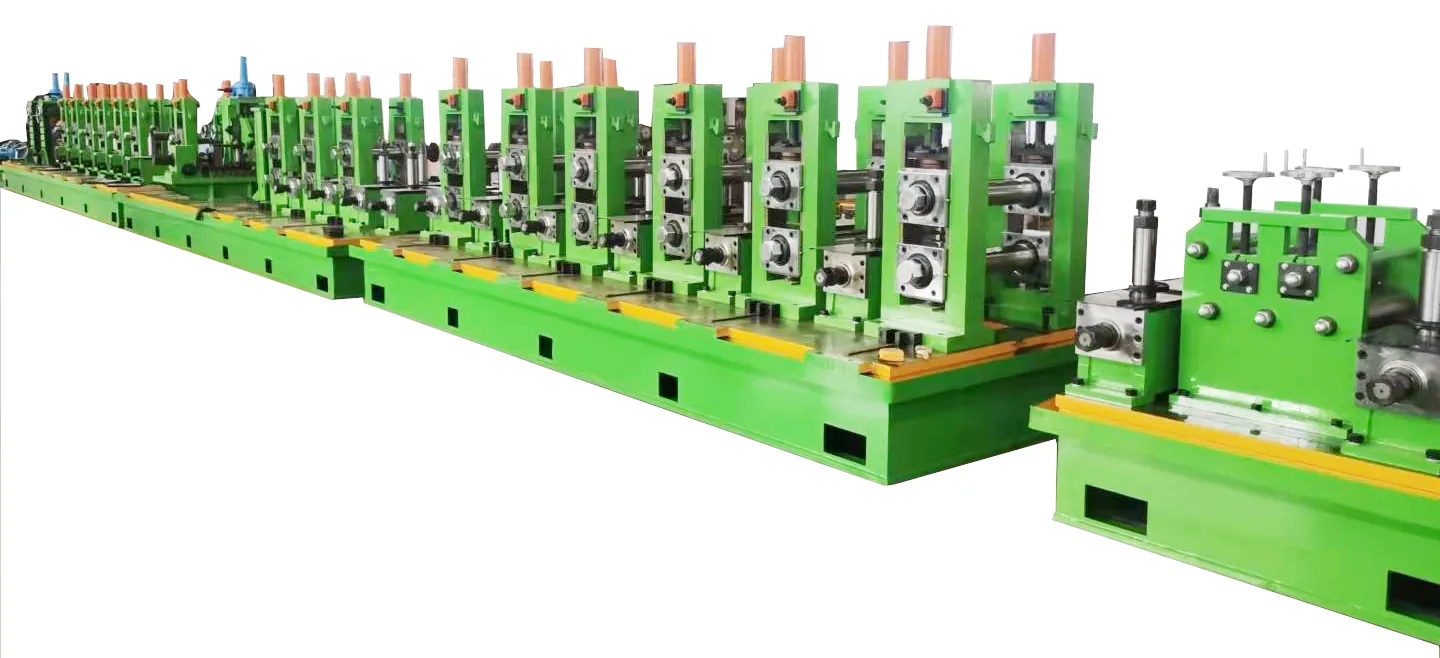
Selection starts with the largest outside diameter the plant intends to sell. That number decides the welding technology; the technology decides the model step, the welder power band and the line layout.
Choosing by Target Outside Diameter
High-frequency longitudinal welding is practical to Φ630 mm; above that, spiral submerged-arc welding is what makes the pipe. Diameter is the first and largest fork in the decision, and it is not a preference — it is a physical boundary.
On the high-frequency side Tengtian builds twelve model steps, HG32 through HG630, and each step covers a diameter band rather than a single size:
HG32 Φ10–32 · HG50 Φ16–50.8 · HG76 Φ12.7–76 · HG89 Φ32–89 · HG114 Φ45–114 · HG165 Φ60–165 · HG219 Φ114–219 · HG273 Φ114–273 · HG325 Φ165–325 · HG426 Φ165–426 · HG508 Φ219–508 · HG630 Φ325–630 (mm) Bands overlap deliberately, so a plant whose product range straddles two steps usually has a real choice —
and that choice is decided by where the volume sits, not by the extreme.
The overlap is worth reading carefully rather than skimming. HG76 covers Φ12.7–76 mm while HG89 starts at Φ32 mm; HG273 covers Φ114–273 mm while HG325 starts at Φ165 mm. A plant whose main product is Φ150 mm can be served by HG165, HG219, HG273 or HG325 — four steps — and the right one is decided by what sits either side of that main product, not by the number itself.
Choosing the step whose band centre is nearest the highest-volume size usually gives the easiest running; choosing the largest step “for headroom” costs money at purchase and again at every changeover.
Wall thickness is the second constraint and it is not independent of diameter. Across the high-frequency range the mills handle 0.5–16 mm; on the spiral side the 820 class runs 3–12 mm and the 1620 class 5–16 mm. A requirement that is thin-wall at large diameter, or heavy-wall at small diameter, narrows the options faster than the diameter alone suggests.
Section shape narrows them further. Round, square and rectangular sections all come off high-frequency lines, and square tube has a dedicated route — direct forming, where size is changed by combined dies instead of by changing rolls and roll consumption falls by more than 90%. Spiral lines make round pipe only. One exception is worth stating: making 100 × 100 mm tube needs the upper roll on the final open stand changed.
On the spiral side there are two machine classes: Φ219–820 mm × 3–12 mm, and Φ219–1620 mm × 5–16 mm. Within a class, diameter is changed by changing the forming angle rather than by changing rolls, which is why one spiral mill covers so wide a band.
A plant that intends to sell line pipe, large-diameter water main or heavy structural section above that ceiling is choosing a spiral mill whether or not it started the search expecting to, and a plant whose whole range sits below it gains nothing from spiral capability it will not use.
Welder Power Band: 150 kW to 1500 kW by Size Class
Welder power is matched to diameter in steps across the range 150–1500 kW. Under-powering gives lack of fusion; over-powering gives burn-through — so the rating is sized to the pipe rather than bought as headroom.
HG630 = 1500 kW. The rating of each intermediate model (HG50 / HG76 / HG89 / HG114 / HG165 / HG219 / HG273 / HG325 / HG426 / HG508) is quoted per
Spiral mills are rated differently: the Φ219–820 class carries a main installed capacity of about 200 kW including welding, and the two classes also differ in welding arrangement — outer-single/inner-single on the 820 class, outer-double/inner-single on the 1620 class.
Publishing an interpolated figure would give a number that is easy to quote and wrong to design against, and a plant that sized its power supply from it would find out at commissioning. So the two endpoints stand as fact and the rest is quoted.
Why the intermediate steps are not published as a table is worth saying plainly, because the absence looks like an omission and is not one. Welder rating is quoted against the actual product mix — diameter band, wall thickness, line speed and duty — rather than read off a model number.
HFW or SSAW for Your Diameter and Application
| HFW — high-frequency longitudinal | SSAW — spiral submerged-arc | |
|---|---|---|
| Diameter range | Φ10–630 mm, 12 model steps (HG32–HG630) | Φ219–820 mm and Φ219–1620 mm, 2 classes |
| Wall thickness | 0.5–16 mm | 3–12 mm (820 class) / 5–16 mm (1620 class) |
| Seam | Straight longitudinal, HF induction, no filler | Helical, automatic submerged arc, inside and out |
| Size change | By changing rolls (or by combined dies on direct-square lines) | By changing forming angle — no roll change |
| Production mode | Continuous | Discontinuous |
| Welding speed | Line runs continuously between coils | 0.5–3 m/min |
| Section shapes | Round, square, rectangular | Round |
| Suits | Higher volume at small and medium diameter | Large diameter, medium batch, heavy wall |
An API line-pipe mill is a high-frequency line plus intermediate-frequency annealing, straightening, end facing, hydrostatic testing, ultrasonic and eddy-current inspection, and covers OD 114–508 mm at 6–24 mm wall by class. Application decides more of this than the equipment list suggests. What comes off these lines goes to fluid conveyance, building structure and scaffolding, machinery and automotive components, furniture tube, solar mounting structures, and long-distance oil and gas transmission line pipe — and the last of those changes the line rather than the paperwork.
Spiral lines carry their own inspection chain and are built against GB/T 9711 and, on the 1620 class, API SPEC 5L.
The overlap band Φ219–630 mm is where both technologies can make the pipe, and it is where most selection conversations actually happen.
Wall thickness often settles it before either argument does — above roughly 12 mm the spiral classes are the ones carrying that range as standard, while thin wall at those diameters is where the longitudinal route stays workable.
Ask an Engineer — Reply Within a Single Contact →
What decides it is batch size, wall thickness and the standard the finished pipe must meet — a spiral line changes diameter without changing rolls, which favours a wide product range in medium batches; a longitudinal line runs continuously between coils, which favours volume in a narrower range.
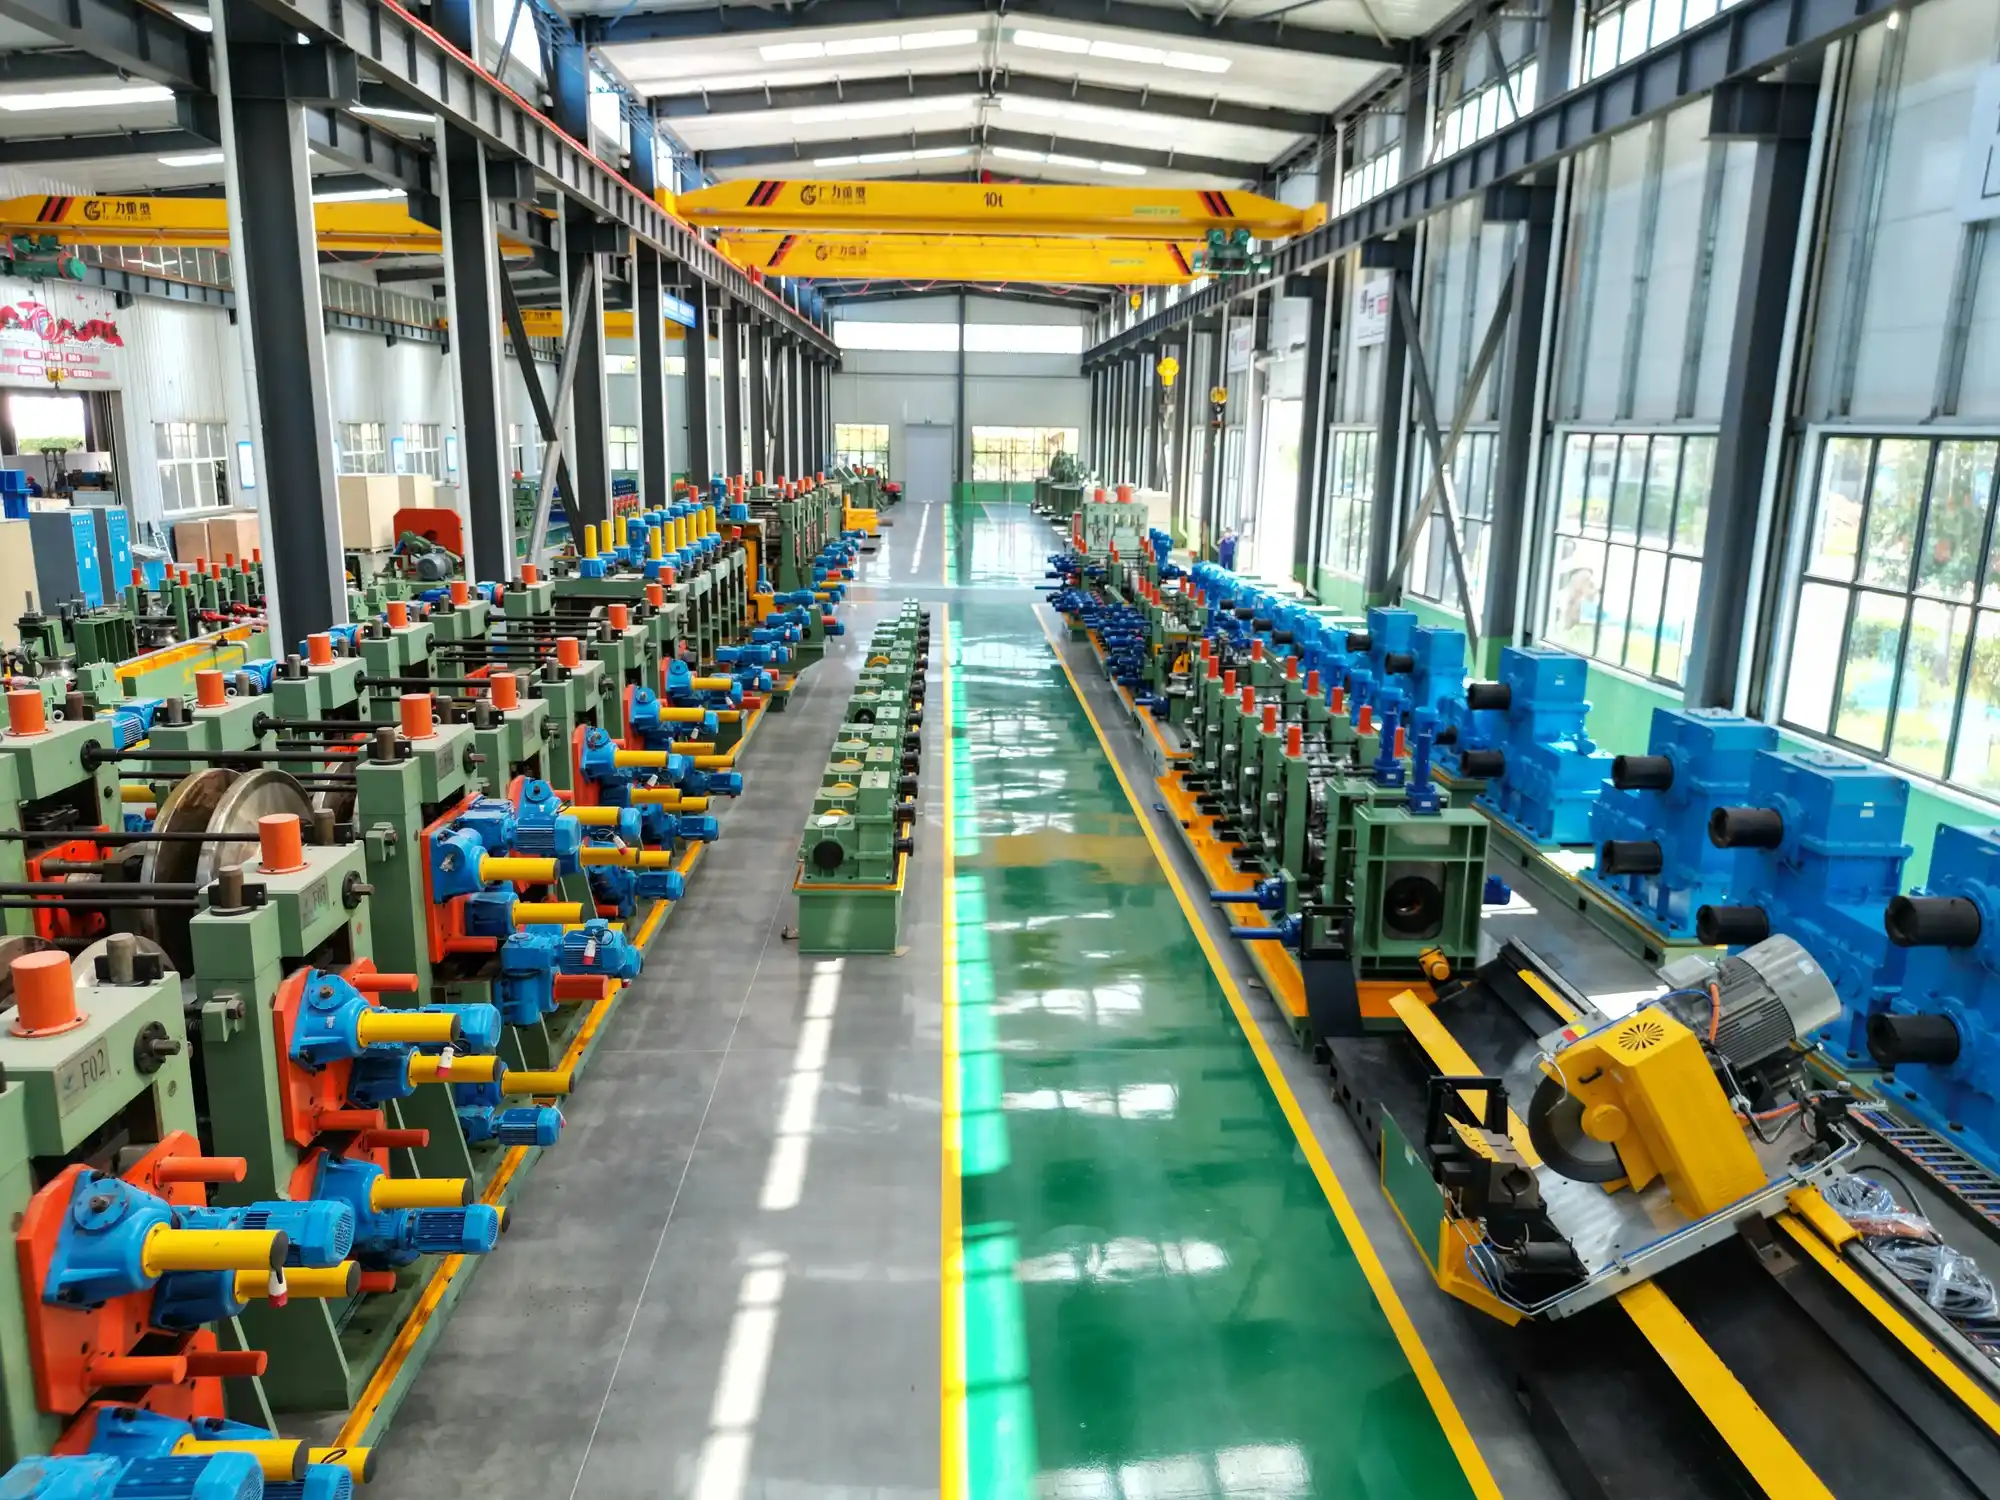
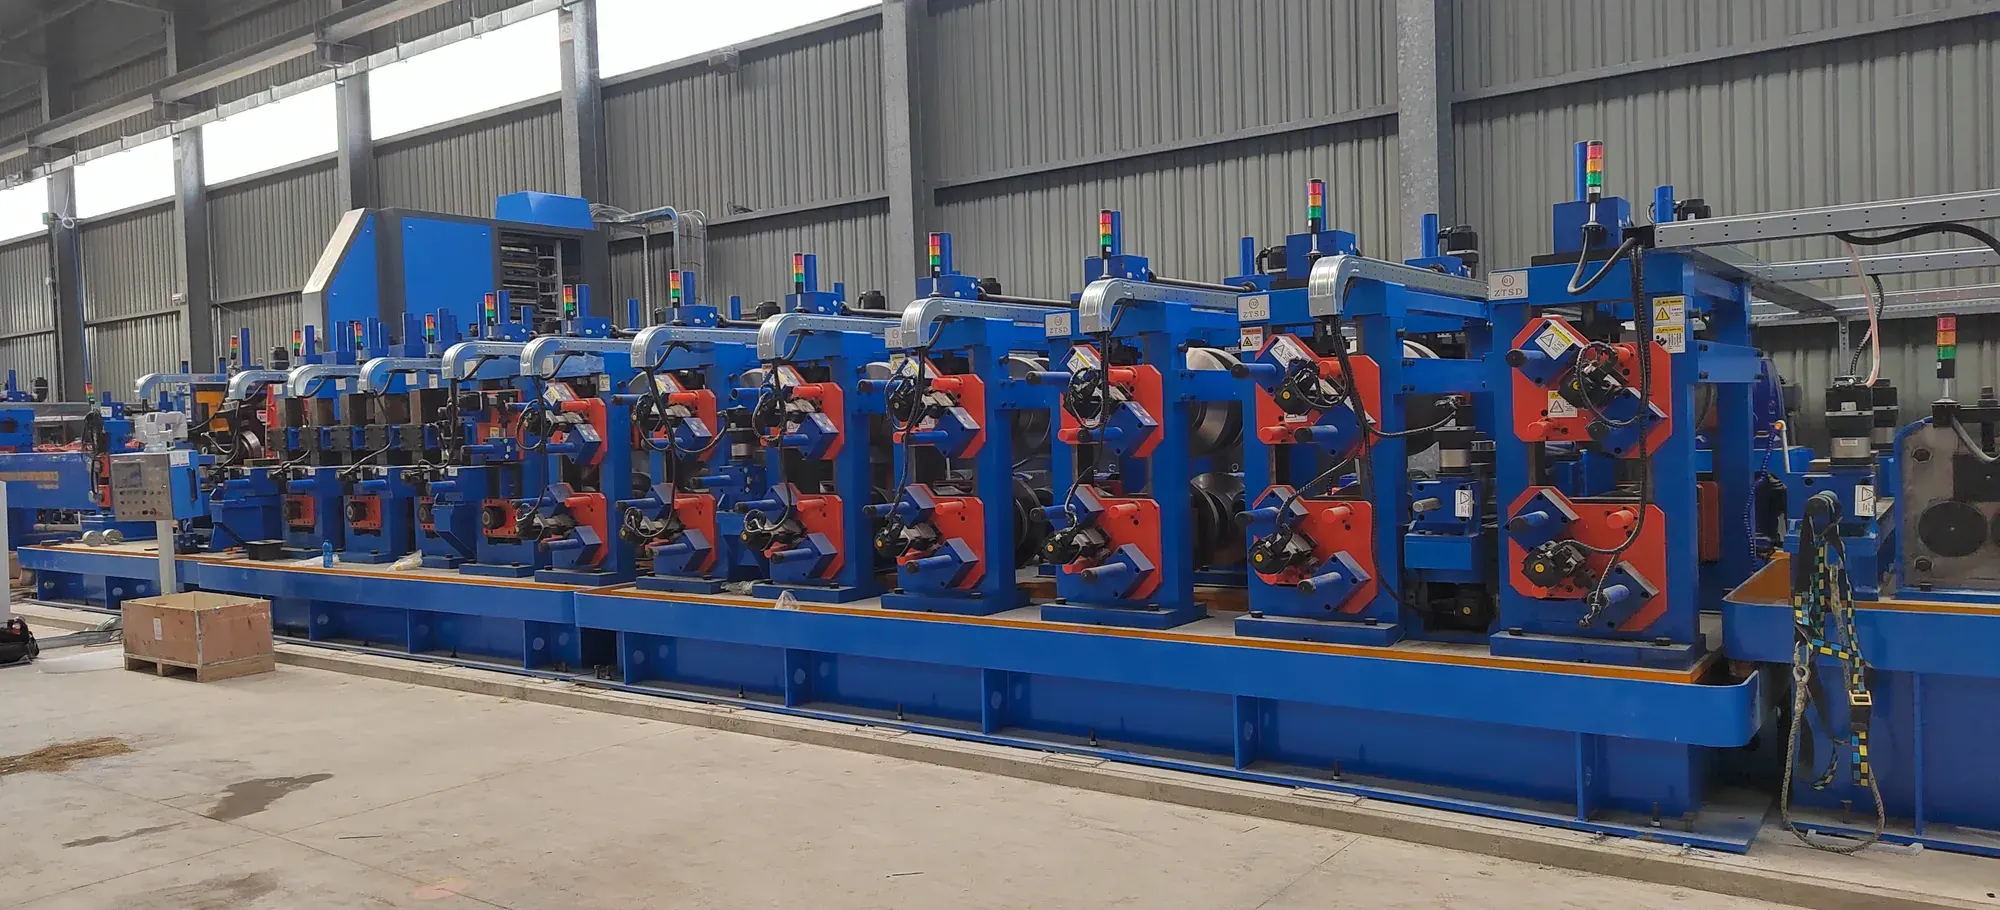
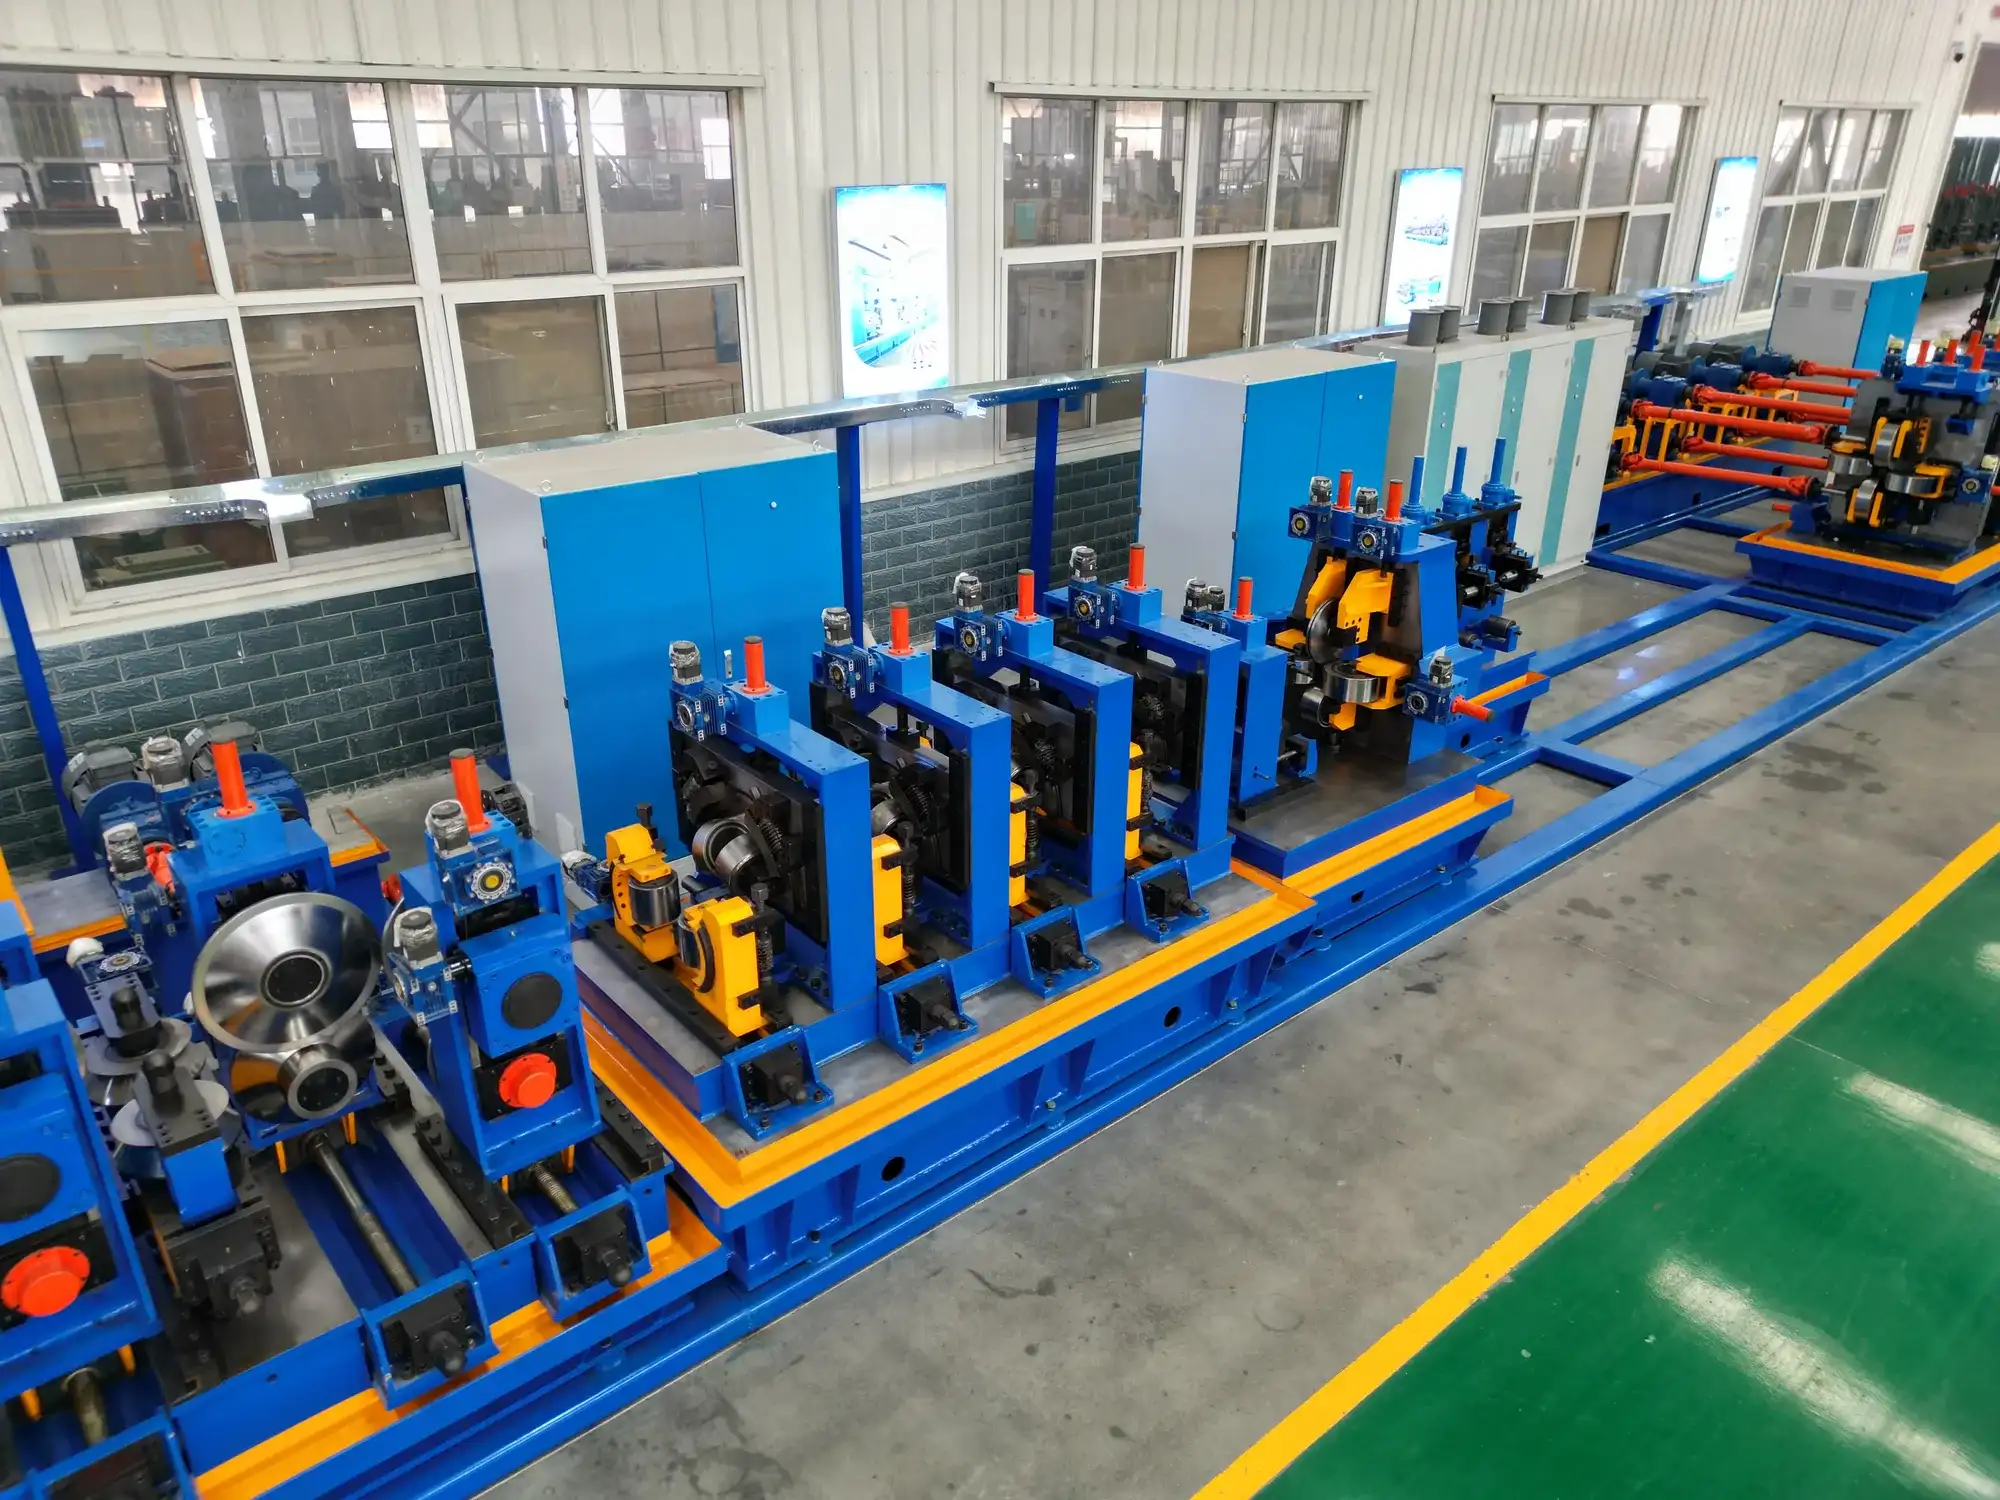
From the Workshop
Send Your Enquiry
Tell us the pipe outside-diameter range, the wall thickness and the output you need. An engineer reads every enquiry — it does not land in a general sales inbox.