
 Scan on WeChat
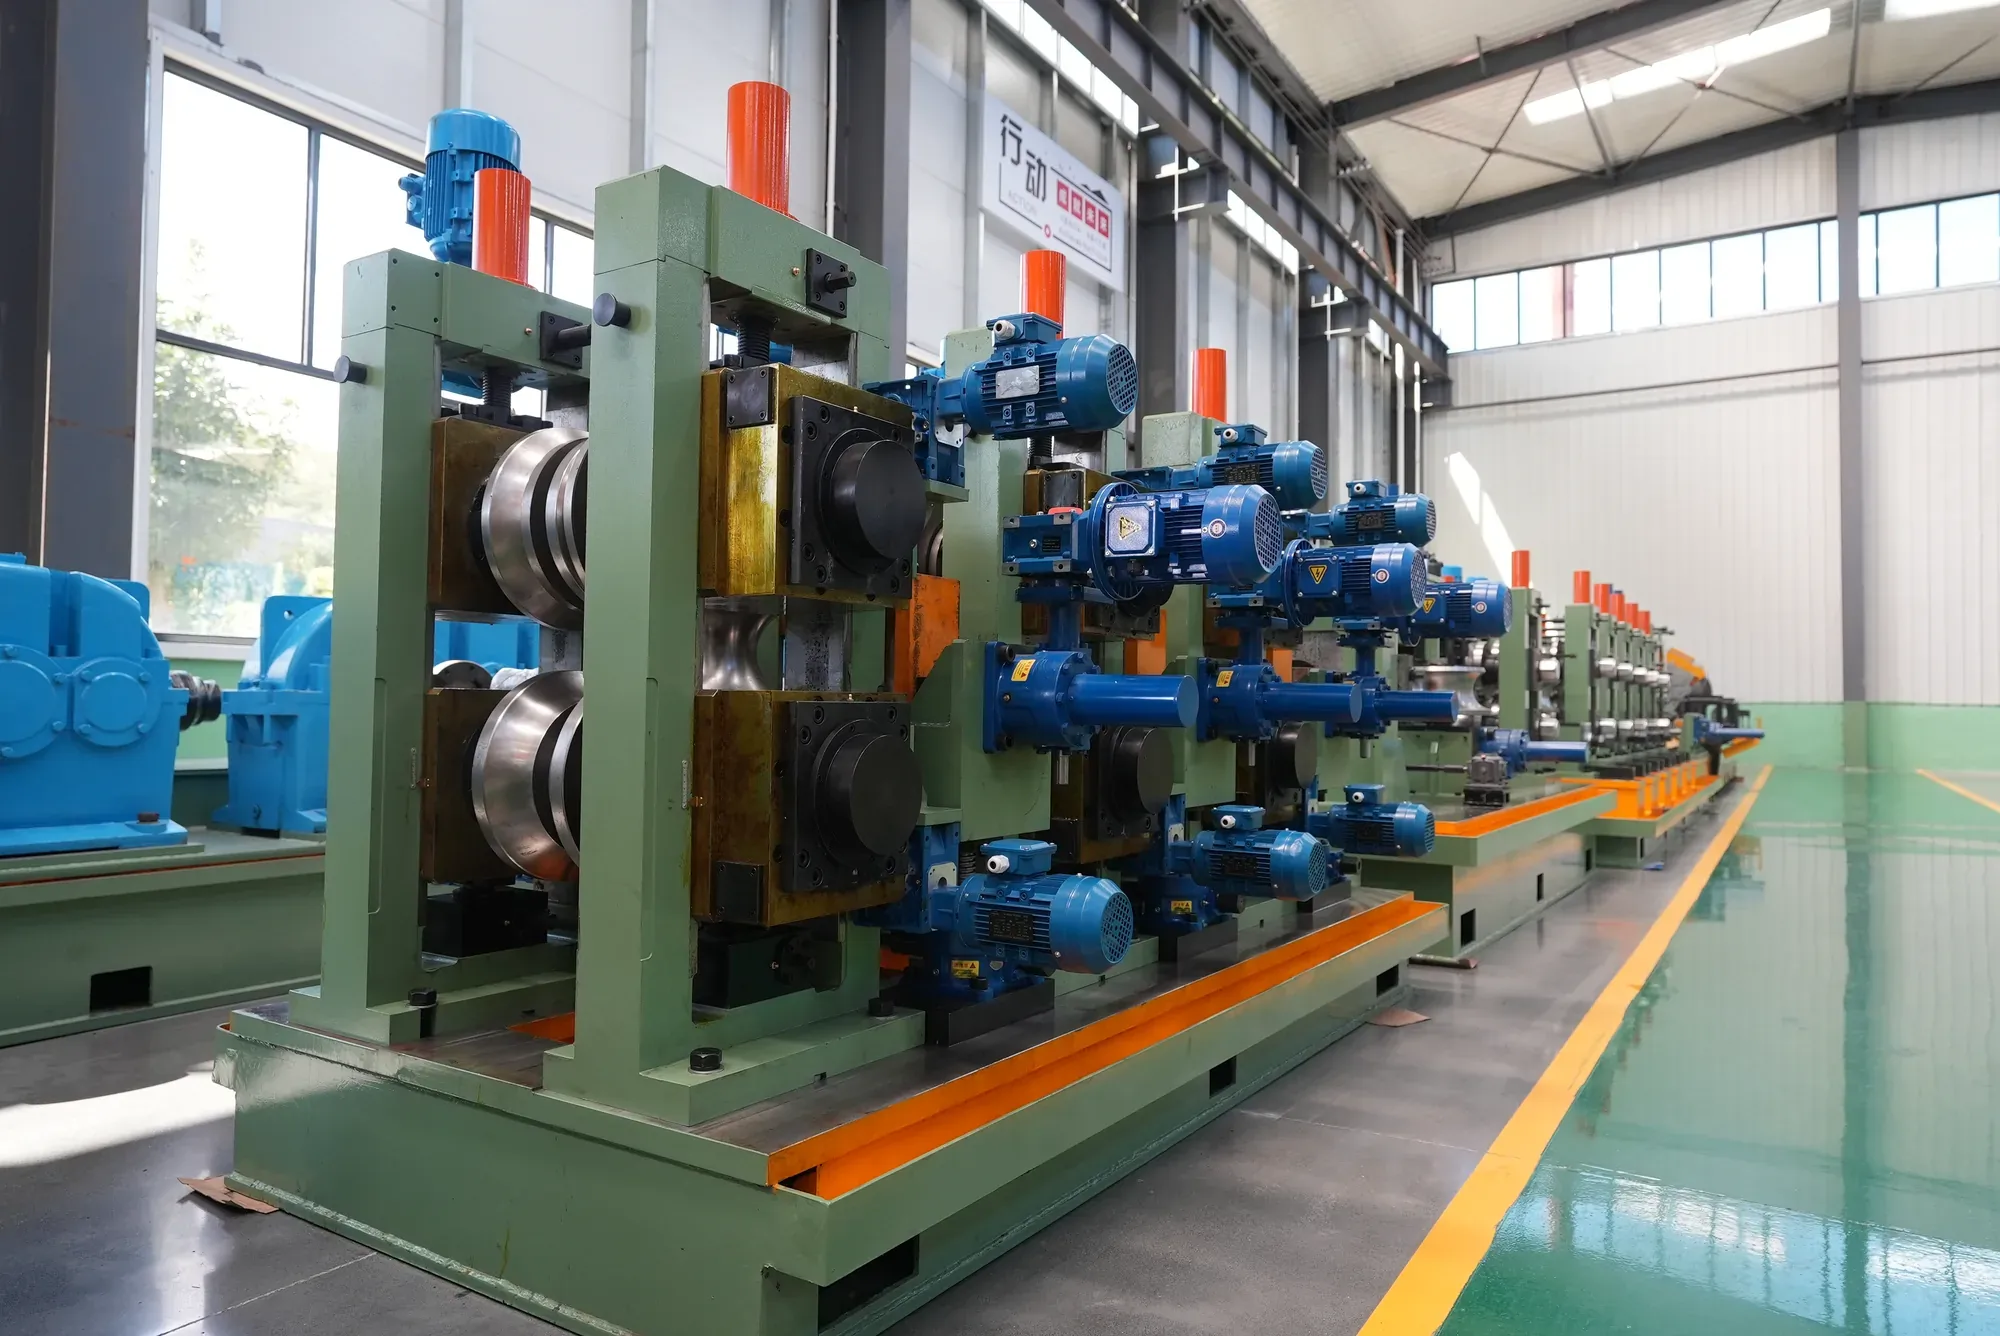
The first question most buyers ask is whether to use seamless or welded pipe, and, if welded, which welding process. The answers below cover what our own equipment does, and go no further.
What Is Welded Pipe Guide
Welded pipe is made by forming strip into a tube and joining the seam. Seamless pipe is made by piercing and rolling a solid billet, with no seam at all. The two are different products from different plants, and what we can speak to is the equipment side.
Our position for high-frequency welding against seamless rolling and UOE/JCOE is specific: lower investment and running cost, higher continuity, suited to medium and small diameter in volume.
Welded Pipe Guide — Range, Configuration and Output
Coverage is Φ10–630 mm across twelve model steps, wall 0.5–16 mm. Tengtian builds lines for two welding processes, and the two lines are genuinely different.
High-frequency welding. Pressure welding: high-frequency current concentrates at the seam through skin and proximity effects, heats the edges to welding temperature, and squeeze rolls press them together. There is no filler metal.
Spiral submerged-arc welding. Strip is fed at an angle and welded in a spiral seam, inside and out, under a flux layer with dedicated welding power sources. Coverage is Φ219–820 mm with wall 3–12 mm on one class and Φ219–1620 mm with wall 5–16 mm on the other.
Key Parameters: Size Range, Wall Thickness, Line Speed and Welder Power Band
| What | High-frequency welded | Spiral submerged-arc |
|---|---|---|
| Seam | Straight, pressure welded, no filler | Spiral, submerged arc, inside and out |
| Outside diameter | Φ10–630 mm, twelve steps | Φ219–820 / Φ219–1620 mm |
| Wall | 0.5–16 mm | 3–12 / 5–16 mm |
| Welding energy | HF welder 150–1500 kW by step | SAW power sources by class |
Line speed and output are available on request on both sides.
How to Choose the Right Model
The first cut is diameter. Below 219 mm, only high-frequency welding is in our range; above 630 mm, only spiral. Between those two numbers both are available, and the choice comes down to the application rather than capability, so we make no default recommendation.
The second cut is what the pipe has to prove. If it has to carry an in-line inspection record — hydrostatic test, ultrasonic, eddy current — that is the API line, built on the tube mill with intermediate annealing, straightening, end facing and the inspection units added.
Scope of Supply, Installation and Commissioning
Certification held is ISO 9001 and CE from UDEM, with certificate numbers given and checkable at the issuing body.
Rolls and key wear parts are machined in-house on our own CNC equipment. The engineering team is twenty people averaging twenty years’ experience; the base is open to factory audit.
What these answers cover
The answers cover what our own equipment does: which process each line uses, what diameter and wall each covers, what the weld is physically, and what inspection can be added and on which line.
They do not cover the comparative performance of pipe made on other manufacturers’ equipment, or the properties of seamless pipe.
The three questions buyers actually bring
Does a welded seam matter for my application? Our answer is procedural rather than promotional: high-frequency welding is a pressure weld with no filler, so seam quality is set by power matching, edge alignment and squeeze at the weld box. Those three are on the equipment side; strip quality and operating practice are on the buyer’s.
How do I prove the pipe? If the order is gated on an inspection record, the API line is the configuration that carries it: intermediate annealing, straightening, end facing, hydrostatic testing, ultrasonic and eddy-current inspection, added on top of the tube mill.
Which standards are in play? The target standards fall into these categories: conventional structural and fluid pipe, API 5L line pipe, GOST H-section and GB. The standards actually named on the equipment side are GB/T 9711 and API SPEC 5L on the spiral and API routes, GOST R 58966-2020 on H-beam, and the company’s own enterprise standard Q/GYLTT01-2023.
Downstream Applications
There are six downstream application categories: fluid transport; building structure and scaffolding; machinery and automotive components; home and furniture; PV mounting; and long-distance oil and gas pipelines.
Who is asking
The buyers who start here rather than with a specific model are the ones still choosing: regional pipe makers building or expanding, and system integrators specifying a plant for someone else. Their triggers are a new plant, a capacity expansion, entry into a new product type, or a new standard market.
Certification, and what each certificate actually covers
ISO 9001 is held under certificate number 18524Q11269R2S, issued by National Standard Integration (Beijing) Certification Co., Ltd. under IAF MLA and CNAS accreditation.
CE certificates are held from UDEM under three separate numbers, and each covers a different line type: welded pipe equipment under M.2022.206.C72171, cold roll forming equipment under M.2022.206.C72172, and slitting lines under M.2022.206.C72173. A fourth CE certificate for cold forming is held from Ente Certificazione Macchine in Italy under 0P250616.HTWTT37.
Each number can be checked at the issuing body rather than taken on trust, which is why we publish numbers and verification routes instead of certificate images.
An enterprise standard, Q/GYLTT01-2023 for HGF150 high-frequency welded pipe equipment, is published on the national enterprise-standard platform. High-Tech Enterprise certificate GR202413001148 is held. The Madrid international trademark for TENGTIAN is registered under number 1 707 606. The patent portfolio is 30 granted utility model patents, with 7 invention patents applied for.
Delivery, payment and after-sales
Lines are dismantled into units and shipped in containers: heavy frames braced bare on cradles with designated lifting points and rust protection, precision and wear items in moisture-protected wooden cases with a spare-parts pack. Delivery takes 50 to 90 days.
Installation and commissioning are part of the supply rather than a separate quotation, backed by on-site dispatch and round-the-clock online support. There is a single point of contact and the response time is under one hour. Payment is staged — 30 per cent deposit, 70 per cent before shipment — with third-party escrow and multiple trade terms available.
Anonymised reference deliveries
Our lines are running in more than a dozen countries — mostly on construction tube, and also on fire-extinguisher tube, furniture tube and other sections. Delivery cards show region and model or size; commissioning dates are available on request.
What high-frequency welding physically is
Three process principles explain why the seam behaves the way it does.
Roll forming: forming rolls rotate continuously and press the strip, bending a flat band progressively into an open round or square tube blank. Pass count, roll gap and roll profile decide shape accuracy and seam alignment.
Skin and proximity effect: high-frequency current concentrates at the open edges of the blank because of these two effects, heating exactly that line to welding temperature. Current frequency, power and welding speed decide whether the heating stays concentrated, and what it costs.
Pressure welding: the two heated edges are pressed together by squeeze rolls into a continuous seam. Squeeze amount, temperature and alignment decide fusion quality and pressure rating. Then cooling, sizing and straightening bring the tube to final dimension and straightness.
That third principle is the one that answers the seamless question directly. A high-frequency weld is made by pressing heated parent metal together — there is no filler and no weld deposit — which is a different kind of joint from an arc weld with consumable.
Where an inspection record comes from
If the buyer’s requirement is a document rather than a dimension, the relevant line is the API configuration, and its inspection chain is stage by stage: medium-frequency annealing, straightening, end facing, hydrostatic test, ultrasonic and eddy current.
Two of those do different jobs. Post-weld medium-frequency annealing heats the weld zone and lets it cool naturally, improving the metallurgical structure and toughness of the weld and heat-affected zone. Hydrostatic, ultrasonic and eddy-current testing then inspect seam and body in line and judge each pipe against the standard.
Standards status
API 5L is mandatory for line-pipe orders, and the equipment side is ready — annealing, hydrostatic testing, UT and ECT. Certification of the finished pipe is handled under the pipe maker’s own quality system. For North America, ASTM specifications are the usual reference. GOST R 58966-2020 is mandatory for Russian and CIS H-section orders.
For the machinery itself, no single mandatory certification applies — the requirement follows the destination market’s machinery-safety rules plus whatever standard the finished pipe must meet.
Checking a quotation against these answers
Three checks turn the material above into something you can use on a supplier’s offer.
Check which process the offer is for, and read the diameter and wall against that process’s own window rather than against a general one — Φ10–630 mm with wall 0.5–16 mm for high frequency, Φ219–820 or Φ219–1620 mm with wall 3–12 or 5–16 mm for spiral.
Check whether the offer includes post-weld treatment and inspection, because that is the difference between a tube mill and an API line rather than an option on the same machine.
Check what is claimed about certification, and separate equipment readiness from factory certification — the first is a specification, the second is a document held by the plant.
Whichever process is chosen, the delivery pattern is the same. Export packing is specified per item, with control cabinets, impeders and coils, rolls and cutting tools in moisture-protected wooden cases and heavy frames braced bare on cradles with designated lifting points.
More from the knowledge base
More on this line — specifications, model steps and photographs.
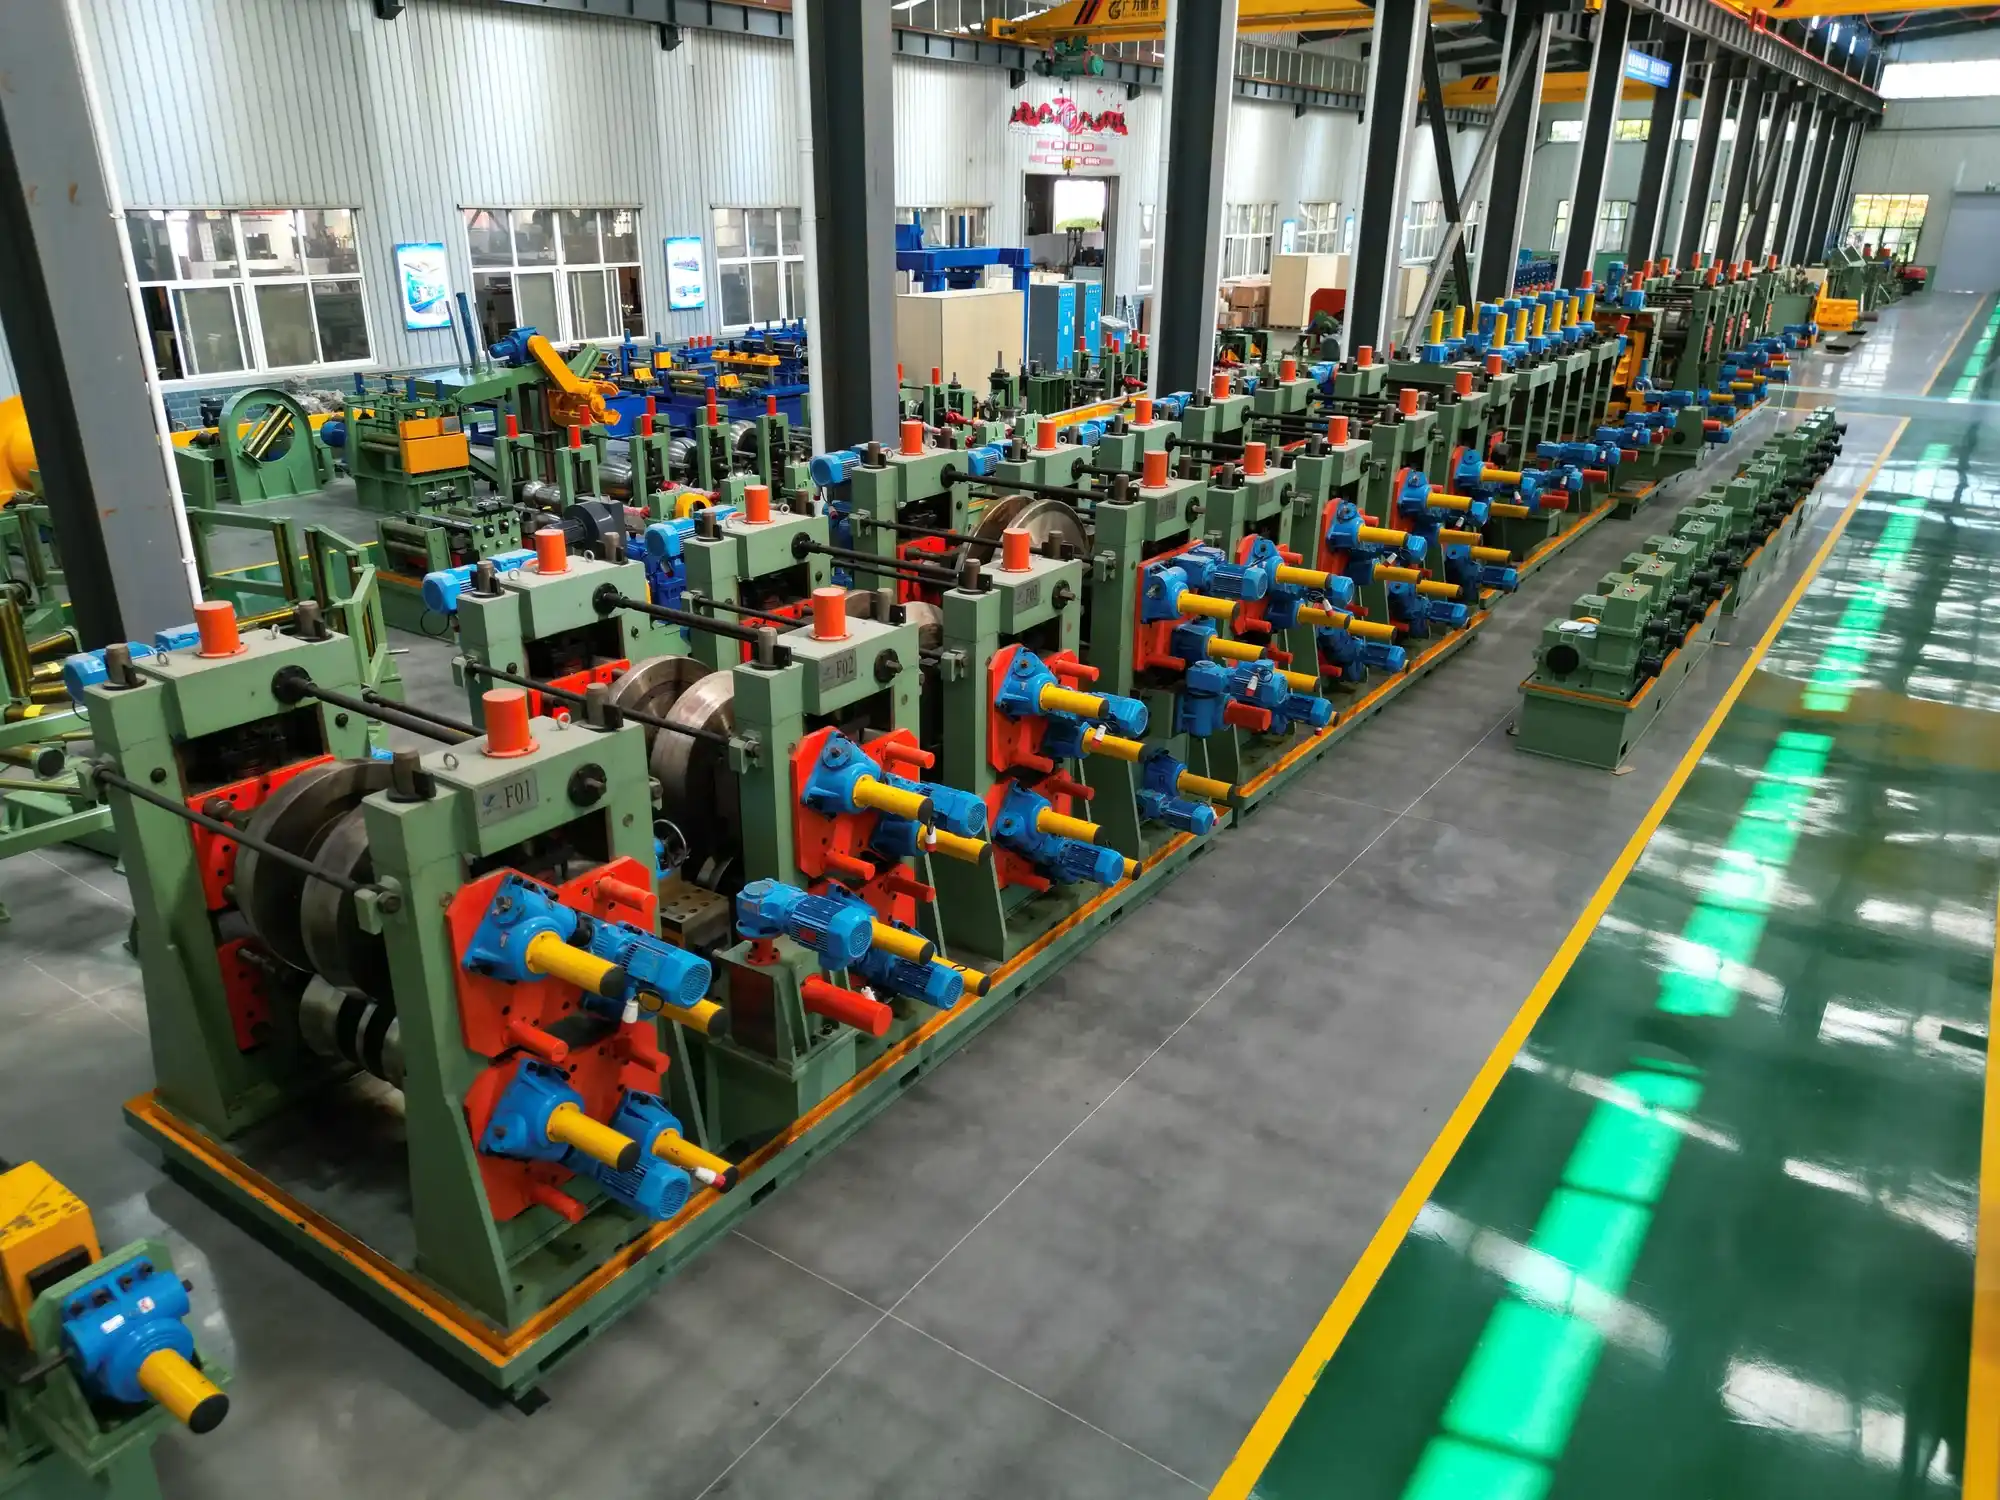
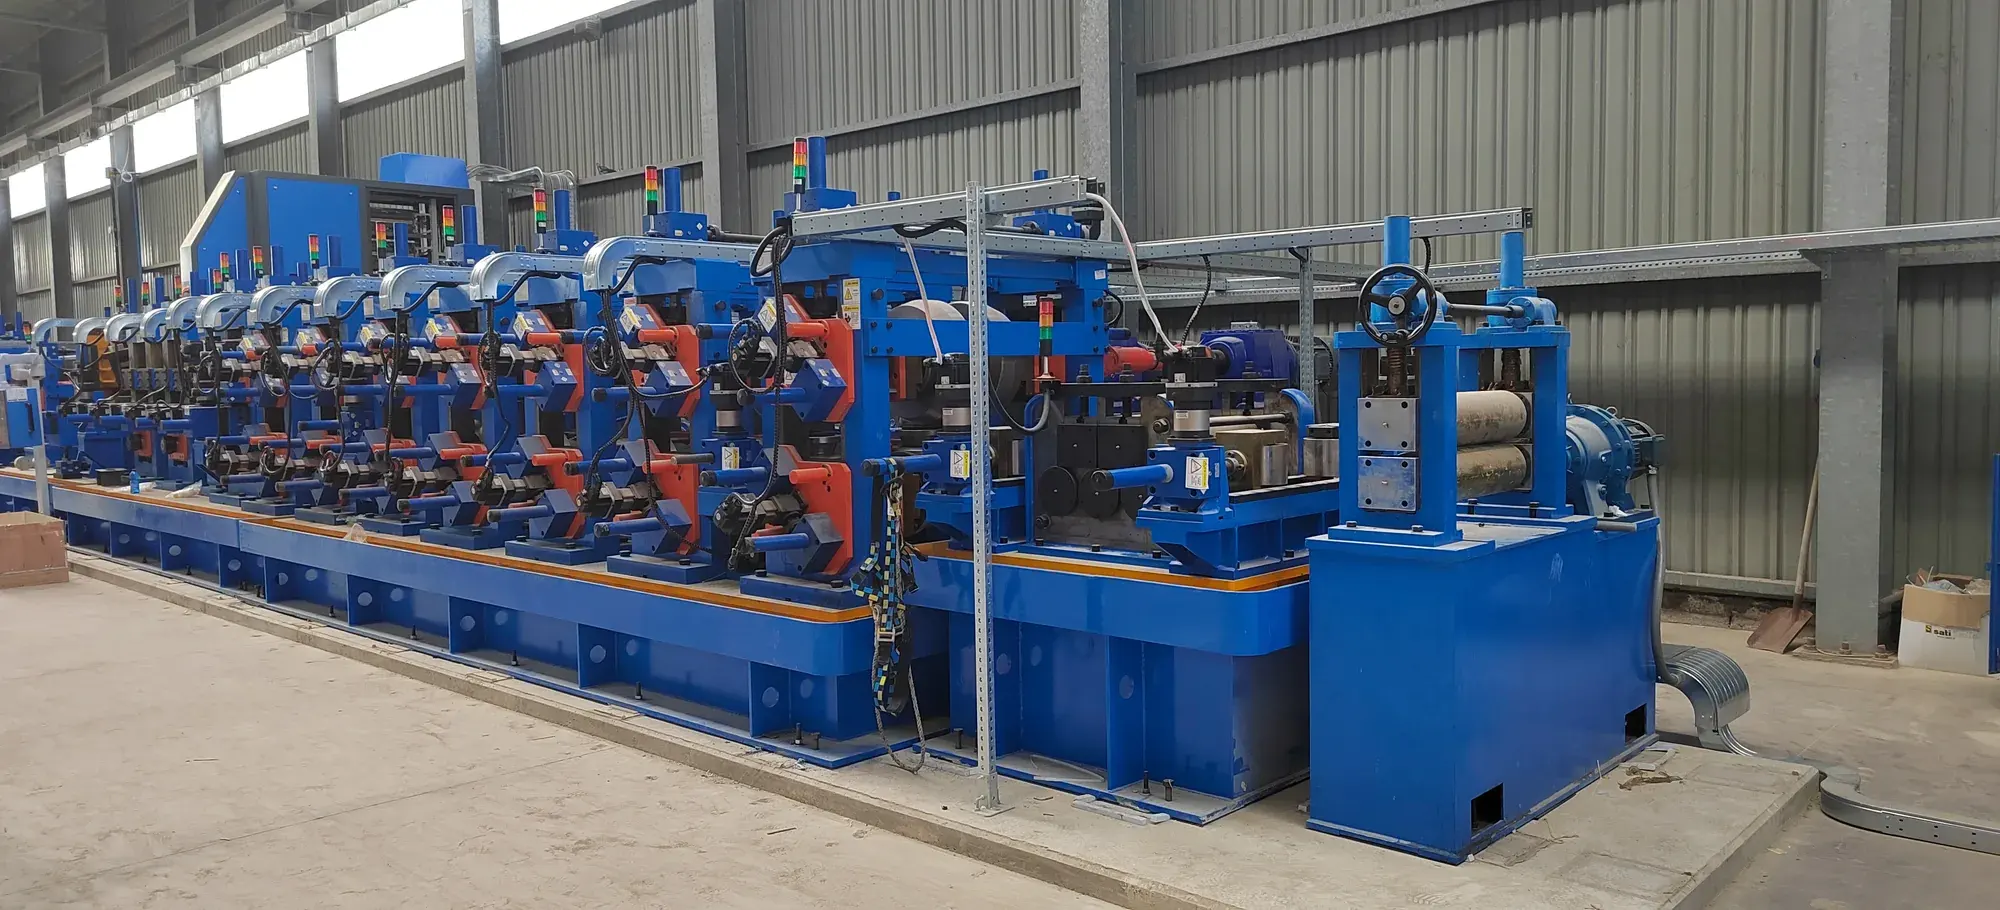
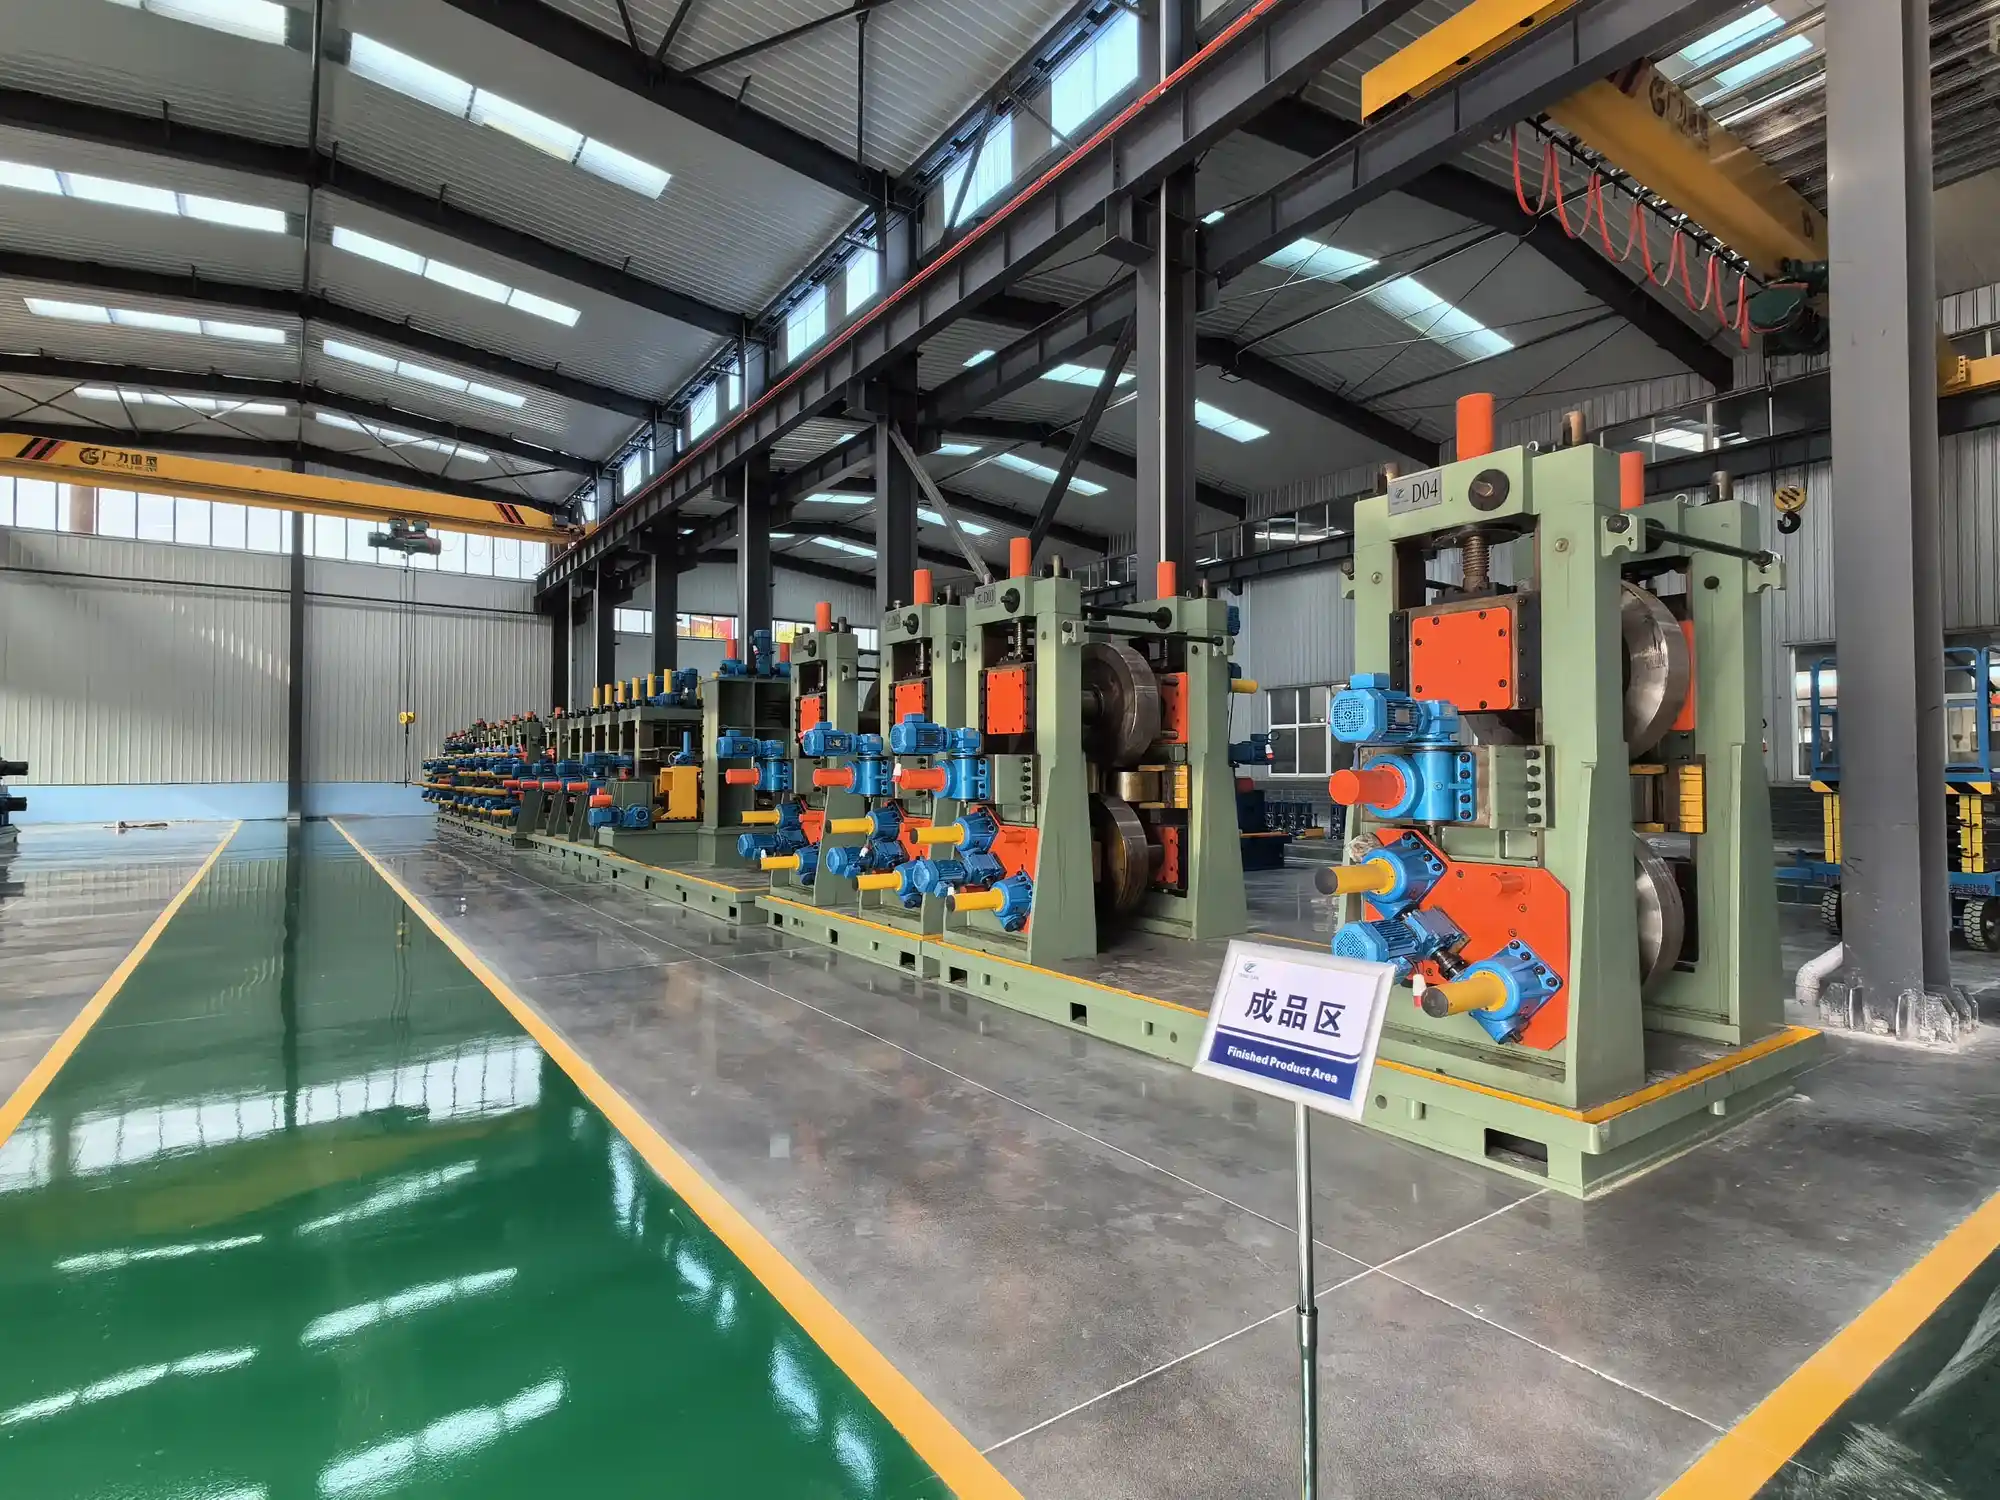
From the Workshop
Send Your Enquiry
Tell us the pipe outside-diameter range, the wall thickness and the output you need. An engineer reads every enquiry — it does not land in a general sales inbox.