
 Scan on WeChat
Home › Tube Mill Rolls and Spares › What Wears and What Gets Replaced
Different welded-pipe lines wear out different parts.
Quick Contact
Hebei TengtianYuanle@tentubemill.com
+86-311-83025332
WhatsApp +852 5425 3155
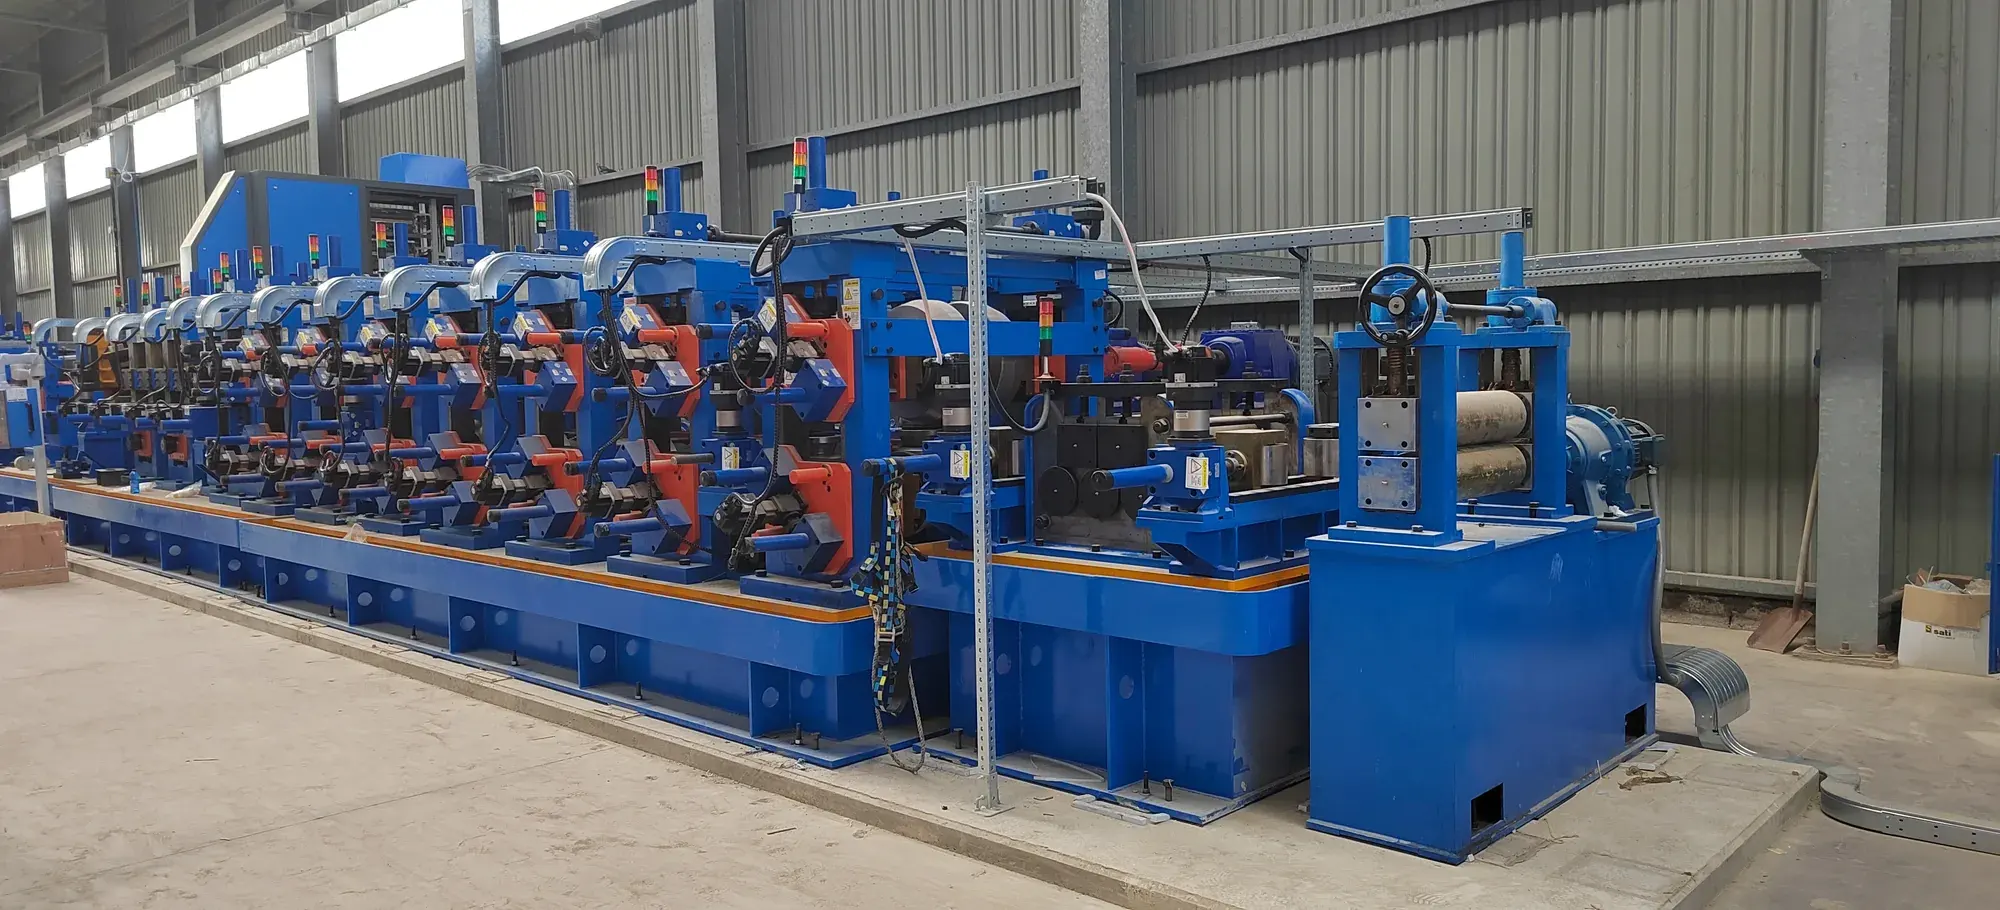
High-frequency mills consume impeders, coils and saw blades; spiral submerged-arc mills consume wire, flux, plasma tips and milling inserts. Rolls are machined in-house on every line we build.
Technical Specification Table
The only useful way to table this subject is by line, because a part that is a consumable on one line does not exist on another. The parts list below follows that order.
- HIGH-FREQUENCY WELDED PIPE LINE (HFW tube mill)
- Saw blades and cutting tools — consumed against cutting volume; supplied continuously, normally with an initial set on the line.
- Induction coil and impeder — wear items, replaced against welding hours; they concentrate the high-frequency current at the seam.
- Cooling water and emulsion — process media for post-weld cooling and forming lubrication; purchased locally to our specification.
- Hydraulic oil and grease — replaced on a maintenance interval; specification from us, purchase local.
- Forming and sizing rolls — a wear replacement item rather than a consumable, backed by in-house CNC capacity; a change-size roll set is supplied with the line. There is no welding wire and no flux on this line. High-frequency welding joins the two heated edges by pressure between squeeze rolls; no filler metal is added.
- SPIRAL SUBMERGED-ARC LINE (SSAW)
- Submerged-arc welding wire — the filler metal for inner and outer seam welding, consumed against welded tonnage; two wire reels are supplied with the line.
- Submerged-arc flux, with drying, magnetic separation and recovery — forms the slag and gas shield over the weld pool and takes part in the metallurgy; a drying and magnetic separation system plus a recovery unit are supplied with the line, while the flux itself is purchased locally to our specification.
- Plasma cutting tips and electrodes, LGK-200 and LGK-160 — consumed by the flying cutter that cuts pipe to length.
- Edge-milling inserts and Ф500 cutter head — they cut the bevel on both strip edges and therefore decide joint gap and weld quality directly.
- Forming, pressure, pre-bending and levelling rolls — pressure rolls in GCr15 hardened to HRC 56-60; pinch, straightening, vertical and pre-bending rolls in 42CrMo hardened to HRC 52-58. Because diameter is changed by changing the forming angle rather than the rolls, roll consumption on this line is lower than on a longitudinal mill.
- Facing and chamfering tools with clamping dies — twelve die sets and two single-head tool posts are supplied.
- Ultrasonic probes and reference blocks — the reference block carries Φ1.6 and Φ3.2 radial through-holes, an N5 rectangular notch and a Φ6 flat-bottom hole; the line is configured with 32 body channels and 8 weld channels.
- X-ray tube and cooler parts, XL-225HP/11 and XL-2 — life items replaced against cumulative exposure time.
- PURLIN ROLL FORMING LINE
- Forming rolls, and punching dies and cutters in Cr12 — dies are reground or replaced against punch count; a set is supplied with the line.
- API LINE-PIPE LINE
- NDT couplant and calibration blocks — replenished against inspection volume.
- SLITTING AND CUT-TO-LENGTH LINE
- Slitting knives, spacers, rubber sleeves and separator discs — configured to strip thickness, and the parts that hold slit width to ±0.2 mm and burr to 4% of thickness.
Line Configuration and Scope of Supply
Supplied with the line as standard: an initial set of saw blades on a tube mill; a change-size roll set on a tube mill; two wire reels, a flux drying and magnetic separation system and a flux recovery unit on a spiral line; twelve clamping die sets and two single-head tool posts on the facing machine; a die and cutter set on a purlin line;
and the probe and reference-block set that comes with the ultrasonic unit.
Available as an optional spares pack rather than standard: impeders and induction coils on a tube mill, plasma tips and electrodes on a spiral line, and milling inserts for the edge miller.
Purchased locally to our specification rather than supplied by us: cooling water and emulsion, hydraulic oil and grease, and the submerged-arc flux itself. We supply the specification and the handling system; the medium is sourced near the plant.
Some of these parts arrive with the line and some do not, and the difference is worth knowing before commissioning rather than after.
Size Change, Roll Wear and Running Cost
On a direct-forming square build, a combined die set is adjusted by servo and the roll saving is above 90%, because contact is point contact rather than full face. Rolls are the item buyers ask about most, and the answer that matters is about availability rather than about life. There is one exception: making 100 × 100 mm tube needs the upper roll on the final open stand changed.
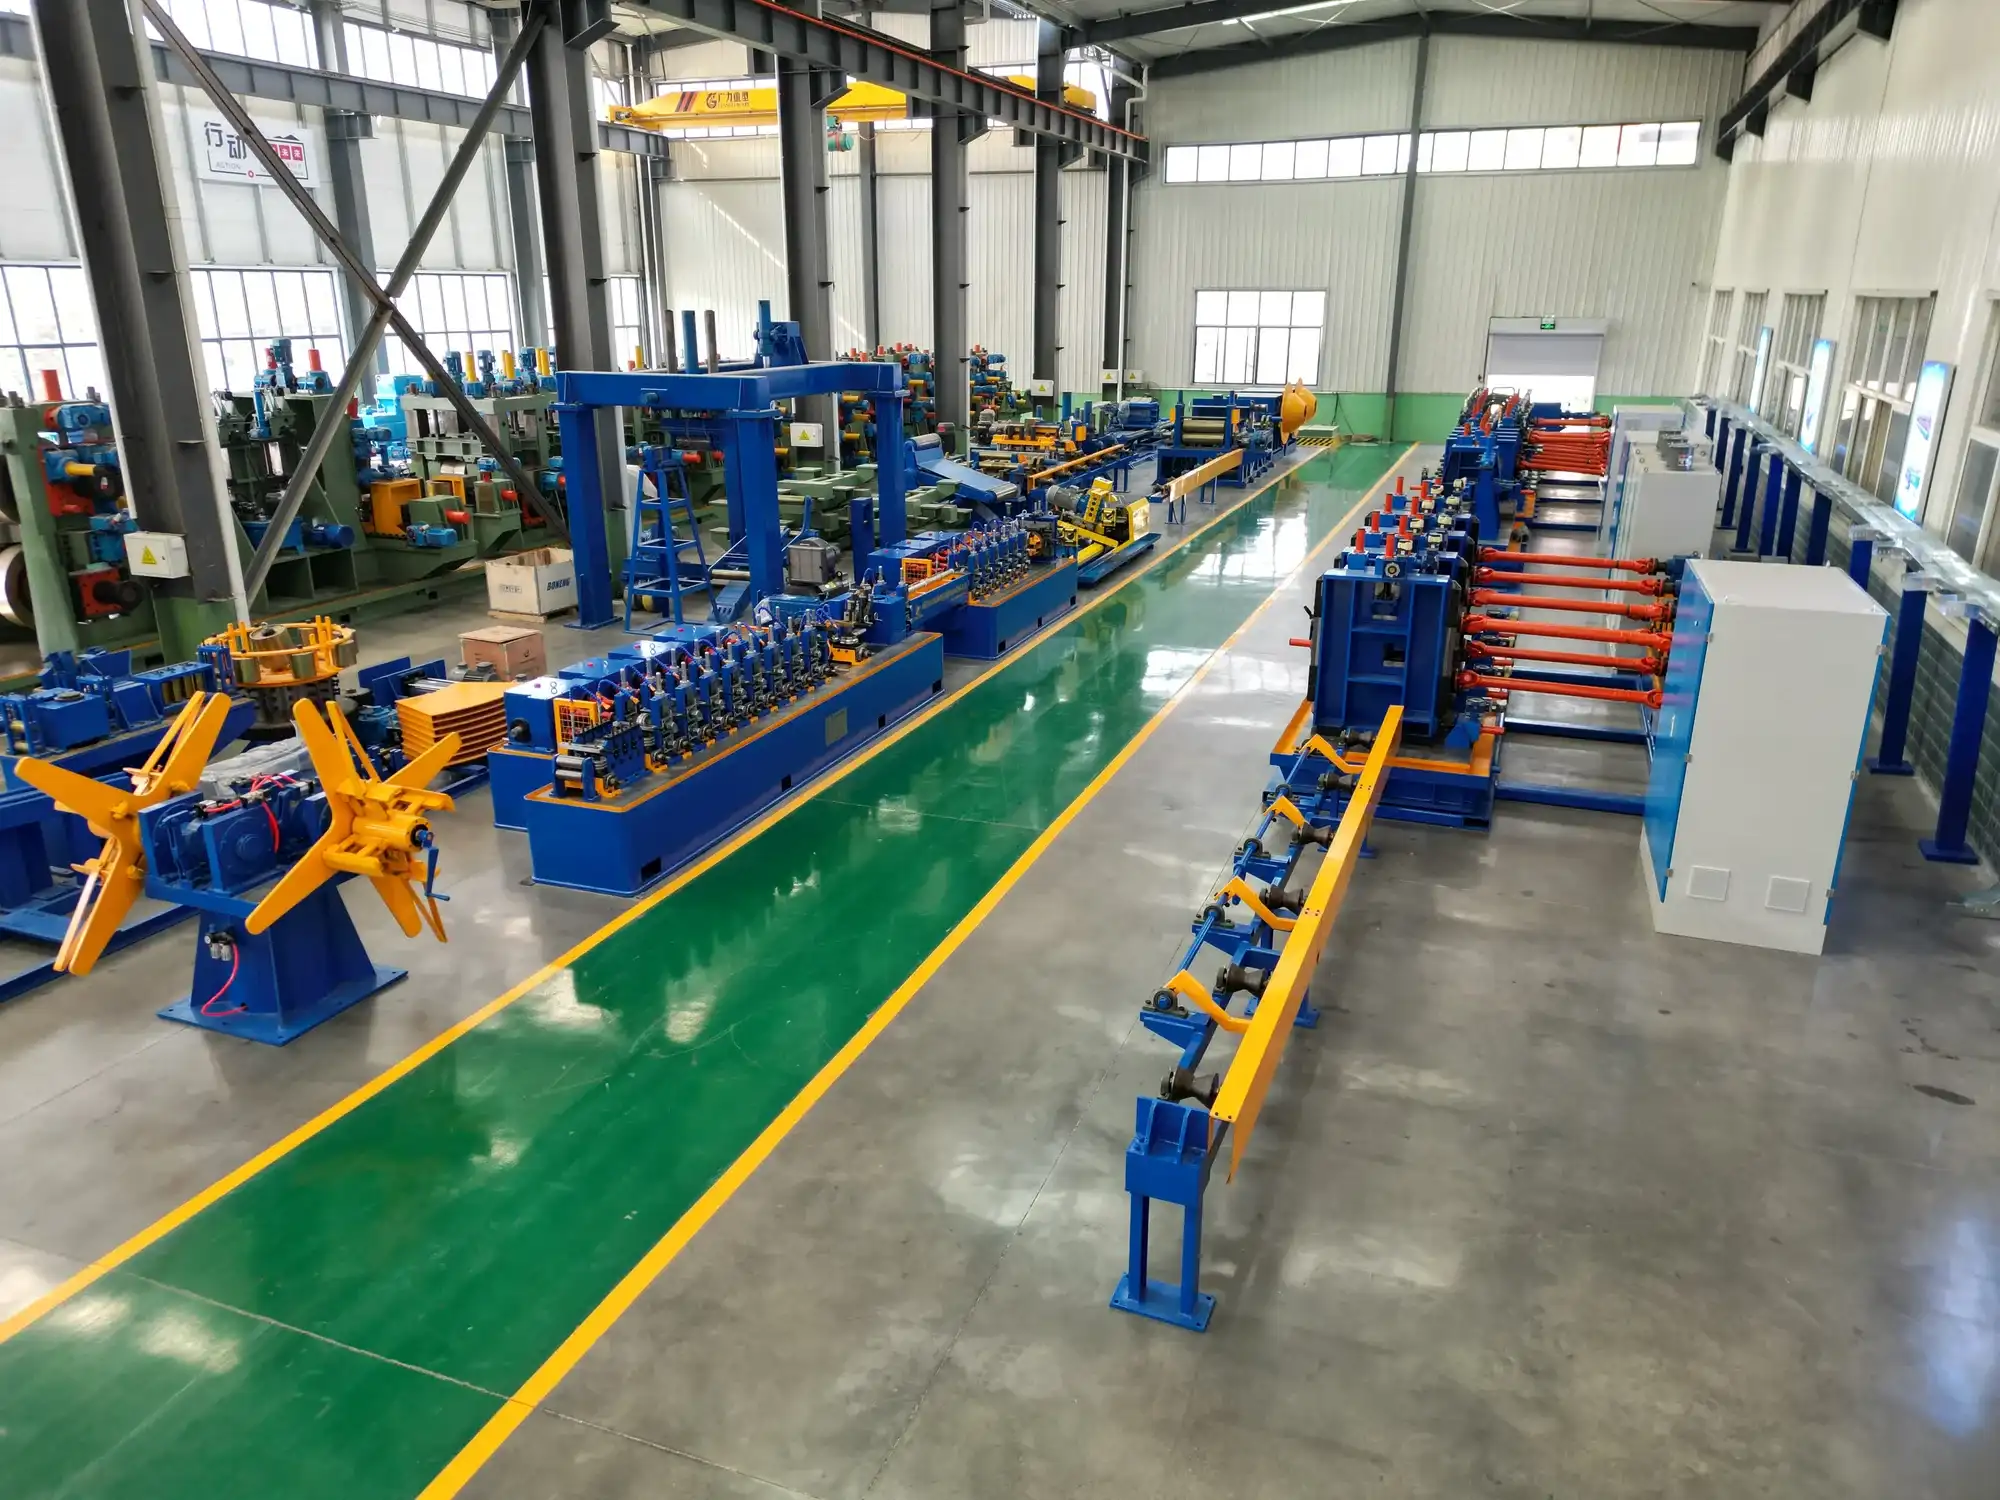
We machine rolls in-house on our own CNC equipment, and that matters for exactly the reason a plant manager would give: replacement rolls stay obtainable years after handover instead of becoming an obsolescence problem. The same capability covers edge-milling inserts and cutter heads on the spiral line.
Roll consumption differs by line. On a longitudinal mill, changing pipe size means changing rolls.
On a spiral line, diameter is changed by changing the forming angle, so the roll set is not changed for size at all.
Two failure modes are worth naming because they are the ones that show up as scrap rather than as a stopped line. A degraded impeder or induction coil spreads the welding energy instead of concentrating it, so seam quality fluctuates and consumption rises before anything actually breaks.
A blunt edge-milling insert produces an uneven bevel, and an uneven bevel produces an uneven joint gap — which on a submerged-arc seam means lack of penetration and misalignment found later at ultrasonic or X-ray inspection.
A third failure mode belongs with the media rather than with the hardware, and it is the one most often mistaken for a machine fault. Submerged-arc flux absorbs moisture, which is why the line is supplied with a drying and magnetic separation system and a recovery unit rather than with flux alone.
Damp flux, or recovered flux returned to the hopper without magnetic separation, produces porosity and slag inclusions in the seam — and those are found at ultrasonic or X-ray inspection, after the pipe has already been made.
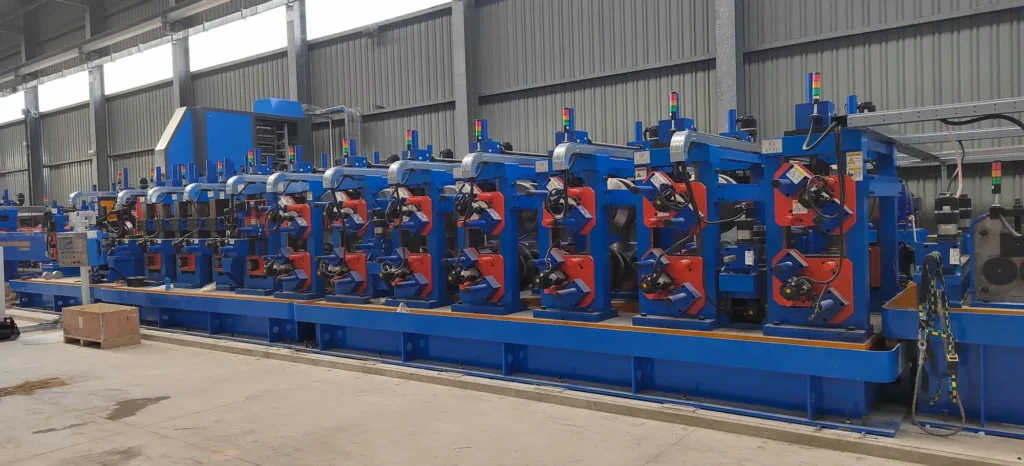
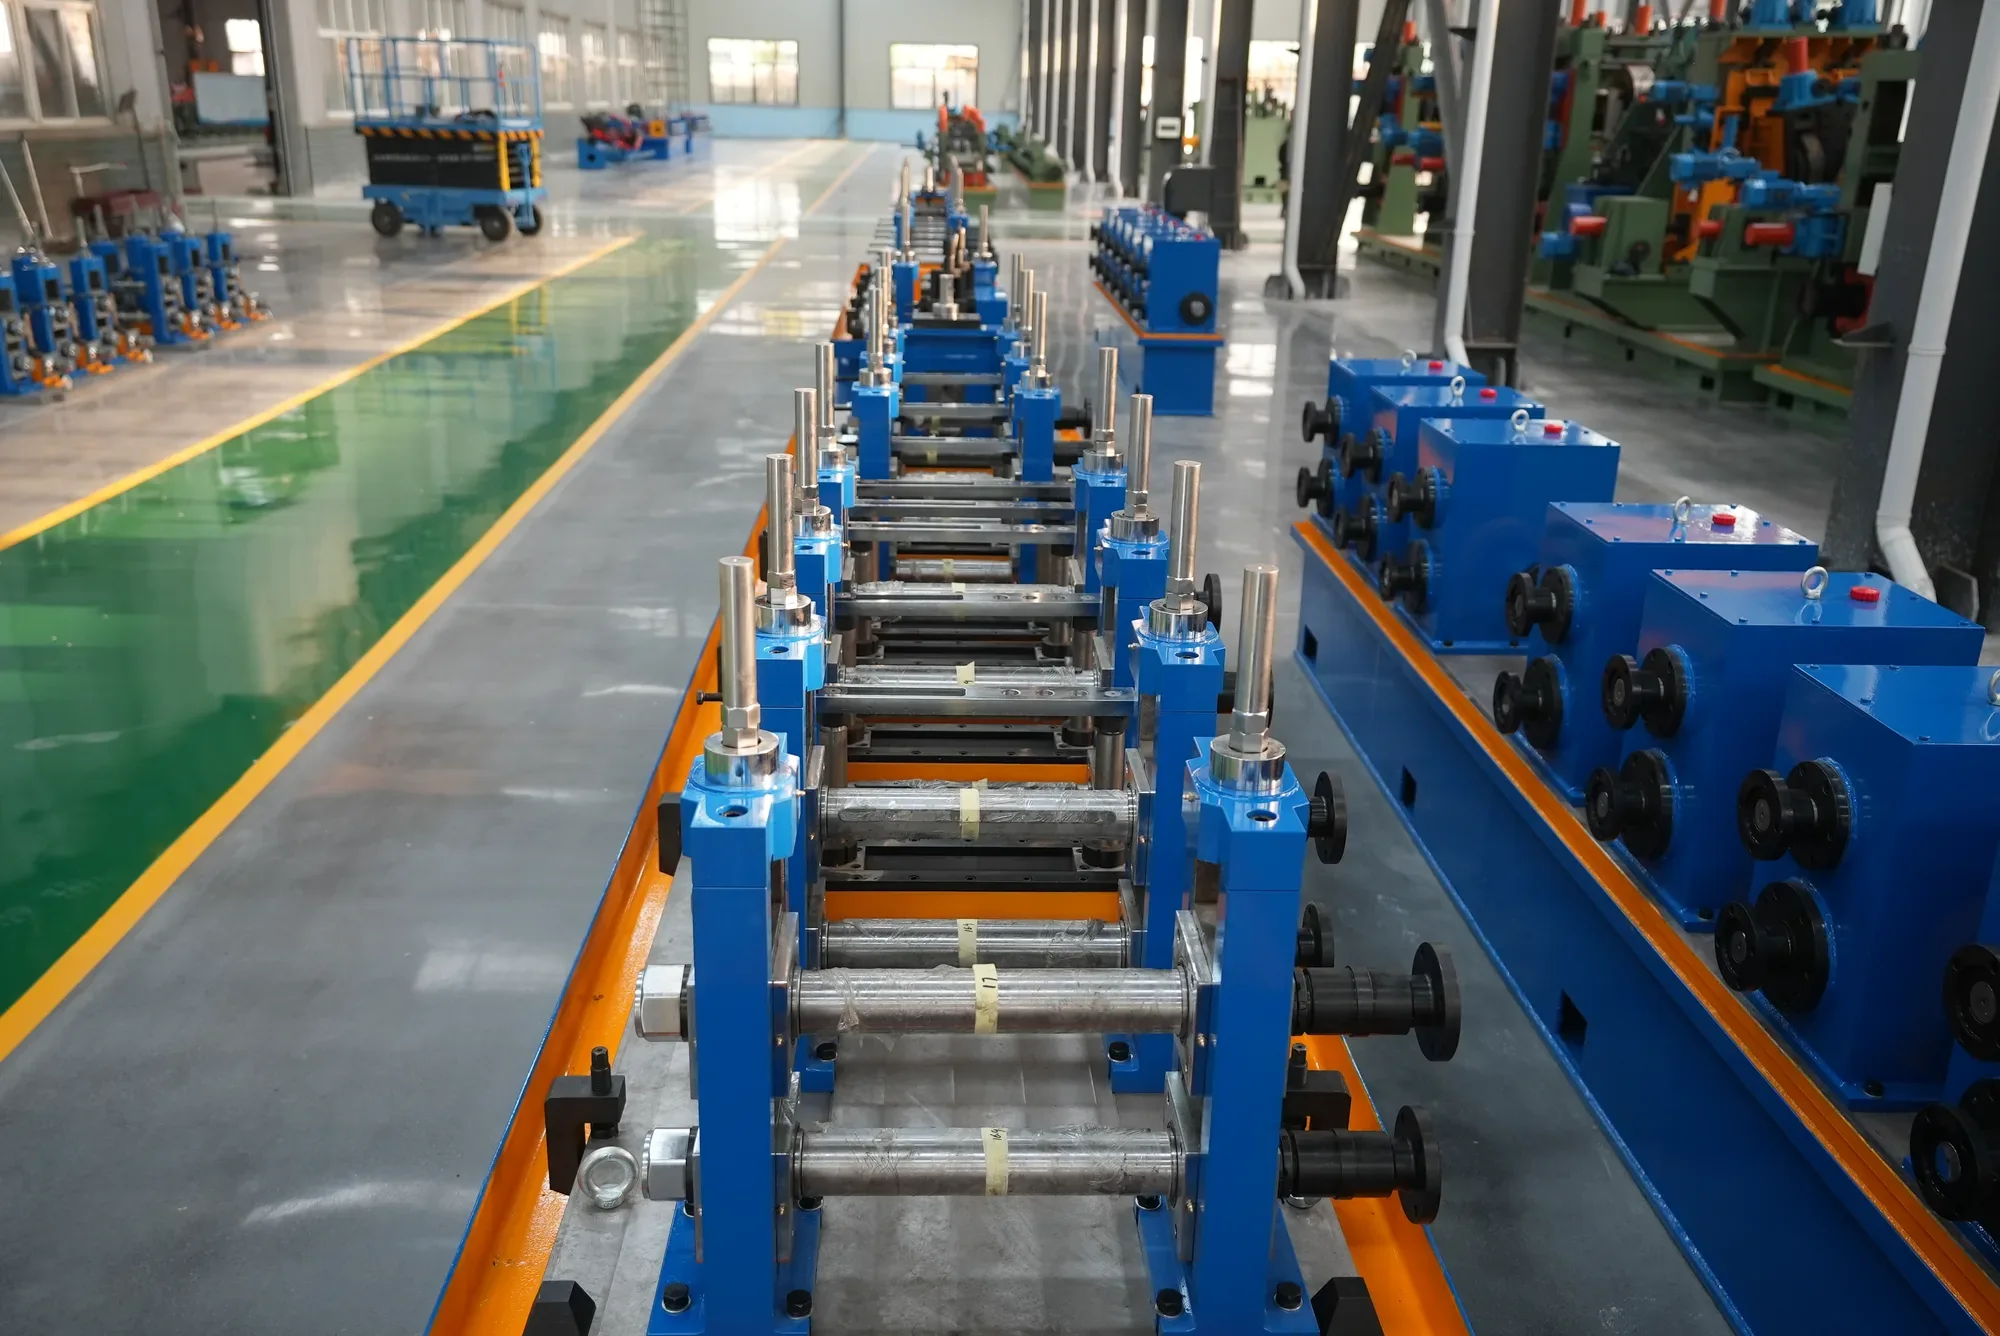
Forming and sizing rolls determine shape accuracy, roundness and squareness, edge definition and dimensional consistency; roll material and heat treatment decide how long that holds.
Applications and Output Examples
Poor after-sales and spare-part supply is a known reason plants change equipment suppliers: they need a manufacturer that can keep supplying rolls and parts and respond quickly.
Our after-sales commitment answers that requirement — a single named point of contact, all-hours online support, on-site dispatch and direct spare-part shipment.
For distributors and agents the emphasis shifts to continuity of supply over years rather than speed on a single order: long-term roll and spare-part supply is one of the things an agent needs from a manufacturer, alongside on-time delivery and technical support.
For end users in precision-driven sectors the emphasis shifts again, towards dimensional stability and technical response rather than part price.
Where responsibility sits is simple here and worth stating once. Supplying the part and specifying the medium is our side. Replacing wear parts on time is the operating side: disciplined consumable replacement is one of the factors that decide whether a line holds quality across a run.
The buyer for spare parts is usually an existing plant rather than a new one.
Delivery, Installation and Training
Equipment lead time is 50–90 days; spare-part lead time may differ.
Direct spare-part shipment is part of our after-sales commitment, which for an overseas plant is the practical question behind “can I still get these in three years”.
Spare-part supply is also what decides whether a plant comes back. A track record of repeat purchases and global references is the basis of the long-term relationship, and expanding plants reorder from the same source for compatibility across the shop.
Spare parts are where that claim is actually tested: a supplier that cannot ship an impeder to a plant three countries away in year four has not earned the reorder, whatever the original line was like.
Behind the supply sits in-house CNC machining capacity for rolls and key wear parts, an engineering team of twenty averaging twenty years each, and an owned production base open to factory audit.
Certification: GB/T 19001-2016 / ISO 9001:2015 (quality management system, certificate No. 18524Q11269R2S). Material and hardness specifications cited are those for the spiral line rolls (GCr15, HRC 56-60; 42CrMo, HRC 52-58) and the purlin line dies (Cr12).
Export packing is specified per item, and for spare parts that specification is a core part of the supply, not a packing footnote. Control cabinets, impeders and induction coils, forming rolls and cutting tools travel in moisture-protected wooden cases with a spare-parts pack; heavy frames ship bare, braced on cradles with designated lifting points and rust protection.
Welding wire for pipe mill
Accumulator for tube mill
From the Workshop
 Roll Forming Rollers
 The API Pipe Mill Inspection Chain
 Pipe Coating Line Configuration
 H Beam Welding Line
Send Your Enquiry
Tell us the pipe outside-diameter range, the wall thickness and the output you need. An engineer reads every enquiry — it does not land in a general sales inbox.