
 Scan on WeChat
Home › Tube Mill › Small-Diameter Tube Mill › HG76
The third of the twelve model steps — Φ12.7 to 76 mm round pipe and 10×10 to 60×60 mm square section, on a 250 kW high-frequency welder.
Model Steps
In This Line
Quick Contact
Hebei TengtianYuanle@tentubemill.com
+86-311-83025332
WhatsApp +852 5425 3155
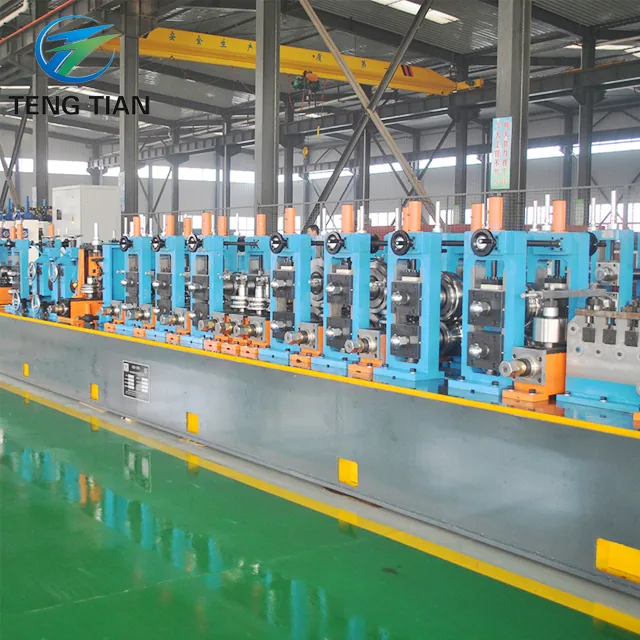
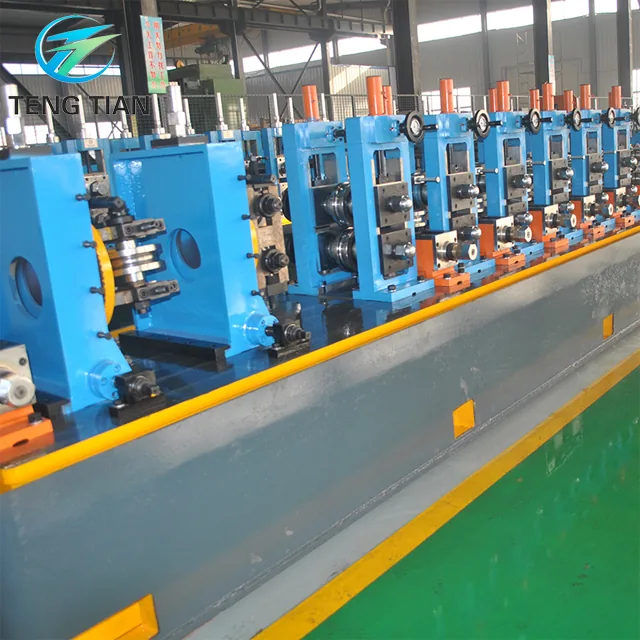
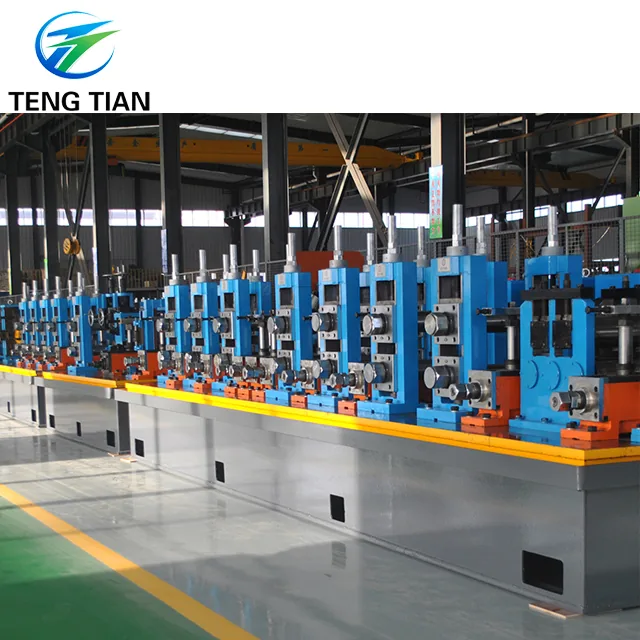
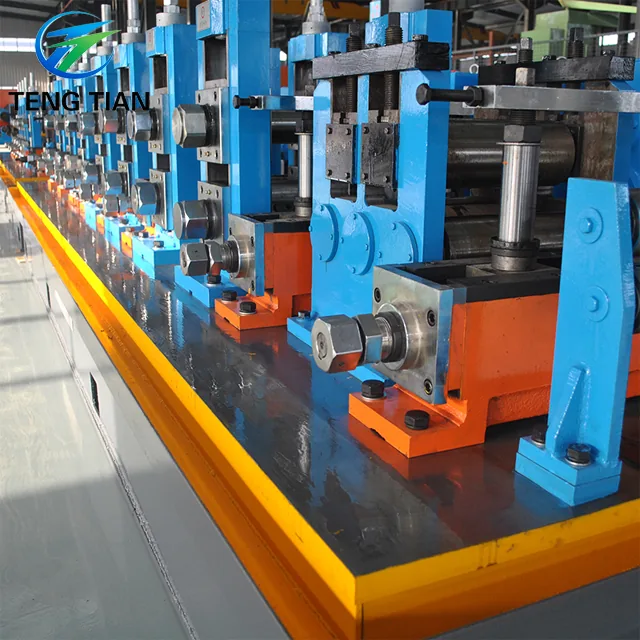
HG76 is the third of the twelve steps, and its band is the widest of the small-diameter group: Φ12.7–76 mm. That width is the reason it is often the first mill a plant buys — one step covers most of what HG32 and HG50 cover and reaches up to 76 mm.
Line Specification — HG76×3.0
| Round tube outside diameter | Φ12.7 – Φ76 mm |
|---|---|
| Wall thickness | 1.5 – 3.0 mm |
| Square / rectangular tube | Square 10×10 – 60×60 mm; wall 1.5 – 2.5 mm |
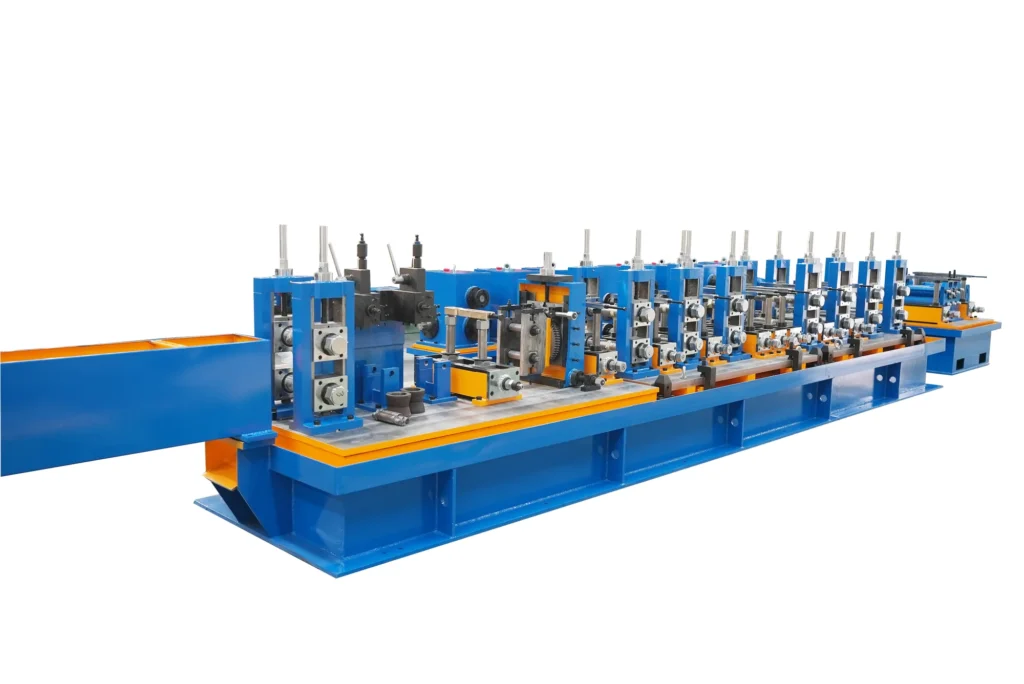
Technical Specification Table
- Outside diameter range: Φ12.7–76 mm, the third of twelve steps.
- Section shapes: round, square and rectangular.
- Forming: conventional roll forming.
- Welding: high-frequency induction.
- Automation: semi-automatic or full PLC.
- Welder power for this step: 250 kW
Series band 0.5–16 mm applies to HG32–HG630 as a whole. Wall thickness per step: 1.5 – 3.0 mm.
Line Configuration and Scope of Supply
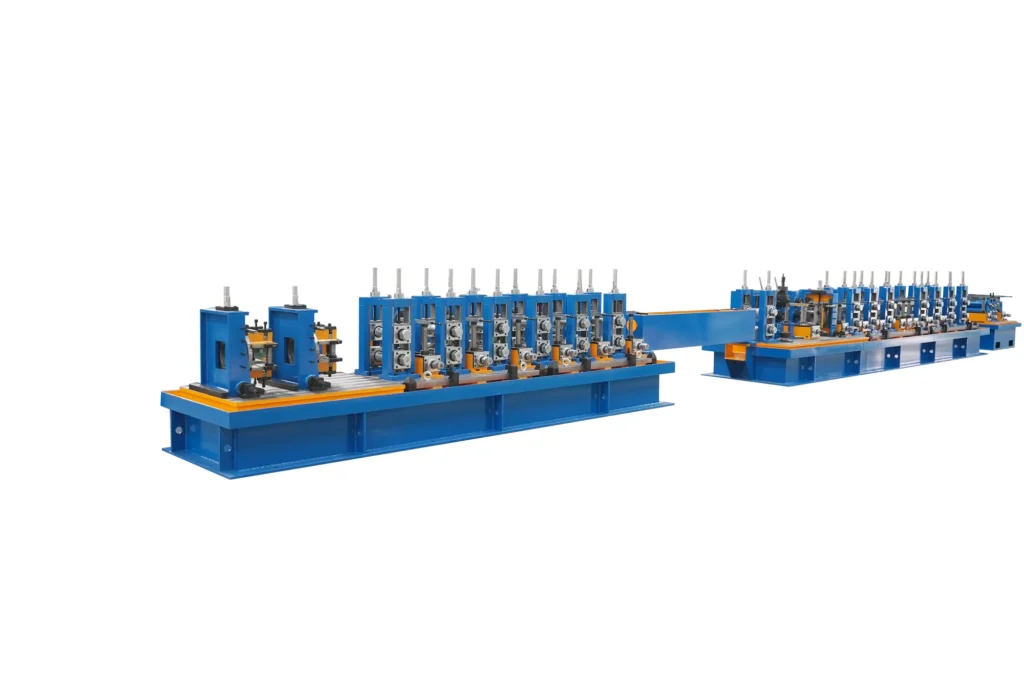
Eight units, at series level:
- Expanding-mandrel uncoiler.
- Five-roller leveller.
- Automatic shear-welder.
- Spiral accumulator.
- Forming and sizing mill.
- HF induction welder.
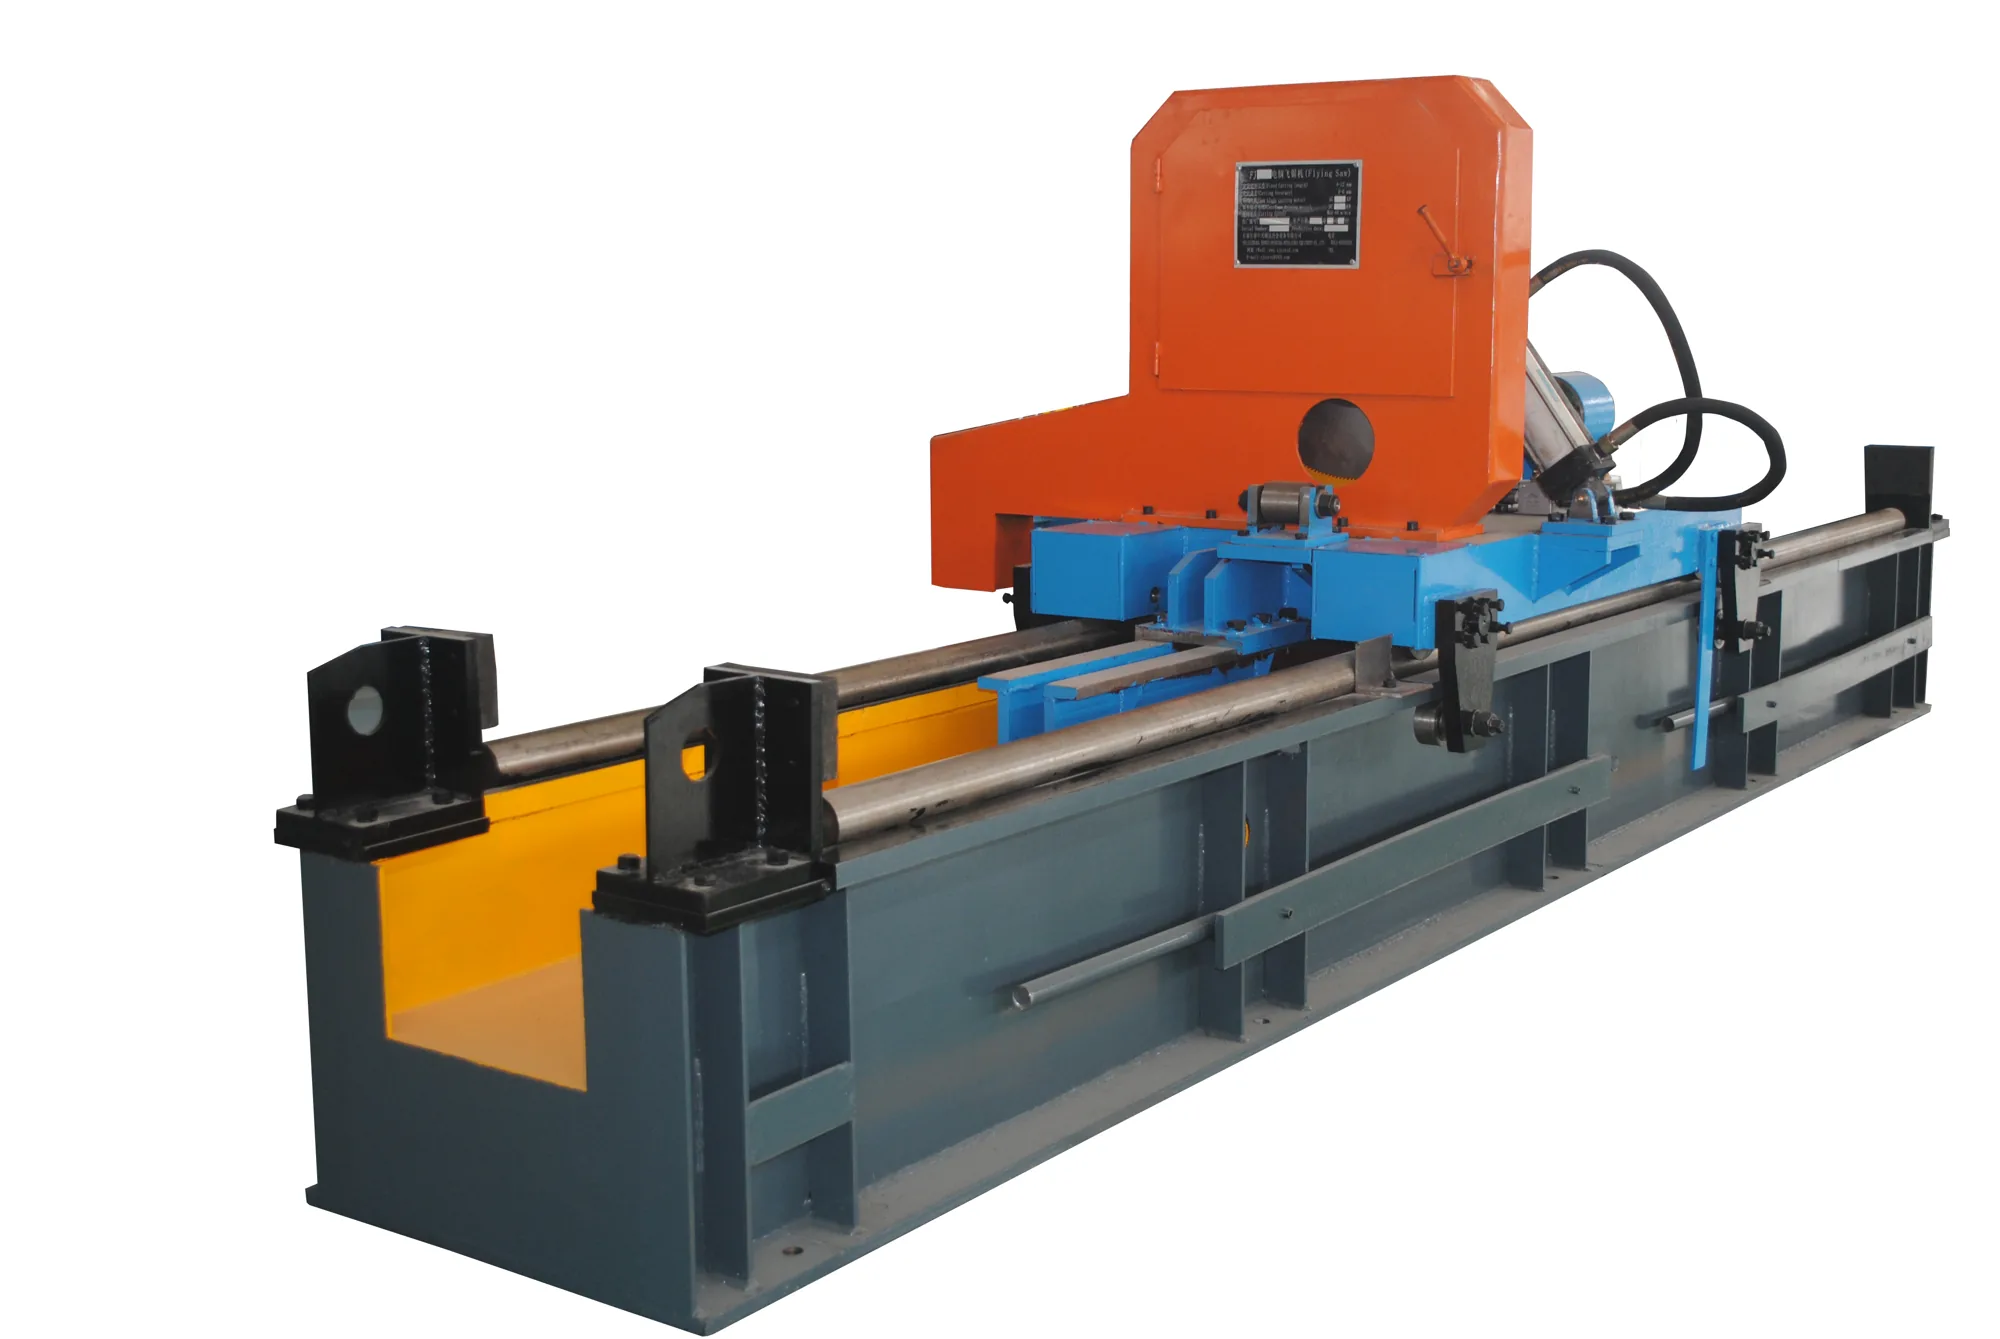
- Flying saw.
- PLC and VFD control.
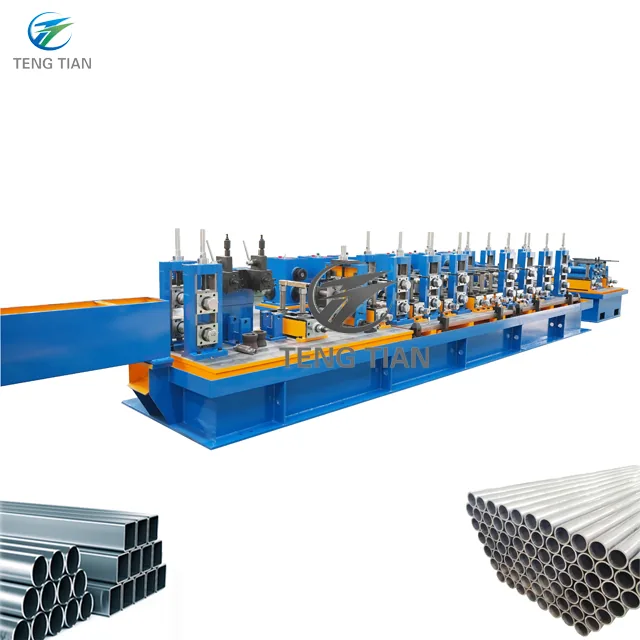
Tube mill for 76mm pipe
Because this step overlaps both HG50 below it and HG89 above it, the practical question is not which mill can reach 76 mm but which mill will spend the least time changing size for the mix you actually run. That is a scheduling question about your product spread, best settled at enquiry.
Wall thickness, line speed and shift output are confirmed against your pipe size, material grade and cut length at quotation. Send us those three and we will state the figures.
Wear Parts and Consumables
Saw blades and cutting tools are consumed by cutting volume; impeders and induction coils by welding hours; forming and sizing rolls are replaced on wear and are machined on our own CNC equipment. Cooling medium and hydraulic oil are specified by us and bought locally by the plant.
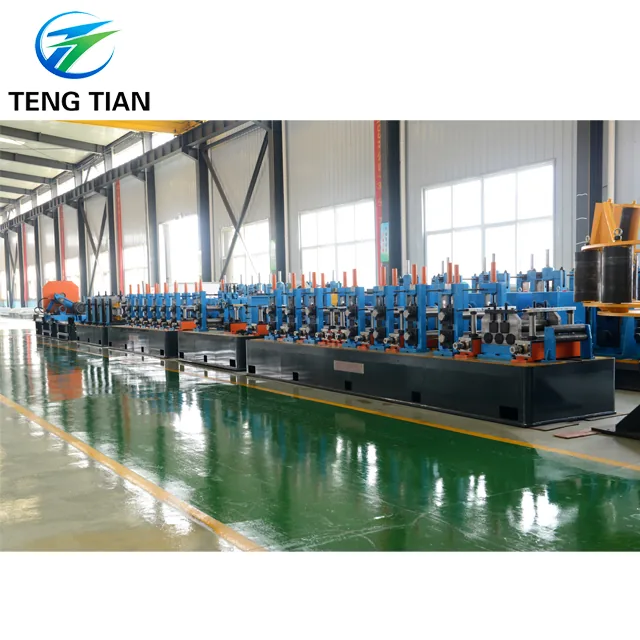
Size Change, Roll Wear and Running Cost
Within Φ12.7–76 mm, a size change is a roll-set change. The roll material and its heat treatment are what decide how often that set has to be reworked: rolls that are under-specified wear early, drift on diameter and need frequent regrinding.
Weld fusion is set on the equipment side by welder power matching, seam alignment and squeeze control; strip quality and operating practice sit with the buyer. Yield above 93 per cent is supported by the line design and also depends on how the plant runs it.
Send diameter, wall and mix and we will size the step and name what is still open.
Where this step sits in the twelve
HG76 is the third rung, and the widest band in the small-diameter group. The ladder above it runs HG89, HG114, HG165, HG219, HG273, HG325, HG426, HG508 and HG630.
Anonymised delivery record
Deliveries in this band: Egypt at HG76 × 3, India at 76 × 3, and Malaysia at HG60 × 3.
The buyer for this band
The end-user profile that fits is the regional pipe and section maker: a small or mid-size plant building or expanding capacity, sensitive to price and lead time, judging on return on investment, changeover efficiency, roll cost and energy per tonne.
Two of that buyer’s objections are worth answering directly. The first is whether spare parts and rolls will keep coming from a Chinese supplier — answered by in-house CNC roll machining, direct spare-parts shipment and on-site dispatch.
The second is whether a size change means a long stoppage — answered honestly here: on a conventional roll-forming step it does mean a roll change, and the line that removes the roll change is the direct-forming square line, not this one.
Delivery, installation and support
Shipped dismantled in containers, delivery 50 to 90 days, installation and commissioning included, on-site dispatch and round-the-clock support, single contact replying within one hour. Payment 30 per cent deposit and 70 per cent before shipment, third-party escrow available.
Quality factors that apply at this diameter
Of the ten quality factors, four are the ones a plant running this band adjusts most often: HF power, frequency and welding speed; squeeze amount and seam alignment; sizing and straightening; and impeder and coil condition.
The other six sit either upstream — incoming strip grade, thickness tolerance and flatness, and roll material and heat treatment — or in control and inspection: PLC and servo stability, operator setup at size change, post-weld cooling, and final inspection.
What to send with an enquiry
Outside diameter, wall, section shape, target output, and the spread of sizes you expect to run, since this band is wide enough that the spread matters more than the peak.
One more boundary on this step
The width of this band makes it the step most often quoted against two others at once. Read it against HG50 below and HG89 above using the bands rather than the model numbers: Φ16–50.8 and Φ32–89 mm respectively. Correct sizing — diameter against power against unit configuration — is its own risk, so the comparison belongs in the enquiry.
One division of responsibility
Responsibility for the finished pipe is split rather than shared. Weld fusion is on the equipment side through power matching, seam alignment and squeeze control; strip quality and operating practice are on the buyer’s. Dimensional accuracy divides the same way: sizing and straightening on the equipment side, incoming strip thickness tolerance on the buyer’s.
Rolls and key wear parts are machined in-house, which is the supply answer rather than a performance claim: it is why a roll set can still be replaced years after handover.
Watch This Line Running

HG76 High-Frequency Welded Pipe Mill — O.D. 12.7-76 mm
HG76 Lines in Service
Photographs taken at customer plants. Customer names are withheld; each card shows the country, the industry and the model or size.
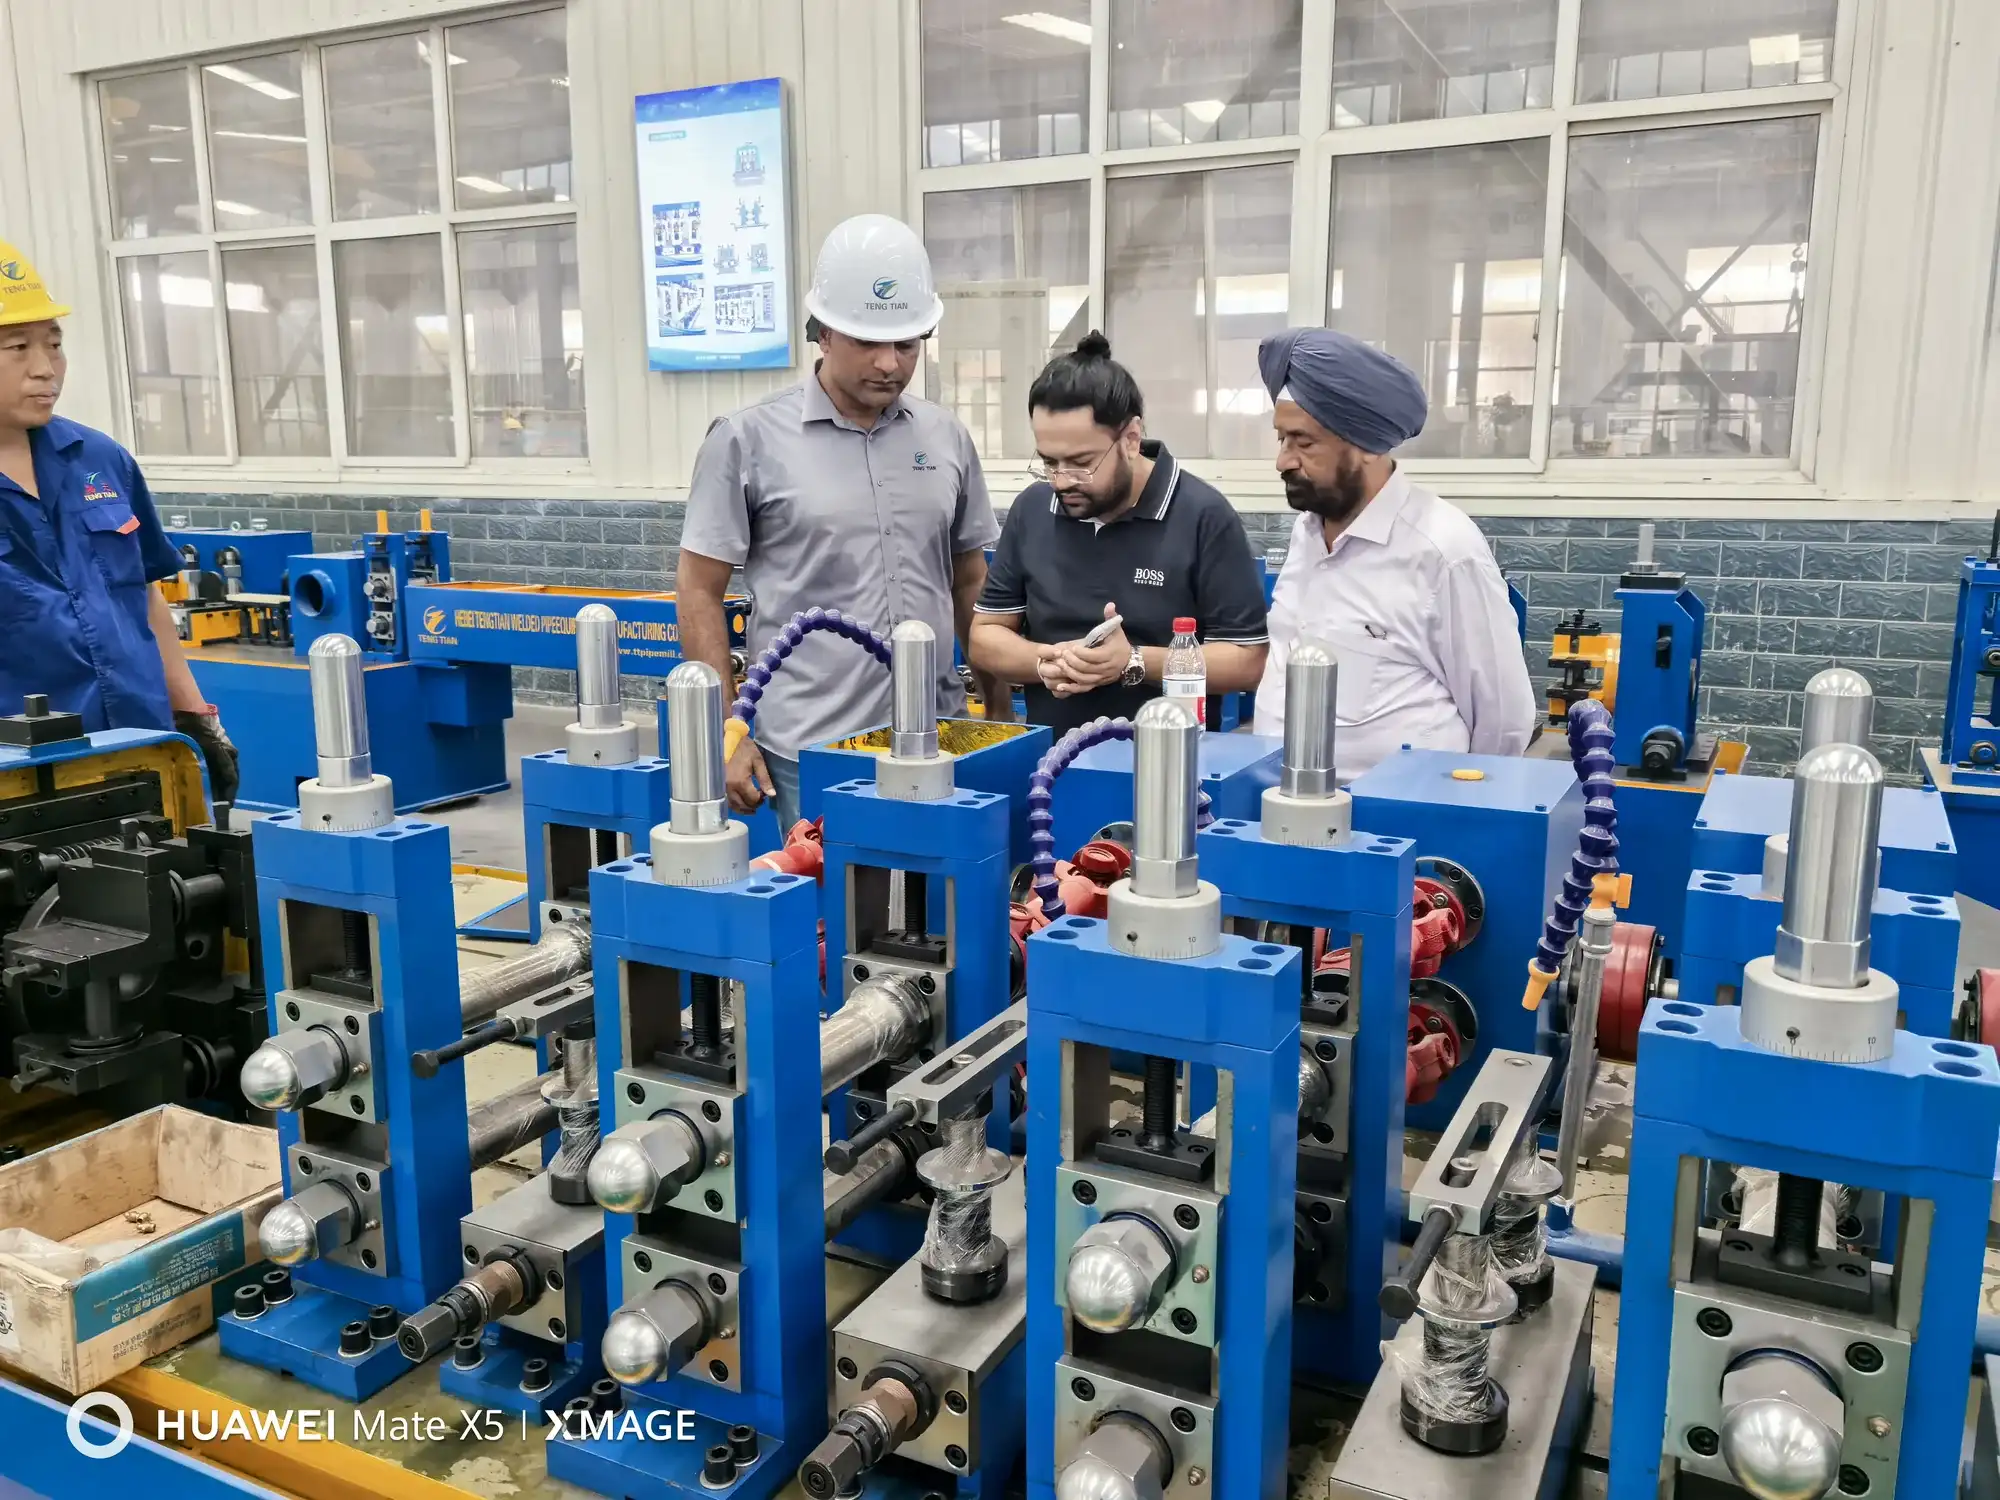
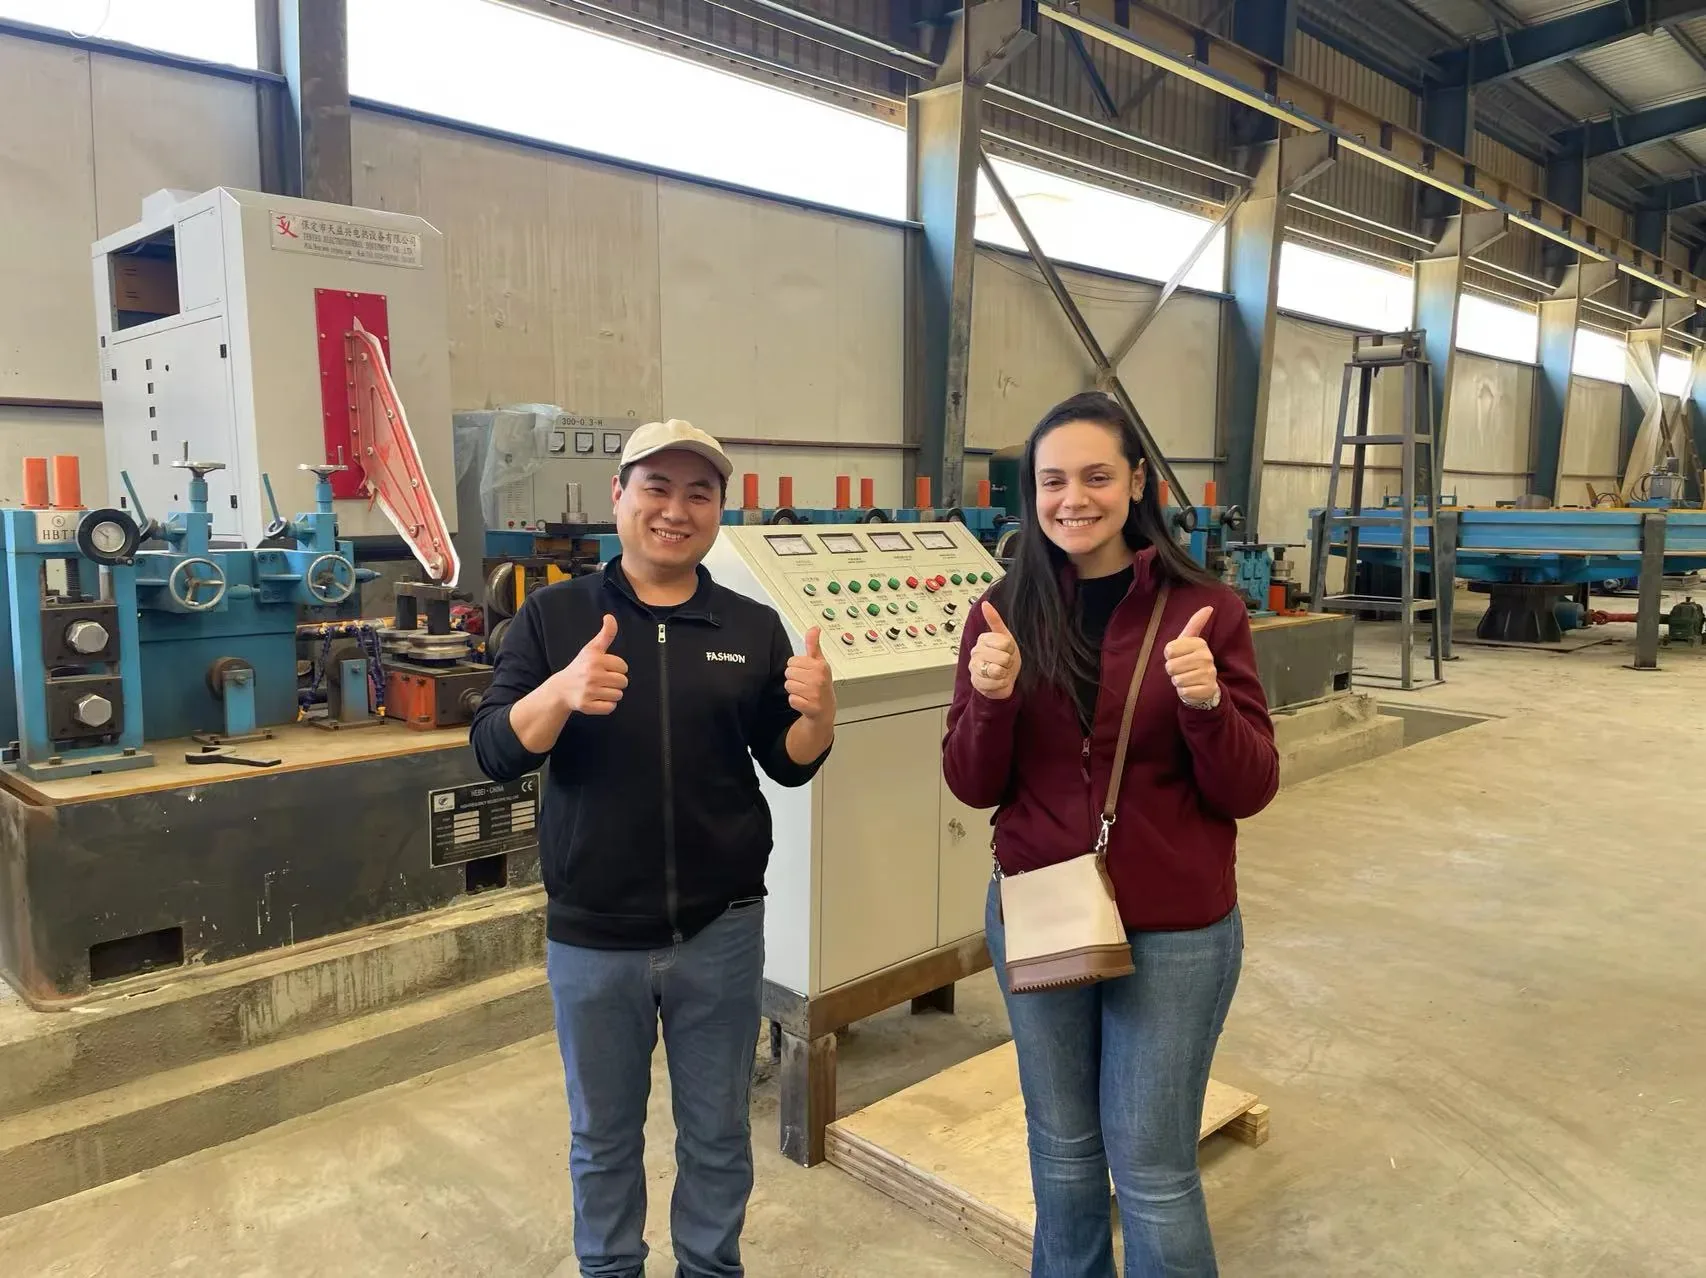
Line Photos from the Works
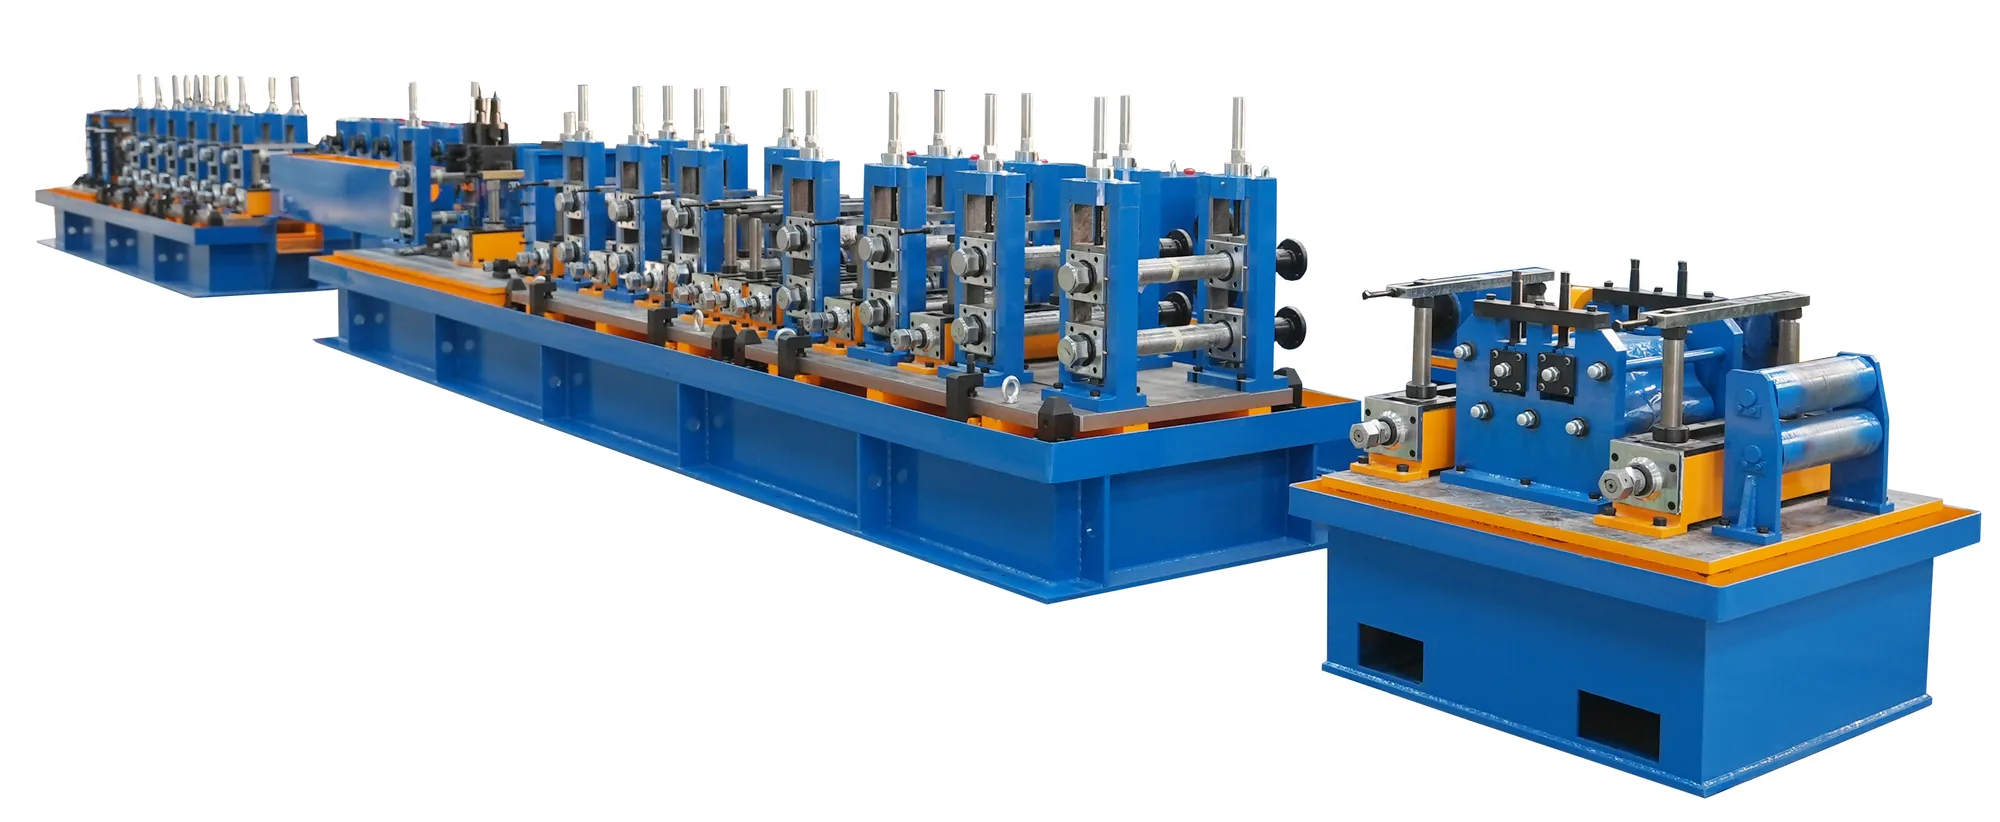
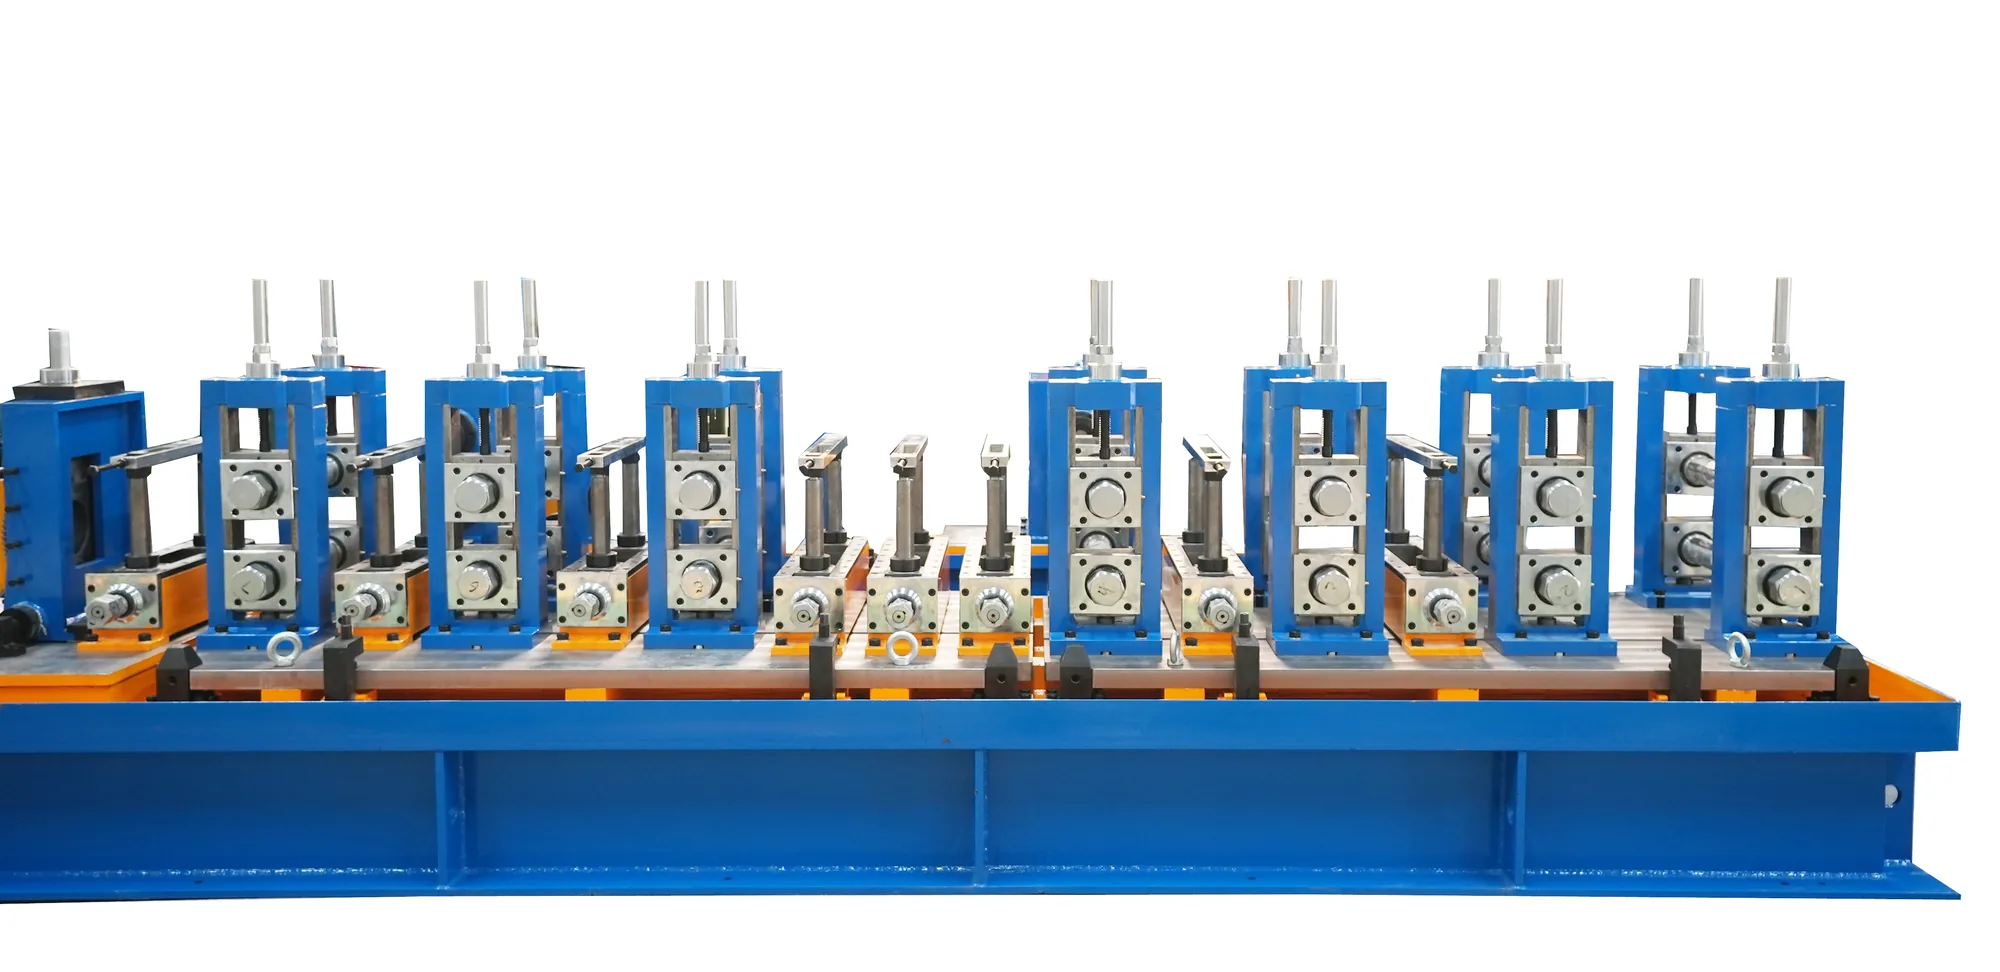
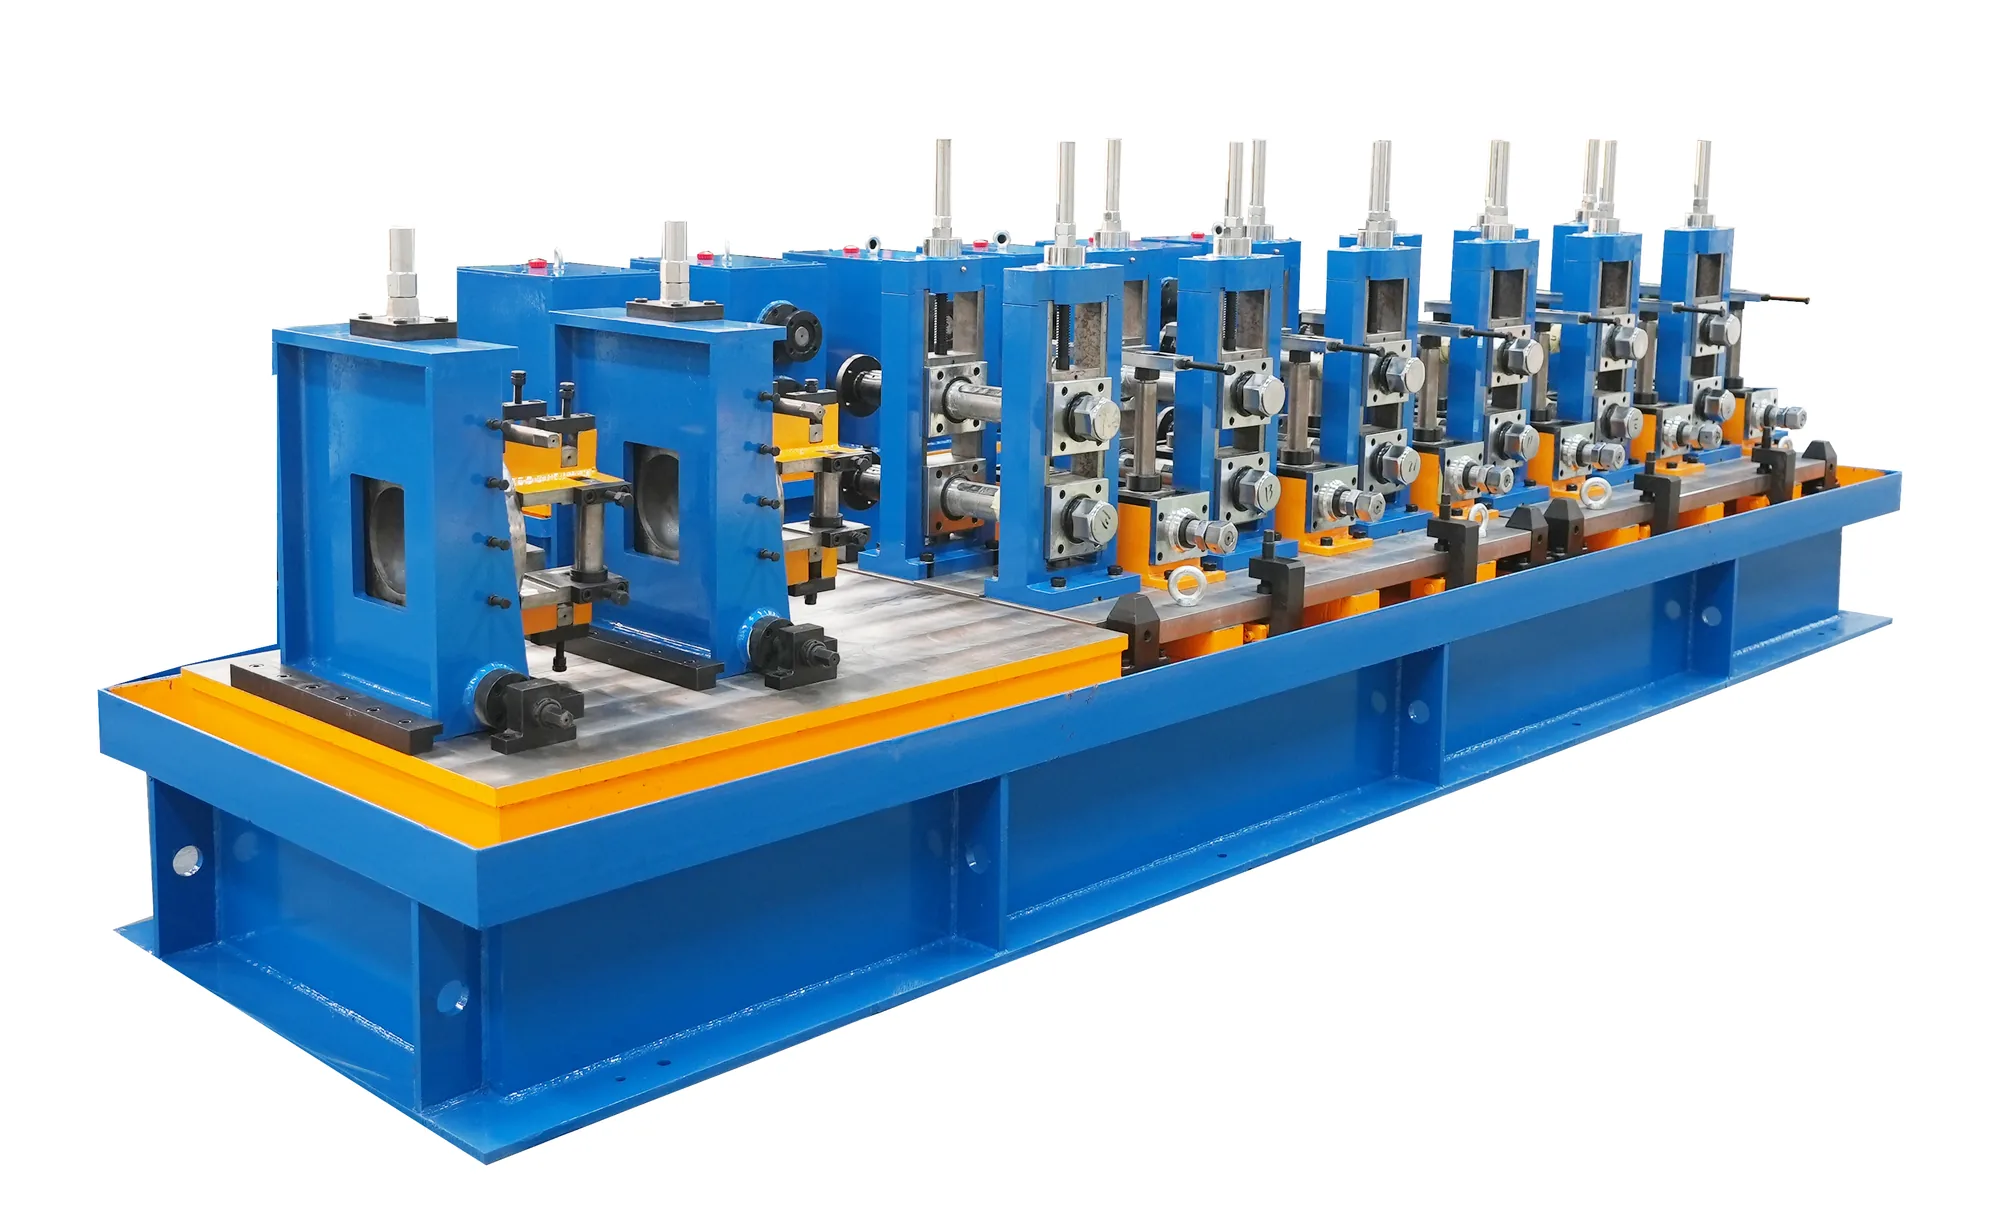
Six photographs of this line, taken in our own workshop. Click any photo for the full-size image.
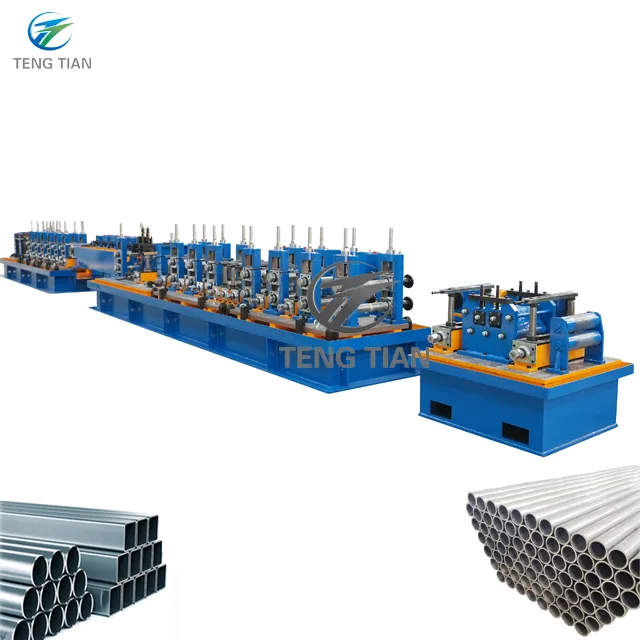
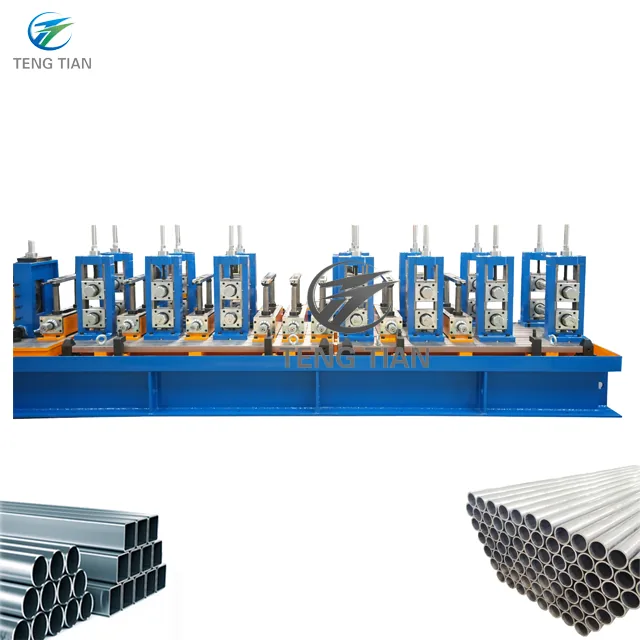
More from this line
Neighbouring Model Steps
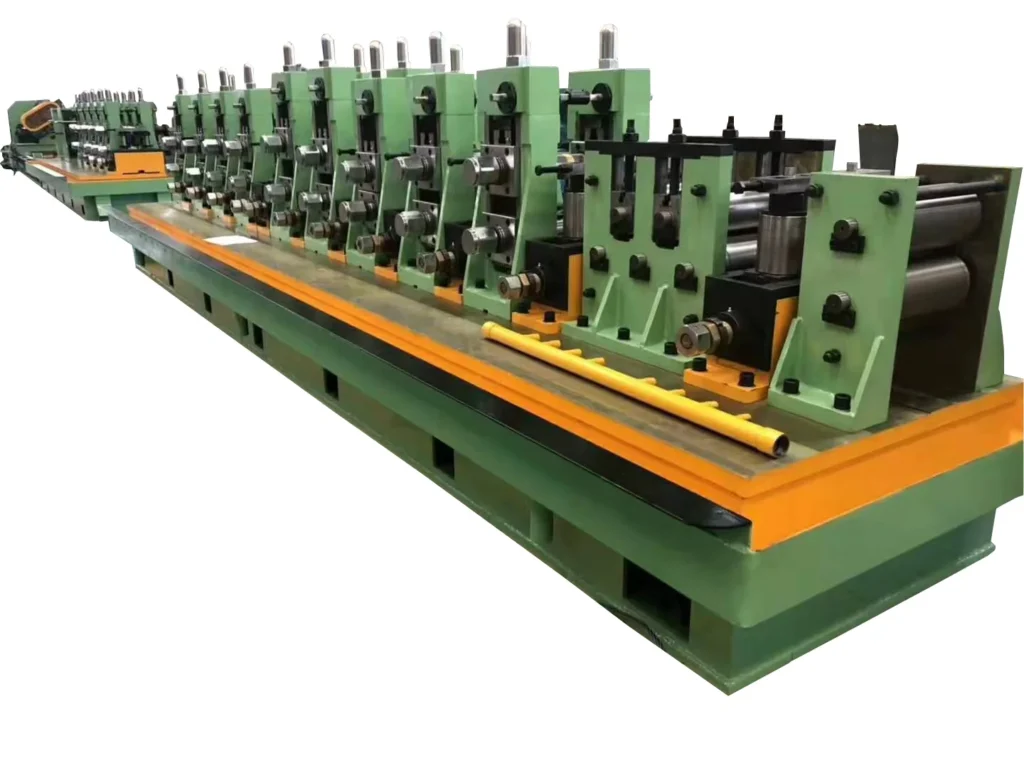 HG50 — Φ16 – 50.8 mm
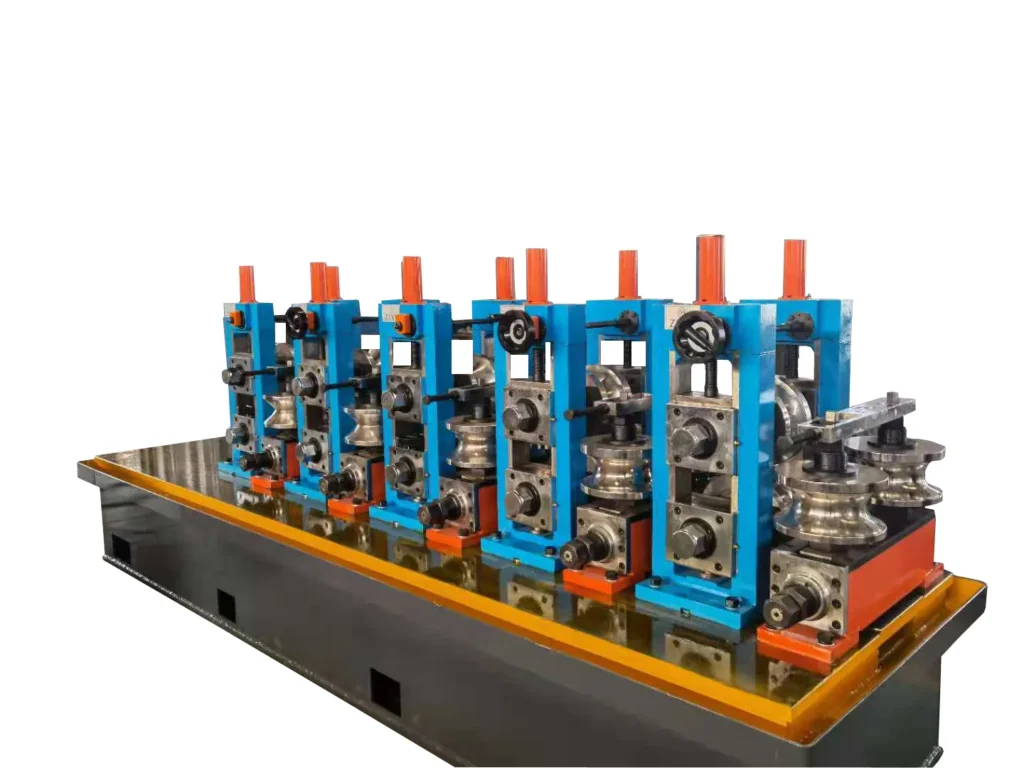 HG89 — Φ32 – 89 mm
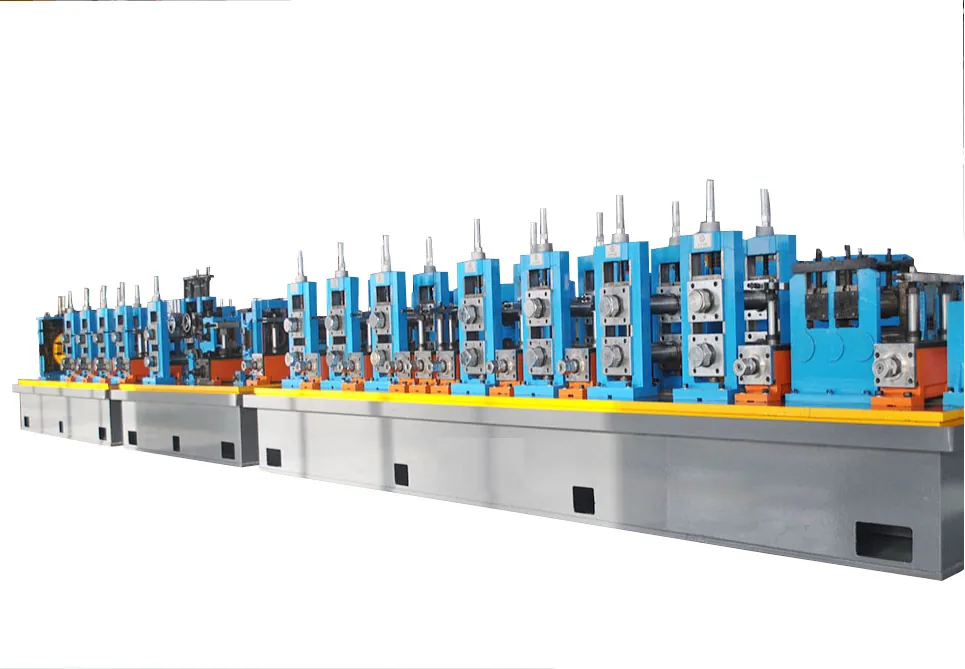 HG114 — Φ45 – 114 mm
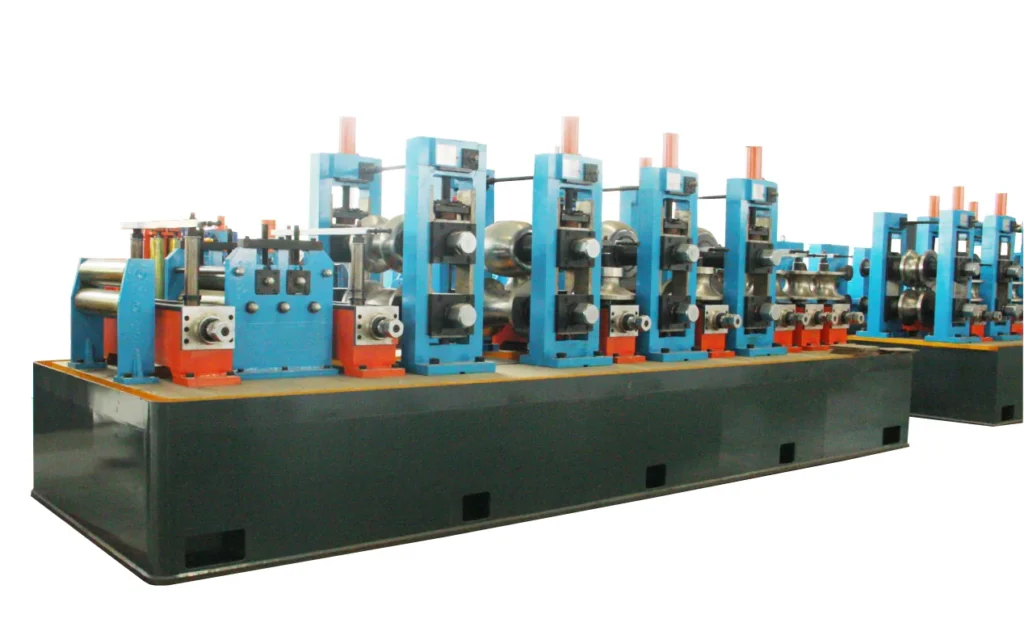 HG165 — Φ60 – 165 mm
Send Your Enquiry
Tell us the pipe outside-diameter range, the wall thickness and the output you need. An engineer reads every enquiry — it does not land in a general sales inbox.