
 Scan on WeChat
Home › Tube Mill › Large-Diameter Tube Mill › HG273
The eighth of the twelve model steps — Φ114 – Φ273 mm round pipe and 90×90 – 215×215 mm square section, on a 600 kW high-frequency welder.
Model Steps
In This Line
Quick Contact
Hebei TengtianYuanle@tentubemill.com
+86-311-83025332
WhatsApp +852 5425 3155
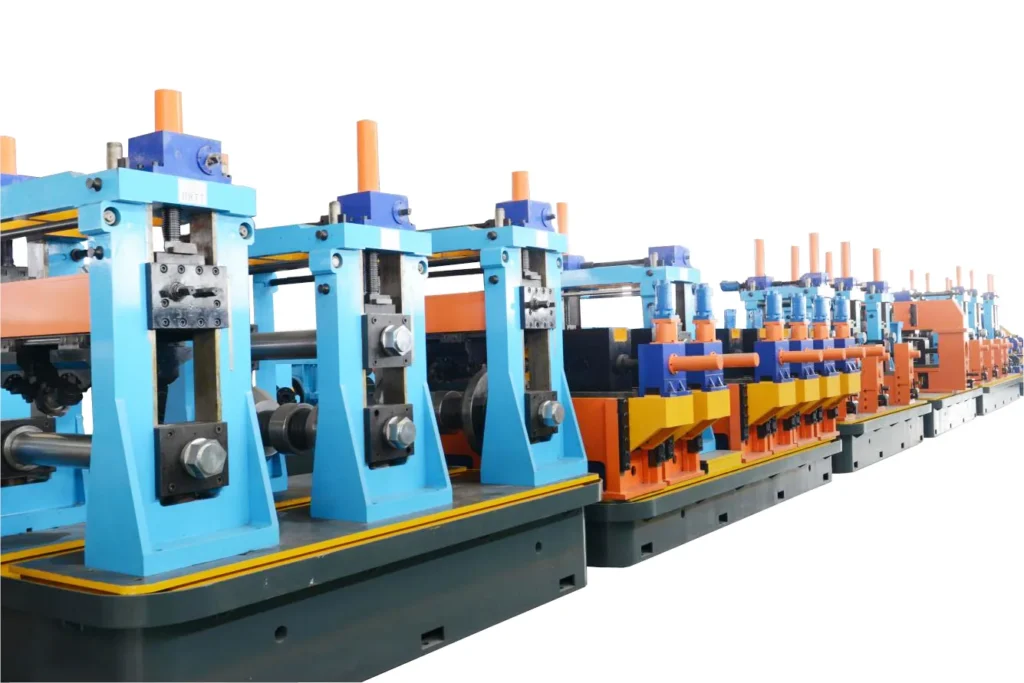
HG273 is the eighth of the twelve steps, covering Φ114–273 mm. Its lower bound is the same as HG219’s, which means the two steps overlap across their whole lower half and the choice between them is not a coverage question but a question of the largest size you actually need.
Line Specification — HG273×10
| Round tube outside diameter | Φ114 – Φ273 mm |
|---|---|
| Wall thickness | 4.0 – 10.0 mm |
| High-frequency welder | 600 kW |
| Square / rectangular tube | Square 90×90 – 215×215 mm; wall 4.0 – 9.5 mm |
Watch This Line Running
HG273 High-Frequency Welded Pipe Mill — O.D. 114-273 mm
Technical Specification Table
- Outside diameter range: Φ114–273 mm, the eighth of twelve steps.
- Section shapes: round, square and rectangular.
- Forming: conventional roll forming.
- Welding: high-frequency induction.
- Automation: semi-automatic or full PLC.
- Welder power for this step: 600 kW
Line Configuration and Scope of Supply
- Expanding-mandrel uncoiler.
- Five-roller leveller.
- Automatic shear-welder.
- Spiral accumulator.
- Forming and sizing mill.
- HF induction welder.
- Flying saw.
- PLC and VFD control.
Tube mill for 273mm pipe
At this diameter the buyer is usually producing line pipe or heavy structural section, and the two application families separate clearly. Fluid transport takes carbon steel welded pipe for oil and gas, municipal water and gas, and chemical and heating lines; structural takes load-bearing and general mechanical section.
Wear Parts and Consumables
Saw blades by cutting volume; impeders and coils by welding hours; forming and sizing rolls on wear, machined in-house so replacements stay available. Cooling medium and hydraulic oil: specification from us, sourcing local.
Size Change, Roll Wear and Running Cost
Line design supports yield above 93 per cent, with the achieved figure depending on plant practice. Roll sets at this diameter are the heaviest in the conventional forming range, so a size change is the single largest planned stoppage on the line. Wall thickness, line speed and shift output are confirmed against your pipe size, material grade and cut length at quotation. Send us those three and we will state the figures.
What we offer is the supply answer: rolls and key wear parts are machined on our own CNC equipment, so a worn set can be replaced years after handover rather than becoming a sourcing problem.
Send the largest diameter you need, the wall and the target output and we will confirm whether this step or HG219 fits, and list what is still open.
Where this step sits in the twelve
HG273 is the eighth rung. HG219 shares its lower bound at 114 mm; above it HG325 starts at 165 mm and HG426 at 165 mm, so from here upward the bands overlap heavily and the selection question is always the largest size actually needed.
Anonymised reference deliveries
Our deliveries inside Φ114–273 mm: South Korea, construction, 254 × 8 and 200 × 200 × 12; Turkey, construction, 200 × 200; Italy, construction, 150 × 150; Kenya, construction, 150 × 150 × 6; and Afghanistan, construction, 250 × 250.
The buyer for this band
Two profiles apply: large energy and infrastructure groups gated on standards and delivery dates, and regional pipe makers expanding into larger section.
The purchase trigger that fits best is entering a new product type — moving into larger line pipe or heavy structural section usually means a dedicated line rather than a rebuild of an existing one. A second trigger is a supplier switch driven by after-sales failure: spares and rolls not arriving. Our answer is in-house CNC roll machining plus direct spare-parts shipment.
Delivery, installation and support
At this diameter the heavy frames ship bare, braced on cradles with designated lifting points and rust protection, which needs heavy-lift handling at the destination; precision and wear items travel cased with a spare-parts pack.
Delivery is 50 to 90 days; installation and commissioning are included with on-site dispatch and round-the-clock support; a single contact replies within one hour. Payment is 30 per cent deposit and 70 per cent before shipment, with third-party escrow and multiple trade terms.
Handling and shipping at this size
Heavy frames at this diameter ship bare, braced on cradles with designated lifting points and rust protection, which is specifically for large-diameter and heavy lines and needs heavy-lift handling at the destination. Precision and wear items — control cabinets, impeders and induction coils, rolls and cutting tools — travel in moisture-protected wooden cases with a spare-parts pack.
That split is why packing at this size differs from packing on a smaller step: the pattern changes with line size, not with model number.
If the pipe has to carry an inspection record
The API configuration adds annealing, straightening, end facing, hydrostatic test, UT and ECT on top of the mill, and covers API 219/406/426/508 at OD 114–508 mm with wall 6–24 mm.
What to send with an enquiry
Largest outside diameter, wall, grade, target output, and whether an inspection record is required. Correct line sizing — diameter against power against unit configuration — is its own risk, which is why all five are asked for.
One more boundary on this step
At this diameter, operator setup at size change is a quality factor in its own right: the failure mode is shape drift after the change and scrap while setting up, and the mitigation is tooling-change training plus quick roll change. That is why installation and commissioning include training rather than handover alone.
One division worth repeating here
Material yield is shared rather than guaranteed: the line design supports a yield above 93 per cent, and the figure actually achieved also depends on scheduling and operating practice at the plant.
Servo setup limits drift after a change; PLC and variable-frequency control keep speed and cut length repeatable. Weld fusion sits on the equipment side through power matching, alignment and squeeze; strip quality and operation sit with the buyer.
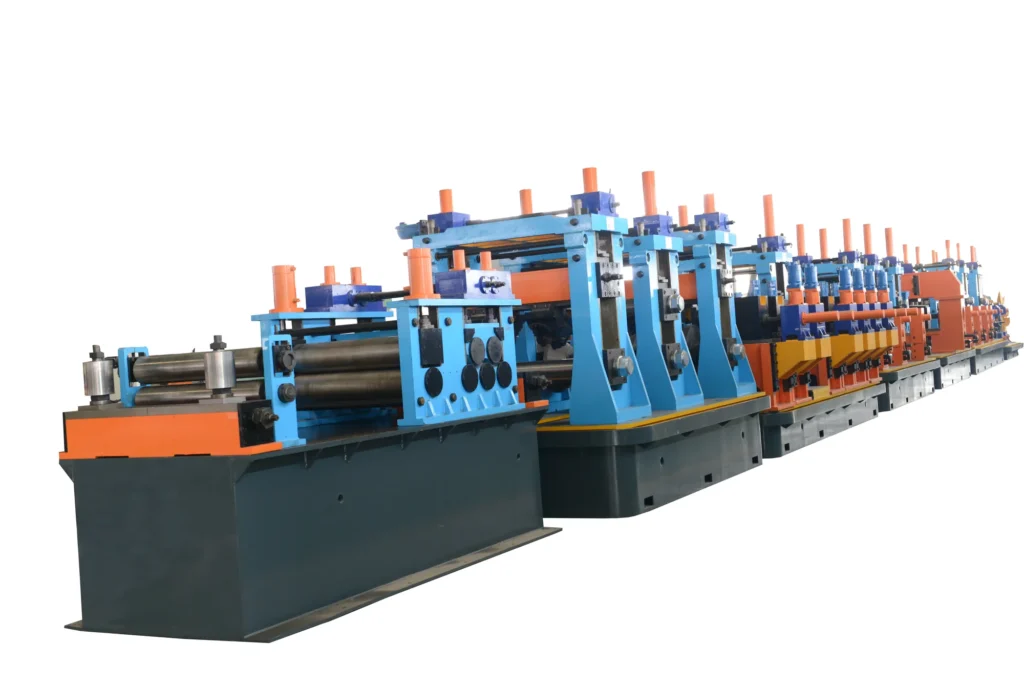
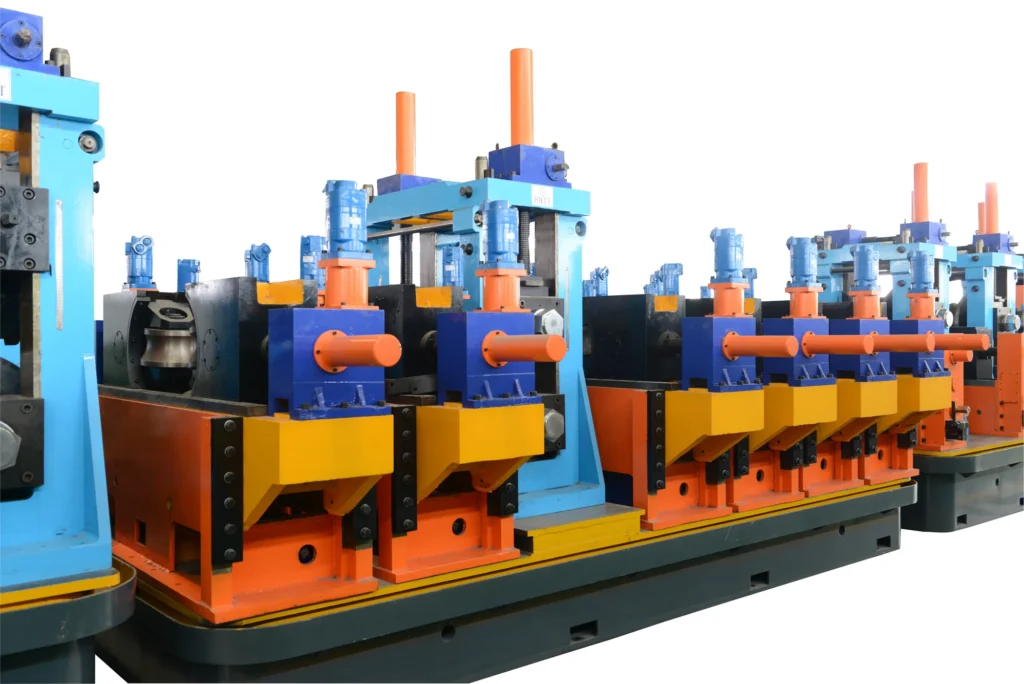
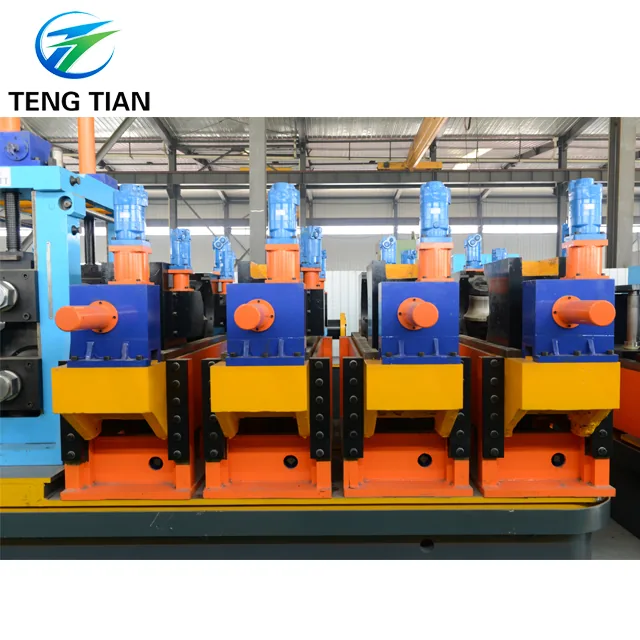
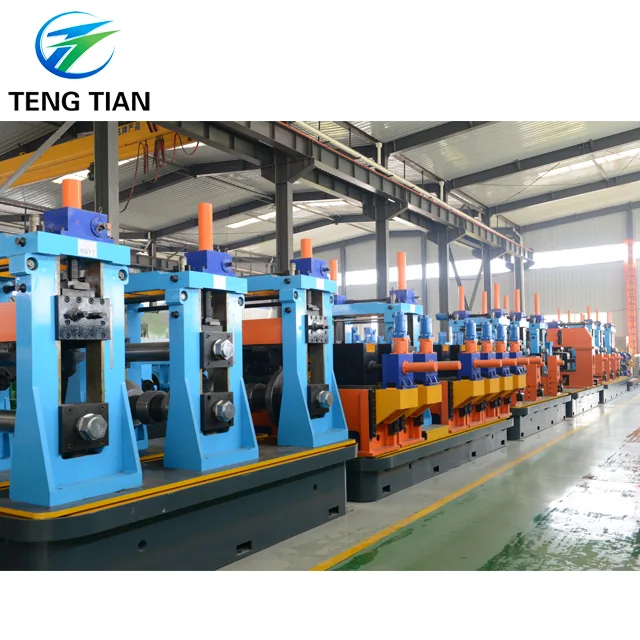
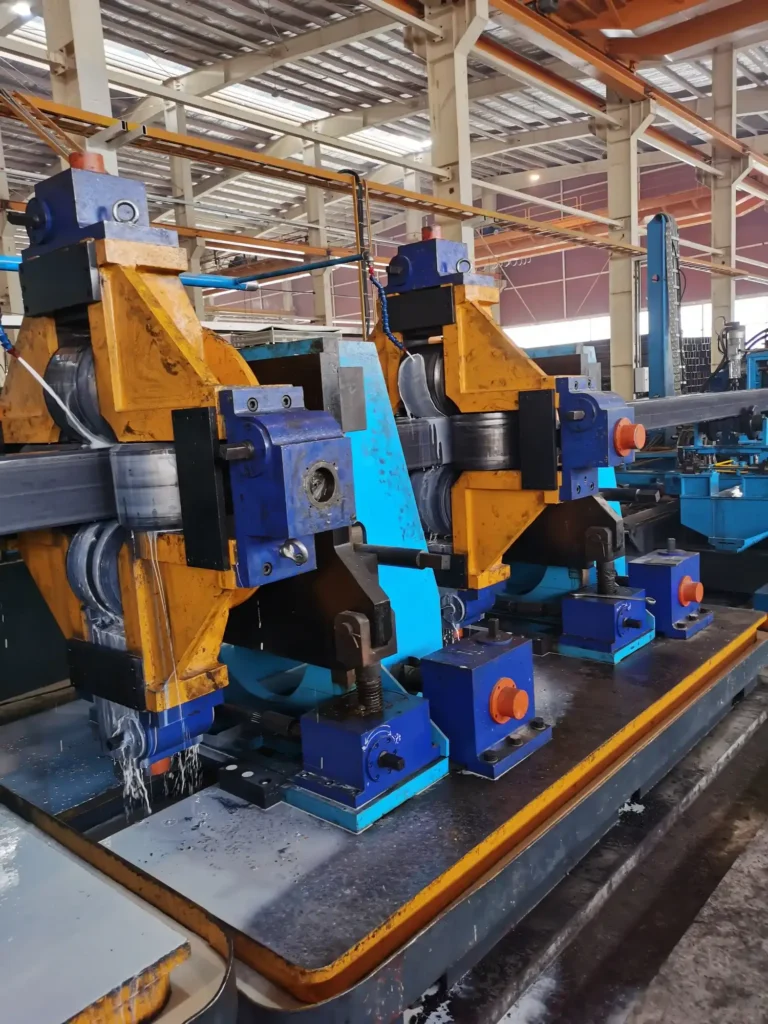
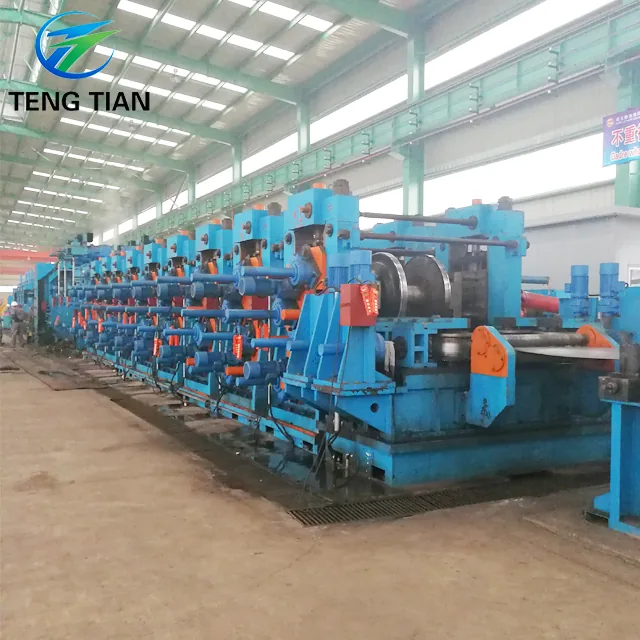
Line Photos from the Works
Three photographs of this line, taken in our own workshop. Click any photo for the full-size image.
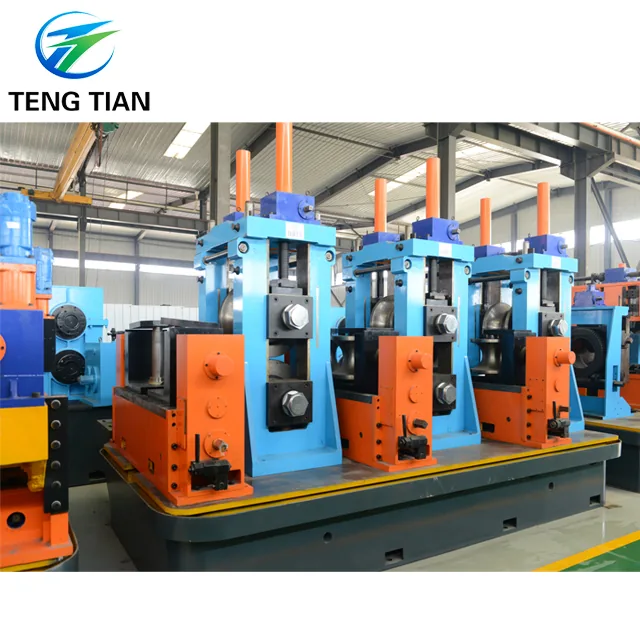
More from this line
 HG165
 HG219
 HG325
 HG426
Send Your Enquiry
Tell us the pipe outside-diameter range, the wall thickness and the output you need. An engineer reads every enquiry — it does not land in a general sales inbox.