
 Scan on WeChat
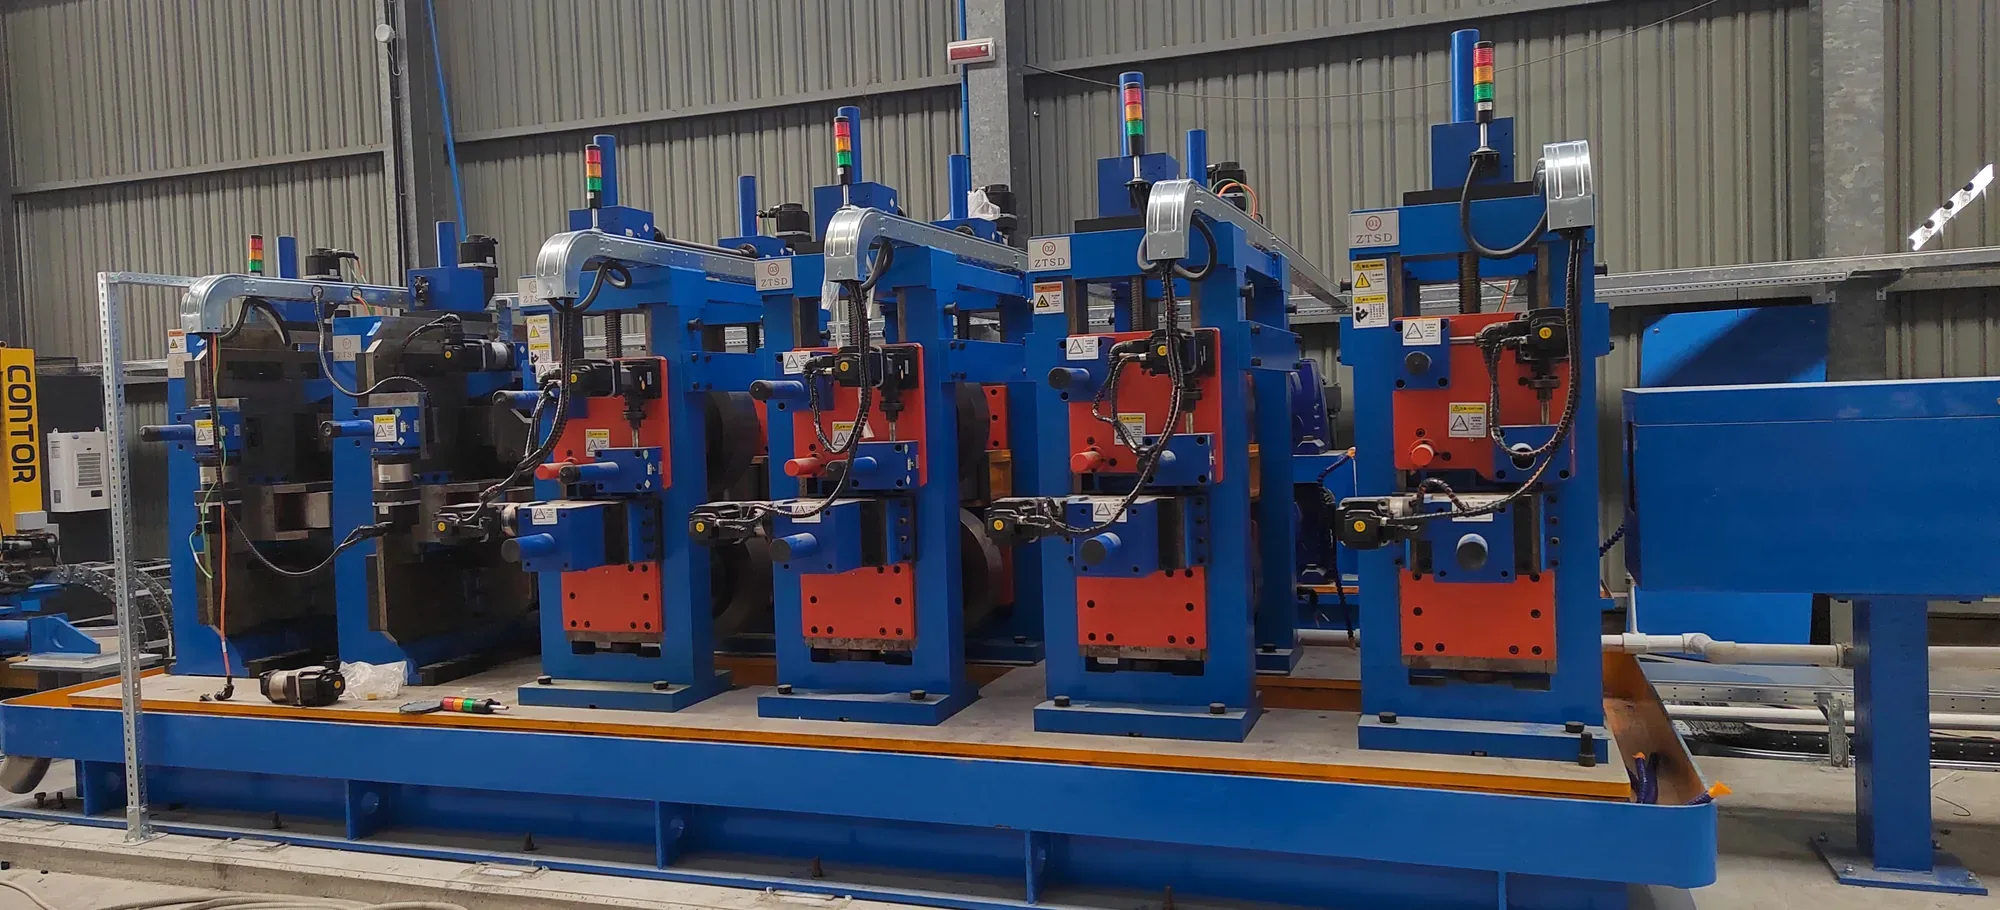
Tube Mill & Welded Pipe Production Lines
Twelve model steps, HG32 to HG630 — round, square and rectangular straight-seam welded pipe.
In This Line
Model Steps
Quick Contact
Hebei TengtianYuanle@tentubemill.com
+86-311-83025332
WhatsApp +852 5425 3155
This range covers the welded pipe production lines: continuous mills that take a steel coil in at one end and deliver straight-seam welded pipe at the other.Twelve model steps run from HG32 to HG630, covering finished outside diameters from Φ10 to Φ630 mm with wall 0.5 to 16 mm.
More from this line
More on this line — specifications, model steps and shop-floor photographs.
 PLC Automatic Tube Mill for Round and Square PipeAutomation is a grade of the same HG mill, not a different machine.See the line →
 Tube Mill Machine for Steel Pipe ProductionOne continuous train: coil in at one end, cut-to-length welded pipe off the other.See the line →
 Tube Mill Output, Material Yield and Roll-Change CostLine design supports a material yield of not less than 93 per cent.See the line →
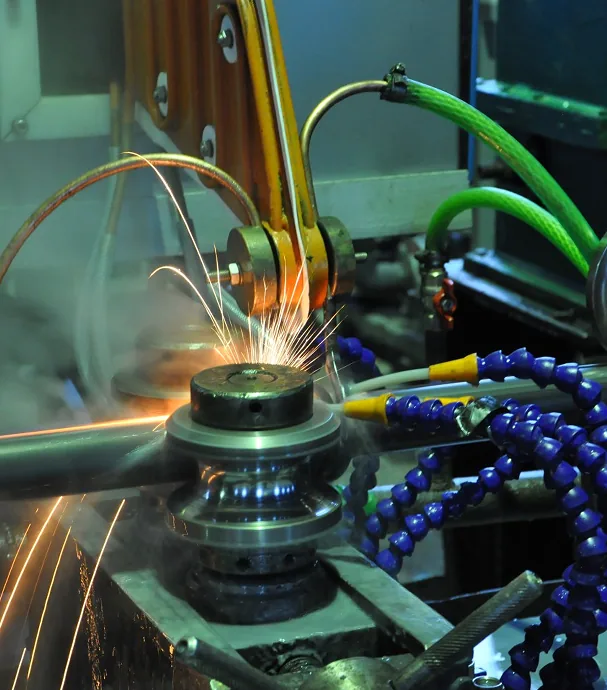 What Is an ERW Tube MillUncoil, roll form, high-frequency induction weld, size, cut.See the line →
What Is a Tube Mill?
What it solves is a capacity question rather than a part question: a plant that wants to build or expand pipe-making capacity needs a line that runs without stopping between coils, covers several specifications without a rebuild, holds yield and weld quality steady, and changes size quickly.
How it compares with the alternatives.Compared with seamless rolling or UOE/JCOE, high-frequency welding has lower investment and running cost and higher continuity, which suits medium and small diameters in volume. Compared with spiral submerged-arc welding, it is faster, straight-seam, and suited to structural and general fluid pipe.
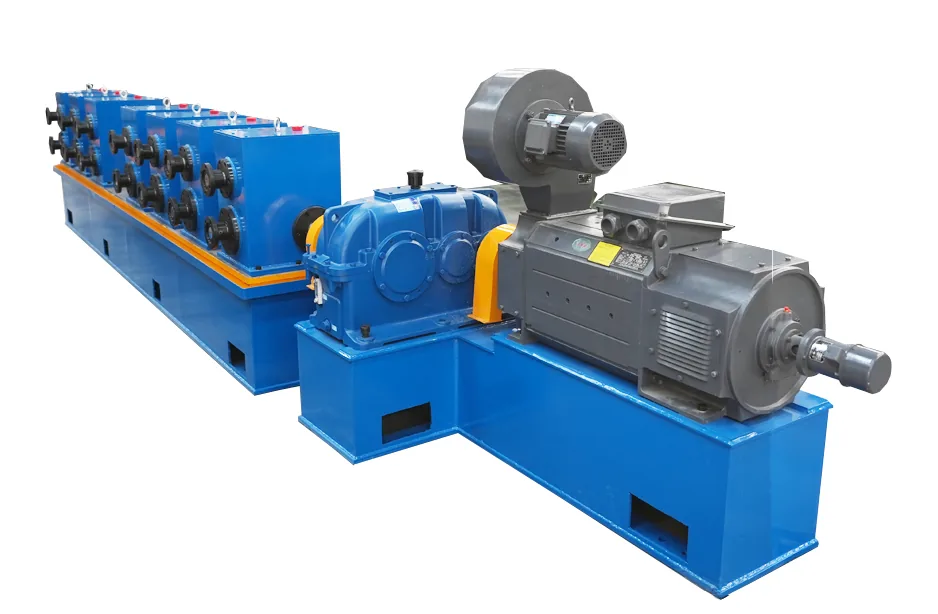
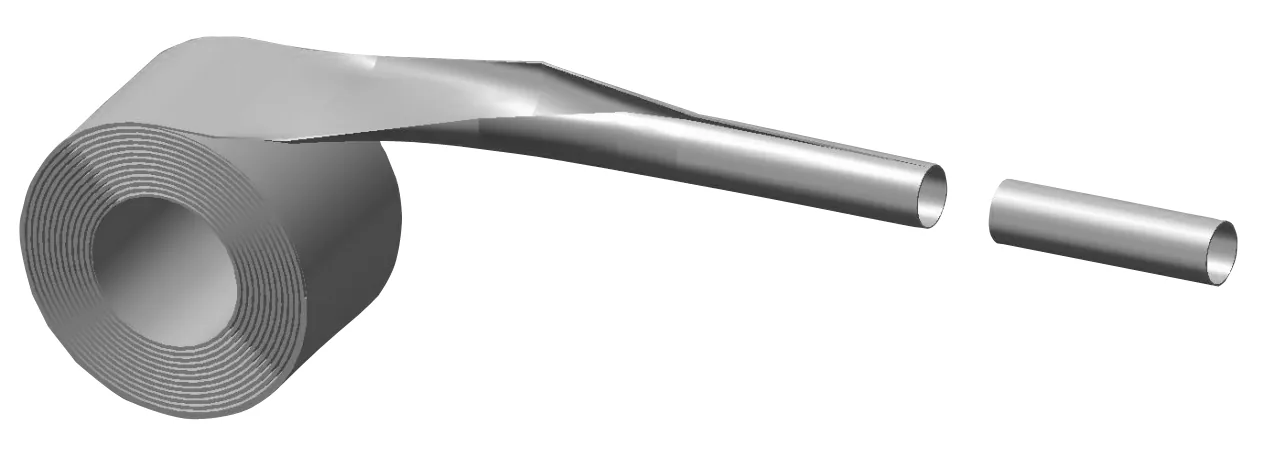
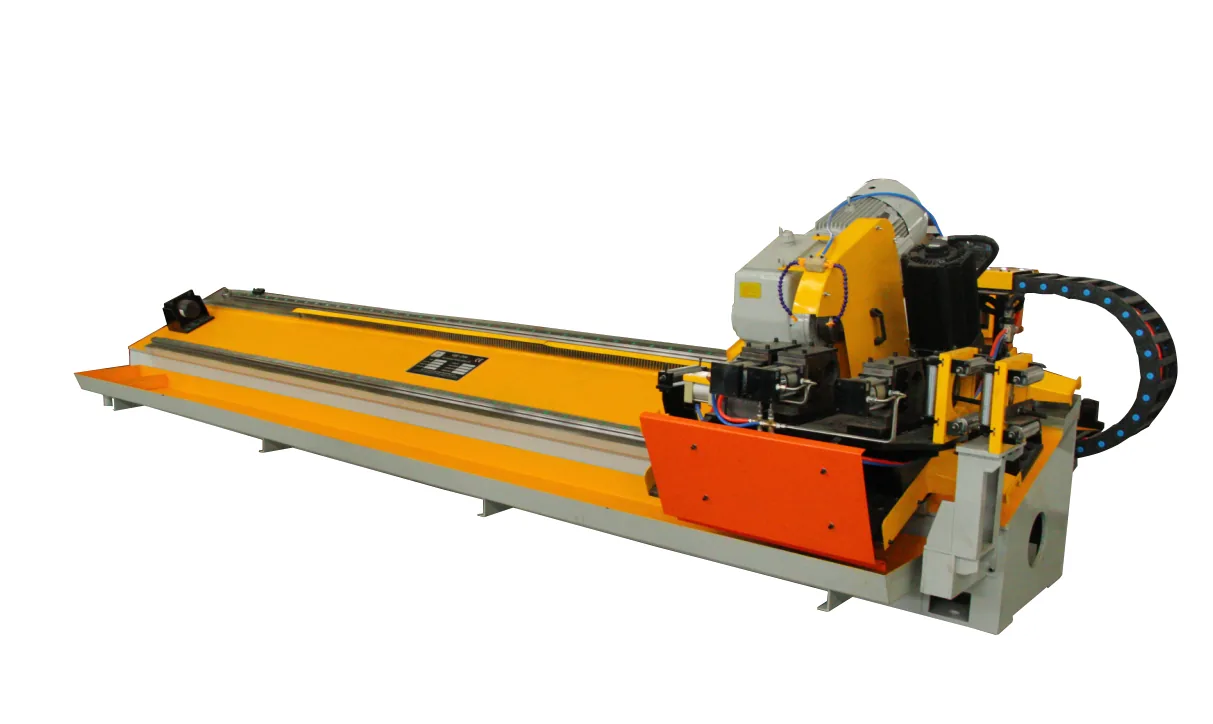
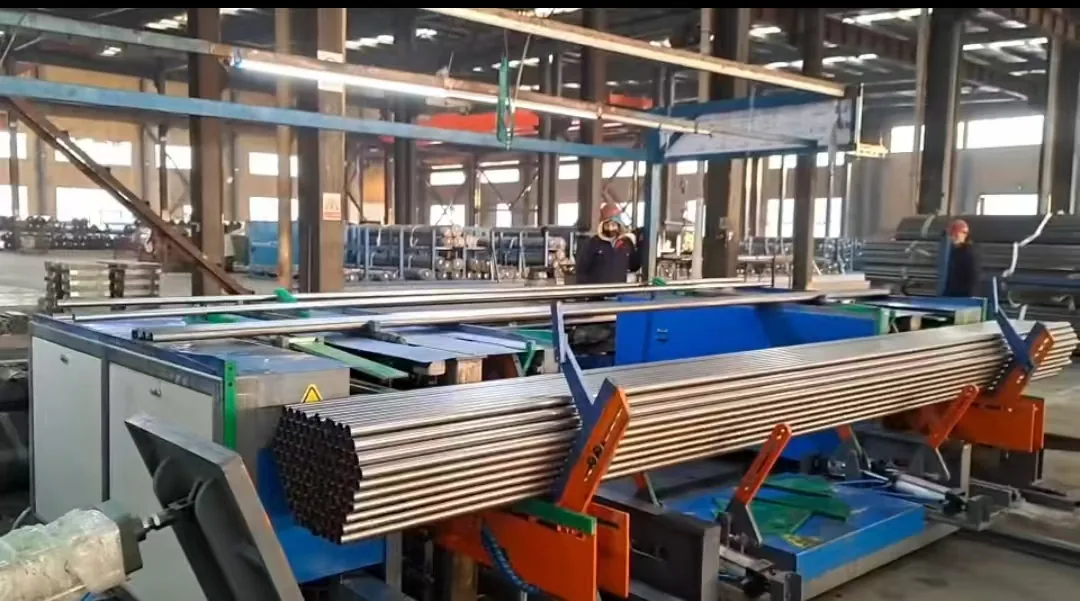
A tube mill is a complete continuous forming, welding and sizing plant.Coil is uncoiled, rolled progressively into shape, welded along the seam by high-frequency induction, sized, and cut to length — producing round, square and rectangular straight-seam welded pipe.
Tube Mill & Welded Pipe Production Line — Range, Configuration and Output
The twelve steps are the selection axis buyers actually use, and they are step by step: Φ10–32, 16–50.8, 12.7–76, 32–89, 45–114, 60–165, 114–219, 114–273, 165–325, 165–426, 219–508 and 325–630 mm.
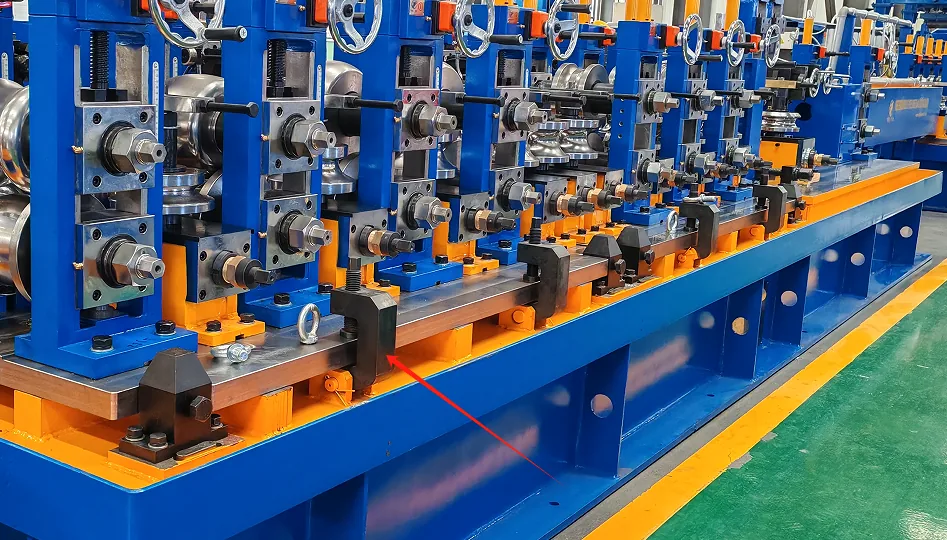
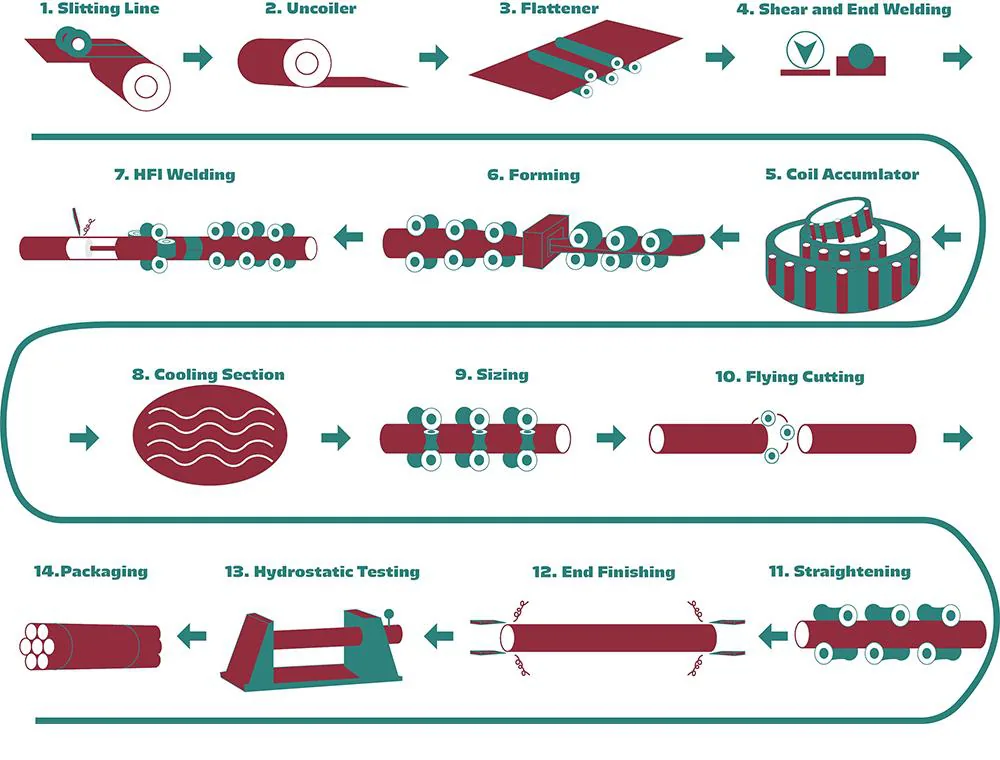
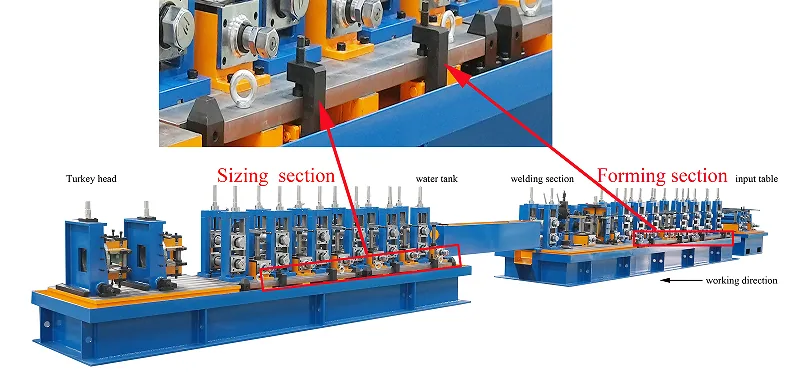
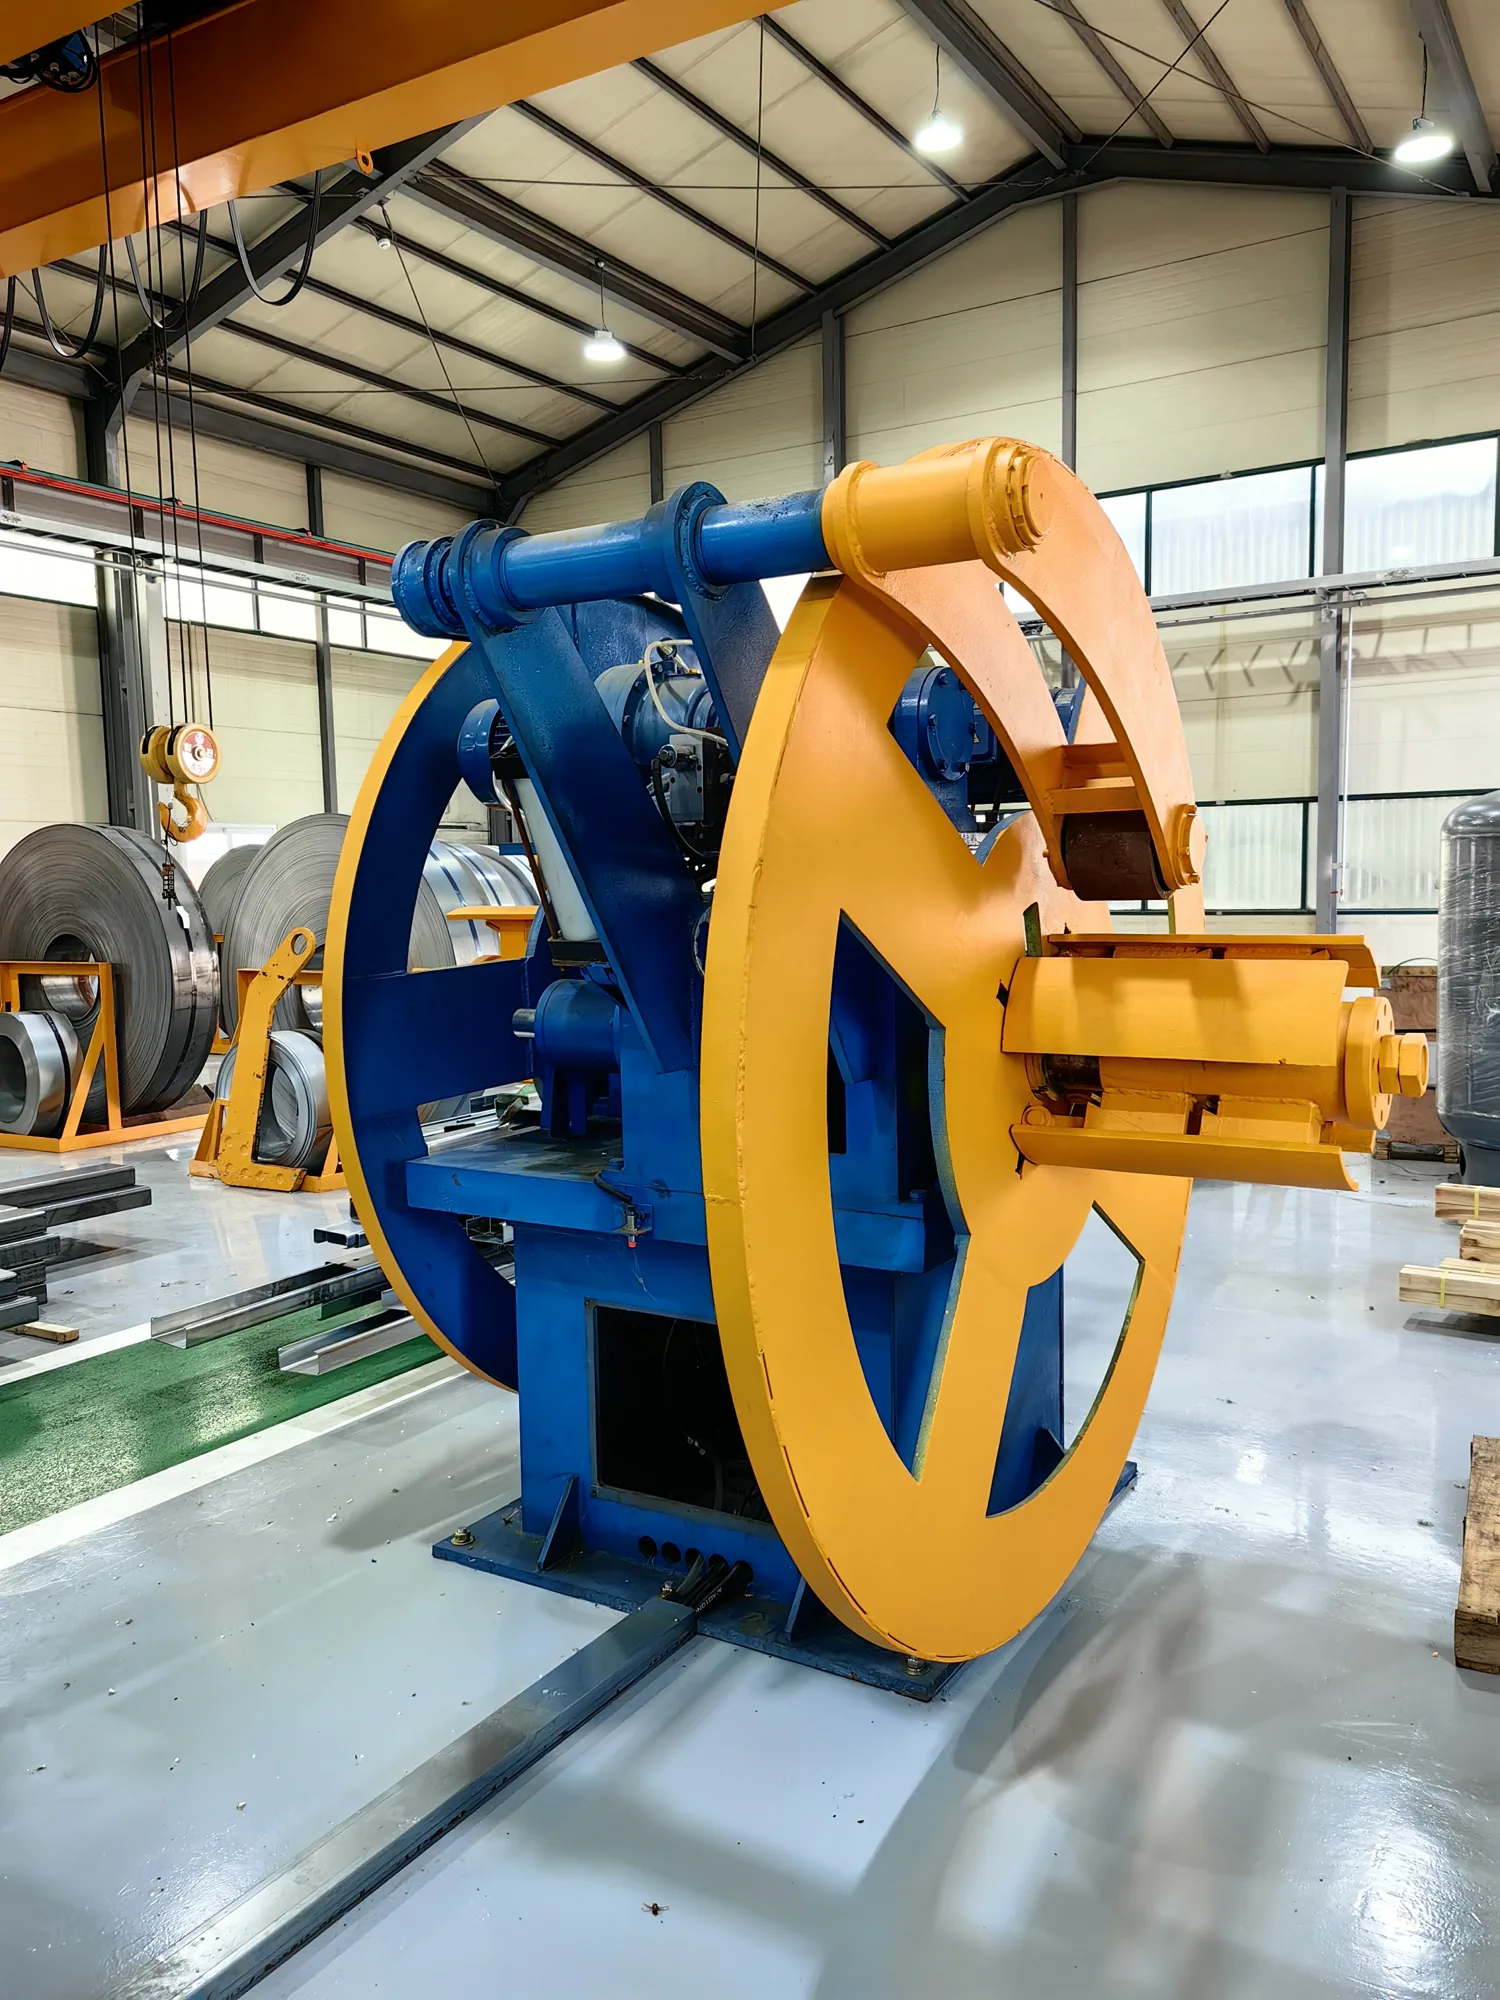
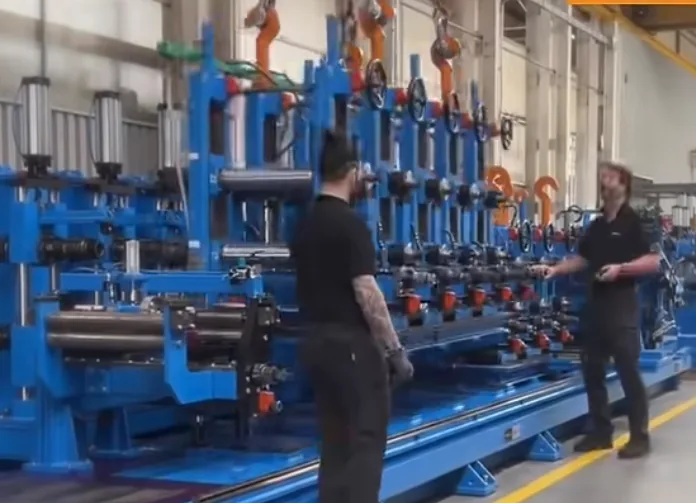
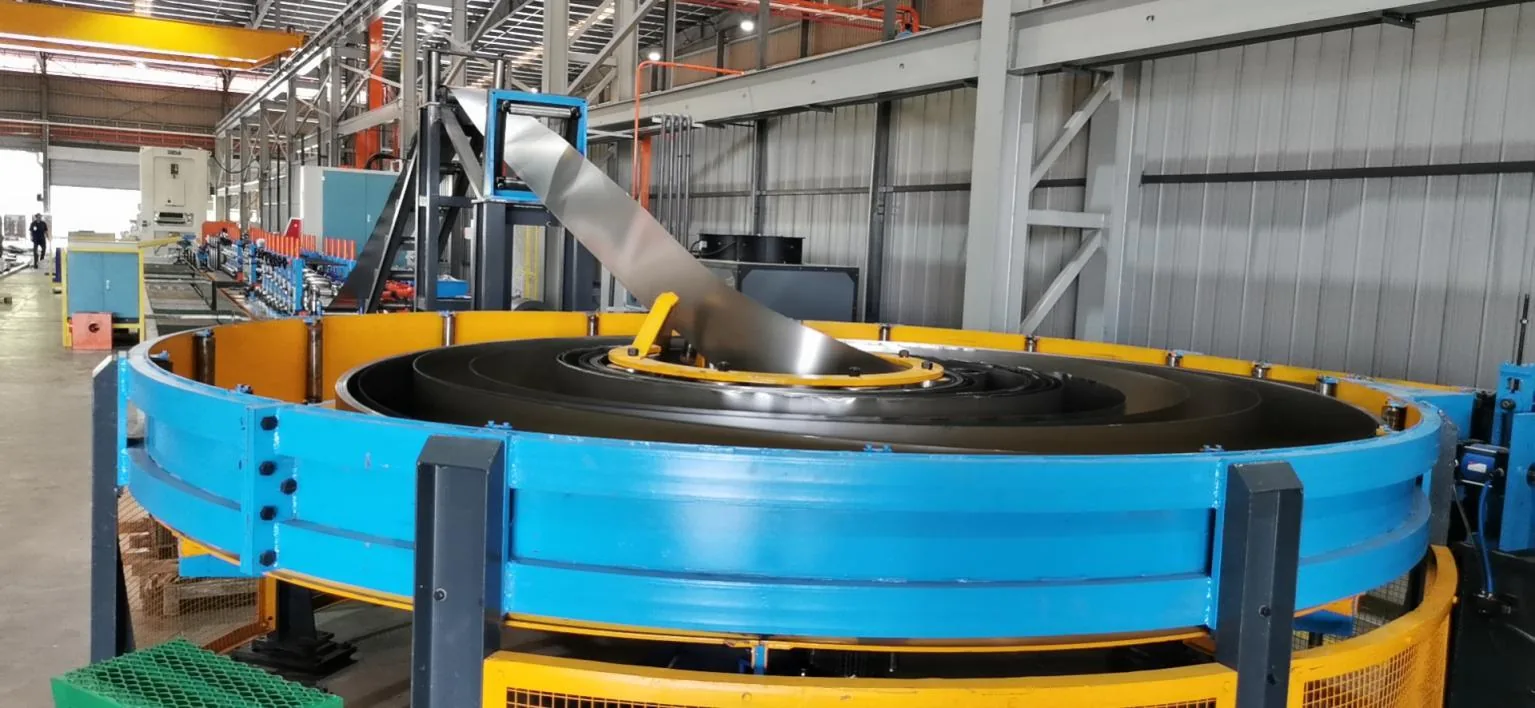
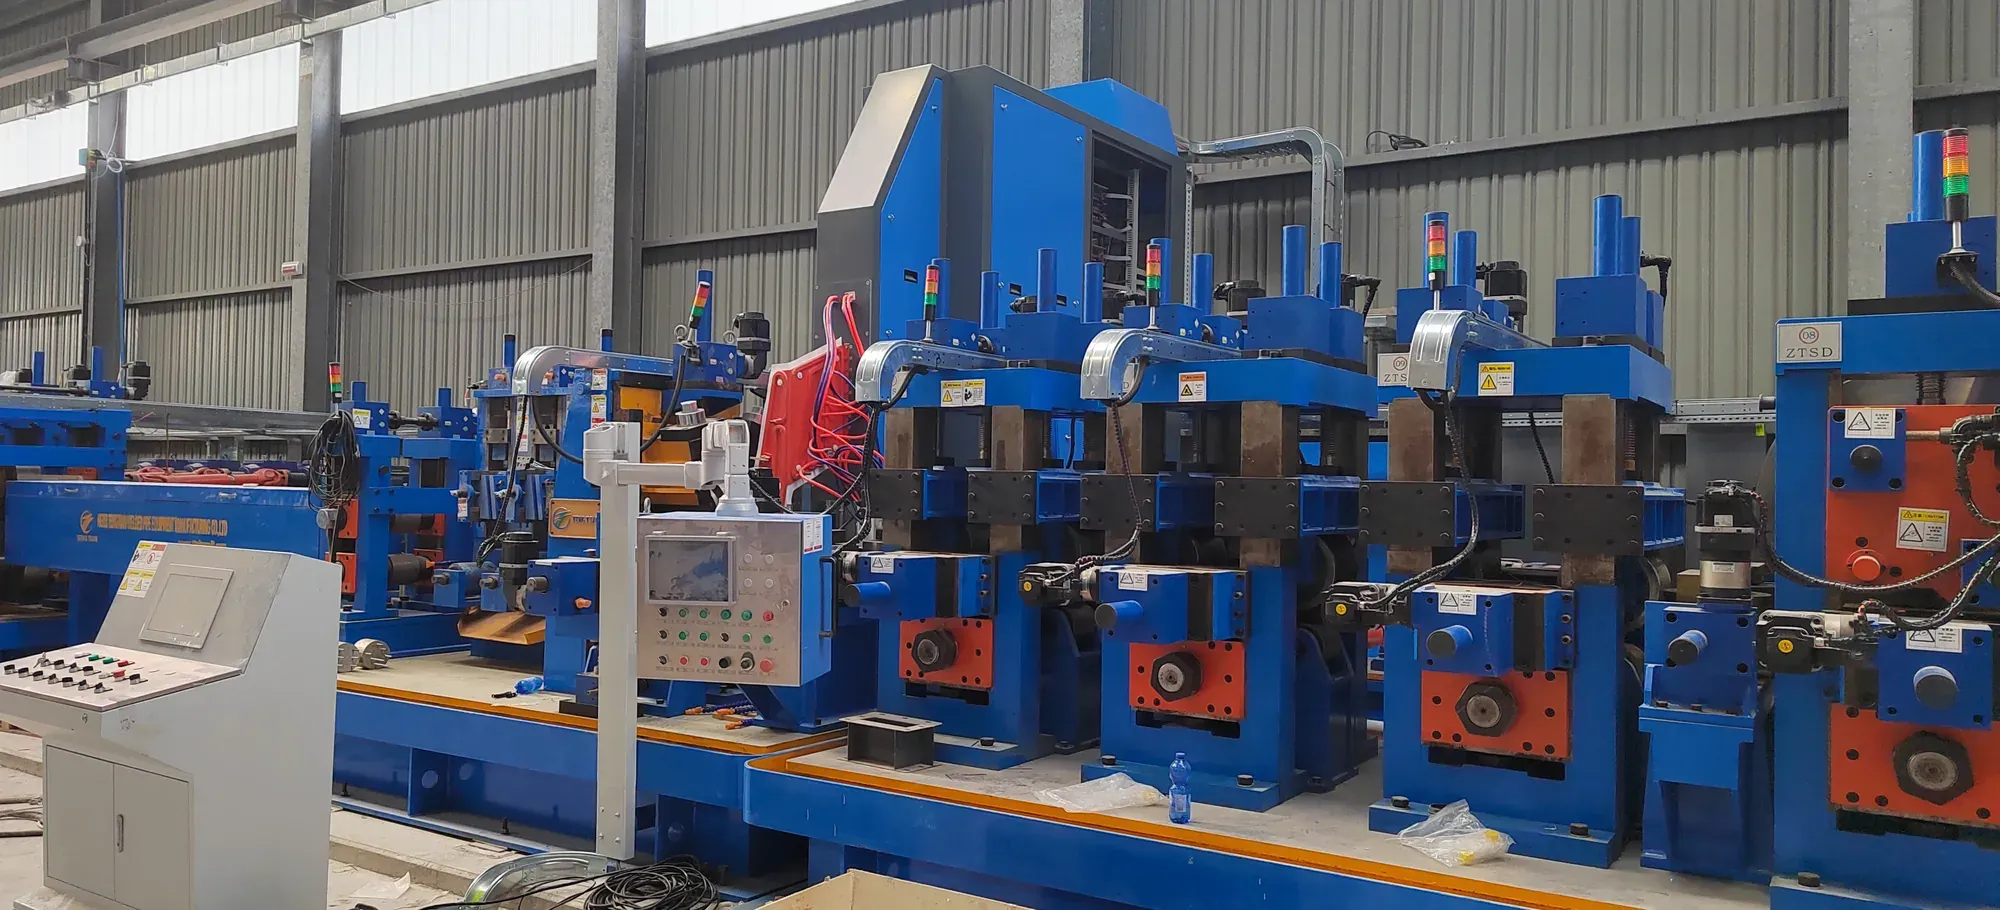
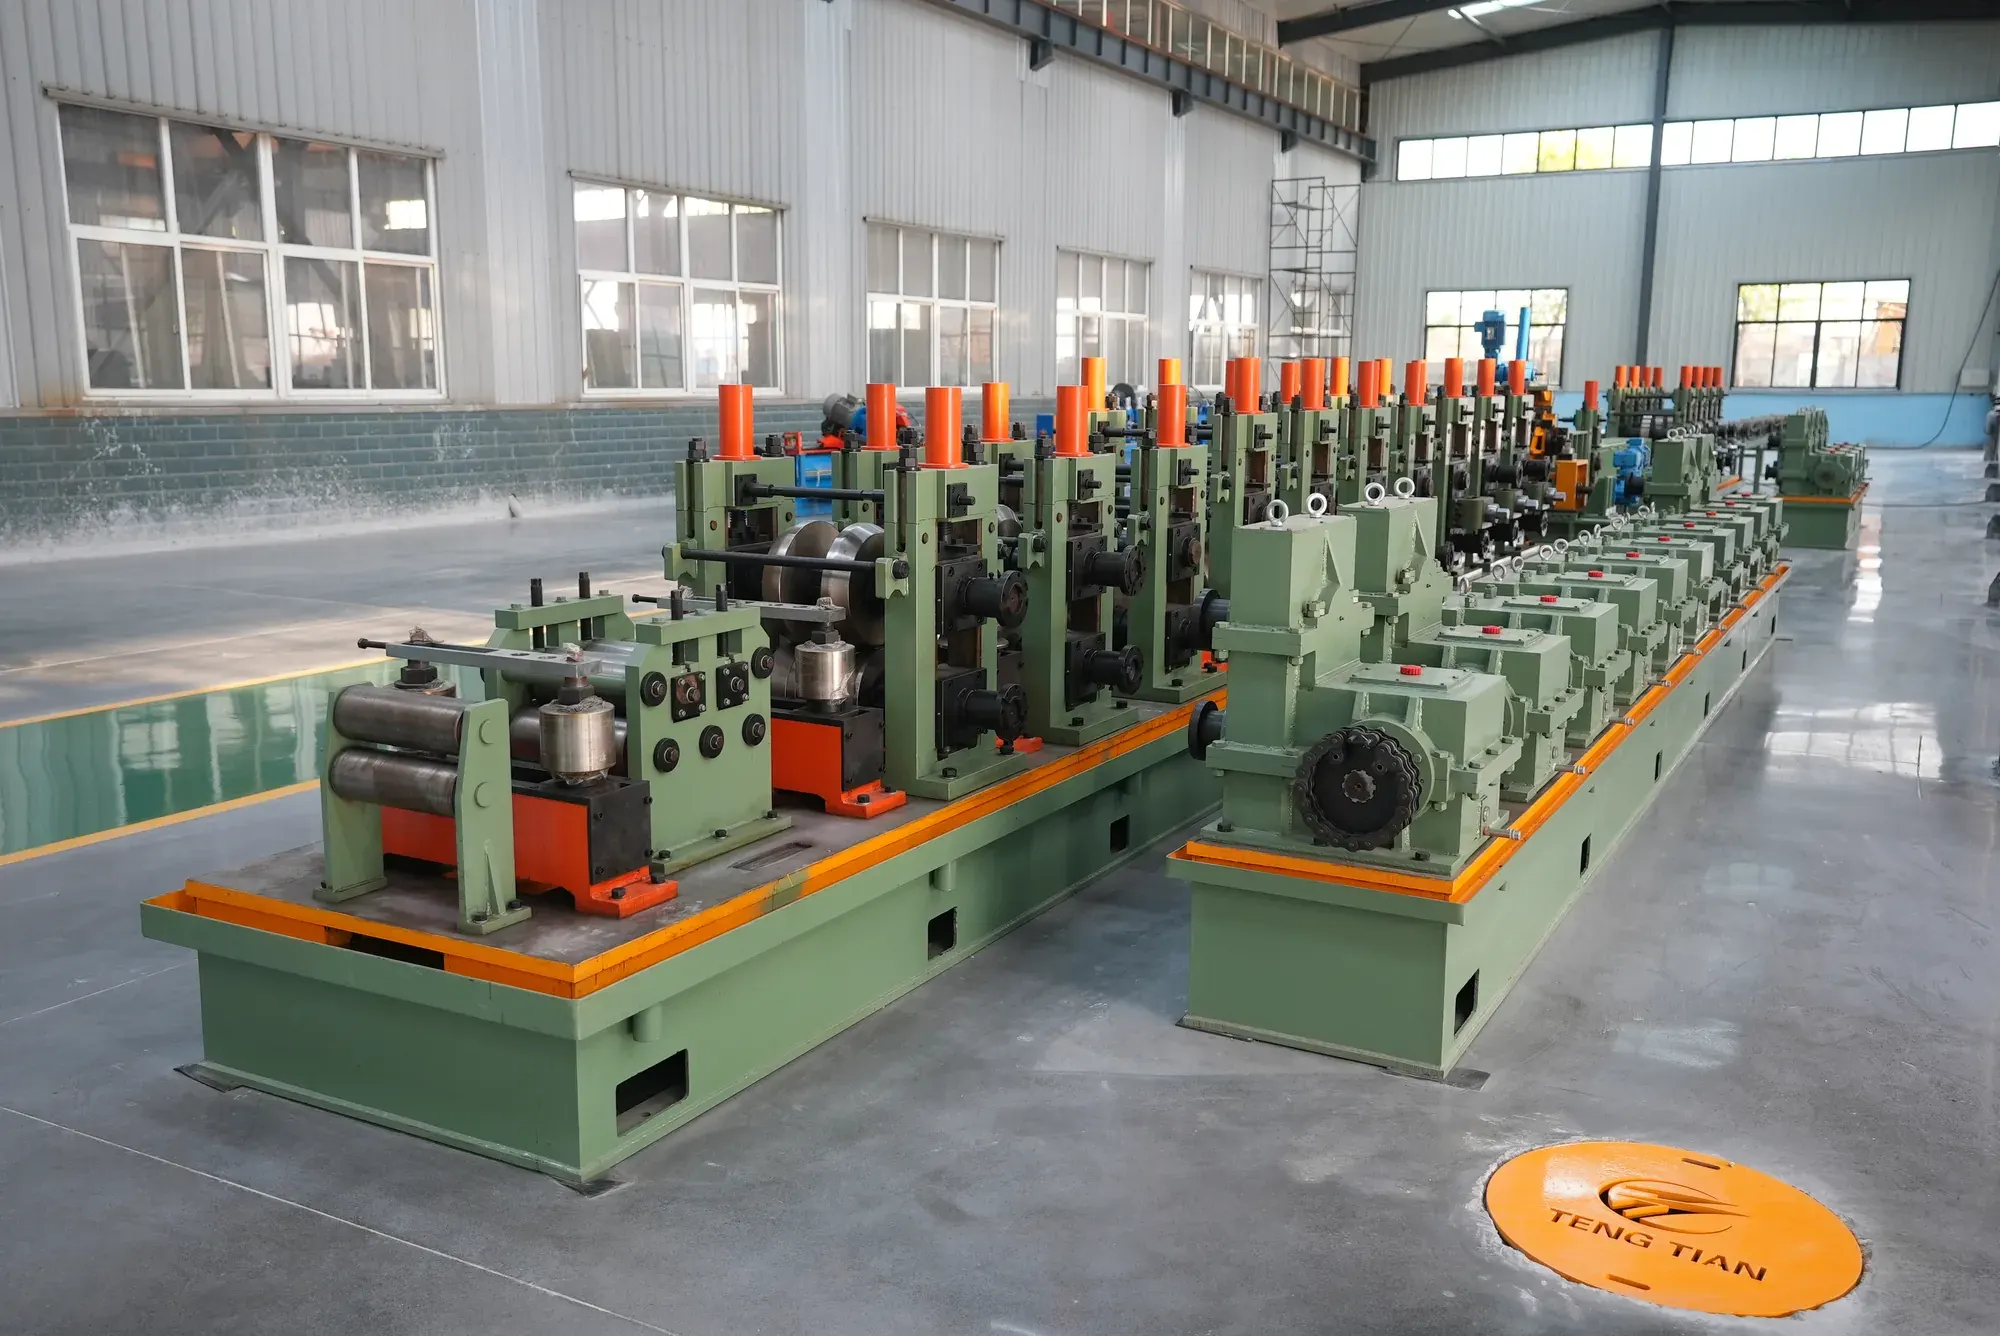
Every step runs the same eight units: expanding-mandrel uncoiler, five-roller leveller, automatic shear-welder, spiral accumulator, forming and sizing mill, HF induction welder, flying saw, and PLC with variable-frequency control.
Two of those units exist purely so the mill does not stop.The shear-welder joins the tail of one coil to the head of the next; the spiral accumulator stores strip while that join is made. Together they are what “non-stop running” means on this line, and they are the reason a coil change is not a production stop.
Key Parameters: Size Range, Wall Thickness, Line Speed and Welder Power Band
- Outside diameter across the series: Φ10–630 mm.
- Wall thickness across the series: 0.5–16 mm.
- Welder power: matched to the pipe range, 150 kW to 1500 kW by step.
- Material yield: line design supports above 93 per cent.
Line speed and shift output per step: available on request.
Automation is a grade rather than a separate machine: semi-automatic or full PLC control, with the full-automatic tube mill sitting as the high-automation grade of the same series.
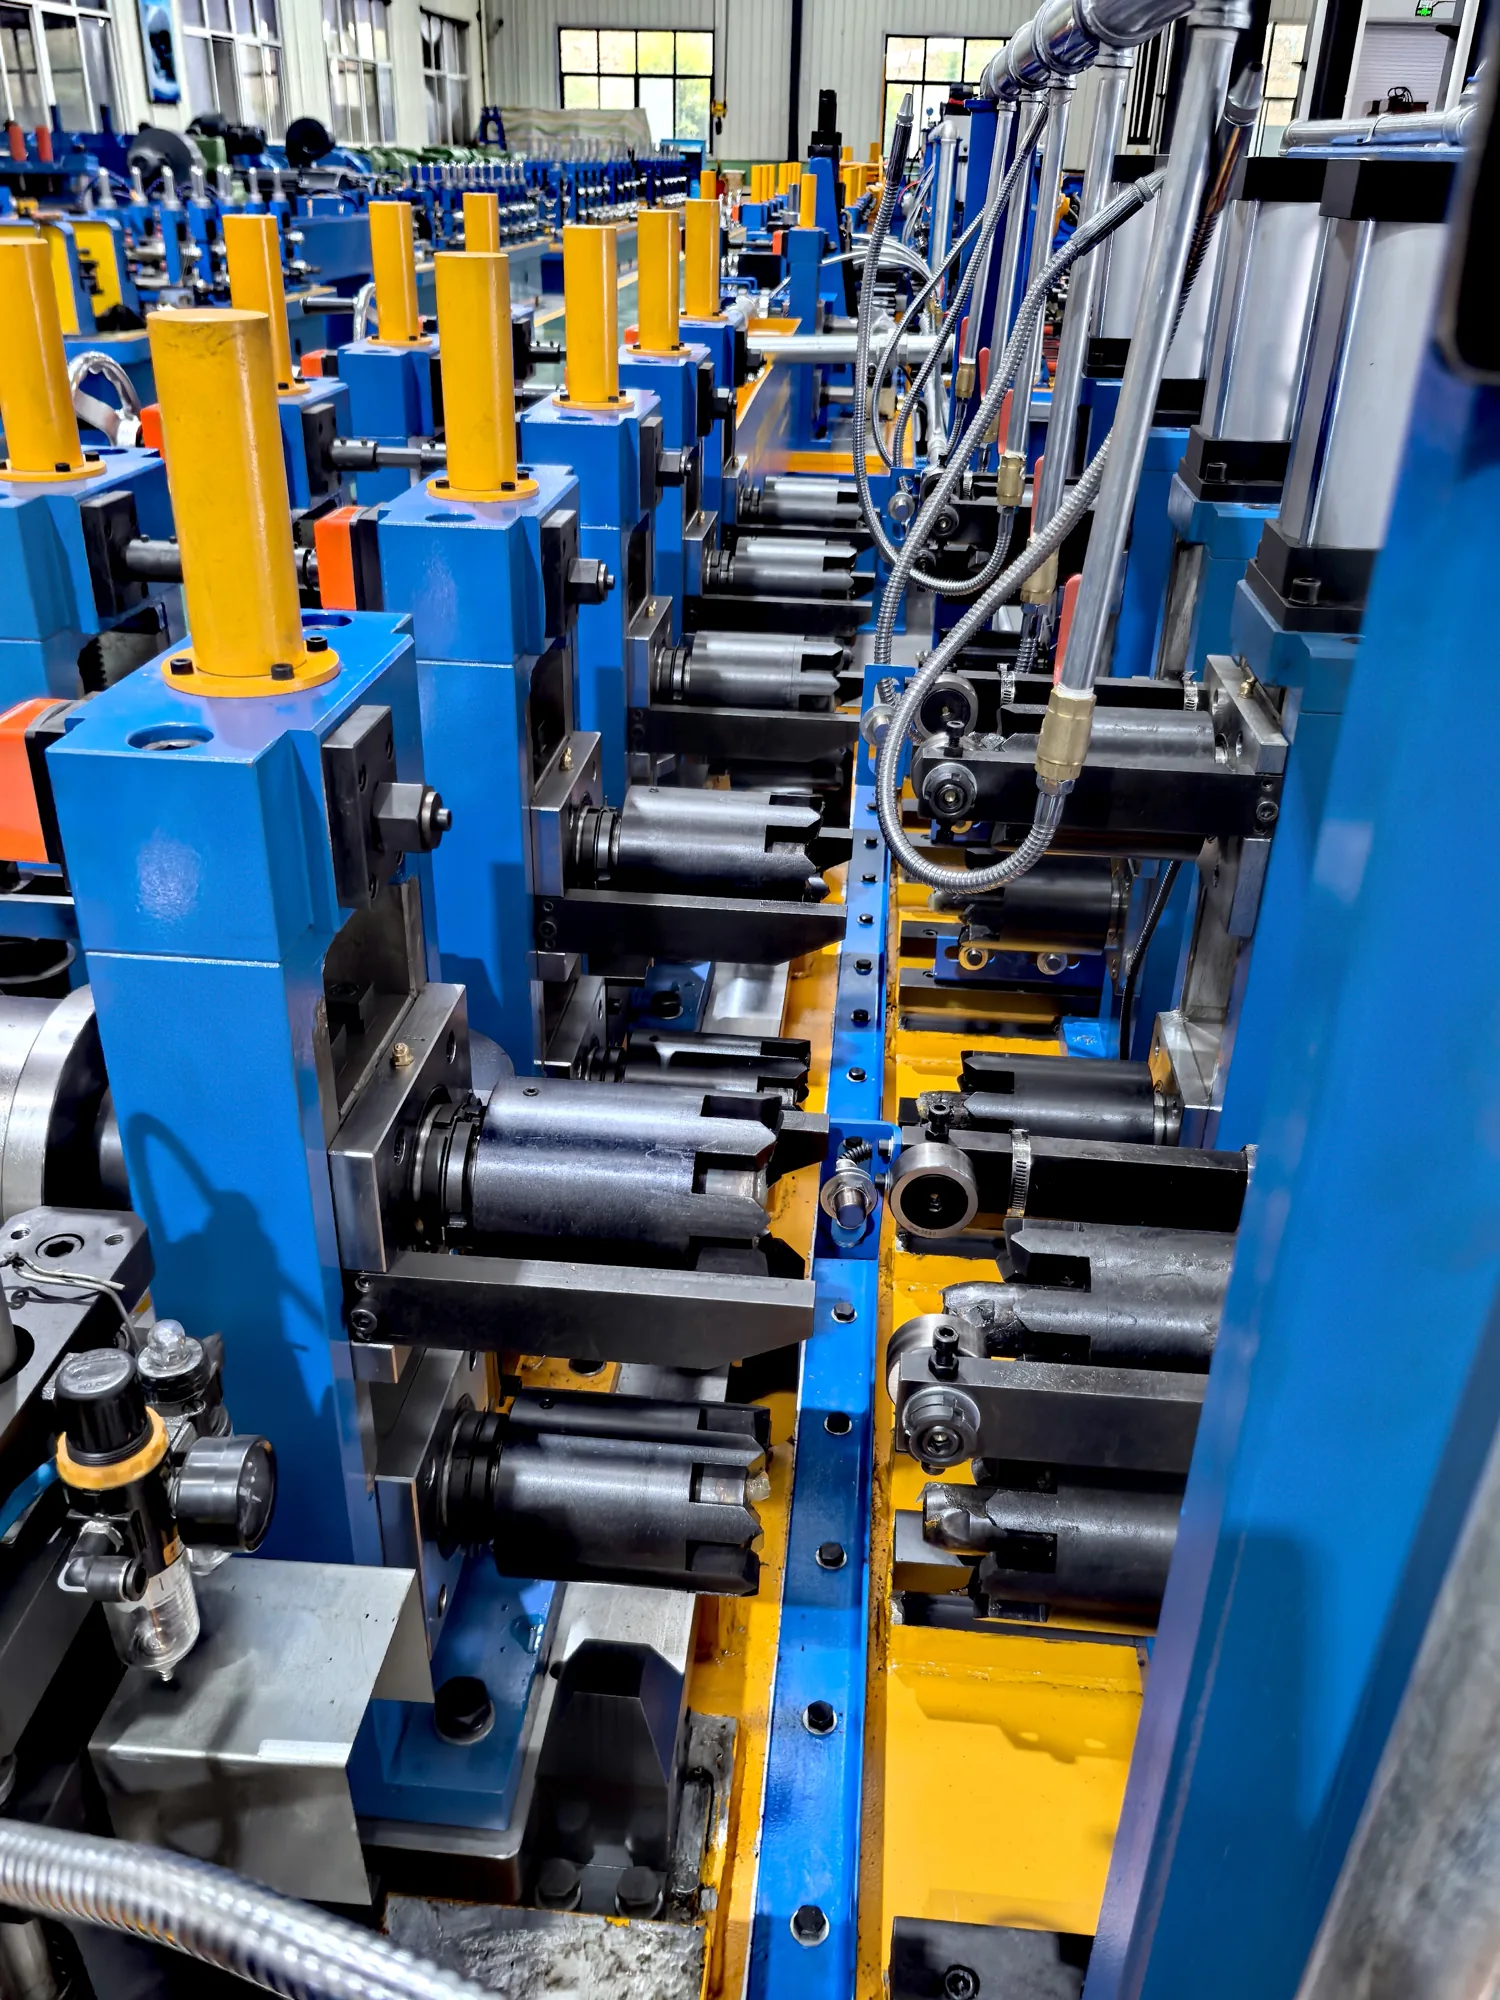
Forming on these lines uses the W, FFX and FF forming methods.The roll pass is designed in the German COPRA roll-forming design software, which serves both as the design guide for the roll means and as the final verification before the rolls are cut.
Model Specifications
| Model | Outside diameter | Wall thickness | Square section | HF welder |
|---|---|---|---|---|
| HG32 | Φ10 – 32 mm | 0.5 – 1.5 mm | 10×10 – 20×20 mm | 150 kW |
| HG50 | Φ16 – 50.8 mm | 0.8 – 2.0 mm | 12×12 – 40×40 mm | 200 kW |
| HG76 | Φ12.7 – 76 mm | 1.5 – 3.0 mm | 10×10 – 60×60 mm | 250 kW |
| HG89 | Φ32 – 89 mm | 1.0 – 4.0 mm | 25×25 – 70×70 mm | 300 kW |
| HG114 | Φ45 – 114 mm | 1.5 – 5.0 mm | 35×35 – 90×90 mm | 300 kW |
| HG165 | Φ60 – 165 mm | 3.0 – 7.0 mm | 50×50 – 130×130 mm | 400 kW |
| HG219 | Φ114 – 219 mm | 4.0 – 8.0 mm | 90×90 – 170×170 mm | 500 kW |
| HG273 | Φ114 – 273 mm | 4.0 – 10.0 mm | 90×90 – 215×215 mm | 600 kW |
| HG325 | Φ165 – 325 mm | 4.0 – 10.0 mm | 130×130 – 250×250 mm | 600 kW |
| HG426 | Φ165 – 426 mm | 4.0 – 10.0 mm | 130×130 – 330×330 mm | 800 kW |
| HG508 | Φ219 – 508 mm | 4.0 – 16.0 mm | 170×170 – 400×400 mm | 1000 kW |
| HG630 | Φ325 – 630 mm | 4.0 – 16.0 mm | 250×250 – 500×500 mm | 1500 kW |
How to Choose the Right Model
Start from the largest finished outside diameter you need and read it against the twelve steps — that is the axis the series is built on.
Then three questions narrow it further.What section do you need: round only, or square and rectangular as well, since most steps run all three. How often do you change size, because that decides whether a conventional roll-forming step or the direct-forming square line fits your schedule.
And does the pipe need in-line non-destructive testing, because that is the API line — a separate configuration built on the tube mill with intermediate annealing, straightening, end facing, hydrostatic testing, ultrasonic and eddy-current inspection added.
Scope of Supply, Installation and Commissioning
Whether the equipment can meet a required standard such as API 5L or GOST — answered by showing the API line’s inspection chain and the GOST H-beam capability, as equipment capability.Export packing is specified per item: control cabinets, impeders and induction coils, forming rolls and cutting tools travel in moisture-protected wooden cases with a spare-parts pack, while heavy large-diameter frames ship bare, braced on cradles with designated lifting points and rust protection.
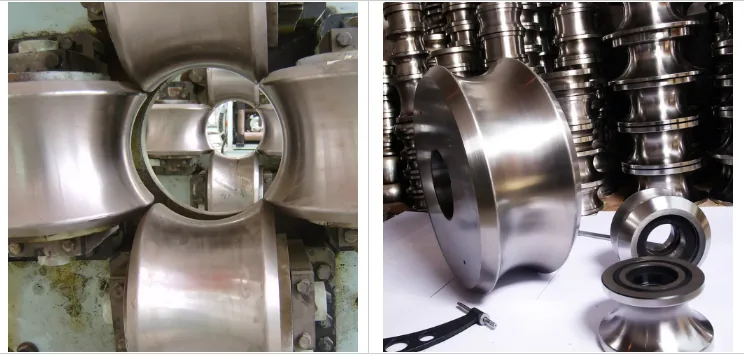
Forming rolls and key wear parts are machined in-house on our own CNC equipment — the reason spare rolls stay available years after handover.Wear items are supplied continuously: saw blades and cutting tools by cutting volume, impeders and induction coils by welding hours. Cooling medium and hydraulic oil are specified by us and sourced locally by the plant.
The engineering team is twenty people averaging twenty years’ experience and the production base is open to factory audit.
Who buys a tube mill, and what they check
Six buyer profiles read the same specification sheet differently.
Distributors and resellers work a region on turnover: their criteria are price competitiveness, lead time and whether the manufacturer can backstop after-sales for their own downstream customers.Regional agents work on long-term margin and punctuality: their criteria are on-time delivery, manufacturer responsiveness and technical support.
System integrators build whole plants for end users: their criteria are full-plant customisation, on-site presence and end-to-end cooperation.
On the end-user side, large energy and infrastructure groups are gated on standards compliance, delivery date and long-term service.Regional pipe and section makers are gated on payback, changeover efficiency, yield and energy. Auto-parts and new-energy manufacturers are gated on dimensional accuracy, stability and technical response time.
Common Objections, Answered
Buyers raise seven common concerns; four apply to this range. The standards question is answered above, and the other three below.
Whether after-sales and spare parts from a Chinese supplier will keep up — answered by in-house CNC roll machining, direct spare-parts shipment and on-site engineer dispatch.
Whether a size change means a long stoppage — answered honestly by separating the two forming routes: conventional roll forming needs a roll change; direct forming square does not.Whether delivery and capacity are secure on a large investment — answered with the stated 50 to 90 day delivery and plant-level customisation from an owned manufacturing base.
When Buyers Switch Lines
Purchase triggers: a new pipe or section plant buying a first line; capacity expansion or automation upgrade; entering a new product type such as square tube, API line pipe or H-beam; a large downstream order forcing fast capacity addition; and a distributor stocking a region.
Switching triggers: after-sales or spare-parts failure at the previous supplier; slow changeover and high roll cost; a new standard market such as API 5L or GOST; and unstable delivery or price rises.
Certification, and what each certificate actually covers
ISO 9001 is held under certificate number 18524Q11269R2S, issued by National Standard Integration (Beijing) Certification Co., Ltd. under IAF MLA and CNAS accreditation.
CE certificates are held from UDEM under three separate numbers, and each covers a different line type: welded pipe equipment under M.2022.206.C72171, cold roll forming equipment under M.2022.206.C72172, and slitting lines under M.2022.206.C72173. A fourth CE certificate for cold forming is held from Ente Certificazione Macchine in Italy under 0P250616.HTWTT37.
Each number can be checked at the issuing body rather than taken on trust, which is why we publish numbers and verification routes instead of certificate images.
An enterprise standard, Q/GYLTT01-2023 for HGF150 high-frequency welded pipe equipment, is published on the national enterprise-standard platform.High-Tech Enterprise certificate GR202413001148 is held. The Madrid international trademark for TENGTIAN is registered under number 1 707 606. The patent portfolio is 30 granted utility model patents, with 7 invention patents applied for.
Delivery, payment and after-sales
Lines are dismantled into units and shipped in containers: heavy frames braced bare on cradles with designated lifting points and rust protection, precision and wear items in moisture-protected wooden cases with a spare-parts pack.Delivery takes 50 to 90 days.
Installation and commissioning are part of the supply rather than a separate quotation, backed by on-site dispatch and round-the-clock online support.There is a single point of contact, with a response time of under one hour. Payment is staged — 30 per cent deposit, 70 per cent before shipment — with third-party escrow and multiple trade terms available.
Anonymised reference deliveries
Our lines are running in more than a dozen countries — mostly on construction tube, and also on fire-extinguisher tube, furniture tube and other sections. Delivery cards show region and model or size; commissioning dates are available on request.
The process chain, stage by stage
The line has eight stages. For each, we note whether it is a quality watershed and what goes wrong when it is set badly.
Uncoiling: a coil car feeds the coil, a pneumatic four-link expanding mandrel tensions it.Not a quality watershed — but poor centring or tension shows up later as strip wander. Head straightening and levelling: the coil head is flattened and a five-roller leveller makes the strip straight into the next stage.
This one is a watershed, because strip flatness is the precondition for forming quality.Shear and weld: irregular head and tail are cut off and the strip ends joined, so production does not stop between coils. A watershed, because a bad joint means a broken strip and scrap pipe at the junction.
Spiral accumulator: strip is stored between the shear-welder and the mill so the mill keeps feeding during the change.A watershed — it is the buffer the whole continuity claim rests on. Roll forming: rolls progressively bend the strip into shape. The decisive stage for shape and seam alignment.
High-frequency welding: current concentrates at the seam, heats the edges, squeeze rolls press them together.The decisive stage for fusion. Sizing and straightening: after cooling, the tube is sized and straightened to final dimension. The decisive stage for dimensional accuracy. Cutting: the flying saw cuts to length at speed. Not a watershed — an end stage.
Reading that list backwards is how a plant diagnoses: three of the eight are watersheds for different things, so a dimensional problem, a seam problem and a continuity problem have different places to look.
The Ten Quality Factors
Ten factors govern output quality, and they divide into four groups that a buyer can act on separately.
Material: incoming strip grade, thickness tolerance and flatness — checked on entry, but the strip itself is the buyer’s side.Tooling: roll material and heat treatment, which govern shape stability, and impeder and coil condition, which govern where the weld energy goes.
Process: HF power, frequency and welding speed; squeeze amount and seam alignment; sizing and straightening; post-weld cooling.People and control: PLC and servo stability, and operator setup at size change. Inspection: final inspection, with UT and eddy current on API lines specifically.
Service lives for wear items are available on request; unit-level scope of supply is available on request.
Tube Mills Running
Footage from lines built at our own works. Each clip opens on our YouTube channel.


From the Workshop
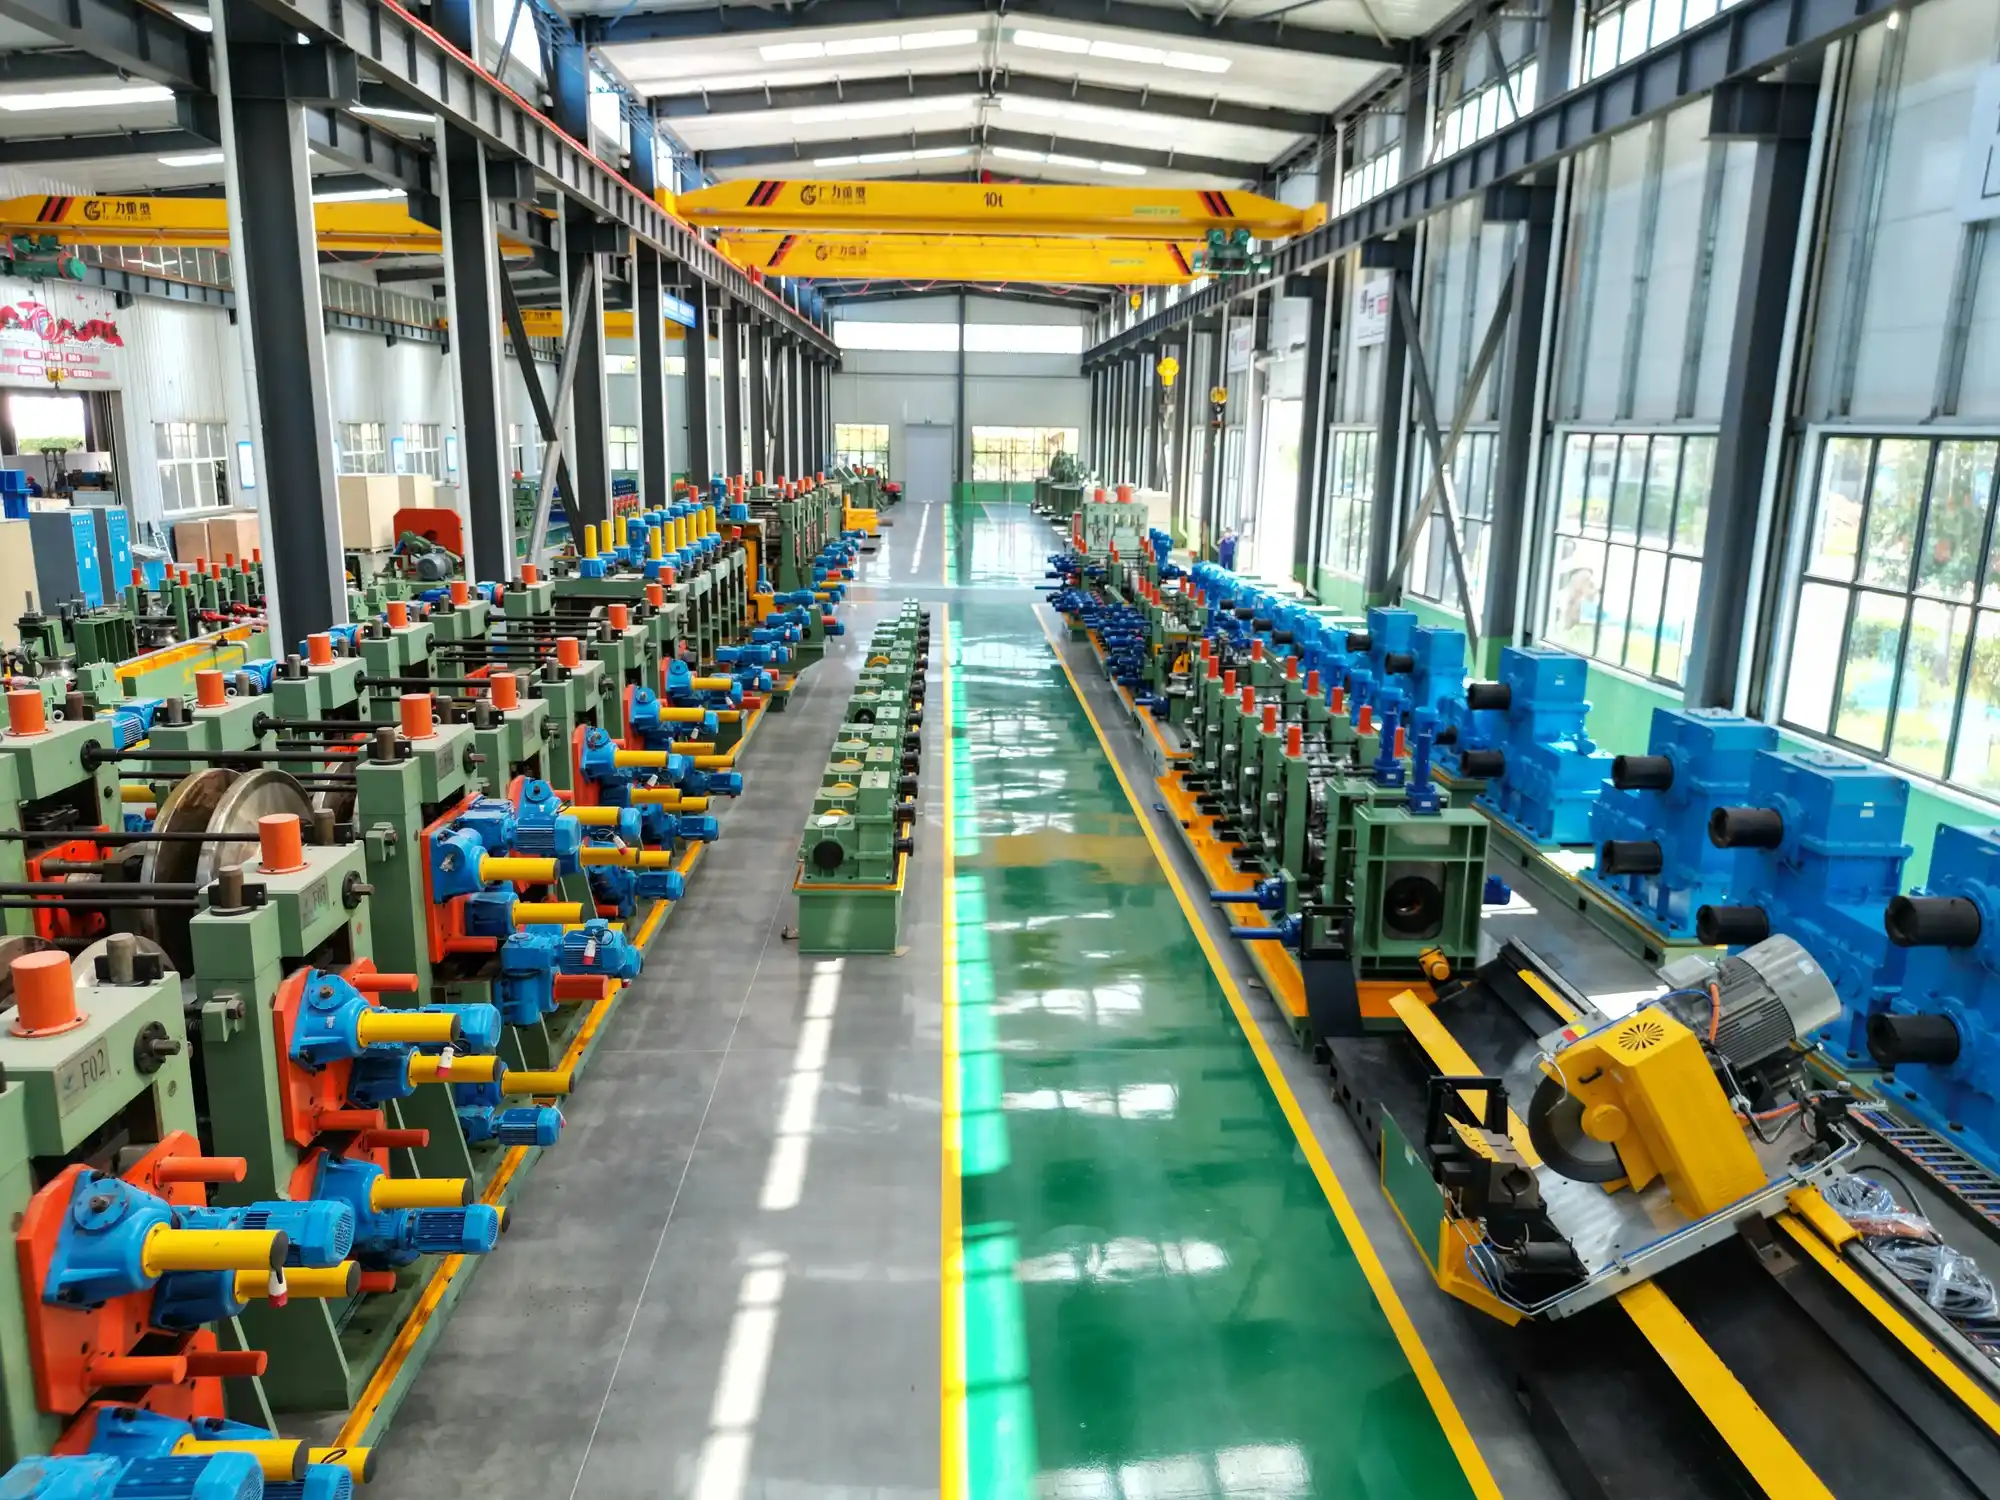
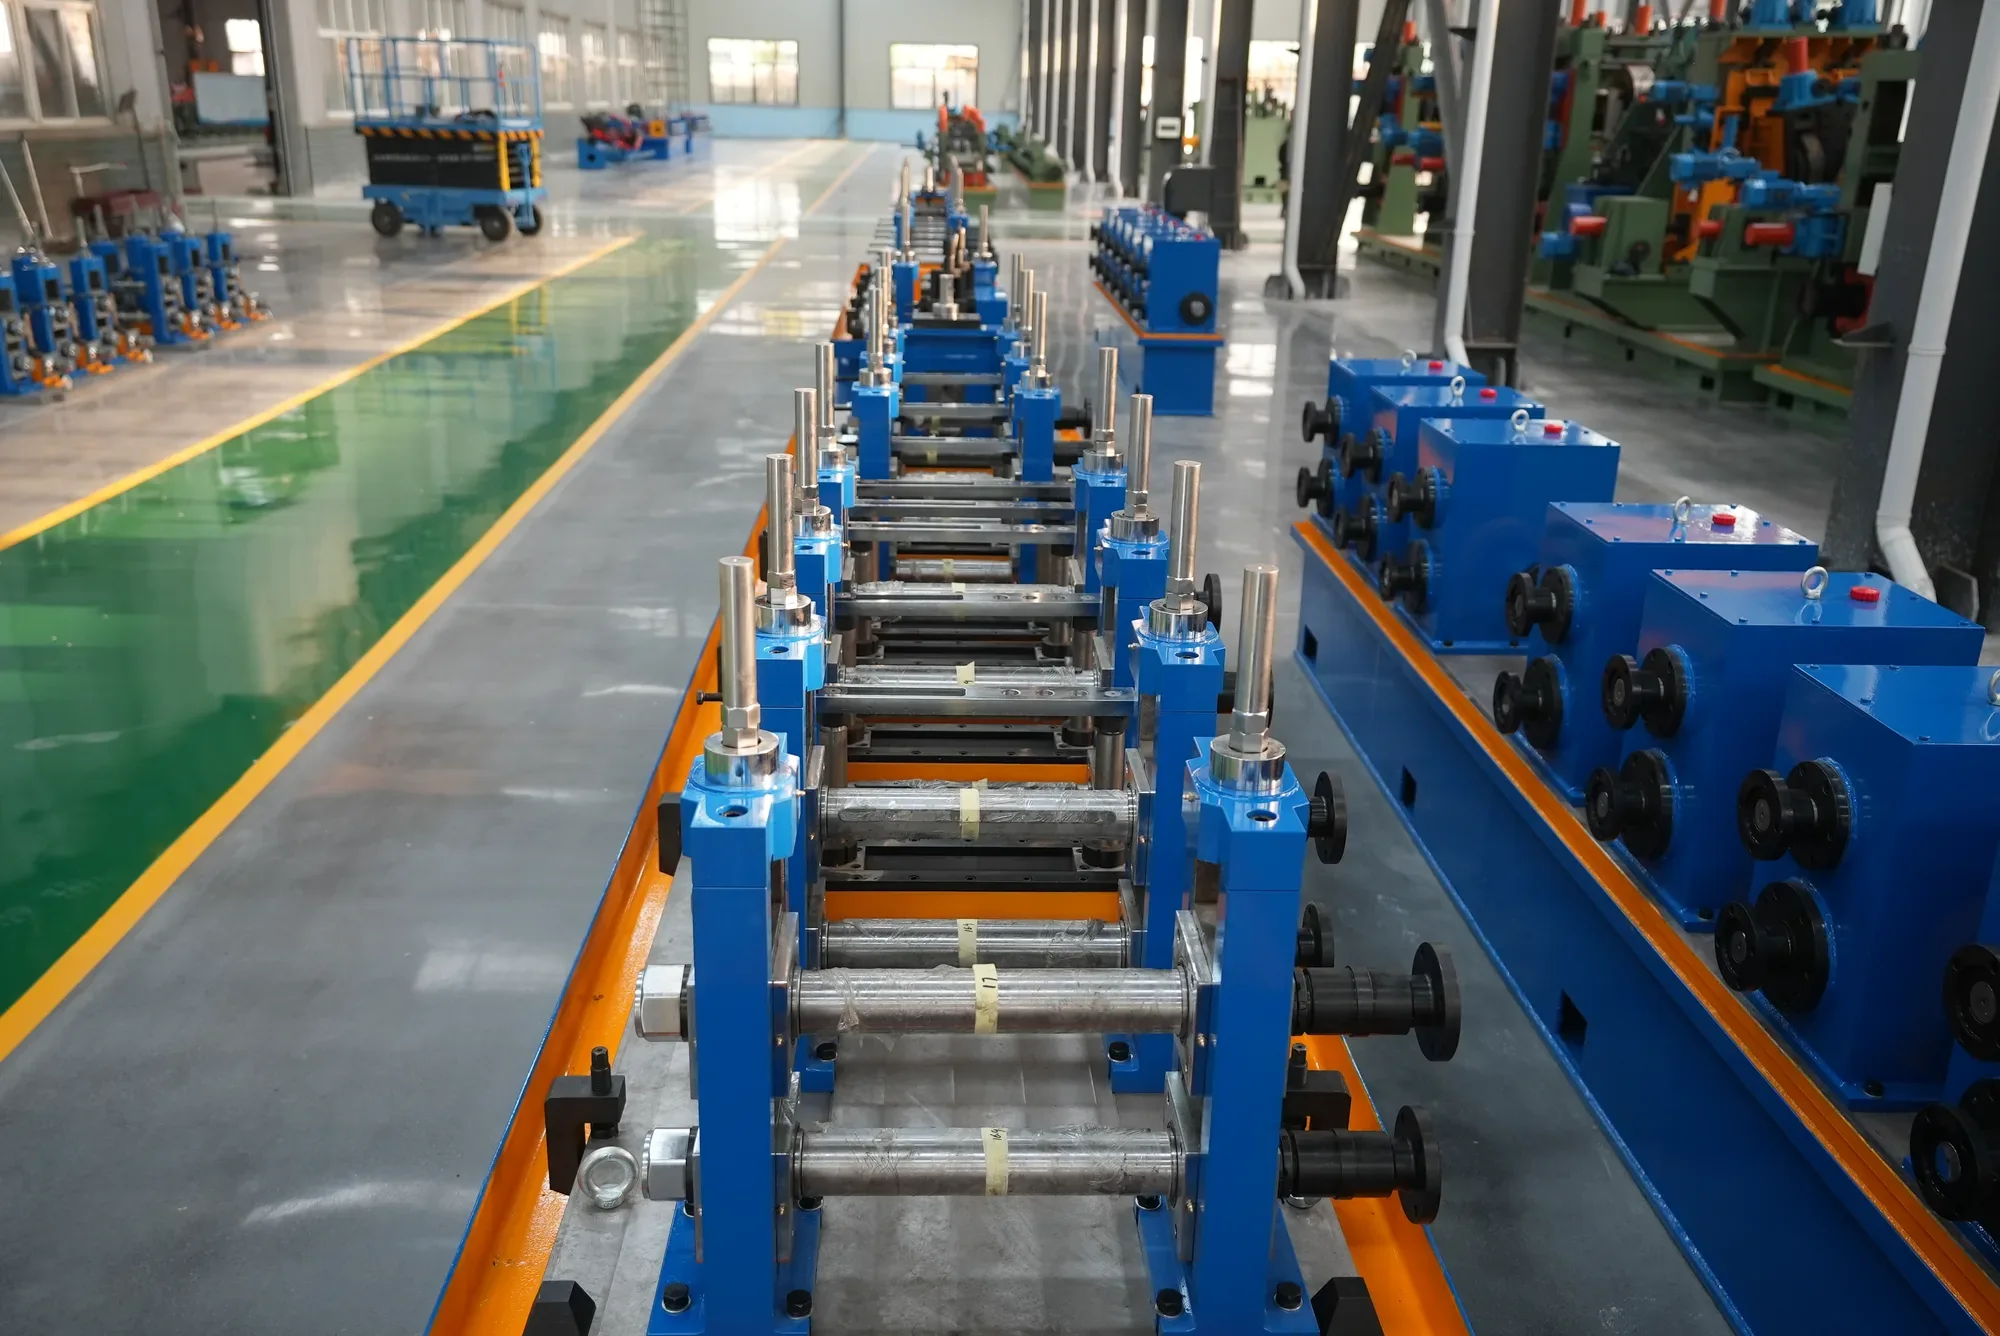
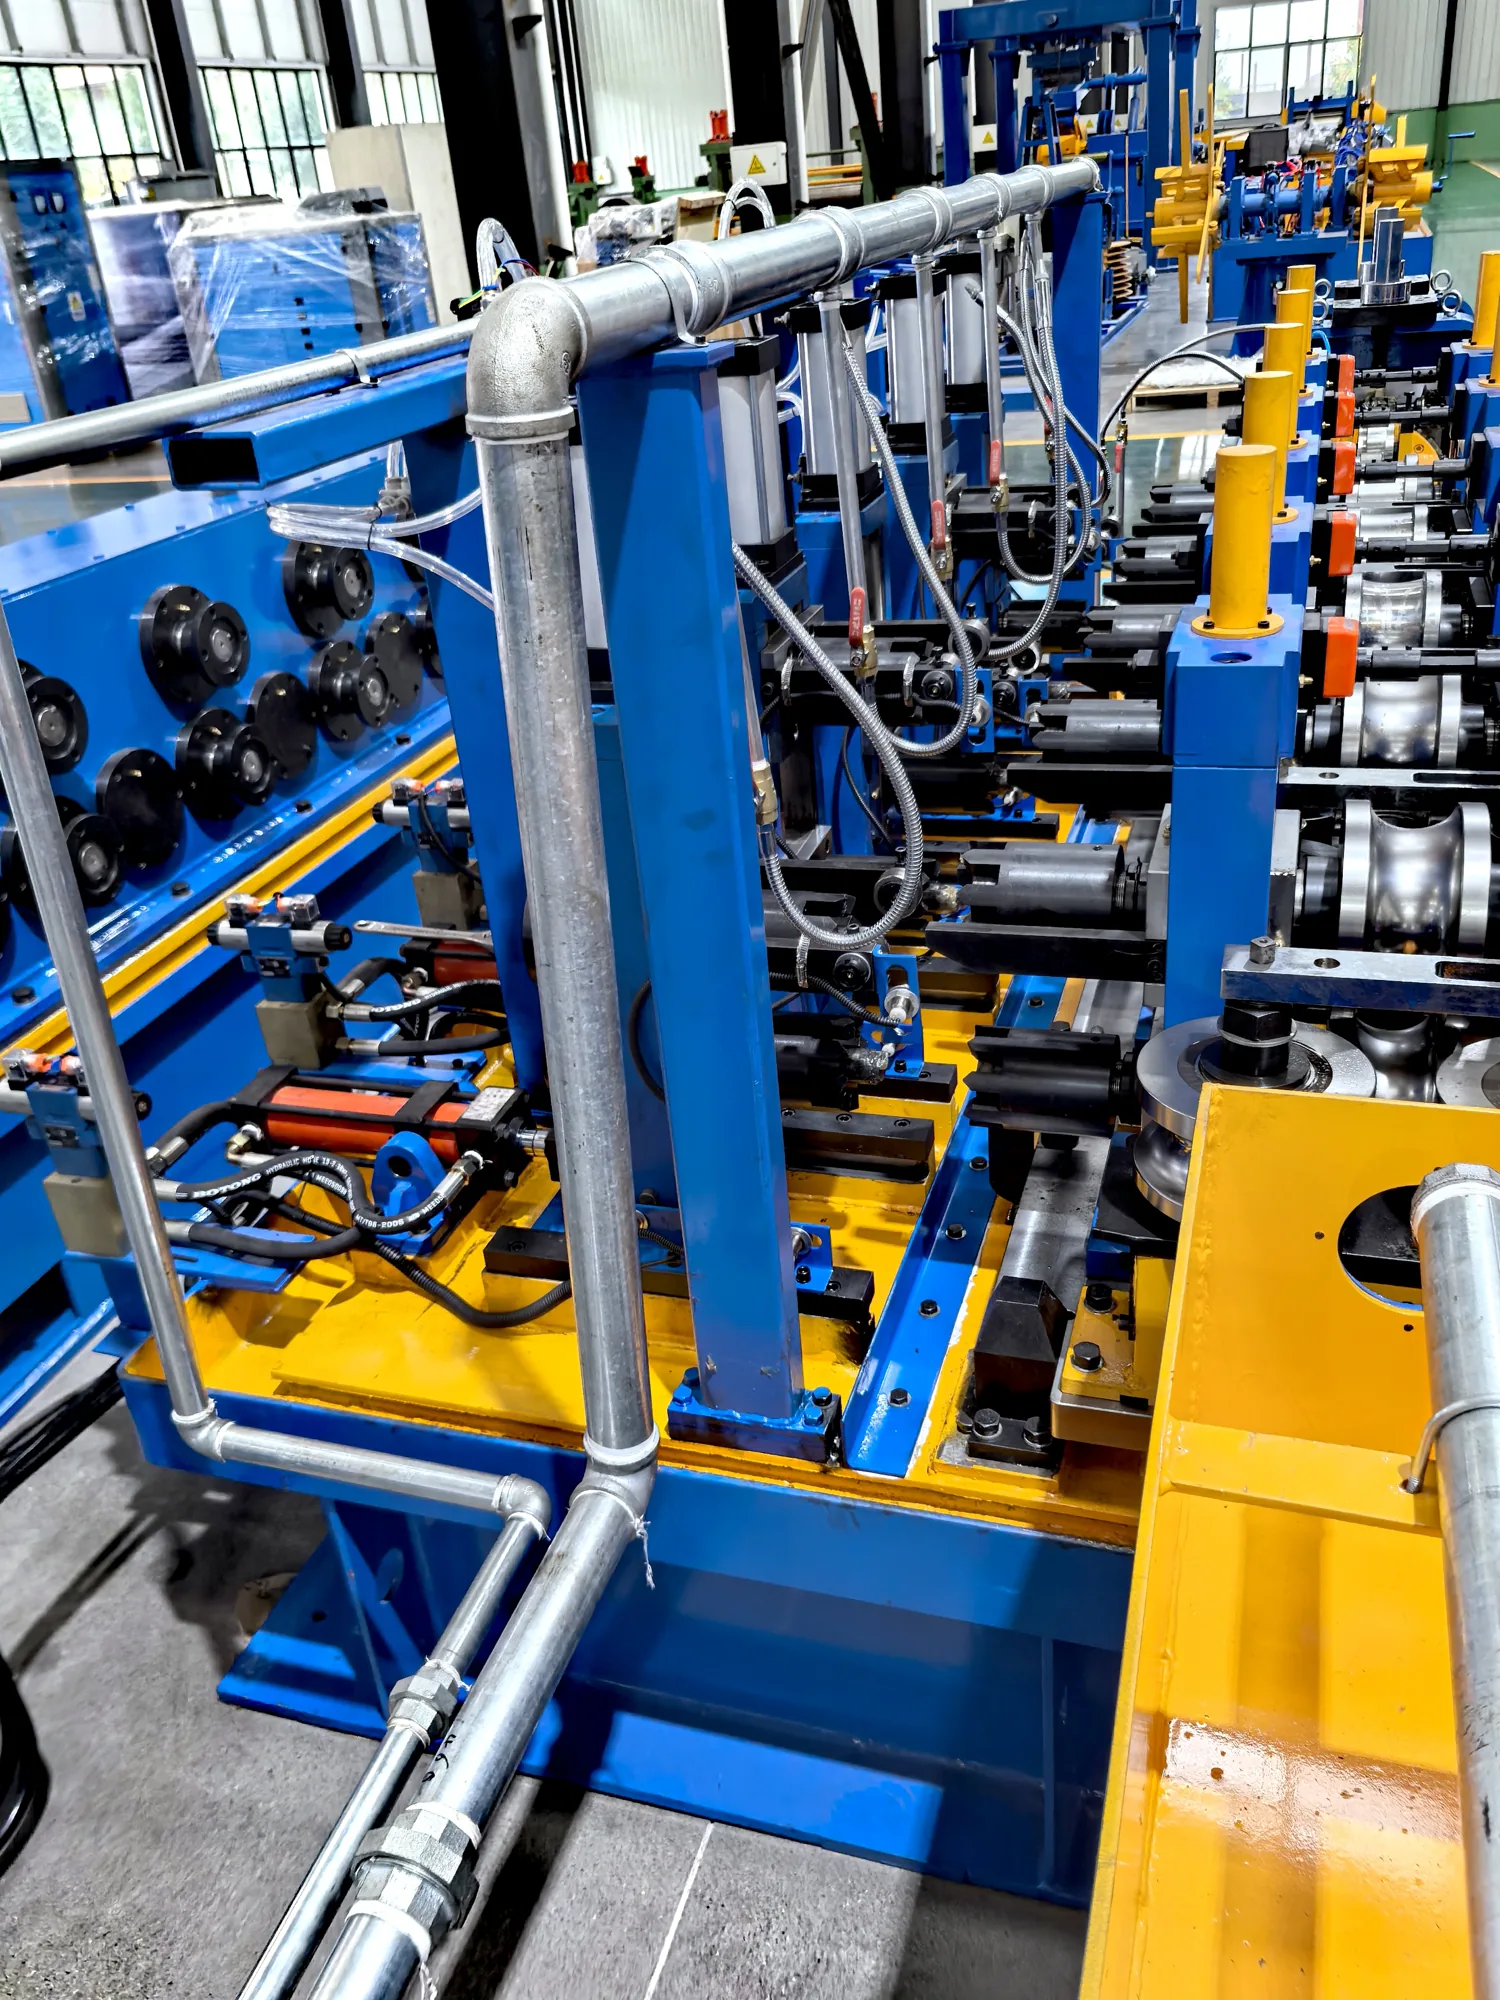 Small-Diameter Tube Mill
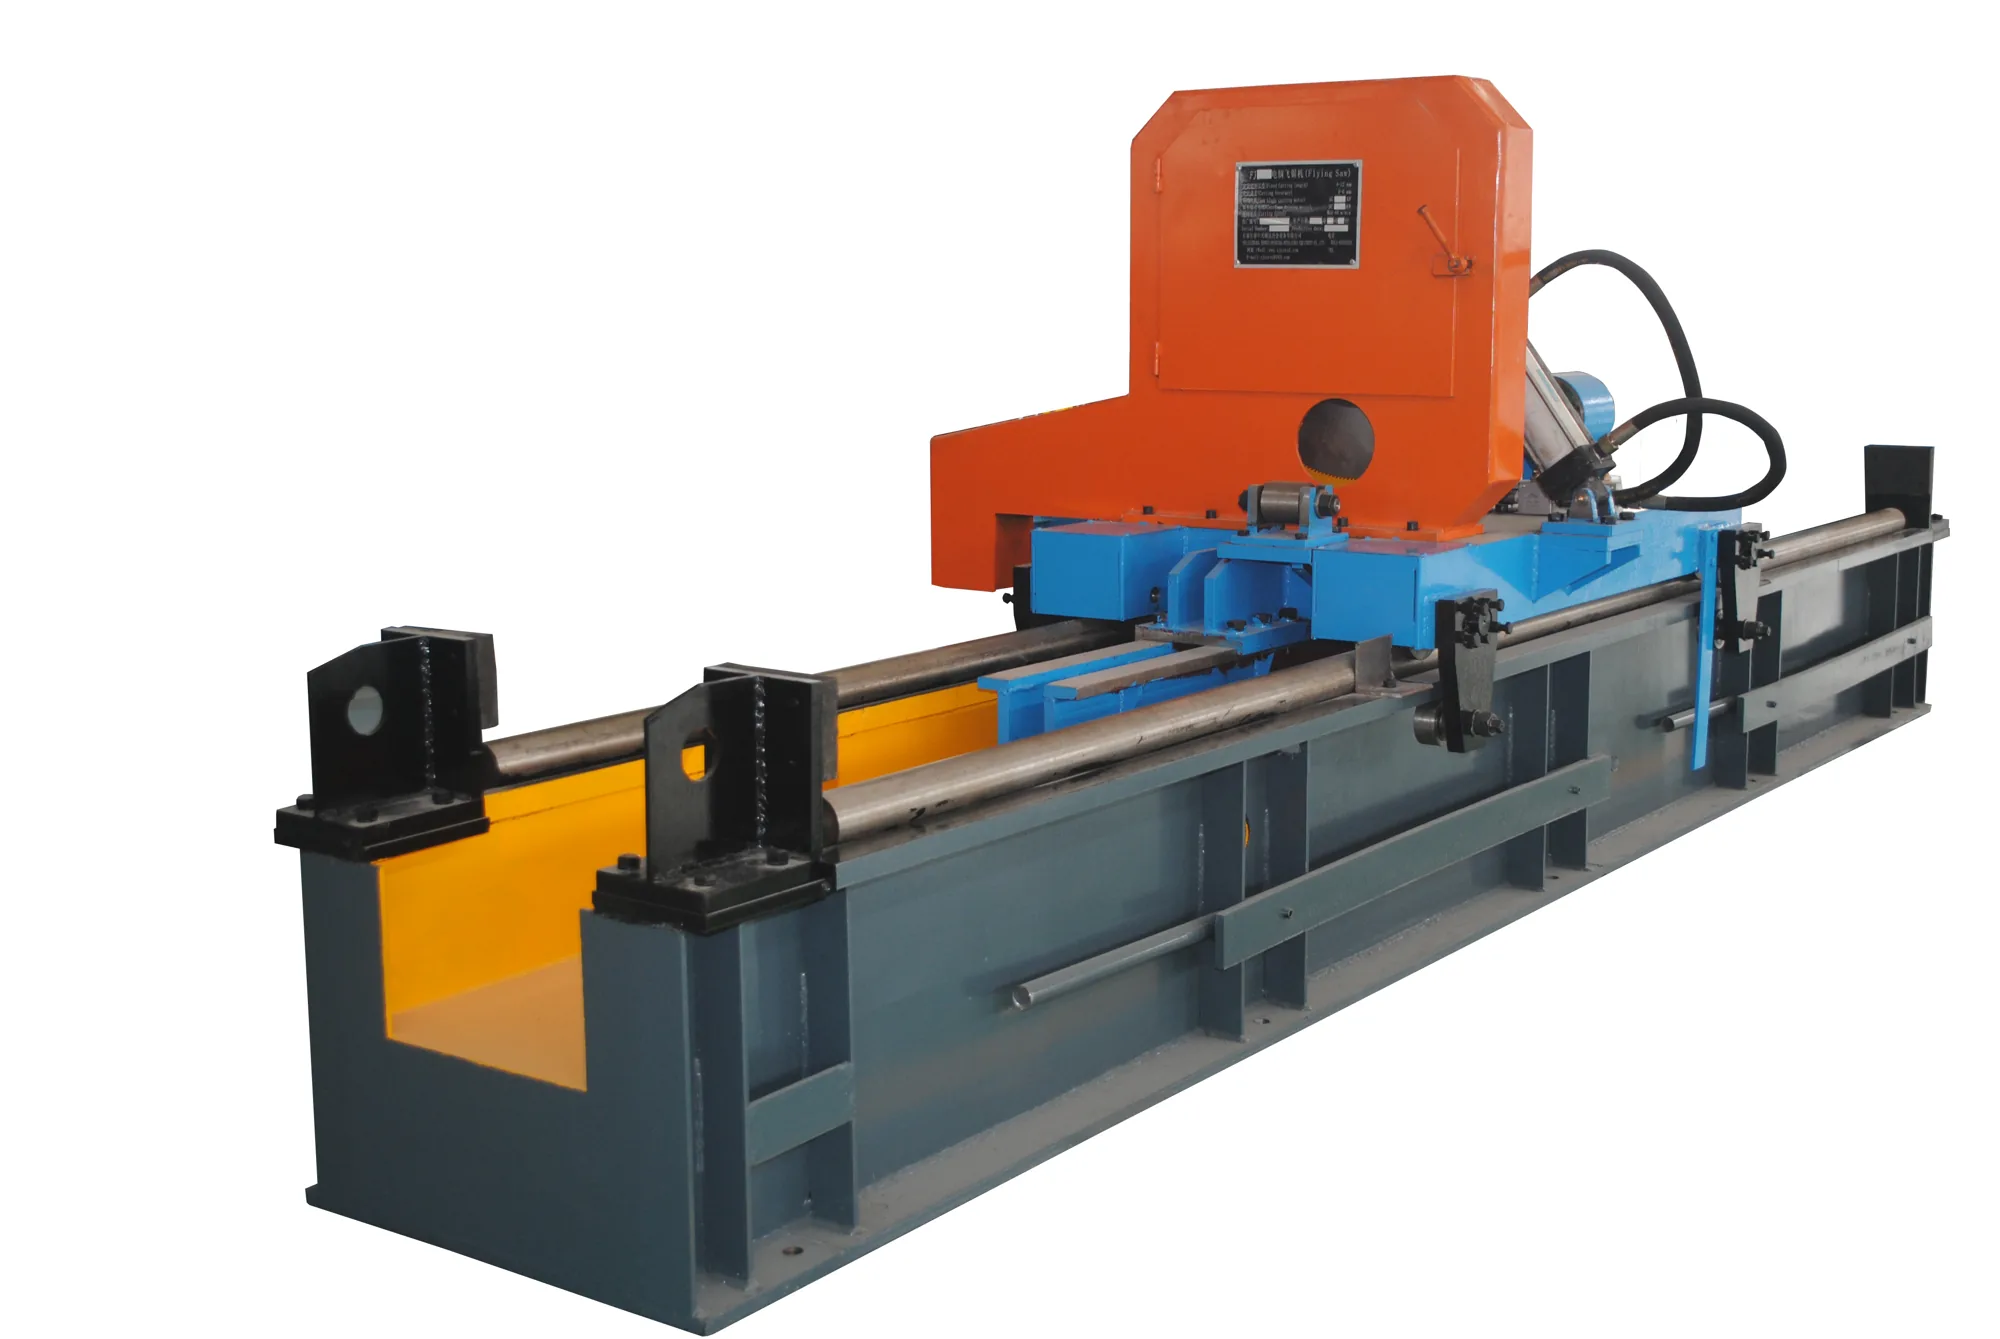 Large-Diameter Tube Mill
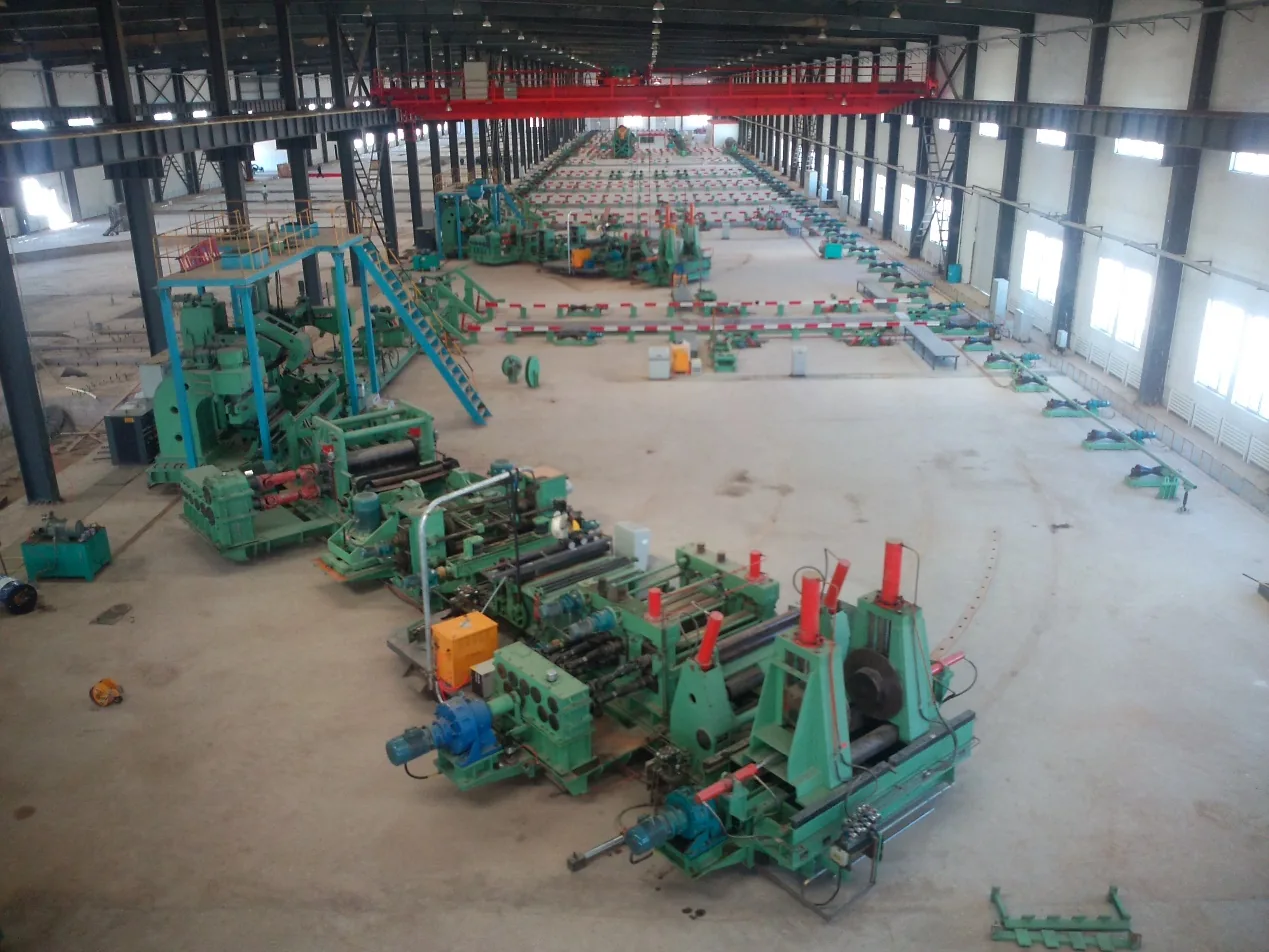 SSAW Spiral Welded Pipe Mill
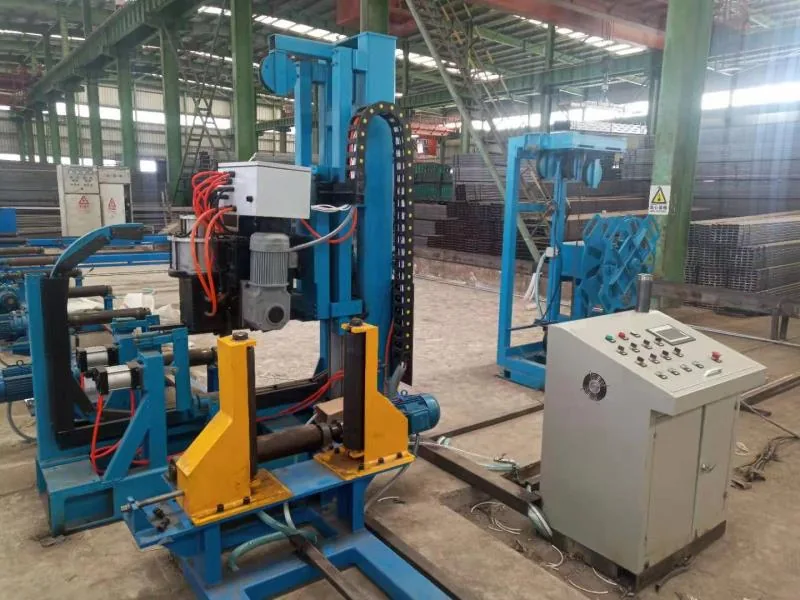 Direct-Forming Square Tube Mill
Send Your Enquiry
Tell us the pipe outside-diameter range, the wall thickness and the output you need. An engineer reads every enquiry — it does not land in a general sales inbox.